Industrial Dispersants for Pigments and Fillers: How to Improve Stability and Flow
Why Dispersants Matter in Real Production
Industrial dispersants are often treated as a minor formulation add-on, but operators know the practical reality: if pigments and fillers do not stay properly dispersed, everything downstream becomes harder. Viscosity drifts, color strength becomes uneven, settling starts in storage, pumps work harder, and batches that looked acceptable at the tank stage fail later in coating, ink, plastic, or construction material use.
For production teams, the real question is not whether a dispersant exists, but whether it helps a formulation stay stable under the exact stresses of the process: mixing energy, temperature shift, shear, storage time, and the chemistry of the resin or binder system. That is where the choice of dispersant starts to affect yield, consistency, and rework.
What Operators Are Usually Trying to Solve
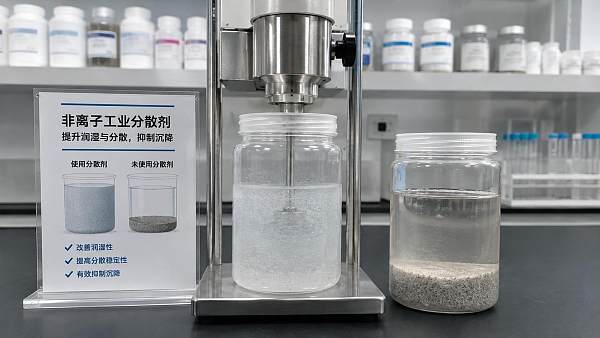
When people search for Industrial Dispersants, they are usually trying to fix one of a few recurring problems. Pigments may not wet out quickly enough, causing floating powder or persistent agglomerates. Fillers may settle before use. High-solids systems may become too thick to pump. Or a formulation may appear smooth in the lab but show instability after transport or a few days on the shelf.
The underlying issue is simple: solid particles need to remain separated and compatible with the surrounding liquid phase. A good dispersant helps create and maintain that separation. But it only works well when it matches the particle surface, the binder chemistry, and the way the formulation is processed.
Stability Is More Than “No Settling”
In production, stability has several layers. Visual settling is only the most obvious one. A system can look acceptable in the drum and still show hard sediment, flocculation, viscosity drift, or color shift later. That matters because many plants do not lose money on the first batch failure; they lose it on inconsistent repeat runs, blocked lines, cleaning time, and customer complaints that arrive after shipment.
For pigments, poor dispersion often shows up as weak tint strength, shade variation, or poor gloss development. For fillers, it can appear as poor flow, abrasive buildup, or inconsistent packing density. In both cases, dispersant performance is tied to particle wetting, electrostatic or steric stabilization, and compatibility with the full formulation package.
How Dispersants Improve Flow
Flow improvement is not just a convenience issue. It affects how easily a formulation can be mixed, transferred, pumped, filled, or applied. When particles are poorly dispersed, the system behaves like a network of clusters rather than a controlled suspension. That raises apparent viscosity and can make a product feel heavy or inconsistent during processing.
A suitable dispersant reduces particle-particle attraction and helps keep the solids separated. The result is usually better fluidity at the same solids loading, and in some systems, lower energy demand during mixing. That does not mean every formulation should chase the lowest viscosity possible. Too much thinning can hurt anti-settling behavior or film build. The target is controlled flow, not just easier pumping.
Where Selection Goes Wrong
Many formulation failures come from assuming dispersants are interchangeable. They are not. Two products that both improve dispersion may behave very differently once temperature, pH, electrolyte load, resin type, or grinding method changes.
- A dispersant that works in one resin system may destabilize another.
- A product that helps during milling may hurt long-term storage stability.
- Overdosing can sometimes increase foam, shift viscosity, or create compatibility issues.
- Underdosing often looks fine initially, then fails after aging or transport.
Operators should be cautious about any claim that a single dispersant “works universally.” In practice, the best choice depends on the pigment or filler surface, the carrier medium, and whether the product must survive high shear, heat, freeze-thaw, or extended storage.
Practical Selection Criteria
A useful selection process starts with the solids, not the marketing sheet. Ask what particles are being dispersed, what the particle size distribution looks like, and whether the issue is wetting, deagglomeration, stabilization, or all three. Then check what the formulation needs to do after mixing.
Why Lab Success Does Not Always Scale
One of the most common mistakes is assuming a dispersant that performs well in a beaker will behave the same in a plant tank. Scale changes the stress profile. Mixing zones are less uniform, residence time changes, and solids addition sequence becomes more important. A product that disperses quickly in the lab may still leave defects if it cannot tolerate the plant’s actual shear conditions or addition order.
This is especially relevant for high-solids coatings, inks, and construction materials, where process windows are narrower. If the formulation depends on a tight balance between viscosity, stability, and application behavior, operators should test under realistic mixing and hold conditions, not only under ideal lab conditions.
What to Watch During Trials
When evaluating Industrial Dispersants, the most useful trial data often comes from simple operational checks rather than complex claims. Look at wetting speed, grind quality, viscosity over time, sediment behavior, and how easily the batch can be remixed after storage. Also check whether the dispersant changes color development, gloss, opacity, or film uniformity in the final application.
It helps to keep the trial structure disciplined:
- Use the same raw materials and mixing order across comparisons.
- Measure viscosity immediately and after aging.
- Check bottom-settling or hard-pack formation after storage.
- Compare application behavior, not only tank appearance.
- Document any foaming, odor, or unexpected compatibility shift.
Compliance and Supply Risk Also Matter
In many industries, dispersant selection is no longer just a technical choice. Regulatory status, environmental profile, and supplier consistency can affect whether a formulation is viable at scale. Some systems need to avoid restricted surfactant families, formaldehyde-related concerns, or ingredients that complicate downstream customer approvals. In other cases, the main risk is not regulation but supply continuity and batch-to-batch drift.
That is why procurement and operations should look beyond the technical datasheet. Confirm the supplier’s consistency, the available documentation, and whether the product fits the target market’s compliance expectations. For export-oriented operations, this can matter as much as the dispersion performance itself.
When a More Expensive Dispersant Is Actually Cheaper
Low-cost options can be attractive, but price per kilogram is a weak metric if the additive forces more rework, longer mixing time, or higher scrap rates. A better dispersant may allow higher loading, fewer defects, lower energy use, and more stable inventory. In that case, the formulation cost rises on paper while total operating cost falls in practice.
For operators, the right comparison is not additive price alone. It is total impact on throughput, batch consistency, storage stability, and final customer acceptance. If the dispersant saves one failed batch or one round of reprocessing, it may already have paid for itself.
A Practical Way to Think About It
The most reliable Industrial Dispersants are the ones that fit the job tightly. They should help the solid phase wet quickly, keep particles apart during processing and storage, and preserve the final properties the product is supposed to deliver. If any one of those three fails, the formulation is still vulnerable.
For operators handling pigments and fillers, the decision should be based on actual plant conditions, not generic claims about “better dispersion.” The right question is whether the additive improves the specific process you run today, under the stability window your customer will actually see. That is where the value is, and that is where most of the risk is hidden.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+