How High Purity Aspartame Supports Consistent Zero-Calorie Formulas
Purity Is a Formula-Control Variable, Not Just a Purchasing Specification
In zero-calorie beverages, dairy products, tabletop sweeteners, and nutrition-focused foods, aspartame is often discussed in terms of sweetness intensity and cost-in-use. For quality control and safety teams, that is only part of the picture. The practical question is whether the supplied material will deliver the same sensory, processing, and compliance outcome across production runs.
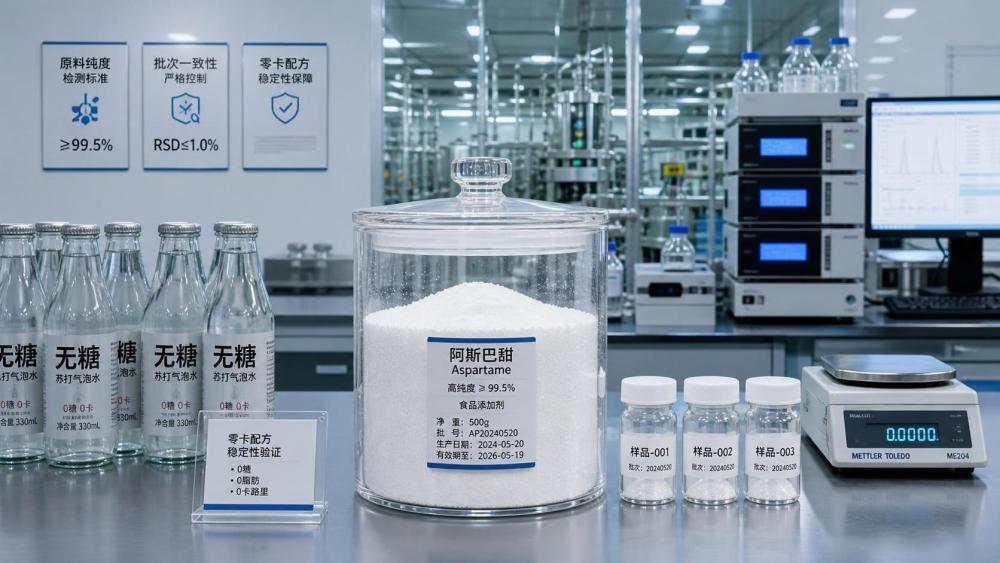
That is where high purity aspartame becomes operationally important. Purity is not simply a number on a certificate of analysis. It influences sweetness consistency, the probability of off-notes, the behavior of the sweetener during storage and processing, and the confidence with which a manufacturer can release finished goods. In a formula with little or no sugar to mask variation, small differences in raw-material quality can become visible to consumers much faster than teams expect.
For a quality manager, the relevant issue is not whether a material meets a generic assay limit in isolation. It is whether its complete quality profile is controlled well enough for the intended formula, manufacturing process, packaging format, market destination, and shelf-life target.
Why Zero-Calorie Formulas Expose Raw-Material Variation
Sucrose contributes more than sweetness. It provides bulk, mouthfeel, solids, and some sensory buffering. When sugar is removed, formulations commonly become more sensitive to the characteristics of high-intensity sweeteners, acid systems, flavors, stabilizers, and processing conditions. A variation that might be difficult to notice in a conventional sweetened product can become pronounced in a zero-calorie product.
Aspartame has a clean sweetness profile in many applications, but its performance is affected by the matrix around it. Beverage acidity, thermal exposure, moisture level, storage temperature, flavor composition, and the presence of other sweeteners can all shape the final sensory result. Material with a tightly controlled impurity profile gives formulators a more stable starting point. Material that only narrowly meets a basic specification may create more uncertainty, particularly when the product is positioned around a familiar flagship taste profile.
This is why teams should avoid treating “food-grade” as a complete suitability assessment. Food-grade status is necessary, but it does not answer every practical question. Two materials can both be eligible for food use and still differ in batch consistency, particle characteristics, flow behavior, trace impurity control, sensory neutrality, packaging protection, and documentation quality.
For safety and QC teams, a useful framing is simple: a finished formula can only be as consistent as the critical raw materials that enter it. In low-dose ingredients, this principle is sometimes underestimated because the inclusion rate is small. Yet high-intensity sweeteners can have an outsized sensory effect precisely because small changes in concentration or composition matter.
The Quality Attributes That Matter Beyond Assay
Assay remains a central release criterion, but it should sit within a broader control package. The precise specification limits should be determined by applicable food regulations, customer requirements, internal risk assessment, and validated application needs. A procurement specification copied from a general supplier sheet is rarely sufficient for a high-volume or brand-sensitive zero-calorie program.
The table does not mean that every batch requires every possible test. It means that a risk-based program should define what must be verified routinely, what can be qualified through supplier assurance, and what triggers expanded investigation. A tabletop sweetener packed in a low-moisture environment does not face exactly the same risk profile as a ready-to-drink acidic beverage stored through a warm distribution chain.
Related substances deserve particular attention. It is tempting to see them only as analytical compliance items, but their practical significance depends on both level and application. A quality team should understand which related substances are monitored, how the supplier identifies and quantifies them, whether the analytical method is stability-indicating, and whether trend data show a stable manufacturing process. A certificate reporting a passing result is useful; a quality system that can explain control of the result is more valuable.
Method comparability also matters when an ingredient changes supplier, plant, or analytical laboratory. Results generated by different methods may not be directly interchangeable even when they use the same parameter name. Before changing specifications or approving an alternate source, technical teams should confirm method suitability, sample preparation, reference standards, detection capability, and the way results are calculated and rounded.
Process Conditions Can Change the Real Risk
High purity aspartame cannot compensate for an unsuitable process. Its value is best understood as a foundation for control, not as a guarantee that every formulation will remain stable under any condition.
In beverages, formulation pH, heat treatment, holding time, and storage temperature are especially relevant. In powdered applications, moisture ingress, premix segregation, and local concentration differences may become more important. In dairy and nutritional products, the interaction with proteins, flavors, minerals, hydrocolloids, and other sweetening systems should be evaluated in the actual product matrix rather than inferred from a simple water solution.
One frequent misconception is that a higher assay figure automatically means a longer shelf life. It may reduce one source of variation, but shelf life is a system outcome. Degradation pathways can be influenced by temperature, moisture, pH, oxygen exposure, packaging headspace, and interactions with other ingredients. A product can use a high-purity material and still develop sensory drift if its processing or packaging conditions are poorly matched to the formula.
Another common assumption is that a sweetener replacement can be assessed through a single bench-top taste comparison. This can identify major sensory differences, but it does not establish manufacturing equivalence. The evaluation should include pilot-scale mixing, heat exposure where relevant, finished-product aging, package-specific storage, and sensory review at multiple points in shelf life. For products distributed across climates, the storage study should reflect realistic distribution stress rather than only ideal laboratory conditions.
What a Robust Incoming-Control Program Looks Like
Incoming control should be designed around risk, supplier maturity, and the criticality of the ingredient in the finished product. A highly standardized, well-documented source with a strong performance history may justify reduced routine testing under an approved supplier program. A new source, a source change, an unusual lot, or an ingredient intended for a sensitive application may require more extensive verification.
A practical program usually combines documentary review, physical inspection, analytical confirmation, and traceability checks. The exact balance depends on the company’s food safety plan and applicable requirements, but several questions should be answered before lot release:
- Does the certificate of analysis correspond clearly to the delivered lot, manufacturing date, retest or expiry date, and approved specification?
- Has the material arrived in packaging that protects it from moisture, contamination, damage, and mix-up?
- Are seals, labels, pallet configuration, and transport records consistent with the approved supplier and shipment conditions?
- Does the lot meet identity, assay, moisture, and other critical parameters using qualified methods or justified supplier verification?
- Has the supplier reported any manufacturing, raw-material, process, analytical, packaging, or site changes that could affect equivalence?
- Are retention samples stored under conditions that allow meaningful complaint or deviation investigation later?
Sampling deserves the same discipline as testing. A representative result cannot be obtained from an unrepresentative sample. Powder ingredients may segregate during transport or handling, and a sample taken only from an accessible surface may fail to reveal variation within the container or lot. Sampling plans should define container selection, sampling tools, prevention of cross-contamination, composite-sample rules, sample quantity, chain of custody, and safe handling requirements.
For safety managers, the dust aspect should also be considered. Aspartame is used in relatively small amounts, but powder handling can still create exposure, housekeeping, and cross-contact concerns. Controls should be proportionate to the site risk assessment: closed transfer where justified, local extraction, appropriate cleaning validation, labeled utensils, controlled staging, and procedures that prevent ingredient mix-up. The goal is not to impose unnecessary complexity; it is to make a small-dose critical ingredient reliably manageable in a real plant environment.
Supplier Qualification Should Test the System, Not Only the Sample
A single conforming sample is evidence of a sample. It is not proof of a controlled supply system. When approving a supplier of high purity aspartame, procurement and quality teams should examine whether the producer can maintain the required profile over time and communicate effectively when conditions change.
Key review areas include manufacturing-site controls, raw-material traceability, change management, deviation handling, corrective and preventive action processes, lot-release authority, storage conditions, complaint response, and document availability. Depending on the market and product category, teams may also need to review food safety certifications, allergen and genetically modified organism statements where relevant, contaminant declarations, origin information, and regulatory status for destination countries. Specific certificate or regulatory requirements should be verified against the current jurisdictional rules rather than assumed from a supplier’s general marketing material.
Supplier resilience is part of quality assurance as well. A material can be technically acceptable but commercially risky if lead times are unpredictable, packaging formats are not standardized, transportation routes expose it to unsuitable conditions, or there is no qualified alternate source. For a zero-calorie formula with a highly recognizable taste target, changing sweetener source under supply pressure can become a significant product risk. The best time to establish comparability data and contingency plans is before a disruption occurs.
Application Fit Requires More Than a Pass/Fail Specification
Quality specifications should be connected to the application’s failure modes. A beverage producer may prioritize dissolution behavior, sensory neutrality, heat-and-acid stability, and low lot-to-lot variability. A dry-blend manufacturer may focus more heavily on particle-size compatibility, blend uniformity, dust control, and moisture protection. A nutrition-product manufacturer may require heightened attention to documentation, traceability, and compatibility with a more complex ingredient system.
This distinction matters because specifications can otherwise become either too vague or unnecessarily restrictive. A vague specification leaves quality teams unable to investigate drift. An overly restrictive specification can exclude capable suppliers without improving the finished product. The most useful approach is to translate actual product risks into measurable controls, then review whether those controls are meaningful in routine production.
For example, a complaint about “reduced sweetness” should not automatically lead to a request for a higher assay target. The investigation should examine dosing accuracy, premix homogeneity, formula version control, scale calibration, flavor variability, process losses, storage conditions, and sensory-panel methodology alongside the ingredient certificate. In many cases, the issue is not a single failing parameter but an interaction between process variation and a formula with limited tolerance.
Documentation Is Part of Release Readiness
For safety and quality teams, documentation is not an administrative afterthought. It is the evidence that supports release decisions, customer inquiries, audits, and incident response. A well-managed aspartame supply program should allow the business to connect a finished batch to its ingredient lots, confirm the specification in force at the time of manufacture, identify the relevant certificates and test results, and reconstruct any change history.
Document control is especially important when products are supplied across multiple markets. Permitted uses, labeling expectations, additive designations, and customer requirements may differ by jurisdiction or evolve over time. A statement that was suitable for one destination or customer may not be sufficient for another. Regulatory affairs, quality, and commercial teams should therefore agree on a current document set and an ownership model for reviewing it. Where requirements are uncertain, the correct position is to verify them before release rather than rely on precedent.
Clear documentation also helps distinguish an acceptable deviation from a potentially material change. A minor revision to a certificate format may have little relevance. A change in production site, purification route, assay method, packaging material, or retest period may require formal quality assessment and, in some cases, application confirmation before approval.
The Decision Standard Should Be Consistency Under Real Conditions
High purity aspartame is worth attention because zero-calorie products are often judged on consistency more sharply than on ingredient novelty. Consumers expect the same sweetness, flavor balance, and product experience each time they purchase a familiar beverage, dairy item, or nutrition product. Meeting that expectation depends on more than selecting a material with an impressive assay value.
The stronger decision framework asks whether the ingredient is controlled, traceable, compatible with the formula, stable enough for the intended process and shelf life, and supported by a supplier system that can sustain performance. When purity is evaluated in that broader context, it becomes a useful quality-management tool rather than a number that disappears into a purchasing specification.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+