How Locust Bean Gum for Yogurt Improves Texture and Stability
A stable yogurt texture begins with control of the water phase. During fermentation and refrigerated storage, the protein network can contract and release serum, creating visible whey separation or a thin layer around the product. Locust bean gum for yogurt is used to hold water within the structure, reinforce body, and create a smoother spoon feel without relying on excessive total solids. Its effect is most apparent when the base must remain uniform after filling, transport, and normal temperature variation in the chilled chain.
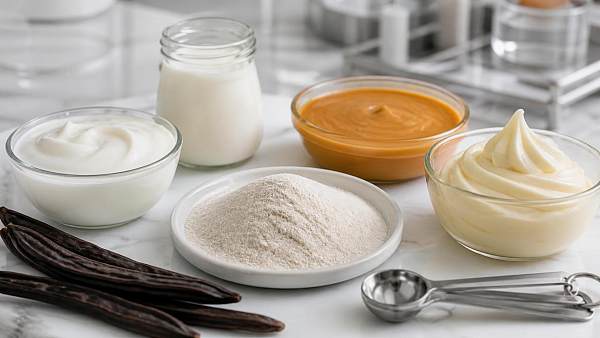
Locust bean gum is a galactomannan obtained from carob seed. In a yogurt formulation, it hydrates in the aqueous phase and increases viscosity through long-chain polymer interactions. The gum does not replace the acid gel formed by milk proteins during culture fermentation. Instead, it supports that gel by limiting serum mobility and contributing a fuller, less brittle texture. This distinction matters in troubleshooting: a stabilizer can improve water retention, but it cannot correct weak milk solids, unsuitable heat treatment, poor homogenization, or an unstable fermentation profile.
Texture Depends on the Whole System
Yogurt is not a simple thickened liquid. Its final body comes from protein concentration, heat history, homogenization pressure, fat level, culture activity, final acidity, shear after fermentation, and the stabilizer system. A gum that performs well in a high-solids stirred yogurt may behave differently in a low-fat drinkable yogurt or in a fruit-prepared cup product.
In set yogurt, the protein gel forms after filling and should remain relatively undisturbed. Locust bean gum can contribute to water management, but excessive agitation before or after incubation may still fracture the gel. In stirred yogurt, controlled breaking and smoothing of the fermented gel are part of the process, so the gum is often valued for rebuilding apparent viscosity and reducing the watery appearance that can develop after pumping. In drinkable yogurt, the target is usually suspension and a clean, pourable flow rather than a spoon-standing body. The same gum level that suits a spoonable product can make a beverage too heavy or produce an uneven mouthfeel.
Its interaction with other hydrocolloids also changes the result. Locust bean gum may be paired with pectin, starch, carrageenan, or another permitted stabilizing material depending on the formulation target and local labeling framework. Some combinations create useful synergy; others can give a short, gel-like texture, excessive thickness, or instability if the hydration and acidity conditions are poorly matched. A blend should therefore be evaluated as a system, not treated as a collection of independent ingredients.
Hydration Is Where Many Problems Start
Locust bean gum generally requires sufficient heat and time to hydrate effectively. If powder is added directly into cool milk with limited mixing, particles can wet on the outside and form lumps with dry centers. Those particles may remain visible after processing or hydrate slowly during storage, causing late viscosity changes. A product that looks acceptable at filling may then become thicker, less smooth, or inconsistent between batches.
A common processing route is to preblend the gum with dry ingredients such as sugar, milk powder, or another compatible powder before introduction to the liquid phase. The dry blend is added slowly into a well-agitated vortex, followed by a heating step designed to hydrate the gum and support the required dairy processing treatment. The exact temperature, hold time, addition rate, and mixer configuration need to reflect the specific gum grade, solids level, and plant equipment.
High shear can improve initial dispersion, but it is not a substitute for complete hydration. Excessive shear after the gum has developed viscosity may entrain air, complicate deaeration, or alter the desired body. The practical objective is uniform wetting first, controlled hydration second, and only enough mechanical energy to remove agglomerates and establish a homogeneous base.
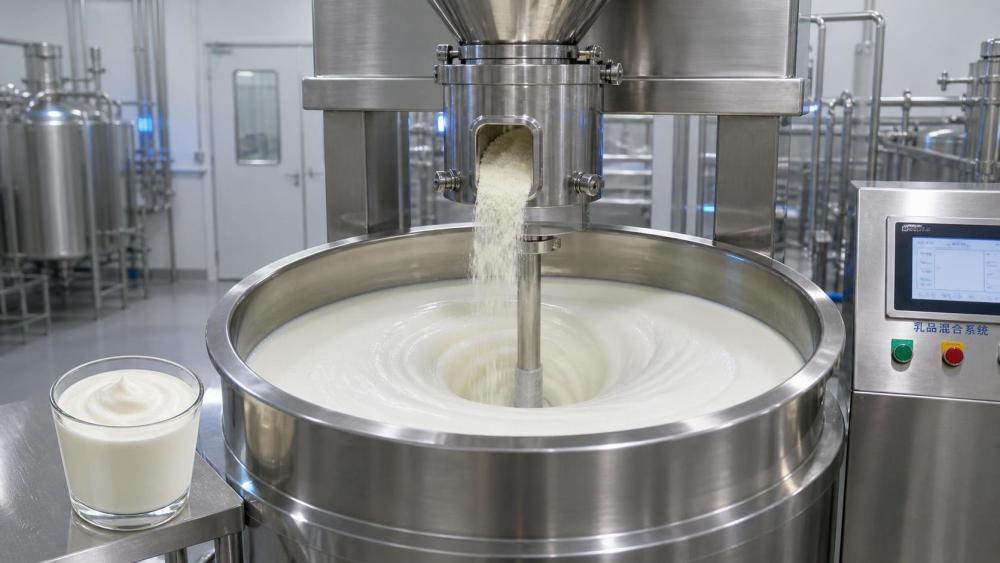
When trials produce small translucent lumps or a grainy texture, the cause is often traced incorrectly to fermentation. Before changing cultures or incubation settings, inspect the powder addition point, liquid temperature at dosing, agitation pattern, premix quality, and time between dispersion and the main heat treatment. A poor hydration event cannot usually be repaired later by adding more gum.
Managing Whey Separation Without Creating a Heavy Product
Whey separation, often called syneresis, is a visible sign that water is escaping from the protein network. It can occur immediately after filling, after several days in storage, or after mechanical stress during distribution. Locust bean gum can reduce the tendency by increasing serum-phase viscosity and restricting water movement. The result is normally most balanced when the gum level is aligned with milk protein, total solids, and the amount of fruit preparation or sweetener added after fermentation.
Adding more stabilizer is not always the right response. Overuse can produce a pasty, elastic, or overly dense texture that masks fresh dairy character. It may also reduce the perception of flavor release because the product remains longer in the mouth and coats the palate differently. An overly thick yogurt can be as commercially disruptive as a weak one when filling equipment, consumer expectation, or serving format requires a specific flow behavior.
The visual test should include more than a single unopened cup. Evaluate the product after filling, after chilled storage, after a defined period at a moderately elevated but controlled handling temperature, and after gentle inversion or spooning. Observe surface serum, body in the center of the cup, recovery after stirring, and the interface between a fruit layer and white mass where applicable. A formulation that appears stable at rest can still show separation after vibration or thermal cycling.
Sequence Around Fermentation and Fruit Addition
The stage at which ingredients enter the process affects stability. The gum is generally hydrated in the milk base before fermentation rather than dispersed into a finished acidic yogurt. Once the pH has fallen, hydration conditions are less favorable and any undispersed powder may form defects. The fermented base is then cooled according to the product process before it is stirred, blended, or combined with fruit preparation.
Fruit preparations add another layer of variability. Their sugar content, acidity, pectin level, particulate load, and water activity can affect local viscosity and water movement. A fruit component with a thin syrup may draw attention to serum release even if the yogurt base itself is stable. Conversely, a very thick fruit preparation can create a sharp texture transition that makes the dairy phase seem weak. Testing the white base alone is useful, but it does not replace testing the final assembled product.
For fruit-on-the-bottom products, the interface should be observed after chilled storage because migration can occur gradually. For blended products, mixing intensity needs careful control. Insufficient blending can leave uneven fruit distribution; aggressive blending can reduce the fermented gel structure and change apparent viscosity. Locust bean gum can provide resilience, yet it will not prevent texture loss caused by unnecessary post-acidification shear.
Choosing a Grade and Defining Incoming Controls
Commercial locust bean gum grades can differ in particle size, viscosity development, microbial specification, color, odor, and hydration behavior. A change in grade may alter process performance even when the stated ingredient name is unchanged. The specification should therefore include the properties that matter in the intended yogurt, rather than relying only on a general identity description.
- Particle size influences dispersibility and the risk of dusting or fisheyes during powder addition.
- Viscosity should be reviewed under a method relevant to the actual formulation, since a simple water test may not predict behavior in milk solids and acid conditions.
- Color and odor deserve attention in plain yogurt, where small sensory differences are easier to notice than in heavily flavored products.
- Microbiological limits, allergen status, origin documentation, and packaging integrity should be confirmed against the finished-product control program.
Incoming material should be kept dry, sealed, and protected from odor pickup. Hydrocolloid powders can absorb moisture during poor storage, which increases lumping and makes feeding less consistent. Open bags should be closed promptly, identified clearly, and used under a defined stock-rotation practice. During transport within the plant, avoid placing powder near wet washdown zones or strong-smelling raw materials.
Using Trials to Separate Cause from Symptom
A useful development trial changes one meaningful variable at a time. When the base is weak, altering gum dosage, culture rate, heat treatment, milk solids, and homogenization settings simultaneously may generate a result without revealing why it occurred. A more reliable sequence starts with a stable reference batch, then compares a small range of gum levels under identical processing conditions. After the preferred body is identified, test the effect of intended fruit preparation, filling temperature, storage time, and expected handling stress.
Record actual temperatures rather than relying only on equipment setpoints. Inadequate heating at the gum hydration stage, extended hold time before fermentation, or a delay between homogenization and incubation can all affect the final product. Likewise, measure pH and viscosity at consistent points in the process. Comparing readings taken at different temperatures or after different rest periods can create misleading conclusions.
Sensory review should include spoon resistance, smoothness, perceived creaminess, clean breakdown in the mouth, and any gummy or powdery note. Instrumental viscosity is useful for batch control, but two yogurts with a similar viscosity value can feel different because the flow curve and protein-gel structure are different. A short, clean body may suit one product style, while another requires a fuller, more cohesive texture.
Common Misinterpretations During Production
Visible whey is sometimes blamed entirely on insufficient stabilizer. In practice, low protein solids, excessive post-fermentation shear, unstable incubation temperature, weak heat treatment, or poor filling conditions may be the primary cause. Raising gum dosage without examining these factors can conceal the symptom while making the yogurt unappealingly heavy.
Another frequent error is judging the base only when warm. Viscosity and hydration expression change as the product cools, and cold storage reveals the behavior that matters at consumption. Evaluation should include the actual refrigerated condition and the intended shelf-life window, not just the tank sample.
Finally, a successful bench formula may not transfer directly to production equipment. Powder induction, shear exposure, heat-up rate, residence time, homogenizer performance, and transfer piping are all different at larger scale. A pilot or plant confirmation should focus especially on dispersion quality and the period after fermentation, where pumping and blending can alter the body built during incubation.
When locust bean gum is fully hydrated, matched to the yogurt style, and assessed with the complete process in view, it can support a stable, creamy product without forcing the formulation toward excessive thickness. The most dependable results come from treating gum selection, milk base preparation, fermentation control, and post-acidification handling as connected parts of one texture system.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+