How Food Hydrocolloids Improve Texture and Stability in Formulations
How Food Hydrocolloids Improve Texture and Stability in Formulations
Food hydrocolloids play a critical role in helping manufacturers achieve consistent texture, viscosity, moisture control, and shelf-life stability. In beverages, dairy products, sauces, bakery goods, meat systems, and prepared foods, a small change in the hydrocolloid system can alter how a product pours, sets, freezes, reheats, or feels in the mouth.
For production teams, the practical question is rarely “which thickener is strongest?” More often, it is whether the ingredient can deliver the intended texture without creating mixing problems, unwanted gel formation, sedimentation, syneresis, flavour masking, or batch-to-batch variation. The right choice depends on the complete formulation and process, not on viscosity data from a supplier specification alone.
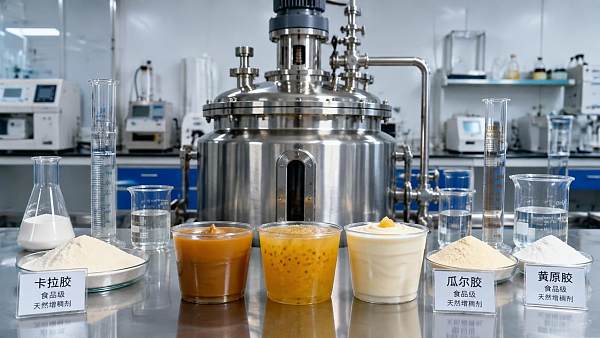
Food hydrocolloids include polysaccharides and certain proteins that interact with water to thicken, bind, suspend, emulsify, gel, or stabilize food systems. Common examples include xanthan gum, guar gum, locust bean gum, carrageenan, pectin, alginate, gellan gum, cellulose derivatives, starch-based systems, and microbial gums. Their functions may overlap, but their processing behaviour often differs sharply.
Texture Is a Formulation Outcome, Not a Single Ingredient Property
A hydrocolloid does not simply “make food thicker.” It changes the way water moves through the formula. By increasing viscosity or forming a structured network, it can slow particle settling, reduce serum separation, retain moisture, control ice crystal growth, improve cling on a surface, or create a specific bite and body.
This is why two products with a similar apparent viscosity can feel completely different. A xanthan-containing sauce may show strong shear-thinning behaviour: it remains thick at rest but becomes easier to pump, pour, or spread under movement. A starch system may provide a fuller, more familiar body but can be more sensitive to prolonged heating, acidity, or freeze-thaw stress. A pectin gel may give a clean cut and short texture, while a gum blend may create a more elastic or creamy perception.
The operator should therefore look beyond a single Brookfield viscosity value. Useful questions include: Does the product need to flow through filling equipment? Is it consumed cold or hot? Will it undergo retort processing, high-shear mixing, freezing, thawing, or repeated temperature cycling? Does the texture need to remain stable through the stated shelf life, rather than only immediately after production?
In many formulations, the best result comes from combining materials with complementary functions. One ingredient may establish viscosity, another may control water release, and an emulsifier may be needed to stabilize fat droplets. Treating a hydrocolloid as an isolated ingredient can lead to unnecessary dosage increases and a less acceptable final texture.
How Different Systems Behave in Practical Food Applications
In acidified beverages and fruit preparations, pectin is often selected because its behaviour can be matched to the pH, soluble solids, calcium level, and target texture of the system. However, the type of pectin matters. Some pectins require specific conditions to form a gel, while others can form gels in the presence of calcium. The process team needs to understand when and how the pectin is hydrated, since poor dispersion can create fisheyes or undissolved particles that are difficult to remove later.
For sauces, dressings, and seasonings, xanthan gum is frequently valued for suspension and viscosity under varying temperature conditions. It can help keep herbs, spices, or insoluble particles distributed through the product. Yet excessive use may produce a stringy or overly slick mouthfeel. In emulsified dressings, the hydrocolloid must also be considered alongside oil content, emulsifier type, homogenization conditions, salt level, and acid addition sequence.
Dairy and dairy-alternative products present another set of challenges. Hydrocolloids may support protein stability, reduce whey-off, improve spoonability, or help maintain a smooth texture after storage. But protein interactions can be highly formulation-specific. Changes in pH, mineral content, heat treatment, protein source, or flavour system may alter the outcome. A gum that performs well in one cultured product may be unsuitable in a high-protein beverage processed at a different temperature.
Bakery applications are often less about immediate viscosity and more about water management. Hydrocolloids can assist dough handling, gas retention, crumb softness, moisture retention, and frozen-dough tolerance. They may be particularly relevant where formulation changes have reduced gluten, fat, sugar, or egg content. Still, more water binding is not automatically better. A system that holds too much water can make a product gummy, interfere with oven spring, or alter the expected eating quality.
Stability Problems Usually Reveal a Process or Compatibility Issue
Separation, sedimentation, weak gel strength, viscosity loss, and syneresis are sometimes blamed on the hydrocolloid itself. In practice, the root cause may sit elsewhere: insufficient hydration time, incorrect order of addition, poor powder dispersion, excessive shear, a late pH adjustment, incompatible salts, or a mismatch between the processing profile and the selected grade.
Hydrocolloid powders often hydrate rapidly at the surface. If they are added directly to water without adequate agitation or premixing, the outer layer can hydrate first and trap dry powder inside a lump. This is a common operating problem. Dry blending with sugar, starch, salt, or another compatible powder may improve distribution, although the best approach depends on the formula. Some systems require hot processing for complete hydration; others are designed for cold-water use and can lose functionality if subjected to unsuitable conditions.
A useful development habit is to separate hydration testing from final-product testing. First confirm that the ingredient develops its expected functionality in a simple controlled base. Then test it in the real formulation, where sugar, salt, acids, proteins, fats, flavours, preservatives, and particulate ingredients can change the result. This prevents teams from drawing conclusions too early from a laboratory sample that does not reflect production reality.
Processing Conditions Can Change the Final Performance
The same hydrocolloid grade may perform differently on a bench mixer, a pilot line, and a full-scale manufacturing line. Scale changes affect mixing energy, powder induction, residence time, heating rate, cooling rate, and shear history. A stable pilot formulation can fail at plant scale if the powder is no longer properly wetted or if the product experiences more aggressive pumping and homogenization.
Temperature deserves close attention. Some materials require heat to hydrate fully; others build viscosity quickly under cold conditions. Acid may need to be added after hydration rather than before it. Calcium and other ions can be essential to a desired structure in some systems, but disruptive in others. Salt, sugar, alcohol, and high levels of soluble solids can alter water availability and change how quickly a gum develops viscosity.
Operators should record the actual process rather than only the intended recipe. That includes water temperature at addition, mixing speed, addition duration, hold time, pH before and after heat treatment, homogenization pressure where relevant, and fill temperature. These details are often more useful in troubleshooting than simply increasing dosage.
Selecting Food Hydrocolloids: What to Confirm Before Approval
A technical evaluation should begin with the target product experience: pourable, creamy, spoonable, elastic, gelled, aerated, or freeze-thaw stable. From there, the formulation team can define the operating conditions that the material must tolerate. A hydrocolloid suitable for a chilled dessert may not meet the needs of a shelf-stable sauce or an instant powdered beverage.
Before approving a material, it is sensible to review the following points:
- Intended functional role: thickening, gelling, suspension, moisture retention, emulsion support, or a combination of these.
- Compatibility with pH, salt, sugar, proteins, minerals, fats, acids, and other additives in the finished formula.
- Hydration conditions, including water temperature, mixing equipment, shear sensitivity, and required hold time.
- Performance after the full process: heating, cooling, filling, transport, storage, freezing, thawing, or reheating.
- Sensory impact, especially sliminess, gumminess, opacity, flavour release, and clean-label expectations.
- Specification consistency, microbiological requirements, allergen information where applicable, packaging integrity, storage conditions, and documentation for the target market.
Regulatory status and permitted use conditions should be verified for the relevant country or sales region. Food additive requirements may differ by market, food category, declared ingredient name, and use level. Product specifications may also need to align with customer standards, applicable food additive regulations, and recognized quality references used in the supply chain. This review should happen before final label design and commercial production, not after a formula has been locked.
Why a System View Is More Reliable Than Ingredient Substitution
Replacing one gum with another because of price, availability, or label preference can be reasonable, but it should not be treated as a one-to-one swap. Differences in molecular structure, particle size, hydration rate, viscosity profile, gel mechanism, and interaction with proteins or minerals can change the product noticeably. The cost per kilogram is only one part of the decision; effective dosage, process impact, yield, waste risk, and sensory acceptance also matter.
This is particularly relevant when supply conditions change. Procurement teams need a clear specification, but technical teams also need a defined acceptance method. A supplier’s certificate of analysis may confirm that a batch meets agreed limits, yet it does not replace a practical check in the intended formulation. Incoming quality controls should be relevant to function, not limited to appearance or basic identity.
Global Fine Chemicals & Agrochemical Intelligence Network (FCAS) approaches food ingredients through application performance, technical documentation, processing requirements, and supply-chain considerations rather than treating materials as isolated chemical names. For hydrocolloid users, that perspective is useful because texture issues often sit at the intersection of formulation design, production control, packaging, storage, and regulatory readiness.
The most dependable route is to define the sensory target, map the real process conditions, test stability over the intended product life, and document the variables that affect performance. When a formula fails, start with hydration, process sequence, pH, thermal history, and ingredient compatibility before assuming that more hydrocolloid is the answer. In many cases, a better-balanced system produces a more stable food with less compromise in texture.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+