Choosing Maltodextrin for Flavor Carriers in Dry Food Blends
Choosing Maltodextrin for Flavor Carriers in Dry Food Blends
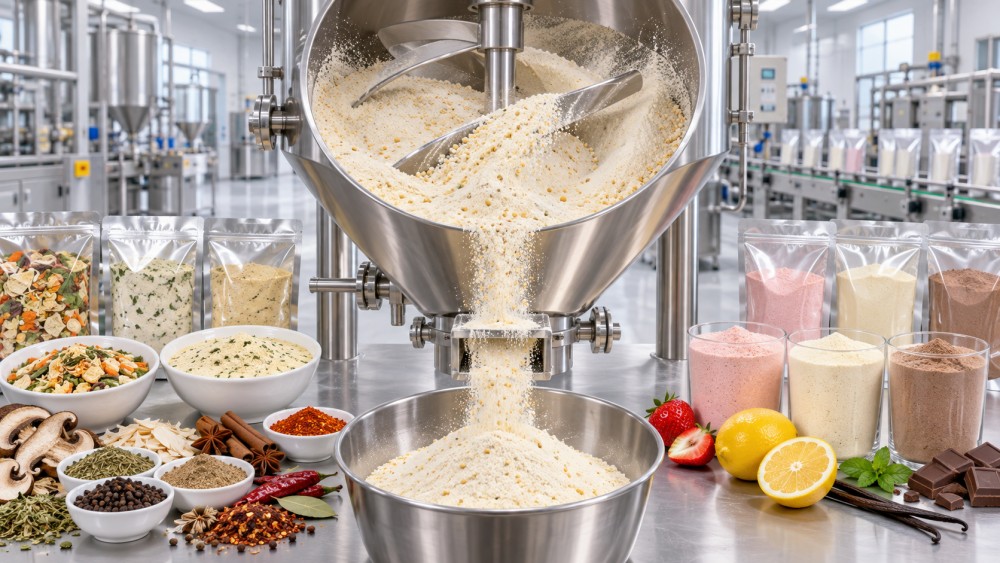
Selecting maltodextrin for flavor carriers in dry food blends requires more than comparing price, appearance, and nominal flowability. In powdered soups, seasoning systems, beverage premixes, bakery mixes, snack coatings, and dry sauces, the carrier becomes part of the flavor-delivery system. It affects how aroma survives manufacture, how evenly a flavor disperses, how readily powder moves through equipment, and what happens after the pack is opened in a humid kitchen or warehouse.
For quality and food safety functions, the question is not simply whether a maltodextrin is food grade. The practical question is whether its properties are suitable for a particular flavor, processing route, finished-product shelf-life target, packaging format, and destination market. A material that works well in a dry beverage blend may be unsuitable for a high-fat savory seasoning exposed to repeated temperature changes. The lowest-cost carrier can also become expensive if it creates batch variation, aroma loss, caking complaints, or documentation gaps.
Maltodextrin remains widely used because it can provide a relatively neutral solid matrix, support spray-dried flavor systems, dilute and standardize potent flavor components, and contribute manageable powder handling. Yet “maltodextrin” is a category, not a complete specification. Sensible selection starts by defining the real operating conditions around the powder.
The carrier is part of the flavor system, not an inactive filler
A flavor carrier may contain volatile aroma compounds, essential oils, extracts, oleoresins, emulsifiers, antioxidants, or other processing aids depending on how the flavor was made. Maltodextrin can form part of the protective wall around these materials during drying, but it is rarely the only factor controlling retention. The feed emulsion, drying conditions, oil load, emulsifier choice, particle structure, and storage environment all matter.
That distinction matters during supplier discussions. Asking only for a maltodextrin certificate of analysis does not establish that the final encapsulated flavor will perform consistently. A carrier with acceptable incoming specifications may still behave differently when paired with a citrus oil, a sulfur-containing savory note, a heat-sensitive botanical extract, or a high-impact cooling ingredient. Evaluation should therefore include the carrier’s inherent properties and a representative flavor application trial whenever the product risk justifies it.
For dry food blends, performance is often judged by sensory consistency at three points: immediately after production, after expected storage, and after preparation by the consumer or food-service operator. A powder can smell strong in the bag but release weakly after reconstitution. Conversely, a poorly protected flavor may seem acceptable at release yet lose top notes during distribution. The intended moment of aroma release should guide carrier selection.
Start with dextrose equivalent, but do not stop there
Dextrose equivalent, commonly shortened to DE, is one of the first values buyers examine. It indicates the degree of starch hydrolysis and is associated with properties such as molecular size distribution, sweetness, reducing-sugar content, viscosity behavior, and glass-transition behavior. In general terms, lower-DE maltodextrins tend to have larger carbohydrate molecules and lower sweetness, while higher-DE materials are more hydrolyzed and can behave differently in moisture-sensitive systems.
There is no universally correct DE range for flavor carriers. A choice that supports a stable spray-drying process may not produce the best result in a finished blend exposed to humidity. Higher-DE grades can be attractive where rapid dissolution is important, but they may require closer attention to hygroscopicity and caking risk. Lower-DE grades may offer advantages in certain encapsulation or stability contexts, but viscosity of the feed system and processability must be checked. A specification sheet should be read as a starting point for formulation work, not as proof of end-use suitability.
It is also wise to ask whether DE is controlled as a target, a range, or simply a typical value. A broad acceptable range may be commercially reasonable for some applications but can introduce unwanted variation where flavor retention, bulk density, or powder flow is tightly controlled. The relevance of that variation depends on the formula and manufacturing process.
Moisture control is a quality issue and a safety-control issue
Dry blends are often treated as low-risk products because their water activity is low. That assumption becomes less comfortable when powders are hygroscopic, packed in inadequate barriers, stored through hot and humid logistics routes, or repeatedly exposed to ambient air after opening. Moisture uptake can lead to clumps, poor dosing, loss of free-flowing behavior, flavor migration, and uneven distribution of potent components.
Incoming moisture content is important, but it should not be considered in isolation. The more revealing question is how the selected maltodextrin-containing flavor behaves at the relevant relative humidity and temperature. Teams should consider equilibrium moisture behavior, caking tendency, sieve retention after storage, bulk-density change, and sensory stability. If the blend is packed in sachets, canisters, flexible pouches, or bulk bags, the packaging barrier and pack-headspace conditions may be as consequential as the carrier itself.
This is particularly relevant for products that include salt, acids, sugars, protein powders, hydrocolloids, or dehydrated vegetable particles. These ingredients may have very different moisture interactions. A well-performing encapsulated flavor can be undermined after blending if another component attracts moisture and promotes localized caking. The right control plan examines the whole blend rather than approving each raw material independently.
A practical review of carrier selection factors
Source transparency and allergen management deserve early attention
Maltodextrin may be produced from different starch sources, including corn, tapioca, potato, rice, or wheat. The source can matter for customer specifications, regional labelling expectations, dietary claims, and allergen-risk assessments. It is not prudent to infer allergen status from the generic ingredient name alone. The supplier’s raw-material declaration, allergen statement, process controls, and cross-contact policy should be reviewed against the finished product’s intended market and label position.
Where wheat-derived material is under consideration, the regulatory and labeling implications should be assessed carefully rather than assumed. Requirements can differ by jurisdiction and by the nature of the processing. Similar caution applies to non-GMO claims, identity-preserved sourcing, organic positioning, kosher or halal requests, and clean-label expectations. These are commercial and compliance questions that must be documented before the formula is locked, not resolved after packaging artwork has been approved.
Change management is equally important. A supplier’s ability to notify customers of changes in starch origin, manufacturing location, processing conditions, specification limits, packaging materials, or food-safety status can be more valuable than a narrowly favorable purchase price. For a flavor carrier used at a low inclusion level, an undeclared change can still create significant downstream work.
Do not separate powder flow from worker safety
Fine powders can generate dust during bag emptying, conveying, screening, blending, and cleaning. Maltodextrin is often selected partly for its handling profile, but the final flavor powder may behave very differently from the plain carrier due to oil content, particle morphology, anti-caking components, and the amount of fines. Dust control is therefore an operational safety consideration as well as a yield and housekeeping issue.
The appropriate assessment should reflect the actual installed process: manual tipping versus closed transfer, local extraction capability, cleaning method, potential ignition sources, and whether the site handles other combustible powders. Safety data sheets, dust-characterization information where available, and site-specific hazard reviews should be aligned. It is not enough to transfer a generic handling instruction from one powder to another.
Flowability also affects flavor uniformity. If a low-dose encapsulated flavor segregates from larger salt crystals, spice particles, sugar, or cereal fractions, a finished blend may pass average compositional checks while still delivering uneven sensory performance across individual packs. Particle-size matching, blending sequence, blend time, transfer points, and vibration during transport should be part of the trial design.
Documentation should follow the material through the chain
A robust approval file for maltodextrin for flavor carriers normally needs more than a basic certificate of analysis. The exact document set depends on market, internal standards, and product category, but procurement, quality, regulatory, and formulation teams commonly need a current specification, batch certificate format, food-safety and allergen statements, country-of-origin information where required, storage and shelf-life guidance, packaging description, traceability details, and change-control expectations.
For the flavor preparation itself, confirm what is present besides maltodextrin. This may include carrier co-materials, emulsifiers, antioxidants, processing aids, or anti-caking agents. The final label and regulatory assessment must address the flavor system in its actual supplied form, not an oversimplified view of its principal carrier. If the flavor is purchased through a distributor, responsibilities for document updates, lot traceability, complaint handling, and recall communication should be unambiguous.
FCAS approaches food ingredients and flavor systems through this application-level lens: a material’s name and headline specification are only one part of its commercial fitness. Buyers and technical teams generally make better decisions when formulation compatibility, storage behavior, documentation readiness, packaging conditions, and supplier reliability are examined together.
A sensible approval route before committing supply
The most reliable route is usually staged. Begin with a written application brief that states the flavor type, target dosage, blend composition, thermal exposure, pack format, intended shelf life, storage conditions, and destination markets. Use that brief to narrow carrier options rather than requesting an undifferentiated list of grades.
Then review representative batches in the actual blend. Check not only initial aroma and flow, but also sieve profile, caking tendency, dispensing behavior, blend uniformity, reconstitution or cooking performance, and sensory change after storage conditions relevant to the product. Where the product contains oxidation-sensitive flavor notes, the test plan may also need to consider oxygen exposure and package performance. Accelerated studies can be useful for screening, but they should not automatically replace real-time shelf-life evidence.
Finally, approve the supply arrangement rather than merely the sample. Confirm lot identification, retention-sample practice, lead times, storage requirements, pack integrity expectations, and the procedure for handling deviations. A technically suitable grade is not a complete solution if it cannot arrive consistently with the required documentation and protective packaging.
The best choice of maltodextrin for flavor carriers is usually the one that creates the fewest unresolved questions across flavor protection, powder behavior, food safety, labeling, and supply continuity. Before finalizing the specification, it is worth asking one direct question: does the evidence describe how this exact flavor powder will behave in this exact dry blend, or only how maltodextrin behaves in general? The answer often determines whether a routine purchase becomes a stable, controllable formulation decision.
Related News
 Antioxidants & Natural PreservativesWhat Quality Checks Matter When Sourcing Butylparaben for Personal CareButylparaben for personal care sourcing guide: compare assay, impurities, physical performance, documentation, traceability, and supplier quality to reduce formulation risk.MORE+
 Nano-microcapsule FormulationsHow Encapsulated Flavors Protect Taste During Processing and StorageEncapsulated Flavors protect taste from heat, oxygen, moisture, and storage loss. Explore smarter release, carrier selection, and processing strategies.MORE+
 Chelated Trace Element FertilizersHow Greenhouse Fertigation Systems Reduce Water and Fertilizer WasteGreenhouse fertigation systems reduce water and fertilizer waste with precise dosing, uniform irrigation, drainage monitoring, and smarter crop-zone control. Learn practical strategies.MORE+
 Supercritical CO2 Essential OilsHow Natural Essential Oil Blends Improve Consistent Product FragranceNatural essential oil blends help brands achieve consistent, appealing fragrance across batches. Explore smart blend design, stability testing, and product compatibility strategies.MORE+
 Non-ionic Surfactants & DefoamersHow to Choose Non Ionic Low Foaming Surfactants for CIP CleaningNon ionic low foaming surfactants for CIP cleaning: learn how to balance wetting, foam control, compatibility, and rinseability for reliable cleaning performance.MORE+
 Nano-microcapsule FormulationsHow Food Grade Cyclodextrin Complexes Protect Sensitive FlavorsFood grade cyclodextrin inclusion complexes help protect sensitive flavors from oxidation, evaporation, and processing loss while supporting controlled release and consistent sensory quality.MORE+
 Polymer-Coated Water Soluble NPKHow Fertilizer Coating Polymers Improve NPK Granule ReleaseFertilizer coating polymers for NPK granules improve controlled nutrient release, reduce loss risks, and enhance product consistency. Discover key selection and process insights.MORE+
 Chelated Trace Element FertilizersWhat Diammonium Phosphate Means for Crop Nutrition PlanningDiammonium Phosphate: learn how DAP supports early phosphorus access, nitrogen budgeting, smart placement, and balanced crop nutrition planning.MORE+
 Maillard Reaction Savory FlavorsHow to Assess a Flavor Bases Supplier List for Reliable SourcingGlobal Fine Chemicals & Agrochemical Intelligence Network flavor bases supplier list: assess specs, samples, supply risk, and true cost to source with confidence.MORE+
 Hydrocolloids & EmulsifiersHow Konjac Gum Powder Improves Texture in Low-Calorie FoodsKonjac gum powder improves body, stability, and mouthfeel in low-calorie foods. Discover practical tips for smoother sauces, beverages, and reduced-fat formulations.MORE+
 Supercritical CO2 Essential OilsWhat to Check Before Choosing a Botanical Essential Oils ManufacturerChoose a botanical essential oils manufacturer with confidence. Explore key checks for purity, traceability, compliance, batch consistency, and reliable supply.MORE+
 Microencapsulated FragrancesHow Fragrance Carriers for Detergents Improve Scent PerformanceFragrance carriers for detergents improve stability, fabric deposition, and long-lasting scent. Explore practical solutions for better wash-to-wear fragrance performance.MORE+
 Antioxidants & Natural PreservativesWhen Propyl Gallate Antioxidant Is the Right Choice for Oil StabilityPropyl gallate antioxidant: learn when it is the right choice for oil stability, shelf-life protection, processing compatibility, and smarter formulation decisions.MORE+
 Antioxidants & Natural PreservativesHow Potassium Sorbate Extends Shelf Life in Food and Beverage ProductsPotassium Sorbate helps food and beverage brands control yeast and mold spoilage. Explore pH, dosage, processing, and packaging strategies for reliable shelf life.MORE+
 Antioxidants & Natural PreservativesHow to Source Bulk Herbal Extracts With Reliable Quality ControlBulk herbal extracts sourcing guide: compare suppliers, verify traceability, review CoAs, and build reliable quality controls for safer, consistent purchasing.MORE+
 Antioxidants & Natural PreservativesWhat to Check Before Sourcing Butylparaben for Personal Care FormulasButylparaben for personal care sourcing guide: check market eligibility, purity, supplier controls, formula compatibility, packaging, and total risk before buying.MORE+
 Targeted Bio-pesticides & APIsChoosing Microbial Fungicides for Foliar Diseases in Integrated Crop ProgramsMicrobial fungicides for foliar diseases: learn how to match biology, formulation, tank compatibility, and timing for stronger integrated crop protection.MORE+
 Targeted Bio-pesticides & APIsHow Microbial Insecticides Control Caterpillars With Lower Crop Residue RiskMicrobial insecticides for caterpillars help protect crops with targeted early-larval control and lower residue-management pressure. Learn timing, coverage, compliance, and scouting essentials.MORE+
 Microencapsulated FragrancesHow to Add Encapsulated Laundry Fragrances Without Weakening Wash ResultsEncapsulated laundry fragrances: learn how to boost long-lasting scent while protecting cleaning power, stability, foam control, and fabric care.MORE+
 Supercritical CO2 Essential OilsHow Aroma Ingredients Shape Lasting and Skin-Safe Personal Care ProductsAroma ingredients for personal care: discover how to achieve lasting scent, formulation stability, skin safety, and confident product performance.MORE+
 Targeted Bio-pesticides & APIsInsecticides Explained Through Labels, Active Ingredients, and SafetyInsecticides explained through labels, active ingredients, formulations, and safety. Learn how to compare products, manage risk, and make informed crop protection decisions.MORE+
 Heavy-duty Industrial DegreasersHow to Select Parts Wash Cleaners for Automotive ComponentsParts wash cleaners for automotive components: learn how to match chemistry, materials, rinsing, safety, and waste controls for reliable cleaning results.MORE+
 Chelated Trace Element FertilizersHow Precision Fertigation Systems Improve Water and Nutrient ControlPrecision fertigation systems improve water and nutrient control with accurate dosing, uniform irrigation, smart monitoring, and reduced waste. Discover how to optimize crop performance.MORE+
 Hydrocolloids & EmulsifiersHow Bulk Price Factors Affect Hydrocolloid Stabilizer Blend SourcingHydrocolloid stabilizer blends bulk price: compare dosage efficiency, quality consistency, logistics, and documentation to reduce total sourcing costs.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow to Choose a Natural Sweeteners Supplier for Clean-Label ProductsNatural sweeteners supplier selection guide for clean-label products: compare formulation fit, traceability, documentation, and supply reliability.MORE+
 Non-ionic Surfactants & DefoamersWhat Cationic Surfactants Do and Where They Are UsedCationic Surfactants deliver antimicrobial action, conditioning, antistatic control, and surface treatment benefits. Explore key uses, compatibility, and safe selection tips.MORE+
 Targeted Bio-pesticides & APIsHow to Evaluate Pesticide Suspension Concentrates for Field StabilityPesticide Suspension Concentrates: learn how to evaluate field stability, redispersibility, dilution, tank-mix compatibility, and spray safety for reliable performance.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Systems for Meat Products Improve Texture and YieldHydrocolloid systems for meat products improve yield, texture, water retention, and slicing quality. Explore practical formulation strategies for stable, high-performing meat products.MORE+
 Microencapsulated FragrancesHow Laundry Fragrances for Liquid Detergents Improve Scent LongevityLaundry fragrances for liquid detergents: discover how fragrance design, deposition, and encapsulation create lasting fabric freshness and stronger product appeal.MORE+
 Nano-microcapsule FormulationsChoosing Fragrance Preparations That Perform Well in Personal WashFragrance preparations for personal wash: learn how to select options that protect clarity, stability, foam, scent performance, and packaging compatibility.MORE+
 Controlled-Release ThermodynamicsModified Cyclodextrins Explained for Controlled Fragrance ReleaseModified cyclodextrins enable controlled fragrance release, odor control, and volatile-note protection. Explore how they optimize performance in detergents, fabric care, and more.MORE+
 Microencapsulated FragrancesHow Fragrance Delivery Systems Improve Fabric Softener LongevityFragrance delivery systems for fabric softeners improve scent longevity through smart protection, reliable deposition, and controlled release for lasting freshness.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Cardamom Oil Supplier for Reliable SupplyNatural cardamom oil supplier evaluation guide: verify botanical origin, purity, batch consistency, documentation, packaging, and delivery reliability for confident sourcing.MORE+
 Maillard Reaction Savory FlavorsHow Ethyl Maltol Purity Testing Supports Flavor Safety ComplianceEthyl Maltol purity testing strengthens flavor safety compliance through identity checks, impurity profiling, supplier verification, and audit-ready documentation.MORE+
 Microencapsulated FragrancesEssential Oil Extracts Compared for Fragrance and Wellness UsesEssential Oil Extracts compared for fragrance and wellness: explore scent profiles, extraction methods, stability, safety, and sourcing insights for smarter formulation choices.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat Drives Zero Calorie Sweeteners Bulk Price in 2026Zero calorie sweeteners bulk price in 2026: compare specifications, dosage, quality, freight, and supply risk to make smarter sourcing decisions.MORE+
 EPA FIFRA & FDA GRAS RegsSynthetic Food Preservatives Rules That Support Safer FormulasSynthetic Food Preservatives: learn the rules for safer formulas, compliant use levels, validated shelf life, labeling, and reliable microbial control.MORE+
 Micelle Fluidics & ChelationHow Anionic Industrial Dispersants Improve Coating StabilityAnionic industrial dispersants improve coating stability, pigment wetting, viscosity control, gloss, and storage performance. Learn how to select and test the right solution.MORE+
 Supercritical CO2 Essential OilsHow to Choose Eucalyptus Oil Grades for Clean, Consistent ProductsChoose the right Eucalyptus Oil grade with confidence. Compare cineole content, purity, origin, processing, documentation, and application fit for consistent products.MORE+
 Micelle Fluidics & ChelationWhat Are Cationic Surfactants and Where Are They Commonly Used?Cationic Surfactants deliver powerful surface affinity for disinfection, fabric softening, hair conditioning, antistatic control, and industrial treatments. Explore key uses and selection factors.MORE+