What to Check Before Choosing a Synthetic Food Preservatives Supplier
A preservative can meet a purchase specification and still create problems on the production floor. A beverage may show unexpected yeast growth near the end of its intended shelf life, a sauce may develop off-notes after storage, or a bakery line may need repeated dosage adjustments because the incoming material behaves differently from the previous lot. In these situations, the issue is not always the preservative itself; it may be the supplier’s consistency, documentation, transport control, or understanding of the application.
Before choosing a synthetic food preservatives supplier, treat the decision as a supply-risk and application-fit review rather than a price comparison. The essential checks are: whether the supplier can legally support the intended market and food category, maintain stable quality from batch to batch, provide usable technical and safety documents, protect the material through packaging and logistics, and respond effectively when a formulation or quality question arises. A low unit price has limited value if it leads to rework, rejected finished goods, delayed release, or extra microbiological testing.
Start with the exact use case, not the ingredient name
“Preservative” is too broad to be a sourcing specification. Synthetic food preservatives may be used to control molds, yeasts, or certain bacteria, but their real-world performance depends on the food matrix. Acidity, water activity, salt content, sugar level, alcohol content, heat treatment, filling process, packaging atmosphere, and expected distribution temperature can all change the result.
Before requesting quotations, define what the material must do in your own process. This avoids a common purchasing problem: receiving offers that appear comparable because they use the same chemical name, while the supplied grade, particle form, solubility, carrier, or documentation scope differs.
- Identify the product category: beverage, bakery filling, sauce, dairy preparation, processed meat, snack coating, or another system.
- State the expected pH range and whether it may shift during production or storage.
- Describe the processing route, including heating, cooling, mixing order, and filling conditions.
- Clarify whether the preservative is added directly, dissolved first, or incorporated through a premix.
- Set the target shelf-life condition: ambient, chilled, frozen, or variable distribution.
- Specify the markets where the finished food will be sold and the label requirements that apply there.
A supplier does not need to design the entire formulation, but it should be able to understand these questions and explain whether its material is suitable for the proposed use. A supplier that only repeats a generic assay value may be adequate for a simple commodity purchase, yet may not be the right source for a sensitive formulation or multi-market product range.
Check regulatory fit before approving a commercial sample
Regulatory acceptability cannot be inferred from the fact that a preservative is widely used somewhere else. Permitted substances, food categories, use limits, purity criteria, labeling conventions, and documentation expectations may differ by destination market. A material may also be allowed in one type of food but not in another, or have a restriction related to the final product composition.
Ask the supplier to provide current documents that identify the product clearly and support its intended food use. Depending on the material and market, this normally includes a specification sheet, certificate of analysis format, safety data sheet, composition or allergen statement where relevant, and traceability information. When a declaration is needed for a particular market or application, assess whether it is specific enough to be useful rather than accepting a broad statement with no defined scope.
Pay close attention to identity. The product name on the quotation, technical data sheet, certificate of analysis, outer label, and shipping document should point to the same grade. Minor naming differences can be harmless, but unexplained differences in chemical form, salt form, concentration, or product code deserve clarification before release.
Questions that reveal documentation quality
Instead of asking only, “Do you have certificates?”, ask whether the documents answer operational questions. Can the supplier state the test methods behind the listed parameters? Does the certificate of analysis identify the batch and manufacturing or retest date? Are impurity limits, moisture, particle size, or other relevant physical characteristics included when they can affect handling? Is there a defined process for notifying buyers when a specification, manufacturing site, packaging format, or test method changes?
Documentation should also be reviewed by the people responsible for product compliance and quality release. Procurement can coordinate the request, but commercial approval should not substitute for the internal assessment needed for a food-contacting production environment.
Do not reduce quality to assay or purity
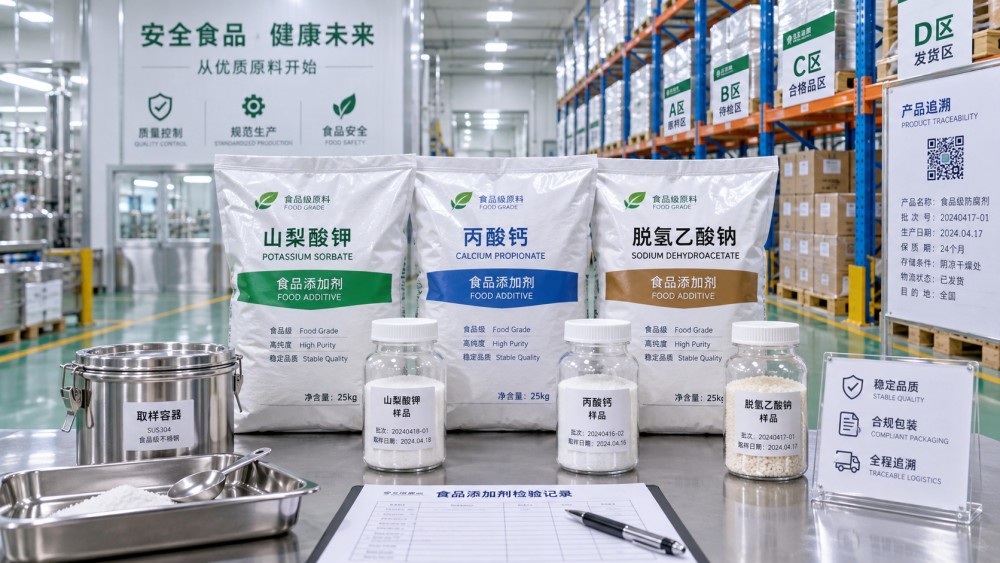
Assay is important, but it does not fully predict how a preservative will perform. A high-assay powder that disperses poorly, takes too long to dissolve, produces dust during charging, or varies in particle size can disrupt a stable manufacturing routine. In liquid or blended products, concentration accuracy, viscosity, sedimentation, appearance, and compatibility with the receiving formulation may matter just as much.
Request the supplier’s normal product specification and compare it against your internal acceptance criteria. The review should distinguish between parameters that are legally or safety critical and those that matter to manufacturing performance. For example, a bakery dry blend may be sensitive to flow and segregation, while a beverage concentrate may be more sensitive to clarity and dissolution behavior.
Ask whether the specification is a guaranteed release specification or merely a typical data sheet. “Typical” values can be informative, but they do not create a reliable acceptance basis. Also establish how out-of-specification material is handled, who authorizes a deviation, and whether substitutions can ever be made without written approval. A supplier should not assume that a commercially similar grade is interchangeable in food production.
Use samples to test the process, not just the laboratory
A small bench trial is useful, but it can miss problems that appear during normal manufacturing. The preservative may dissolve in a laboratory beaker yet form agglomerates in a large tank. A powder may work in a controlled trial but create significant airborne dust when transferred from bags. A liquid material may arrive homogeneous but separate after exposure to storage temperatures encountered in transit.
Where the product risk justifies it, evaluate a sample through the intended addition method and with the actual surrounding ingredients. Observe the time needed for dissolution or dispersion, the ease of dosing, visual uniformity, any effect on taste or odor, and whether the material affects pH, viscosity, foam, or appearance. Microbiological challenge work, where required by the product-development process, should be designed and interpreted by appropriately qualified technical personnel rather than being replaced by a supplier claim.
It is also prudent to ask whether the sample comes from the same manufacturing process and grade that would be supplied commercially. Development samples, pilot batches, and standard production material can differ in meaningful ways. The purpose is not to demand a perfect guarantee from a sample, but to avoid approving a material based on evidence that does not represent future supply.
Examine consistency across batches and through change control
Many sourcing failures are gradual rather than dramatic. The material remains within specification, but a shift toward a finer powder, slightly higher moisture, different packaging liner, or modified manufacturing route changes how it performs at the line. The first sign may be a slower premix, a different dosing correction, or more cleaning time. These changes can be costly even when no formal nonconformance has been declared.
Ask the supplier how it controls batch variation and what triggers customer notification. Important changes may include a new production location, altered raw-material source, revised analytical method, specification update, change in packaging components, or a different subcontracted logistics route. The expected notification process should be documented in the purchasing agreement or quality arrangement when the ingredient is business-critical.
For a new supplier, avoid relying solely on one approved batch. Review certificates from more than one lot when available, compare visible handling characteristics, and consider a staged approval. This is particularly helpful for products with narrow sensory tolerance, complex emulsions, low dosing levels, or a history of preservation-related complaints.
Packaging and logistics can undermine an otherwise suitable material
Food preservatives are often stable materials, but “stable” does not mean immune to poor transport or storage. Moisture exposure can cause powders to cake. Repeated temperature changes may affect some liquid preparations. Damaged sacks, weak seals, missing lot labels, or pallets stored in unsuitable conditions can complicate release and traceability.
Review the package format in the context of consumption rate and warehouse practice. A large bag may lower packing cost but create unnecessary exposure after opening if production uses only small quantities at a time. A smaller unit may simplify control but increase handling and packaging waste. The right choice depends on how quickly the material is consumed, whether it is transferred into a closed system, and whether opened containers can be resealed under controlled conditions.
Confirm the following before placing a routine order:
- Outer and inner packaging materials, sealing method, and label content.
- Net weight tolerances and pallet configuration relevant to receiving and storage.
- Recommended storage conditions and the supplier’s stated shelf-life or retest approach.
- Transport conditions, especially where long transit, hot climates, or seasonal temperature swings are expected.
- Procedures for handling damaged, wet, mislabeled, or short-dated deliveries.
- Whether each delivered unit can be linked to a batch certificate without ambiguity.
Lead time should be assessed beyond the promised dispatch date. Include document review time, inbound inspection, possible testing, customs clearance where relevant, and the time needed to replace a rejected lot. A supplier with a slightly higher quoted price but dependable delivery planning may reduce the need for expensive emergency purchases or excess safety stock.
Compare total procurement cost rather than unit price
Two offers with the same price per kilogram may have very different real costs. One may require longer internal testing, create higher handling loss, arrive in inconvenient packaging, or carry a greater risk of production interruption. Another may include clearer batch records, better technical response, and more predictable lead times. These are not abstract advantages; they affect labor, inventory, release timing, waste, and finished-product risk.
Build a comparison that separates direct cost from operating exposure. Direct cost includes material price, freight, duties where applicable, payment terms, and minimum order quantity. Operating exposure includes the cost of qualification, expected storage loss, cleaning or handling burden, batch-release effort, and the consequence of a late or disputed delivery. There is no need to assign speculative numbers to every risk, but recording them prevents the buying decision from being driven by a single visible figure.
Test the supplier’s response before a problem makes it urgent
Technical support is often evaluated only after an issue occurs, which is late in the decision process. During qualification, note how the supplier answers specific questions. A useful response identifies what is known, what needs confirmation, and which document or test method supports the answer. Vague reassurance, inconsistent documents, or repeated delays in providing basic information can signal future difficulty during a complaint or regulatory review.
Discuss practical scenarios in advance: a batch arrives with packaging damage; the certificate is missing; an internal result differs from the supplier’s result; a finished product shows unexpected spoilage; or a market-specific declaration is requested on short notice. The supplier does not need to promise that no problem will occur. It should, however, have a clear contact route, investigation process, traceability capability, and realistic timeline for corrective action.
The strongest approval decision is usually based on a defined application, usable compliance evidence, representative material evaluation, and a supply arrangement that can withstand ordinary disruptions. That approach gives procurement teams a basis for selecting a synthetic food preservatives supplier that supports consistent food safety and shelf-life control without creating hidden cost elsewhere in the operation.
Related News
 Antioxidants & Natural PreservativesWhat Quality Checks Matter When Sourcing Butylparaben for Personal CareButylparaben for personal care sourcing guide: compare assay, impurities, physical performance, documentation, traceability, and supplier quality to reduce formulation risk.MORE+
 Nano-microcapsule FormulationsHow Encapsulated Flavors Protect Taste During Processing and StorageEncapsulated Flavors protect taste from heat, oxygen, moisture, and storage loss. Explore smarter release, carrier selection, and processing strategies.MORE+
 Chelated Trace Element FertilizersHow Greenhouse Fertigation Systems Reduce Water and Fertilizer WasteGreenhouse fertigation systems reduce water and fertilizer waste with precise dosing, uniform irrigation, drainage monitoring, and smarter crop-zone control. Learn practical strategies.MORE+
 Supercritical CO2 Essential OilsHow Natural Essential Oil Blends Improve Consistent Product FragranceNatural essential oil blends help brands achieve consistent, appealing fragrance across batches. Explore smart blend design, stability testing, and product compatibility strategies.MORE+
 Non-ionic Surfactants & DefoamersHow to Choose Non Ionic Low Foaming Surfactants for CIP CleaningNon ionic low foaming surfactants for CIP cleaning: learn how to balance wetting, foam control, compatibility, and rinseability for reliable cleaning performance.MORE+
 Nano-microcapsule FormulationsHow Food Grade Cyclodextrin Complexes Protect Sensitive FlavorsFood grade cyclodextrin inclusion complexes help protect sensitive flavors from oxidation, evaporation, and processing loss while supporting controlled release and consistent sensory quality.MORE+
 Polymer-Coated Water Soluble NPKHow Fertilizer Coating Polymers Improve NPK Granule ReleaseFertilizer coating polymers for NPK granules improve controlled nutrient release, reduce loss risks, and enhance product consistency. Discover key selection and process insights.MORE+
 Chelated Trace Element FertilizersWhat Diammonium Phosphate Means for Crop Nutrition PlanningDiammonium Phosphate: learn how DAP supports early phosphorus access, nitrogen budgeting, smart placement, and balanced crop nutrition planning.MORE+
 Maillard Reaction Savory FlavorsHow to Assess a Flavor Bases Supplier List for Reliable SourcingGlobal Fine Chemicals & Agrochemical Intelligence Network flavor bases supplier list: assess specs, samples, supply risk, and true cost to source with confidence.MORE+
 Hydrocolloids & EmulsifiersHow Konjac Gum Powder Improves Texture in Low-Calorie FoodsKonjac gum powder improves body, stability, and mouthfeel in low-calorie foods. Discover practical tips for smoother sauces, beverages, and reduced-fat formulations.MORE+
 Supercritical CO2 Essential OilsWhat to Check Before Choosing a Botanical Essential Oils ManufacturerChoose a botanical essential oils manufacturer with confidence. Explore key checks for purity, traceability, compliance, batch consistency, and reliable supply.MORE+
 Microencapsulated FragrancesHow Fragrance Carriers for Detergents Improve Scent PerformanceFragrance carriers for detergents improve stability, fabric deposition, and long-lasting scent. Explore practical solutions for better wash-to-wear fragrance performance.MORE+
 Antioxidants & Natural PreservativesWhen Propyl Gallate Antioxidant Is the Right Choice for Oil StabilityPropyl gallate antioxidant: learn when it is the right choice for oil stability, shelf-life protection, processing compatibility, and smarter formulation decisions.MORE+
 Antioxidants & Natural PreservativesHow Potassium Sorbate Extends Shelf Life in Food and Beverage ProductsPotassium Sorbate helps food and beverage brands control yeast and mold spoilage. Explore pH, dosage, processing, and packaging strategies for reliable shelf life.MORE+
 Antioxidants & Natural PreservativesHow to Source Bulk Herbal Extracts With Reliable Quality ControlBulk herbal extracts sourcing guide: compare suppliers, verify traceability, review CoAs, and build reliable quality controls for safer, consistent purchasing.MORE+
 Antioxidants & Natural PreservativesWhat to Check Before Sourcing Butylparaben for Personal Care FormulasButylparaben for personal care sourcing guide: check market eligibility, purity, supplier controls, formula compatibility, packaging, and total risk before buying.MORE+
 Targeted Bio-pesticides & APIsChoosing Microbial Fungicides for Foliar Diseases in Integrated Crop ProgramsMicrobial fungicides for foliar diseases: learn how to match biology, formulation, tank compatibility, and timing for stronger integrated crop protection.MORE+
 Targeted Bio-pesticides & APIsHow Microbial Insecticides Control Caterpillars With Lower Crop Residue RiskMicrobial insecticides for caterpillars help protect crops with targeted early-larval control and lower residue-management pressure. Learn timing, coverage, compliance, and scouting essentials.MORE+
 Microencapsulated FragrancesHow to Add Encapsulated Laundry Fragrances Without Weakening Wash ResultsEncapsulated laundry fragrances: learn how to boost long-lasting scent while protecting cleaning power, stability, foam control, and fabric care.MORE+
 Supercritical CO2 Essential OilsHow Aroma Ingredients Shape Lasting and Skin-Safe Personal Care ProductsAroma ingredients for personal care: discover how to achieve lasting scent, formulation stability, skin safety, and confident product performance.MORE+
 Targeted Bio-pesticides & APIsInsecticides Explained Through Labels, Active Ingredients, and SafetyInsecticides explained through labels, active ingredients, formulations, and safety. Learn how to compare products, manage risk, and make informed crop protection decisions.MORE+
 Heavy-duty Industrial DegreasersHow to Select Parts Wash Cleaners for Automotive ComponentsParts wash cleaners for automotive components: learn how to match chemistry, materials, rinsing, safety, and waste controls for reliable cleaning results.MORE+
 Chelated Trace Element FertilizersHow Precision Fertigation Systems Improve Water and Nutrient ControlPrecision fertigation systems improve water and nutrient control with accurate dosing, uniform irrigation, smart monitoring, and reduced waste. Discover how to optimize crop performance.MORE+
 Hydrocolloids & EmulsifiersHow Bulk Price Factors Affect Hydrocolloid Stabilizer Blend SourcingHydrocolloid stabilizer blends bulk price: compare dosage efficiency, quality consistency, logistics, and documentation to reduce total sourcing costs.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow to Choose a Natural Sweeteners Supplier for Clean-Label ProductsNatural sweeteners supplier selection guide for clean-label products: compare formulation fit, traceability, documentation, and supply reliability.MORE+
 Non-ionic Surfactants & DefoamersWhat Cationic Surfactants Do and Where They Are UsedCationic Surfactants deliver antimicrobial action, conditioning, antistatic control, and surface treatment benefits. Explore key uses, compatibility, and safe selection tips.MORE+
 Targeted Bio-pesticides & APIsHow to Evaluate Pesticide Suspension Concentrates for Field StabilityPesticide Suspension Concentrates: learn how to evaluate field stability, redispersibility, dilution, tank-mix compatibility, and spray safety for reliable performance.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Systems for Meat Products Improve Texture and YieldHydrocolloid systems for meat products improve yield, texture, water retention, and slicing quality. Explore practical formulation strategies for stable, high-performing meat products.MORE+
 Microencapsulated FragrancesHow Laundry Fragrances for Liquid Detergents Improve Scent LongevityLaundry fragrances for liquid detergents: discover how fragrance design, deposition, and encapsulation create lasting fabric freshness and stronger product appeal.MORE+
 Nano-microcapsule FormulationsChoosing Fragrance Preparations That Perform Well in Personal WashFragrance preparations for personal wash: learn how to select options that protect clarity, stability, foam, scent performance, and packaging compatibility.MORE+
 Controlled-Release ThermodynamicsModified Cyclodextrins Explained for Controlled Fragrance ReleaseModified cyclodextrins enable controlled fragrance release, odor control, and volatile-note protection. Explore how they optimize performance in detergents, fabric care, and more.MORE+
 Microencapsulated FragrancesHow Fragrance Delivery Systems Improve Fabric Softener LongevityFragrance delivery systems for fabric softeners improve scent longevity through smart protection, reliable deposition, and controlled release for lasting freshness.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Cardamom Oil Supplier for Reliable SupplyNatural cardamom oil supplier evaluation guide: verify botanical origin, purity, batch consistency, documentation, packaging, and delivery reliability for confident sourcing.MORE+
 Maillard Reaction Savory FlavorsHow Ethyl Maltol Purity Testing Supports Flavor Safety ComplianceEthyl Maltol purity testing strengthens flavor safety compliance through identity checks, impurity profiling, supplier verification, and audit-ready documentation.MORE+
 Microencapsulated FragrancesEssential Oil Extracts Compared for Fragrance and Wellness UsesEssential Oil Extracts compared for fragrance and wellness: explore scent profiles, extraction methods, stability, safety, and sourcing insights for smarter formulation choices.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat Drives Zero Calorie Sweeteners Bulk Price in 2026Zero calorie sweeteners bulk price in 2026: compare specifications, dosage, quality, freight, and supply risk to make smarter sourcing decisions.MORE+
 EPA FIFRA & FDA GRAS RegsSynthetic Food Preservatives Rules That Support Safer FormulasSynthetic Food Preservatives: learn the rules for safer formulas, compliant use levels, validated shelf life, labeling, and reliable microbial control.MORE+
 Micelle Fluidics & ChelationHow Anionic Industrial Dispersants Improve Coating StabilityAnionic industrial dispersants improve coating stability, pigment wetting, viscosity control, gloss, and storage performance. Learn how to select and test the right solution.MORE+
 Supercritical CO2 Essential OilsHow to Choose Eucalyptus Oil Grades for Clean, Consistent ProductsChoose the right Eucalyptus Oil grade with confidence. Compare cineole content, purity, origin, processing, documentation, and application fit for consistent products.MORE+
 Micelle Fluidics & ChelationWhat Are Cationic Surfactants and Where Are They Commonly Used?Cationic Surfactants deliver powerful surface affinity for disinfection, fabric softening, hair conditioning, antistatic control, and industrial treatments. Explore key uses and selection factors.MORE+