How to Select Spray Drying Wall Materials for Better Stability
How to Select Spray Drying Wall Materials for Better Stability
Selecting the right spray drying wall materials is essential for protecting sensitive active ingredients, improving powder stability, and achieving consistent performance during storage and processing. For technical evaluators, the decision depends on compatibility, moisture resistance, encapsulation efficiency, release behavior, regulatory fit, and cost. This guide outlines the key criteria for comparing wall materials across food, agrochemical, fragrance, and specialty chemical applications.
The wall material is not simply an inert carrier. It determines whether a volatile flavor remains perceptible after drying, whether an oxidation-sensitive oil retains quality in a warehouse, whether a biological crop-protection ingredient survives processing, and whether a powder disperses as intended in the customer’s final system. A formulation can perform well in a laboratory feed emulsion but fail commercially because the dried particles absorb moisture, release the core too early, cake during transport, or become difficult to reconstitute.
That is why the right starting point is not “Which wall material is best?” It is “What instability must the wall prevent, under which process and end-use conditions?”
Start with the failure mode, not the ingredient name
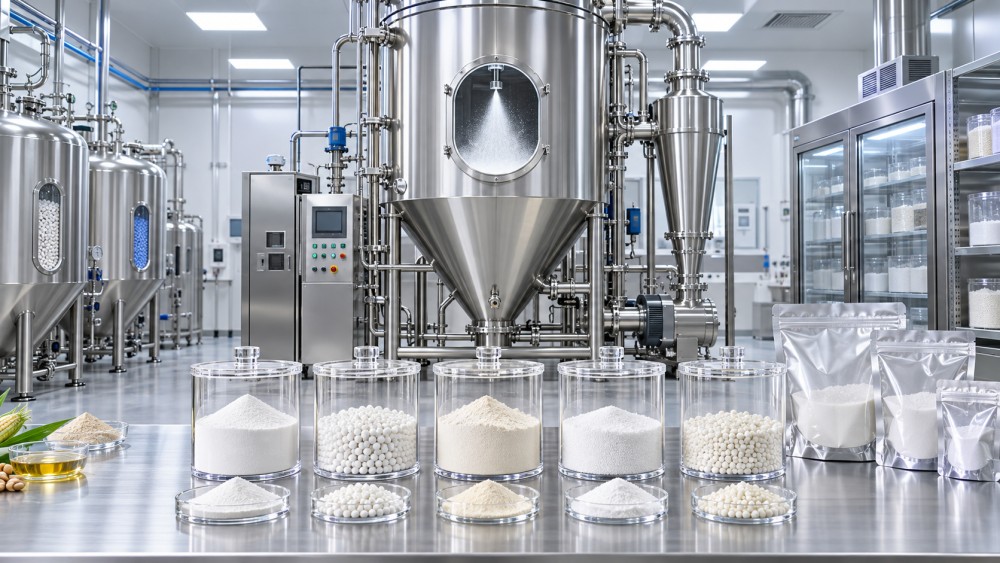
Spray drying is widely used to convert emulsions, suspensions, extracts, and solutions into easier-to-handle powders. The resulting particle typically contains a core material surrounded, at least partly, by a dried matrix or shell. In practice, complete and uniform encapsulation is not always achieved. Surface oil, cracks, pores, and uneven core distribution can all affect stability. Therefore, technical evaluation should define the dominant risk before shortlisting materials.
For an essential oil, aroma loss and oxidation may be the central concerns. For a food antioxidant or botanical extract, the relevant risks may be oxygen exposure, color change, hygroscopicity, and loss of dispersibility. In agrochemical formulations, the wall material may need to protect a sensitive active, limit dust, improve handling, or control release after dilution, soil contact, or application to a seed surface. Industrial formulations may place greater emphasis on compatibility with surfactants, salts, alkaline systems, or downstream cleaning processes.
A useful project brief identifies the core material’s physical state, volatility, solubility, pH sensitivity, thermal sensitivity, oxidative sensitivity, intended loading, end-use medium, expected storage conditions, and regulatory category. Without that brief, comparisons between polymers, carbohydrates, proteins, and gums tend to become generic and misleading.
Understand the main families of wall materials
Most spray drying wall systems are built from carbohydrates, proteins, modified starches, hydrocolloids, or combinations of these materials. Their performance differs because of film-forming ability, interfacial activity, glass-transition behavior, water affinity, molecular structure, and interaction with the core.
In many commercial formulations, a blend is more practical than a single wall material. One component may stabilize the emulsion, while another reduces cost, improves drying behavior, or changes the final powder’s handling characteristics. The right blend is not automatically the most complex one. Each added ingredient can alter feed viscosity, particle morphology, label status, reconstitution, and sourcing risk.
Compatibility is broader than chemical stability
Chemical incompatibility is an obvious reason to reject a wall material, but it is only one part of the assessment. Compatibility also includes whether the wall can form and maintain a stable feed before drying. If an oil phase coalesces in the emulsion, or suspended solids settle during production, a theoretically suitable carrier may yield inconsistent encapsulation and high surface-core content.
For hydrophobic cores, examine the emulsifying function separately from the bulk carrier function. A high-solids carbohydrate can help create a dry powder but may not sufficiently stabilize an oil-water interface. Conversely, an emulsifying material may create a stable feed but produce a powder that is too hygroscopic or expensive for the target market. Homogenization conditions, emulsifier choice, droplet-size distribution, and feed temperature all influence the result, so wall-material screening should not be isolated from process screening.
With reactive fine chemicals, botanical extracts, micronutrients, or agrochemical actives, check for pH-driven degradation, ionic interactions, hydrolysis, oxidation, and adsorption onto processing surfaces. Proteins and polysaccharides can also change viscosity or interact with charged materials. A benchtop compatibility check is useful, but it should be followed by storage evaluation of the actual dried powder rather than the liquid feed alone.
Moisture behavior often decides commercial shelf life
Many spray-dried powders fail in distribution rather than at the dryer outlet. Moisture uptake can soften particles, lower the glass-transition temperature of the matrix, increase stickiness, promote caking, and accelerate loss of volatile or oxidation-sensitive components. This is especially relevant in humid logistics environments and in products packed in large bags that may be opened and resealed during downstream production.
Technical teams should distinguish between low initial moisture and true moisture robustness. A powder may leave the dryer with acceptable moisture content but still be highly sensitive to ambient humidity. Water activity, hygroscopic behavior, particle integrity, flowability, and appearance after defined storage conditions provide a more complete view. The appropriate conditions depend on the product’s target market, packaging format, and anticipated distribution route.
Wall materials with different molecular weights or sugar profiles can behave very differently in this respect. Lower-cost carriers are not necessarily poor choices, but they should be judged against the real packaging system. A formulation that needs a high-barrier laminate, desiccant, or tightly controlled warehouse conditions may have a different total cost than one using a more robust wall matrix with simpler packaging requirements.
Match release behavior to the application, not just the drying process
“Better protection” is not always equivalent to “better performance.” A wall matrix that strongly retains a fragrance may reduce the immediate sensory impact required in a detergent or personal-care product. A food flavor powder may need rapid release after hydration, while an agricultural or seed-treatment formulation may need controlled release or durable retention during handling. For industrial cleaning systems, rapid dissolution and low residue may matter more than maximum barrier properties.
Release should therefore be evaluated in the end-use environment: water, oil, a dry premix, a coating slurry, soil, a wash bath, or a finished consumer product. Reconstitution time, dispersion quality, odor release, active availability, and residue should be considered together. A powder that looks excellent in a stability chamber may still be unsuitable if it does not release effectively when customers use it.
Do not treat dryer settings as an afterthought
Wall material selection and process design are closely linked. Feed solids, viscosity, atomizer type, inlet and outlet temperature, air flow, and residence time affect particle size, porosity, bulk density, surface composition, and retention of sensitive core materials. A material that performs well at pilot scale can behave differently on a production dryer because atomization energy and thermal exposure change.
Thermally sensitive ingredients deserve a more nuanced review than a single “maximum temperature” rule. The product’s actual thermal history depends on droplet evaporation and outlet conditions, not only on inlet air temperature. Still, this does not remove the need for validation. Biological materials, delicate aroma compounds, enzymes, and some oxidation-sensitive actives may require careful pilot work to balance drying efficiency with retention and activity.
The technical specification should also define acceptable powder properties. Depending on the application, this may include moisture, water activity, particle-size distribution, bulk density, flowability, dispersibility, surface oil, assay or active retention, odor profile, and microbial or impurity controls where relevant. Not every project needs every test, but omitting the performance-critical ones creates avoidable uncertainty during supplier qualification.
Regulatory and documentation fit can eliminate options early
A technically attractive wall material may not be usable in the intended market or application. Food, feed, crop protection, personal care, and industrial products operate under different frameworks, and requirements can vary by country or customer segment. Technical evaluators should confirm the intended use, composition, origin where relevant, declarations, safety documentation, impurity expectations, allergen status where applicable, and any restrictions related to labeling or residue concerns.
This review should happen before a lengthy optimization program. It is inefficient to develop a stable powder around a material that procurement cannot source consistently, regulatory teams cannot clear for the target use, or customers will not accept in their specification. Documentation quality is also a supply-chain issue: changes in grade, manufacturing location, or raw-material source may alter performance even when the material name remains the same.
For technical teams comparing options across food ingredients, fragrance systems, fertilizer products, crop-protection formulations, and specialty chemicals, FCAS provides a useful decision context: application performance must be reviewed alongside safety, handling, supply continuity, packaging, and market requirements. This broader view is particularly valuable when a formulation is moving from development to multi-market distribution.
A practical selection sequence
A disciplined selection process usually narrows the field quickly. Begin by defining the core material and the failure mode to be controlled. Remove materials that do not meet regulatory, labeling, or customer requirements. Then compare the remaining options through feed stability, pilot drying behavior, and storage performance in representative packaging.
The comparison should include the full formulation, not only the wall material. Core-to-wall ratio, emulsifier system, solids content, process aids, oxygen exposure, packaging, and storage conditions can each shift the outcome. It is also wise to assess more than one production-scale source when supply resilience matters. A material that works from one supplier may require reformulation when the grade characteristics of another source differ.
Before final approval, ask a simple operational question: what evidence would show that this powder will remain acceptable until the point of use? The answer may involve retained active content, sensory performance, caking resistance, reconstitution, particle integrity, or application results. That answer should guide the stability protocol and acceptance criteria.
Choose for the full product life, not the lowest raw-material cost
The most suitable spray drying wall materials are those that balance protection, processing practicality, end-use release, compliance, and commercial continuity. There is rarely a universal winner. A modified starch-based system may be compelling for one flavor oil, while a carbohydrate-protein blend may fit another food application better. A specialty chemical or agrochemical project may prioritize compatibility with downstream dilution, coating, or field-use conditions over sensory retention.
The final decision should be based on a defined product profile and evidence from representative trials, not on a wall material’s reputation alone. When teams align formulation, process, packaging, documentation, and intended application early, they are more likely to avoid the costly pattern of achieving a good powder in development and an unstable product in the market.
Related News
 Antioxidants & Natural PreservativesWhat Quality Checks Matter When Sourcing Butylparaben for Personal CareButylparaben for personal care sourcing guide: compare assay, impurities, physical performance, documentation, traceability, and supplier quality to reduce formulation risk.MORE+
 Nano-microcapsule FormulationsHow Encapsulated Flavors Protect Taste During Processing and StorageEncapsulated Flavors protect taste from heat, oxygen, moisture, and storage loss. Explore smarter release, carrier selection, and processing strategies.MORE+
 Chelated Trace Element FertilizersHow Greenhouse Fertigation Systems Reduce Water and Fertilizer WasteGreenhouse fertigation systems reduce water and fertilizer waste with precise dosing, uniform irrigation, drainage monitoring, and smarter crop-zone control. Learn practical strategies.MORE+
 Supercritical CO2 Essential OilsHow Natural Essential Oil Blends Improve Consistent Product FragranceNatural essential oil blends help brands achieve consistent, appealing fragrance across batches. Explore smart blend design, stability testing, and product compatibility strategies.MORE+
 Non-ionic Surfactants & DefoamersHow to Choose Non Ionic Low Foaming Surfactants for CIP CleaningNon ionic low foaming surfactants for CIP cleaning: learn how to balance wetting, foam control, compatibility, and rinseability for reliable cleaning performance.MORE+
 Nano-microcapsule FormulationsHow Food Grade Cyclodextrin Complexes Protect Sensitive FlavorsFood grade cyclodextrin inclusion complexes help protect sensitive flavors from oxidation, evaporation, and processing loss while supporting controlled release and consistent sensory quality.MORE+
 Polymer-Coated Water Soluble NPKHow Fertilizer Coating Polymers Improve NPK Granule ReleaseFertilizer coating polymers for NPK granules improve controlled nutrient release, reduce loss risks, and enhance product consistency. Discover key selection and process insights.MORE+
 Chelated Trace Element FertilizersWhat Diammonium Phosphate Means for Crop Nutrition PlanningDiammonium Phosphate: learn how DAP supports early phosphorus access, nitrogen budgeting, smart placement, and balanced crop nutrition planning.MORE+
 Maillard Reaction Savory FlavorsHow to Assess a Flavor Bases Supplier List for Reliable SourcingGlobal Fine Chemicals & Agrochemical Intelligence Network flavor bases supplier list: assess specs, samples, supply risk, and true cost to source with confidence.MORE+
 Hydrocolloids & EmulsifiersHow Konjac Gum Powder Improves Texture in Low-Calorie FoodsKonjac gum powder improves body, stability, and mouthfeel in low-calorie foods. Discover practical tips for smoother sauces, beverages, and reduced-fat formulations.MORE+
 Supercritical CO2 Essential OilsWhat to Check Before Choosing a Botanical Essential Oils ManufacturerChoose a botanical essential oils manufacturer with confidence. Explore key checks for purity, traceability, compliance, batch consistency, and reliable supply.MORE+
 Microencapsulated FragrancesHow Fragrance Carriers for Detergents Improve Scent PerformanceFragrance carriers for detergents improve stability, fabric deposition, and long-lasting scent. Explore practical solutions for better wash-to-wear fragrance performance.MORE+
 Antioxidants & Natural PreservativesWhen Propyl Gallate Antioxidant Is the Right Choice for Oil StabilityPropyl gallate antioxidant: learn when it is the right choice for oil stability, shelf-life protection, processing compatibility, and smarter formulation decisions.MORE+
 Antioxidants & Natural PreservativesHow Potassium Sorbate Extends Shelf Life in Food and Beverage ProductsPotassium Sorbate helps food and beverage brands control yeast and mold spoilage. Explore pH, dosage, processing, and packaging strategies for reliable shelf life.MORE+
 Antioxidants & Natural PreservativesHow to Source Bulk Herbal Extracts With Reliable Quality ControlBulk herbal extracts sourcing guide: compare suppliers, verify traceability, review CoAs, and build reliable quality controls for safer, consistent purchasing.MORE+
 Antioxidants & Natural PreservativesWhat to Check Before Sourcing Butylparaben for Personal Care FormulasButylparaben for personal care sourcing guide: check market eligibility, purity, supplier controls, formula compatibility, packaging, and total risk before buying.MORE+
 Targeted Bio-pesticides & APIsChoosing Microbial Fungicides for Foliar Diseases in Integrated Crop ProgramsMicrobial fungicides for foliar diseases: learn how to match biology, formulation, tank compatibility, and timing for stronger integrated crop protection.MORE+
 Targeted Bio-pesticides & APIsHow Microbial Insecticides Control Caterpillars With Lower Crop Residue RiskMicrobial insecticides for caterpillars help protect crops with targeted early-larval control and lower residue-management pressure. Learn timing, coverage, compliance, and scouting essentials.MORE+
 Microencapsulated FragrancesHow to Add Encapsulated Laundry Fragrances Without Weakening Wash ResultsEncapsulated laundry fragrances: learn how to boost long-lasting scent while protecting cleaning power, stability, foam control, and fabric care.MORE+
 Supercritical CO2 Essential OilsHow Aroma Ingredients Shape Lasting and Skin-Safe Personal Care ProductsAroma ingredients for personal care: discover how to achieve lasting scent, formulation stability, skin safety, and confident product performance.MORE+
 Targeted Bio-pesticides & APIsInsecticides Explained Through Labels, Active Ingredients, and SafetyInsecticides explained through labels, active ingredients, formulations, and safety. Learn how to compare products, manage risk, and make informed crop protection decisions.MORE+
 Heavy-duty Industrial DegreasersHow to Select Parts Wash Cleaners for Automotive ComponentsParts wash cleaners for automotive components: learn how to match chemistry, materials, rinsing, safety, and waste controls for reliable cleaning results.MORE+
 Chelated Trace Element FertilizersHow Precision Fertigation Systems Improve Water and Nutrient ControlPrecision fertigation systems improve water and nutrient control with accurate dosing, uniform irrigation, smart monitoring, and reduced waste. Discover how to optimize crop performance.MORE+
 Hydrocolloids & EmulsifiersHow Bulk Price Factors Affect Hydrocolloid Stabilizer Blend SourcingHydrocolloid stabilizer blends bulk price: compare dosage efficiency, quality consistency, logistics, and documentation to reduce total sourcing costs.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow to Choose a Natural Sweeteners Supplier for Clean-Label ProductsNatural sweeteners supplier selection guide for clean-label products: compare formulation fit, traceability, documentation, and supply reliability.MORE+
 Non-ionic Surfactants & DefoamersWhat Cationic Surfactants Do and Where They Are UsedCationic Surfactants deliver antimicrobial action, conditioning, antistatic control, and surface treatment benefits. Explore key uses, compatibility, and safe selection tips.MORE+
 Targeted Bio-pesticides & APIsHow to Evaluate Pesticide Suspension Concentrates for Field StabilityPesticide Suspension Concentrates: learn how to evaluate field stability, redispersibility, dilution, tank-mix compatibility, and spray safety for reliable performance.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Systems for Meat Products Improve Texture and YieldHydrocolloid systems for meat products improve yield, texture, water retention, and slicing quality. Explore practical formulation strategies for stable, high-performing meat products.MORE+
 Microencapsulated FragrancesHow Laundry Fragrances for Liquid Detergents Improve Scent LongevityLaundry fragrances for liquid detergents: discover how fragrance design, deposition, and encapsulation create lasting fabric freshness and stronger product appeal.MORE+
 Nano-microcapsule FormulationsChoosing Fragrance Preparations That Perform Well in Personal WashFragrance preparations for personal wash: learn how to select options that protect clarity, stability, foam, scent performance, and packaging compatibility.MORE+
 Controlled-Release ThermodynamicsModified Cyclodextrins Explained for Controlled Fragrance ReleaseModified cyclodextrins enable controlled fragrance release, odor control, and volatile-note protection. Explore how they optimize performance in detergents, fabric care, and more.MORE+
 Microencapsulated FragrancesHow Fragrance Delivery Systems Improve Fabric Softener LongevityFragrance delivery systems for fabric softeners improve scent longevity through smart protection, reliable deposition, and controlled release for lasting freshness.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Cardamom Oil Supplier for Reliable SupplyNatural cardamom oil supplier evaluation guide: verify botanical origin, purity, batch consistency, documentation, packaging, and delivery reliability for confident sourcing.MORE+
 Maillard Reaction Savory FlavorsHow Ethyl Maltol Purity Testing Supports Flavor Safety ComplianceEthyl Maltol purity testing strengthens flavor safety compliance through identity checks, impurity profiling, supplier verification, and audit-ready documentation.MORE+
 Microencapsulated FragrancesEssential Oil Extracts Compared for Fragrance and Wellness UsesEssential Oil Extracts compared for fragrance and wellness: explore scent profiles, extraction methods, stability, safety, and sourcing insights for smarter formulation choices.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat Drives Zero Calorie Sweeteners Bulk Price in 2026Zero calorie sweeteners bulk price in 2026: compare specifications, dosage, quality, freight, and supply risk to make smarter sourcing decisions.MORE+
 EPA FIFRA & FDA GRAS RegsSynthetic Food Preservatives Rules That Support Safer FormulasSynthetic Food Preservatives: learn the rules for safer formulas, compliant use levels, validated shelf life, labeling, and reliable microbial control.MORE+
 Micelle Fluidics & ChelationHow Anionic Industrial Dispersants Improve Coating StabilityAnionic industrial dispersants improve coating stability, pigment wetting, viscosity control, gloss, and storage performance. Learn how to select and test the right solution.MORE+
 Supercritical CO2 Essential OilsHow to Choose Eucalyptus Oil Grades for Clean, Consistent ProductsChoose the right Eucalyptus Oil grade with confidence. Compare cineole content, purity, origin, processing, documentation, and application fit for consistent products.MORE+
 Micelle Fluidics & ChelationWhat Are Cationic Surfactants and Where Are They Commonly Used?Cationic Surfactants deliver powerful surface affinity for disinfection, fabric softening, hair conditioning, antistatic control, and industrial treatments. Explore key uses and selection factors.MORE+