Powdered Triple Superphosphate: Handling, Storage, and Blend Compatibility
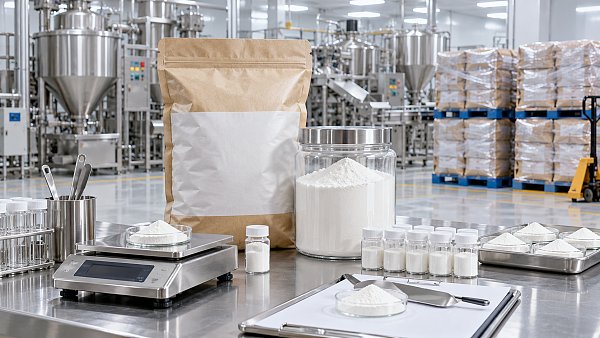
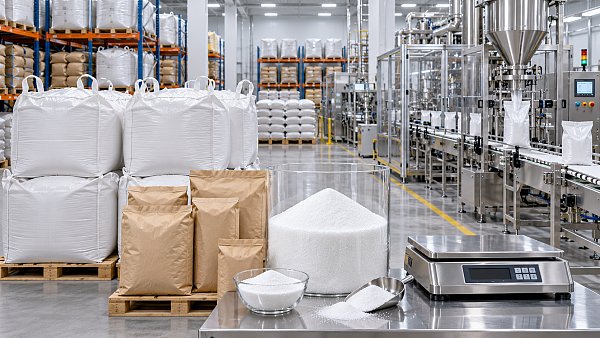
Powdered triple superphosphate requires a dry, controlled material path from receipt to final application. Its high phosphate concentration makes it useful where a compact phosphorus source is needed, but its fine particle size also increases the chance of dust release, moisture pickup, caking, transfer losses, and segregation in mixed fertilizers. Most handling problems begin before blending: damaged packaging, poor housekeeping around conveyors, a humid storage area, or an attempt to combine materials with very different particle characteristics.
The practical objective is to keep the fertilizer free-flowing, contained, and physically uniform until it reaches the intended application equipment. Product quality is affected by both chemical interactions and physical behavior. A blend can remain chemically acceptable yet perform poorly because fine phosphate powder settles between larger granules, generates dust during loading, or forms soft lumps after exposure to humid air.
Start With the Condition of the Delivered Material
Receiving inspection should focus on condition as well as the stated nutrient analysis. Examine bags, bulk liners, seals, and pallet wrapping for punctures, water marks, crushed corners, or hardened areas. Powder that has been compressed during transport may arrive as slabs or compacted sections even when it has not been wetted. These sections should be evaluated before being sent through a blending line, because aggressive breaking can create an excessive fraction of very fine particles.
Material that feels cool, dense, and compacted is not necessarily damp. Condensation, however, often leaves localized sticky zones near the inside of packaging or close to exposed surfaces. A simple visual inspection can distinguish many cases: dry compaction tends to fracture into powdery pieces, while moisture-related agglomerates smear, resist breakup, or leave a denser crust. Treating both conditions as a single “caking” problem can lead to the wrong corrective action.
Record the lot identification, packaging condition, visible lumping, and any unusual odor or discoloration. These observations support later troubleshooting if a blend develops poor flow or uneven nutrient distribution. If the material must be screened before use, retain the screened oversize separately until its condition is understood. Returning large wet lumps directly into a dry stream can distribute moisture through the batch.
Dust Control Is Part of Product Control
Fine phosphate dust is easily released at bag opening, hopper charging, screw transfer points, elevator boots, screen discharge, and bulk loading spouts. The visible dust cloud is only part of the loss. Fine particles can settle on structural members, collect in poorly cleaned equipment, and later contaminate a different formulation. Accumulated dust also makes it difficult to identify fresh leaks and can create slippery surfaces when mixed with moisture.
Use enclosed transfer routes wherever the equipment layout permits. A hopper receiving bagged material benefits from a close-fitting charging arrangement and local extraction placed to capture displaced air rather than pull product from the hopper. Excessive extraction velocity can remove fines preferentially and gradually change the particle distribution of the remaining material. The aim is containment, not a high-airflow system that carries fertilizer into filters.
- Open bags with a controlled cut that avoids tearing the inner liner and creating a sudden powder release.
- Keep drop heights short at transfer points. A long free fall breaks weak agglomerates and raises dust generation even when the material arrived in good condition.
- Clean spills promptly with a suitable industrial vacuum or a method that contains dust. Dry sweeping commonly redistributes fines into walkways, bearings, and nearby stock.
- Inspect extraction filters and ducting when dust levels rise. A blocked filter reduces capture, while a damaged filter can return fine material to the work area.
Personal protective equipment must match the site hazard assessment and the current safety documentation for the material. At a minimum, dust exposure, eye contact, and hand contamination need attention during bag handling, cleaning, and maintenance. Dusty clothing should be dealt with before leaving the work area; shaking it indoors simply transfers the material to another surface.
Keep Moisture Away From the Powder
Moisture management is more important than chasing a single warehouse temperature. Powdered phosphate can draw water from humid air, particularly when warm material enters a cooler building or when bags are moved from cold outdoor conditions into a humid enclosed area. Condensation can occur on packaging surfaces and on metal hoppers before anyone sees free water.
Store stock on sound pallets or racking, clear of floor moisture and away from walls where condensation or rain ingress is more likely. Do not place it beneath roof joints, pipes, door openings, or ventilation outlets that can introduce wet air. Maintain intact wrapping until the material is needed, and reseal partly used bags as soon as practical. A liner that appears closed but has a small tear near a fold can admit enough humid air to harden the product over time.
Bulk storage requires the same discipline at a larger scale. Silo roofs, access covers, fill pipes, and vent filters need regular inspection. Water entering through a compromised vent or cover often affects only the upper or side portion of the stockpile, so a normal sample from the discharge point does not prove that the entire inventory is dry. If a storage vessel is emptied infrequently, inspect for deposits on walls, bridging near outlets, and build-up around internal probes before the next filling cycle.
Temperature cycling deserves attention because it changes both air movement and condensation risk. Heating a room without controlling humid incoming air can worsen conditions near loading doors. Conversely, a dry, stable room with moderate temperature variation may preserve material better than a warm area that repeatedly exchanges humid outside air. The useful measure is whether the storage environment prevents moisture contact and keeps the powder mobile.
Flow Problems Need a Cause-Based Response
Bridging in a hopper, rat-holing above an outlet, and lumps in bags are related symptoms, but they do not always have the same cause. Bridging often reflects poor hopper geometry, a narrow outlet, compacted powder, or a surface that retains fines. Rat-holing can develop when material close to the outlet flows while the surrounding powder remains stationary and consolidates. Wet agglomeration is a material-condition issue; mechanical obstruction may be an equipment issue.
Do not solve recurring flow interruptions by striking hoppers or entering vessels without an approved isolation and entry procedure. Impact can damage equipment, compact the material further, or release a sudden mass of powder. Where flow aid is needed, assess the outlet size, wall angle, surface condition, feeder type, and the actual particle distribution before installing vibrators or air devices. A vibration setting that clears one powder may create compaction or segregation in another.
Feeder selection also matters. Screw feeders can provide controlled delivery, but they may compact fine material if operated with excessive compression or if the inlet is starved and repeatedly refilled. Rotary valves and belt systems have different risks, including leakage, pulsation, and carryover. A stable feed rate is more useful than a high nominal rate that fluctuates as the hopper alternates between free flow and bridging.
Blend Compatibility Has Two Separate Questions
Before combining powdered phosphate with another fertilizer component, consider chemical compatibility and physical compatibility separately. Chemical compatibility concerns whether contact, moisture, heat, or time can lead to undesirable reactions, nutrient losses, sticky surfaces, or changed material properties. Physical compatibility concerns whether the components stay evenly distributed from the blender to the field.
Fine powder blended with coarse granules is physically difficult even when no adverse chemical reaction is expected. During conveying and loading, smaller particles tend to migrate into void spaces between larger particles. The resulting blend may look uniform at discharge but separate during transport or filling. This is especially relevant where the final product is handled through multiple transfer points or spread over a large area.
Do not judge compatibility solely from the label names of fertilizer materials. Grade, moisture condition, surface treatment, particle shape, and storage history can change the result. Two lots described by the same general fertilizer category may behave differently because one contains more fines or has absorbed moisture during distribution.
Particle Size Often Decides Whether a Dry Blend Is Usable
A small amount of fine powder can coat granules and improve visual uniformity, yet a larger proportion can turn the same blend dusty and prone to separation. The relevant question is not whether the materials can be mixed in a short trial, but whether the blend retains uniformity after filling, conveying, transport vibration, discharge, and spreading.
Take samples from more than one location after the material has followed a representative handling route. A sample taken from the top of a freshly mixed batch may not reveal separation at the bottom of a bin or in the first and last portions discharged from a truck. Where the final application rate is low, even modest separation can produce visibly uneven delivery because the phosphate component is concentrated in selected fractions.
Screening can improve consistency when it removes oversize lumps and a problematic excess of fines, but screening is not a substitute for a compatible particle-size profile. It also creates a secondary material stream that must be managed without contaminating later batches. Reprocessing dry, intact oversize is different from reprocessing damp or chemically altered lumps.
Sequence and Residence Time Matter During Blending
Introduce components in a sequence that minimizes prolonged contact between dissimilar materials and avoids placing fine powder into a blender before the main material bed is established. Feeding powder into an empty, fast-moving blender can send it directly to extraction points or cause it to adhere to internal surfaces. Adding it onto a moving bed of compatible material usually improves distribution and reduces loss.
Blend only for the time needed to achieve a consistent mixture. Extra mixing is not automatically better. Extended mechanical action can break fragile granules, create more fines, and increase the separation tendency that the blending step was meant to control. The correct mixing time is demonstrated by representative samples, not by the appearance of a smooth surface.
When a formulation includes a conditioner, coating agent, or other liquid addition, assess its effect on powder adhesion and subsequent storage. A small amount of liquid can reduce dust by attaching fines to larger particles; too much, or poorly distributed liquid, can create wet spots that become hard lumps. Apply any liquid uniformly and allow the blend to stabilize before packaging or bulk loading where the process requires it.
Prepare the Material Path for Application
Before field-use preparation, remove old residues from hoppers, augers, spreaders, and transfer equipment. Residual wet fertilizer is more troublesome than residual dry fertilizer because it can seed new deposits and restrict flow. Examine gates, agitators, delivery belts, and spreader outlets for crusted material. A machine that meters a granular product accurately may not handle a powder-rich blend with the same setting.
Calibration must use the actual blend, not a nominally similar fertilizer. Bulk density, flow rate, moisture condition, and particle distribution affect discharge behavior. Run the material through the intended equipment long enough to observe stable flow, then check output across the width of the spreader or across parallel outlets. A setting adjusted on clean, dry material can drift after the equipment has been standing or after a partly filled hopper has compacted during travel.
Keep mixed material moving toward use rather than holding it unnecessarily. Short-term holding may be unavoidable, but every additional transfer and storage period increases the chance of separation, moisture pickup, and compaction. Where a blend has shown poor stability in trial handling, separate application of the components can be more dependable than repeatedly modifying the mixer settings.
Clean the system after use, especially at low points, hopper corners, and discharge gates. Removing retained powder while it remains dry is far easier than dealing with hardened deposits after humidity or wash water has reached it. Good storage and blending discipline preserves the physical condition that makes concentrated phosphorus fertilizer practical to handle in the first place.
Related News
 Antioxidants & Natural PreservativesWhat Quality Checks Matter When Sourcing Butylparaben for Personal CareButylparaben for personal care sourcing guide: compare assay, impurities, physical performance, documentation, traceability, and supplier quality to reduce formulation risk.MORE+
 Nano-microcapsule FormulationsHow Encapsulated Flavors Protect Taste During Processing and StorageEncapsulated Flavors protect taste from heat, oxygen, moisture, and storage loss. Explore smarter release, carrier selection, and processing strategies.MORE+
 Chelated Trace Element FertilizersHow Greenhouse Fertigation Systems Reduce Water and Fertilizer WasteGreenhouse fertigation systems reduce water and fertilizer waste with precise dosing, uniform irrigation, drainage monitoring, and smarter crop-zone control. Learn practical strategies.MORE+
 Supercritical CO2 Essential OilsHow Natural Essential Oil Blends Improve Consistent Product FragranceNatural essential oil blends help brands achieve consistent, appealing fragrance across batches. Explore smart blend design, stability testing, and product compatibility strategies.MORE+
 Non-ionic Surfactants & DefoamersHow to Choose Non Ionic Low Foaming Surfactants for CIP CleaningNon ionic low foaming surfactants for CIP cleaning: learn how to balance wetting, foam control, compatibility, and rinseability for reliable cleaning performance.MORE+
 Nano-microcapsule FormulationsHow Food Grade Cyclodextrin Complexes Protect Sensitive FlavorsFood grade cyclodextrin inclusion complexes help protect sensitive flavors from oxidation, evaporation, and processing loss while supporting controlled release and consistent sensory quality.MORE+
 Polymer-Coated Water Soluble NPKHow Fertilizer Coating Polymers Improve NPK Granule ReleaseFertilizer coating polymers for NPK granules improve controlled nutrient release, reduce loss risks, and enhance product consistency. Discover key selection and process insights.MORE+
 Chelated Trace Element FertilizersWhat Diammonium Phosphate Means for Crop Nutrition PlanningDiammonium Phosphate: learn how DAP supports early phosphorus access, nitrogen budgeting, smart placement, and balanced crop nutrition planning.MORE+
 Maillard Reaction Savory FlavorsHow to Assess a Flavor Bases Supplier List for Reliable SourcingGlobal Fine Chemicals & Agrochemical Intelligence Network flavor bases supplier list: assess specs, samples, supply risk, and true cost to source with confidence.MORE+
 Hydrocolloids & EmulsifiersHow Konjac Gum Powder Improves Texture in Low-Calorie FoodsKonjac gum powder improves body, stability, and mouthfeel in low-calorie foods. Discover practical tips for smoother sauces, beverages, and reduced-fat formulations.MORE+
 Supercritical CO2 Essential OilsWhat to Check Before Choosing a Botanical Essential Oils ManufacturerChoose a botanical essential oils manufacturer with confidence. Explore key checks for purity, traceability, compliance, batch consistency, and reliable supply.MORE+
 Microencapsulated FragrancesHow Fragrance Carriers for Detergents Improve Scent PerformanceFragrance carriers for detergents improve stability, fabric deposition, and long-lasting scent. Explore practical solutions for better wash-to-wear fragrance performance.MORE+
 Antioxidants & Natural PreservativesWhen Propyl Gallate Antioxidant Is the Right Choice for Oil StabilityPropyl gallate antioxidant: learn when it is the right choice for oil stability, shelf-life protection, processing compatibility, and smarter formulation decisions.MORE+
 Antioxidants & Natural PreservativesHow Potassium Sorbate Extends Shelf Life in Food and Beverage ProductsPotassium Sorbate helps food and beverage brands control yeast and mold spoilage. Explore pH, dosage, processing, and packaging strategies for reliable shelf life.MORE+
 Antioxidants & Natural PreservativesHow to Source Bulk Herbal Extracts With Reliable Quality ControlBulk herbal extracts sourcing guide: compare suppliers, verify traceability, review CoAs, and build reliable quality controls for safer, consistent purchasing.MORE+
 Antioxidants & Natural PreservativesWhat to Check Before Sourcing Butylparaben for Personal Care FormulasButylparaben for personal care sourcing guide: check market eligibility, purity, supplier controls, formula compatibility, packaging, and total risk before buying.MORE+
 Targeted Bio-pesticides & APIsChoosing Microbial Fungicides for Foliar Diseases in Integrated Crop ProgramsMicrobial fungicides for foliar diseases: learn how to match biology, formulation, tank compatibility, and timing for stronger integrated crop protection.MORE+
 Targeted Bio-pesticides & APIsHow Microbial Insecticides Control Caterpillars With Lower Crop Residue RiskMicrobial insecticides for caterpillars help protect crops with targeted early-larval control and lower residue-management pressure. Learn timing, coverage, compliance, and scouting essentials.MORE+
 Microencapsulated FragrancesHow to Add Encapsulated Laundry Fragrances Without Weakening Wash ResultsEncapsulated laundry fragrances: learn how to boost long-lasting scent while protecting cleaning power, stability, foam control, and fabric care.MORE+
 Supercritical CO2 Essential OilsHow Aroma Ingredients Shape Lasting and Skin-Safe Personal Care ProductsAroma ingredients for personal care: discover how to achieve lasting scent, formulation stability, skin safety, and confident product performance.MORE+
 Targeted Bio-pesticides & APIsInsecticides Explained Through Labels, Active Ingredients, and SafetyInsecticides explained through labels, active ingredients, formulations, and safety. Learn how to compare products, manage risk, and make informed crop protection decisions.MORE+
 Heavy-duty Industrial DegreasersHow to Select Parts Wash Cleaners for Automotive ComponentsParts wash cleaners for automotive components: learn how to match chemistry, materials, rinsing, safety, and waste controls for reliable cleaning results.MORE+
 Chelated Trace Element FertilizersHow Precision Fertigation Systems Improve Water and Nutrient ControlPrecision fertigation systems improve water and nutrient control with accurate dosing, uniform irrigation, smart monitoring, and reduced waste. Discover how to optimize crop performance.MORE+
 Hydrocolloids & EmulsifiersHow Bulk Price Factors Affect Hydrocolloid Stabilizer Blend SourcingHydrocolloid stabilizer blends bulk price: compare dosage efficiency, quality consistency, logistics, and documentation to reduce total sourcing costs.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow to Choose a Natural Sweeteners Supplier for Clean-Label ProductsNatural sweeteners supplier selection guide for clean-label products: compare formulation fit, traceability, documentation, and supply reliability.MORE+
 Non-ionic Surfactants & DefoamersWhat Cationic Surfactants Do and Where They Are UsedCationic Surfactants deliver antimicrobial action, conditioning, antistatic control, and surface treatment benefits. Explore key uses, compatibility, and safe selection tips.MORE+
 Targeted Bio-pesticides & APIsHow to Evaluate Pesticide Suspension Concentrates for Field StabilityPesticide Suspension Concentrates: learn how to evaluate field stability, redispersibility, dilution, tank-mix compatibility, and spray safety for reliable performance.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Systems for Meat Products Improve Texture and YieldHydrocolloid systems for meat products improve yield, texture, water retention, and slicing quality. Explore practical formulation strategies for stable, high-performing meat products.MORE+
 Microencapsulated FragrancesHow Laundry Fragrances for Liquid Detergents Improve Scent LongevityLaundry fragrances for liquid detergents: discover how fragrance design, deposition, and encapsulation create lasting fabric freshness and stronger product appeal.MORE+
 Nano-microcapsule FormulationsChoosing Fragrance Preparations That Perform Well in Personal WashFragrance preparations for personal wash: learn how to select options that protect clarity, stability, foam, scent performance, and packaging compatibility.MORE+
 Controlled-Release ThermodynamicsModified Cyclodextrins Explained for Controlled Fragrance ReleaseModified cyclodextrins enable controlled fragrance release, odor control, and volatile-note protection. Explore how they optimize performance in detergents, fabric care, and more.MORE+
 Microencapsulated FragrancesHow Fragrance Delivery Systems Improve Fabric Softener LongevityFragrance delivery systems for fabric softeners improve scent longevity through smart protection, reliable deposition, and controlled release for lasting freshness.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Cardamom Oil Supplier for Reliable SupplyNatural cardamom oil supplier evaluation guide: verify botanical origin, purity, batch consistency, documentation, packaging, and delivery reliability for confident sourcing.MORE+
 Maillard Reaction Savory FlavorsHow Ethyl Maltol Purity Testing Supports Flavor Safety ComplianceEthyl Maltol purity testing strengthens flavor safety compliance through identity checks, impurity profiling, supplier verification, and audit-ready documentation.MORE+
 Microencapsulated FragrancesEssential Oil Extracts Compared for Fragrance and Wellness UsesEssential Oil Extracts compared for fragrance and wellness: explore scent profiles, extraction methods, stability, safety, and sourcing insights for smarter formulation choices.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat Drives Zero Calorie Sweeteners Bulk Price in 2026Zero calorie sweeteners bulk price in 2026: compare specifications, dosage, quality, freight, and supply risk to make smarter sourcing decisions.MORE+
 EPA FIFRA & FDA GRAS RegsSynthetic Food Preservatives Rules That Support Safer FormulasSynthetic Food Preservatives: learn the rules for safer formulas, compliant use levels, validated shelf life, labeling, and reliable microbial control.MORE+
 Micelle Fluidics & ChelationHow Anionic Industrial Dispersants Improve Coating StabilityAnionic industrial dispersants improve coating stability, pigment wetting, viscosity control, gloss, and storage performance. Learn how to select and test the right solution.MORE+
 Supercritical CO2 Essential OilsHow to Choose Eucalyptus Oil Grades for Clean, Consistent ProductsChoose the right Eucalyptus Oil grade with confidence. Compare cineole content, purity, origin, processing, documentation, and application fit for consistent products.MORE+
 Micelle Fluidics & ChelationWhat Are Cationic Surfactants and Where Are They Commonly Used?Cationic Surfactants deliver powerful surface affinity for disinfection, fabric softening, hair conditioning, antistatic control, and industrial treatments. Explore key uses and selection factors.MORE+