Selecting Low Residue Semiconductor Wafer Cleaners for Critical Processes
At the end of a wafer clean, the surface may look perfect to the eye and still carry the contamination that matters most. A faint organic film, trace ionic carryover, poorly rinsed surfactant, or particles released from an incompatible chemistry can remain invisible until they affect electrical performance, lithography, deposition, bonding, or inspection yield. For operators working close to the tool, that uncertainty is stressful: a cleaning step is supposed to reduce risk, not create a new source of variation.
Selecting low residue semiconductor wafer cleaners is therefore not simply a matter of finding a product that removes visible soils. The cleaner must remove the target contamination and then leave the wafer surface, rinse system, and process hardware in a condition suitable for the next critical step. This requires a practical view of chemistry, rinse behavior, materials compatibility, handling discipline, and verification methods.
For high-purity processing environments, the best choice is usually the cleaner that fits a defined process window—not necessarily the most aggressive formulation or the one with the broadest cleaning claim. This guide helps operators and process teams evaluate that fit before a chemical reaches routine production.
Begin with the contamination, not the product label
Terms such as “precision cleaner,” “electronic cleaner,” and “residue-free cleaner” can be useful starting points, but they do not describe the actual soil on a wafer. Before comparing products, identify what needs to be removed and where it originates. The source often determines the appropriate chemistry more reliably than a general product category.
Common contamination classes include:
- Particles: abrasive dust, slurry remnants, polishing debris, fragments from handling equipment, dried chemical deposits, and airborne contamination.
- Organic residues: photoresist traces, polymeric films, processing oils, fingerprints, adhesive remnants, and residues from packaging or carriers.
- Ionic contamination: alkali metals, halides, metal ions, acidic or alkaline carryover, and salts left after incomplete rinsing.
- Metallic residues: traces associated with plating, etch, CMP, deposition, tooling contact, or upstream process fluids.
- Mixed soils: the frequent real-world condition in which particles are embedded in an organic film or metal-containing residue.
A particle-focused clean may depend heavily on wetting, controlled agitation, filtration, and rinse hydraulics. A stubborn organic film may require a different balance of solvent power, alkalinity, surfactancy, temperature, and contact time. If ionic residue is the central concern, the cleanliness of the water system and the ability to rinse the formulation completely may be more important than raw detergency.
Operators should also ask a simple but revealing question: Is the residue coming from the wafer process, the cleaning chemistry, the tool, or the rinse sequence? Replacing a cleaner will not solve a recurring issue caused by exhausted filters, contaminated tanks, improper bath turnover, poor wafer spacing, or a compromised final rinse.
What “low residue” should mean in practice
In semiconductor cleaning, low residue is not a vague promise of a clean-looking surface. It means the formulation is designed and controlled to minimize nonvolatile residues, ionic contaminants, problematic additives, and difficult-to-rinse components that could remain after the intended cleaning cycle.
For the operator, this translates into several practical expectations. The cleaner should disperse or solubilize the target soil without producing persistent foam or deposits. It should rinse away under the available equipment conditions. It should not leave a film that changes surface energy, interferes with coating adhesion, causes water-break behavior, or produces inspection anomalies. Its use should also be compatible with the required final rinse quality and drying method.
Residue risk is rarely determined by one ingredient alone. Surfactants can improve wetting and particle lift, yet some may be harder to rinse than others. Solvents can dissolve organics effectively, but may affect plastics, seals, adhesives, or wafer-mounted materials. Chelating agents can assist with metal removal, while their concentration and rinse behavior still need to be controlled. The right formulation is a balance between cleaning strength and clean departure.
Evaluate cleaner performance as a sequence, not a single bath
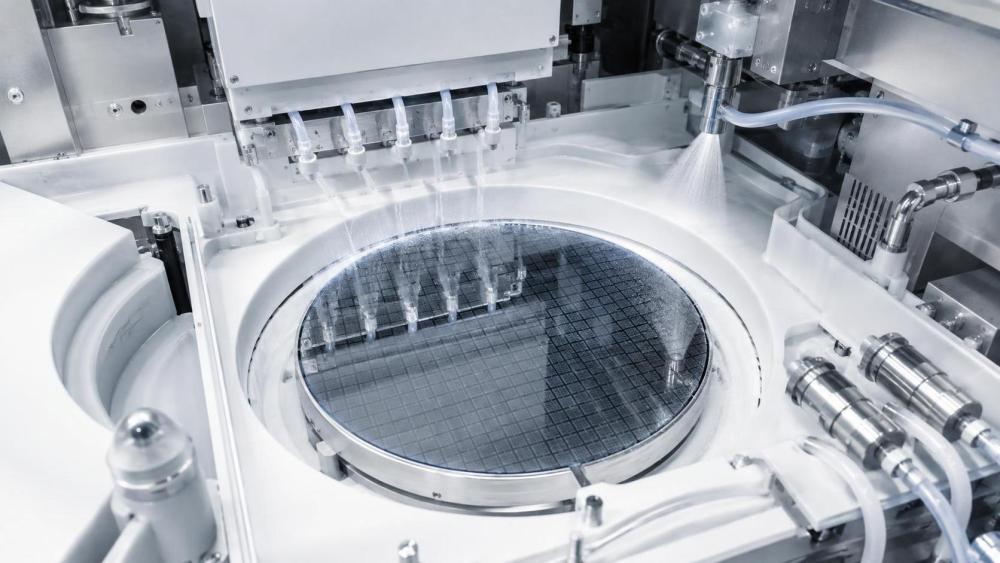
A wafer does not experience the cleaner in isolation. It moves through loading, pre-rinse or pre-wet, chemical exposure, agitation, displacement, multiple rinses, drying, transfer, and inspection. A chemistry that performs well in a laboratory beaker may behave differently in a spray tool, single-wafer processor, immersion tank, megasonic system, or manual-assisted station.
When screening low residue semiconductor wafer cleaners, map the complete sequence and define where the cleaning chemistry must work hardest. Consider the following process questions:
This sequence-based view prevents a common mistake: blaming the cleaning chemistry for residue that appears only because the rinse capacity is insufficient. In many cases, a formulation change and a rinse adjustment should be evaluated together.
Match chemistry to wafer materials and downstream sensitivity
Wafer cleaning is rarely performed on a simple, bare silicon surface. Operators may be handling patterned wafers, oxidized surfaces, compound semiconductors, metal stacks, dielectric layers, fragile low-k structures, bonded assemblies, or wafers carrying temporary protective materials. Each surface can respond differently to pH, oxidation potential, solvent exposure, temperature, and mechanical action.
A cleaner selected for one area of the fab or assembly flow should not automatically be transferred to another. A formulation that removes machining oil from an unpatterned substrate may be unsuitable for a surface awaiting high-resolution coating. Likewise, a chemistry that is acceptable before a robust thermal step may be inappropriate immediately before deposition, bonding, or sensitive metrology.
Ask suppliers and internal process owners for compatibility guidance that is specific to the actual wafer stack and equipment materials. Review possible interaction with silicon, native oxide, thermal oxide, nitrides, metals, glass, ceramics, polymers, photoresist-related materials, and carrier components. Do not overlook the tool itself: valves, tubing, filters, pump components, O-rings, tank linings, and spray nozzles must tolerate the chemistry over repeated cycles.
Where the next process step is especially sensitive, evaluate not only whether the wafer is clean, but whether its surface condition is appropriate. Surface energy, hydrophilicity, oxide condition, and trace ionic background can all influence downstream performance.
A practical screening plan for operators and process teams
A disciplined trial does not need to be unnecessarily complicated, but it should be controlled. Start with representative wafers or approved test coupons carrying the contamination of concern. Use the intended equipment wherever possible, because flow pattern, temperature uniformity, and rinse configuration strongly influence the outcome.
- Set an acceptance question. Define what success means: lower particle counts, improved water-break performance, reduced visible staining, cleaner inspection results, lower ionic carryover, or better downstream consistency.
- Establish a baseline. Record performance using the current approved cleaning sequence. Without a baseline, it is difficult to tell whether a new cleaner truly improves the process.
- Hold the process stable. During early trials, avoid changing concentration, temperature, agitation, and rinse time all at once. One change may hide the effect of another.
- Inspect after cleaning and after drying. Some residues are not evident until the wafer dries or moves through the next process step.
- Test rinse robustness. If a cleaner works only with unusually long rinse cycles, it may create throughput or water-use challenges in routine operation.
- Check repeatability. A successful single run is encouraging, but repeated results across shifts, batches, and normal operating conditions are more meaningful.
For critical applications, verification may involve particle inspection, surface analysis, contact-angle assessment, ionic contamination testing, microscopy, or downstream process checks. The appropriate method depends on the wafer and facility. The key is to select measurements that reveal the failure mode you are trying to prevent, rather than collecting data that looks impressive but does not guide a decision.
Do not confuse strong cleaning with reliable cleaning
When residue problems appear, there is a natural temptation to use a stronger chemistry, raise the concentration, extend exposure, or increase mechanical energy. These actions may improve immediate soil removal while introducing other risks: surface attack, pattern damage, chemical entrapment, material degradation, excessive foaming, redeposition, or a more demanding rinse burden.
Reliable cleaning is usually achieved through balance. The chemistry should be strong enough to release the soil, but controlled enough to protect the wafer and leave the process quickly. This is why a low-residue formulation with predictable rinse behavior can be a better fit than an aggressive general-purpose cleaner.
Another frequent misconception is that more surfactant always means better cleaning. Wetting agents are valuable when they improve contact with small features or lift hydrophobic soils. Yet excessive or poorly matched surfactant systems may complicate rinsing and leave surface-active traces. The question is not whether a cleaner contains surfactants; it is whether the full formulation performs cleanly under the actual rinse conditions.
Supplier documentation is part of the selection process
In a high-purity environment, product selection should include more than a technical data sheet. Operators and quality teams need clear information that supports safe, repeatable use. Review the safety data sheet, recommended dilution and operating conditions, storage limits, material compatibility notes, lot identification, packaging design, and guidance on bath maintenance or disposal.
For critical processes, ask whether the supplier can provide information relevant to impurity control, nonvolatile residue considerations, filtration recommendations, and quality consistency. The exact documentation requirements vary by site and application, but the principle remains the same: a cleaner is easier to manage when its intended use, limits, and control points are clearly understood.
Packaging also deserves attention. A well-formulated cleaner can still become a contamination concern if transferred through unsuitable containers, exposed to poor handling practices, or stored beyond recommended conditions. Clean chemical handling, labeled transfer equipment, controlled dispensing, and trained operators are part of the low-residue strategy.
Build a simple operating discipline around the chosen cleaner
Once a cleaner is selected, consistent execution becomes as important as the chemistry itself. Use approved concentration checks, defined bath-change criteria, and clear records for make-up, replenishment, filtration, temperature, and rinse conditions. If there is an upset—such as a prolonged idle period, abnormal foam, visible bath contamination, water-quality alarm, or changed drying appearance—treat it as a process signal rather than a minor inconvenience.
Operators are often the first people to notice subtle changes: a different drain pattern, unusual odor, slower break-up of foam, altered wafer appearance, or a shift in tool behavior. Creating a clear route for reporting those observations can prevent a small deviation from becoming a wider yield issue.
For teams comparing options, FCAS recommends framing the decision around the entire application: contamination type, wafer stack, equipment conditions, rinse capacity, downstream sensitivity, documentation needs, and routine handling realities. That approach makes the search for low residue semiconductor wafer cleaners more practical and less dependent on generic claims.
The most suitable cleaner is the one that removes the real soil, rinses predictably, respects the wafer and tool materials, and remains controllable from one production cycle to the next. In critical semiconductor work, that quiet consistency is often what protects the process most effectively.
Related News
 Antioxidants & Natural PreservativesWhat Quality Checks Matter When Sourcing Butylparaben for Personal CareButylparaben for personal care sourcing guide: compare assay, impurities, physical performance, documentation, traceability, and supplier quality to reduce formulation risk.MORE+
 Nano-microcapsule FormulationsHow Encapsulated Flavors Protect Taste During Processing and StorageEncapsulated Flavors protect taste from heat, oxygen, moisture, and storage loss. Explore smarter release, carrier selection, and processing strategies.MORE+
 Chelated Trace Element FertilizersHow Greenhouse Fertigation Systems Reduce Water and Fertilizer WasteGreenhouse fertigation systems reduce water and fertilizer waste with precise dosing, uniform irrigation, drainage monitoring, and smarter crop-zone control. Learn practical strategies.MORE+
 Supercritical CO2 Essential OilsHow Natural Essential Oil Blends Improve Consistent Product FragranceNatural essential oil blends help brands achieve consistent, appealing fragrance across batches. Explore smart blend design, stability testing, and product compatibility strategies.MORE+
 Non-ionic Surfactants & DefoamersHow to Choose Non Ionic Low Foaming Surfactants for CIP CleaningNon ionic low foaming surfactants for CIP cleaning: learn how to balance wetting, foam control, compatibility, and rinseability for reliable cleaning performance.MORE+
 Nano-microcapsule FormulationsHow Food Grade Cyclodextrin Complexes Protect Sensitive FlavorsFood grade cyclodextrin inclusion complexes help protect sensitive flavors from oxidation, evaporation, and processing loss while supporting controlled release and consistent sensory quality.MORE+
 Polymer-Coated Water Soluble NPKHow Fertilizer Coating Polymers Improve NPK Granule ReleaseFertilizer coating polymers for NPK granules improve controlled nutrient release, reduce loss risks, and enhance product consistency. Discover key selection and process insights.MORE+
 Chelated Trace Element FertilizersWhat Diammonium Phosphate Means for Crop Nutrition PlanningDiammonium Phosphate: learn how DAP supports early phosphorus access, nitrogen budgeting, smart placement, and balanced crop nutrition planning.MORE+
 Maillard Reaction Savory FlavorsHow to Assess a Flavor Bases Supplier List for Reliable SourcingGlobal Fine Chemicals & Agrochemical Intelligence Network flavor bases supplier list: assess specs, samples, supply risk, and true cost to source with confidence.MORE+
 Hydrocolloids & EmulsifiersHow Konjac Gum Powder Improves Texture in Low-Calorie FoodsKonjac gum powder improves body, stability, and mouthfeel in low-calorie foods. Discover practical tips for smoother sauces, beverages, and reduced-fat formulations.MORE+
 Supercritical CO2 Essential OilsWhat to Check Before Choosing a Botanical Essential Oils ManufacturerChoose a botanical essential oils manufacturer with confidence. Explore key checks for purity, traceability, compliance, batch consistency, and reliable supply.MORE+
 Microencapsulated FragrancesHow Fragrance Carriers for Detergents Improve Scent PerformanceFragrance carriers for detergents improve stability, fabric deposition, and long-lasting scent. Explore practical solutions for better wash-to-wear fragrance performance.MORE+
 Antioxidants & Natural PreservativesWhen Propyl Gallate Antioxidant Is the Right Choice for Oil StabilityPropyl gallate antioxidant: learn when it is the right choice for oil stability, shelf-life protection, processing compatibility, and smarter formulation decisions.MORE+
 Antioxidants & Natural PreservativesHow Potassium Sorbate Extends Shelf Life in Food and Beverage ProductsPotassium Sorbate helps food and beverage brands control yeast and mold spoilage. Explore pH, dosage, processing, and packaging strategies for reliable shelf life.MORE+
 Antioxidants & Natural PreservativesHow to Source Bulk Herbal Extracts With Reliable Quality ControlBulk herbal extracts sourcing guide: compare suppliers, verify traceability, review CoAs, and build reliable quality controls for safer, consistent purchasing.MORE+
 Antioxidants & Natural PreservativesWhat to Check Before Sourcing Butylparaben for Personal Care FormulasButylparaben for personal care sourcing guide: check market eligibility, purity, supplier controls, formula compatibility, packaging, and total risk before buying.MORE+
 Targeted Bio-pesticides & APIsChoosing Microbial Fungicides for Foliar Diseases in Integrated Crop ProgramsMicrobial fungicides for foliar diseases: learn how to match biology, formulation, tank compatibility, and timing for stronger integrated crop protection.MORE+
 Targeted Bio-pesticides & APIsHow Microbial Insecticides Control Caterpillars With Lower Crop Residue RiskMicrobial insecticides for caterpillars help protect crops with targeted early-larval control and lower residue-management pressure. Learn timing, coverage, compliance, and scouting essentials.MORE+
 Microencapsulated FragrancesHow to Add Encapsulated Laundry Fragrances Without Weakening Wash ResultsEncapsulated laundry fragrances: learn how to boost long-lasting scent while protecting cleaning power, stability, foam control, and fabric care.MORE+
 Supercritical CO2 Essential OilsHow Aroma Ingredients Shape Lasting and Skin-Safe Personal Care ProductsAroma ingredients for personal care: discover how to achieve lasting scent, formulation stability, skin safety, and confident product performance.MORE+
 Targeted Bio-pesticides & APIsInsecticides Explained Through Labels, Active Ingredients, and SafetyInsecticides explained through labels, active ingredients, formulations, and safety. Learn how to compare products, manage risk, and make informed crop protection decisions.MORE+
 Heavy-duty Industrial DegreasersHow to Select Parts Wash Cleaners for Automotive ComponentsParts wash cleaners for automotive components: learn how to match chemistry, materials, rinsing, safety, and waste controls for reliable cleaning results.MORE+
 Chelated Trace Element FertilizersHow Precision Fertigation Systems Improve Water and Nutrient ControlPrecision fertigation systems improve water and nutrient control with accurate dosing, uniform irrigation, smart monitoring, and reduced waste. Discover how to optimize crop performance.MORE+
 Hydrocolloids & EmulsifiersHow Bulk Price Factors Affect Hydrocolloid Stabilizer Blend SourcingHydrocolloid stabilizer blends bulk price: compare dosage efficiency, quality consistency, logistics, and documentation to reduce total sourcing costs.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow to Choose a Natural Sweeteners Supplier for Clean-Label ProductsNatural sweeteners supplier selection guide for clean-label products: compare formulation fit, traceability, documentation, and supply reliability.MORE+
 Non-ionic Surfactants & DefoamersWhat Cationic Surfactants Do and Where They Are UsedCationic Surfactants deliver antimicrobial action, conditioning, antistatic control, and surface treatment benefits. Explore key uses, compatibility, and safe selection tips.MORE+
 Targeted Bio-pesticides & APIsHow to Evaluate Pesticide Suspension Concentrates for Field StabilityPesticide Suspension Concentrates: learn how to evaluate field stability, redispersibility, dilution, tank-mix compatibility, and spray safety for reliable performance.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Systems for Meat Products Improve Texture and YieldHydrocolloid systems for meat products improve yield, texture, water retention, and slicing quality. Explore practical formulation strategies for stable, high-performing meat products.MORE+
 Microencapsulated FragrancesHow Laundry Fragrances for Liquid Detergents Improve Scent LongevityLaundry fragrances for liquid detergents: discover how fragrance design, deposition, and encapsulation create lasting fabric freshness and stronger product appeal.MORE+
 Nano-microcapsule FormulationsChoosing Fragrance Preparations That Perform Well in Personal WashFragrance preparations for personal wash: learn how to select options that protect clarity, stability, foam, scent performance, and packaging compatibility.MORE+
 Controlled-Release ThermodynamicsModified Cyclodextrins Explained for Controlled Fragrance ReleaseModified cyclodextrins enable controlled fragrance release, odor control, and volatile-note protection. Explore how they optimize performance in detergents, fabric care, and more.MORE+
 Microencapsulated FragrancesHow Fragrance Delivery Systems Improve Fabric Softener LongevityFragrance delivery systems for fabric softeners improve scent longevity through smart protection, reliable deposition, and controlled release for lasting freshness.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Cardamom Oil Supplier for Reliable SupplyNatural cardamom oil supplier evaluation guide: verify botanical origin, purity, batch consistency, documentation, packaging, and delivery reliability for confident sourcing.MORE+
 Maillard Reaction Savory FlavorsHow Ethyl Maltol Purity Testing Supports Flavor Safety ComplianceEthyl Maltol purity testing strengthens flavor safety compliance through identity checks, impurity profiling, supplier verification, and audit-ready documentation.MORE+
 Microencapsulated FragrancesEssential Oil Extracts Compared for Fragrance and Wellness UsesEssential Oil Extracts compared for fragrance and wellness: explore scent profiles, extraction methods, stability, safety, and sourcing insights for smarter formulation choices.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat Drives Zero Calorie Sweeteners Bulk Price in 2026Zero calorie sweeteners bulk price in 2026: compare specifications, dosage, quality, freight, and supply risk to make smarter sourcing decisions.MORE+
 EPA FIFRA & FDA GRAS RegsSynthetic Food Preservatives Rules That Support Safer FormulasSynthetic Food Preservatives: learn the rules for safer formulas, compliant use levels, validated shelf life, labeling, and reliable microbial control.MORE+
 Micelle Fluidics & ChelationHow Anionic Industrial Dispersants Improve Coating StabilityAnionic industrial dispersants improve coating stability, pigment wetting, viscosity control, gloss, and storage performance. Learn how to select and test the right solution.MORE+
 Supercritical CO2 Essential OilsHow to Choose Eucalyptus Oil Grades for Clean, Consistent ProductsChoose the right Eucalyptus Oil grade with confidence. Compare cineole content, purity, origin, processing, documentation, and application fit for consistent products.MORE+
 Micelle Fluidics & ChelationWhat Are Cationic Surfactants and Where Are They Commonly Used?Cationic Surfactants deliver powerful surface affinity for disinfection, fabric softening, hair conditioning, antistatic control, and industrial treatments. Explore key uses and selection factors.MORE+