How to Verify Semiconductor Process Cleaners Purity Requirements
A cleaner can meet its stated assay value and still be unsuitable for semiconductor processing. A high percentage of the intended solvent, surfactant, acid, base, or oxidizing component does not reveal whether the material carries trace metals, mobile ions, particles, nonvolatile residue, or organic extractables that can remain on a sensitive surface. In a high-purity process area, those hidden contaminants may contribute to wafer defects, corrosion, unstable wetting, rinse failures, or yield variation that is difficult to trace back to one incoming material.
To verify semiconductor process cleaners purity requirements, start with the actual cleaning step rather than a generic “high-purity” label. Define the substrate, process stage, dilution method, contact time, rinse sequence, and contamination budget. Then compare supplier specifications, analytical methods, batch records, packaging controls, and incoming test results against that use-specific requirement. The key decision is not whether a cleaner is chemically pure in general; it is whether its impurity profile is controlled at levels relevant to the process where it will be used.
Begin with the failure mode the cleaner must prevent
Purity requirements change according to where a cleaner enters the manufacturing flow. A material used for general equipment maintenance has a different risk profile from one used near exposed wafers, photomask surfaces, wet benches, precision parts, or final-rinse operations. The closer the cleaner comes to a contamination-sensitive surface, the less useful a broad assay specification becomes on its own.
Before reviewing a supplier’s certificate of analysis, document the condition the cleaner is expected to control. The following questions make the requirement more precise:
- What surface is being cleaned: silicon, glass, metal, ceramic, polymer, quartz, or a coated component?
- Is the material used before a critical deposition, lithography, etch, bonding, inspection, or packaging step?
- Will the cleaner be used neat, diluted with ultra-pure water, recirculated, sprayed, wiped, ultrasonically applied, or dispensed through a closed system?
- Which contaminant families are most harmful at this point: metals, alkali ions, halides, particles, organic films, ionic residues, or microorganisms?
- Can the downstream rinse fully remove residues, or is the cleaner itself part of the final surface-conditioning sequence?
This exercise also prevents an overly narrow purchasing specification. For example, a solvent-based cleaner may show an acceptable assay but leave a nonvolatile film after evaporation. An alkaline cleaner may have controlled active content while carrying trace sodium, potassium, chloride, or sulfate that is unacceptable for a particular process. A surfactant-containing formulation can clean effectively yet introduce organic residue if rinse behavior, total organic carbon, or residue-on-evaporation limits are not evaluated.
Translate “purity” into measurable impurity categories
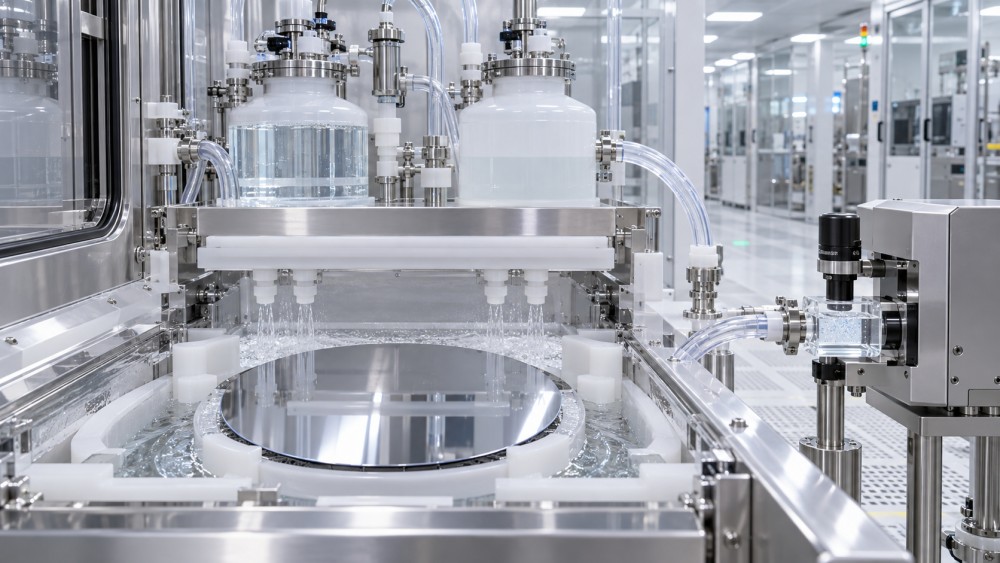
A useful specification separates the desired active component from contaminants that matter in the application. The table below shows the main categories normally considered during technical verification. The acceptable limit must be established by the user’s process requirements and should not be copied from an unrelated cleaner grade.
Not every cleaner requires every test at the same frequency. A concentrated aqueous cleaner used with a controlled rinse may need particularly close attention to metals, ionic contaminants, and particles. A volatile solvent cleaner may require stronger focus on nonvolatile residue, water content, unknown organic peaks, container extractables, and particle control. The correct test package follows the process risk, not a fixed template.
Do not accept analytical values without checking the method
A reported result is meaningful only when the test method can detect and quantify the impurity at the required level. This is a frequent gap in supplier qualification. A certificate may state “metals: pass” or “particles: conforms” without identifying the analytes, reporting units, sample preparation, detection limit, or test method. Such statements are difficult to compare with an internal contamination requirement.
Review each critical analysis with four practical questions. First, does the method cover the relevant impurity? A total-metal screen may not identify the specific elements of concern. Second, is the reporting limit lower than the acceptance limit? A result reported as “less than” a value above the process threshold does not demonstrate compliance. Third, was the sample prepared in a way that avoids loss, contamination, or matrix interference? Strong acids, volatile solvents, concentrated surfactants, and high-salt mixtures can all complicate analysis. Finally, is the method used consistently from batch to batch?
For particle testing, method details are especially important. Particle count can shift significantly depending on container cleanliness, sampling location, agitation, dilution medium, filter condition, instrument threshold, and whether the cleaner contains ingredients that naturally scatter light. A particle result should therefore be interpreted together with the particle-size range, test volume, preparation procedure, and packaging condition. Comparing two values obtained by different methods can create a false impression that one product is cleaner.
Use process-relevant units and limits
Ask suppliers to state impurity data in units that can be compared directly with internal specifications. Mass concentration, parts-per-billion, parts-per-million, particles per unit volume, conductivity, and nonvolatile residue all need clear units and test conditions. Ambiguous descriptions such as “ultra-trace,” “electronic grade,” or “low metal” may support an initial discussion, but they are not acceptance criteria.
Where the cleaner is diluted before use, evaluate both the concentrate and the final-use solution. Dilution can reduce some impurity concentrations, but it can also introduce contaminants through water quality, mixing tanks, transfer hoses, filters, and dispensing hardware. The use point is what reaches the surface. A clean concentrate does not compensate for an uncontrolled dilution and delivery system.
Build an incoming verification plan that matches risk
Testing every parameter on every delivered container may be unnecessary, while accepting every lot solely from a certificate may leave too much exposure. A practical approach divides properties into release-critical, periodic verification, and investigation-only items.
Release-critical properties are those that can immediately affect cleaning function or contamination risk, such as active concentration, appearance, conductivity where relevant, selected ionic impurities, particle count, or water content for sensitive materials. These should be checked against the purchase specification for each lot or according to a justified lot-release plan.
Periodic verification is suitable for tests that are stable but still important for supplier oversight, including broader metal panels, organic impurity screening, nonvolatile residue, or container extractables. The frequency should increase after a supplier change, process complaint, unusual shipping condition, packaging revision, or unexplained shift in downstream inspection results.
Investigation-only tests are reserved for a deviation, suspected contamination event, or process anomaly. They may include expanded metal screening, unknown peak identification, leachable studies, microbial evaluation for water-based systems, or surface residue analysis after a controlled cleaning trial. These tests should not replace a defined release specification, but they can identify why a previously acceptable cleaner is behaving differently.
Review the certificate of analysis as a batch record, not a brochure
A usable certificate of analysis should identify the product, lot number, manufacturing or release date, test methods or method references, actual results, specification limits, and release status. It should be possible to connect the certificate to the exact containers received. Generic specification sheets are useful during early evaluation but cannot confirm the quality of a particular shipment.
Pay attention to values that are repeatedly reported at a rounded limit or always shown as “not detected.” Either result may be acceptable, but quality teams should understand whether the supplier reports the instrument detection limit, the method reporting limit, or a fixed specification convention. Actual numeric results, when available, make trend review more effective.
Lot-to-lot consistency matters as much as a single compliant result. Keep a controlled record of critical certificate values, incoming test outcomes, container condition, and any process observations. A trend toward higher conductivity, rising particle levels, changing residue, or assay drift may appear before a formal out-of-specification event. This record is also useful when a supplier changes a raw material source, manufacturing site, purification train, filter, packaging component, or transport route.
Packaging and handling can invalidate a clean product
High-purity cleaner verification does not stop at the factory release point. Packaging must protect the material from particulate ingress, ionic contamination, moisture uptake, solvent loss, oxidation, light exposure, or leaching. The risk depends on the chemistry and the container system. A material that is stable in an unopened compatible container may change after repeated opening, poor resealing, or transfer through unsuitable tubing.
At receiving, inspect each shipment for damaged closures, distorted containers, leaks, external residue, missing tamper evidence, incorrect labels, and storage-condition excursions. Confirm that container materials, gaskets, caps, liners, valves, and transfer fittings are compatible with the cleaner and appropriate for the required cleanliness level. A chemically compatible component is not automatically a low-extractable component.
Storage should preserve both safety and purity. Segregate incompatible chemicals, follow supplier handling instructions, avoid uncontrolled temperature exposure, and limit unnecessary container opening. For materials dispensed into day tanks or process vessels, define cleaning and flushing practices, filter requirements, maximum hold time, and labeling controls. Without these measures, incoming qualification cannot demonstrate cleanliness at the point of use.
When a batch appears compliant but performance is unstable
A compliant certificate does not automatically rule out the cleaner during a contamination investigation. Start by confirming identity, lot traceability, dilution calculation, water quality, filter status, mixing sequence, and container history. Then compare retained samples or unopened material with the use-point solution. This distinction helps separate supplier-origin contamination from contamination introduced during storage or handling.
Surface symptoms can guide the next test. Particulate defects may justify particle counting of both concentrate and diluted solution, along with inspection of filters and transfer lines. Water-break behavior, poor wetting, or organic haze may call for residue-on-evaporation testing, organic screening, and review of surfactant concentration. Corrosion or unexpected conductivity changes may point toward ionic contamination, dilution error, or rinse-system issues. Where a critical process is affected, use a controlled evaluation plan that protects production material and documents the comparison conditions.
The strongest verification program links the cleaner specification to the actual contamination risks, confirms that the analytical methods are capable of proving compliance, and controls the material after receipt. That approach gives quality and safety teams a defensible basis for accepting, holding, retesting, or escalating a semiconductor process cleaner lot before a small impurity becomes a larger process problem.
Related News
 Antioxidants & Natural PreservativesWhat Quality Checks Matter When Sourcing Butylparaben for Personal CareButylparaben for personal care sourcing guide: compare assay, impurities, physical performance, documentation, traceability, and supplier quality to reduce formulation risk.MORE+
 Nano-microcapsule FormulationsHow Encapsulated Flavors Protect Taste During Processing and StorageEncapsulated Flavors protect taste from heat, oxygen, moisture, and storage loss. Explore smarter release, carrier selection, and processing strategies.MORE+
 Chelated Trace Element FertilizersHow Greenhouse Fertigation Systems Reduce Water and Fertilizer WasteGreenhouse fertigation systems reduce water and fertilizer waste with precise dosing, uniform irrigation, drainage monitoring, and smarter crop-zone control. Learn practical strategies.MORE+
 Supercritical CO2 Essential OilsHow Natural Essential Oil Blends Improve Consistent Product FragranceNatural essential oil blends help brands achieve consistent, appealing fragrance across batches. Explore smart blend design, stability testing, and product compatibility strategies.MORE+
 Non-ionic Surfactants & DefoamersHow to Choose Non Ionic Low Foaming Surfactants for CIP CleaningNon ionic low foaming surfactants for CIP cleaning: learn how to balance wetting, foam control, compatibility, and rinseability for reliable cleaning performance.MORE+
 Nano-microcapsule FormulationsHow Food Grade Cyclodextrin Complexes Protect Sensitive FlavorsFood grade cyclodextrin inclusion complexes help protect sensitive flavors from oxidation, evaporation, and processing loss while supporting controlled release and consistent sensory quality.MORE+
 Polymer-Coated Water Soluble NPKHow Fertilizer Coating Polymers Improve NPK Granule ReleaseFertilizer coating polymers for NPK granules improve controlled nutrient release, reduce loss risks, and enhance product consistency. Discover key selection and process insights.MORE+
 Chelated Trace Element FertilizersWhat Diammonium Phosphate Means for Crop Nutrition PlanningDiammonium Phosphate: learn how DAP supports early phosphorus access, nitrogen budgeting, smart placement, and balanced crop nutrition planning.MORE+
 Maillard Reaction Savory FlavorsHow to Assess a Flavor Bases Supplier List for Reliable SourcingGlobal Fine Chemicals & Agrochemical Intelligence Network flavor bases supplier list: assess specs, samples, supply risk, and true cost to source with confidence.MORE+
 Hydrocolloids & EmulsifiersHow Konjac Gum Powder Improves Texture in Low-Calorie FoodsKonjac gum powder improves body, stability, and mouthfeel in low-calorie foods. Discover practical tips for smoother sauces, beverages, and reduced-fat formulations.MORE+
 Supercritical CO2 Essential OilsWhat to Check Before Choosing a Botanical Essential Oils ManufacturerChoose a botanical essential oils manufacturer with confidence. Explore key checks for purity, traceability, compliance, batch consistency, and reliable supply.MORE+
 Microencapsulated FragrancesHow Fragrance Carriers for Detergents Improve Scent PerformanceFragrance carriers for detergents improve stability, fabric deposition, and long-lasting scent. Explore practical solutions for better wash-to-wear fragrance performance.MORE+
 Antioxidants & Natural PreservativesWhen Propyl Gallate Antioxidant Is the Right Choice for Oil StabilityPropyl gallate antioxidant: learn when it is the right choice for oil stability, shelf-life protection, processing compatibility, and smarter formulation decisions.MORE+
 Antioxidants & Natural PreservativesHow Potassium Sorbate Extends Shelf Life in Food and Beverage ProductsPotassium Sorbate helps food and beverage brands control yeast and mold spoilage. Explore pH, dosage, processing, and packaging strategies for reliable shelf life.MORE+
 Antioxidants & Natural PreservativesHow to Source Bulk Herbal Extracts With Reliable Quality ControlBulk herbal extracts sourcing guide: compare suppliers, verify traceability, review CoAs, and build reliable quality controls for safer, consistent purchasing.MORE+
 Antioxidants & Natural PreservativesWhat to Check Before Sourcing Butylparaben for Personal Care FormulasButylparaben for personal care sourcing guide: check market eligibility, purity, supplier controls, formula compatibility, packaging, and total risk before buying.MORE+
 Targeted Bio-pesticides & APIsChoosing Microbial Fungicides for Foliar Diseases in Integrated Crop ProgramsMicrobial fungicides for foliar diseases: learn how to match biology, formulation, tank compatibility, and timing for stronger integrated crop protection.MORE+
 Targeted Bio-pesticides & APIsHow Microbial Insecticides Control Caterpillars With Lower Crop Residue RiskMicrobial insecticides for caterpillars help protect crops with targeted early-larval control and lower residue-management pressure. Learn timing, coverage, compliance, and scouting essentials.MORE+
 Microencapsulated FragrancesHow to Add Encapsulated Laundry Fragrances Without Weakening Wash ResultsEncapsulated laundry fragrances: learn how to boost long-lasting scent while protecting cleaning power, stability, foam control, and fabric care.MORE+
 Supercritical CO2 Essential OilsHow Aroma Ingredients Shape Lasting and Skin-Safe Personal Care ProductsAroma ingredients for personal care: discover how to achieve lasting scent, formulation stability, skin safety, and confident product performance.MORE+
 Targeted Bio-pesticides & APIsInsecticides Explained Through Labels, Active Ingredients, and SafetyInsecticides explained through labels, active ingredients, formulations, and safety. Learn how to compare products, manage risk, and make informed crop protection decisions.MORE+
 Heavy-duty Industrial DegreasersHow to Select Parts Wash Cleaners for Automotive ComponentsParts wash cleaners for automotive components: learn how to match chemistry, materials, rinsing, safety, and waste controls for reliable cleaning results.MORE+
 Chelated Trace Element FertilizersHow Precision Fertigation Systems Improve Water and Nutrient ControlPrecision fertigation systems improve water and nutrient control with accurate dosing, uniform irrigation, smart monitoring, and reduced waste. Discover how to optimize crop performance.MORE+
 Hydrocolloids & EmulsifiersHow Bulk Price Factors Affect Hydrocolloid Stabilizer Blend SourcingHydrocolloid stabilizer blends bulk price: compare dosage efficiency, quality consistency, logistics, and documentation to reduce total sourcing costs.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow to Choose a Natural Sweeteners Supplier for Clean-Label ProductsNatural sweeteners supplier selection guide for clean-label products: compare formulation fit, traceability, documentation, and supply reliability.MORE+
 Non-ionic Surfactants & DefoamersWhat Cationic Surfactants Do and Where They Are UsedCationic Surfactants deliver antimicrobial action, conditioning, antistatic control, and surface treatment benefits. Explore key uses, compatibility, and safe selection tips.MORE+
 Targeted Bio-pesticides & APIsHow to Evaluate Pesticide Suspension Concentrates for Field StabilityPesticide Suspension Concentrates: learn how to evaluate field stability, redispersibility, dilution, tank-mix compatibility, and spray safety for reliable performance.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Systems for Meat Products Improve Texture and YieldHydrocolloid systems for meat products improve yield, texture, water retention, and slicing quality. Explore practical formulation strategies for stable, high-performing meat products.MORE+
 Microencapsulated FragrancesHow Laundry Fragrances for Liquid Detergents Improve Scent LongevityLaundry fragrances for liquid detergents: discover how fragrance design, deposition, and encapsulation create lasting fabric freshness and stronger product appeal.MORE+
 Nano-microcapsule FormulationsChoosing Fragrance Preparations That Perform Well in Personal WashFragrance preparations for personal wash: learn how to select options that protect clarity, stability, foam, scent performance, and packaging compatibility.MORE+
 Controlled-Release ThermodynamicsModified Cyclodextrins Explained for Controlled Fragrance ReleaseModified cyclodextrins enable controlled fragrance release, odor control, and volatile-note protection. Explore how they optimize performance in detergents, fabric care, and more.MORE+
 Microencapsulated FragrancesHow Fragrance Delivery Systems Improve Fabric Softener LongevityFragrance delivery systems for fabric softeners improve scent longevity through smart protection, reliable deposition, and controlled release for lasting freshness.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Cardamom Oil Supplier for Reliable SupplyNatural cardamom oil supplier evaluation guide: verify botanical origin, purity, batch consistency, documentation, packaging, and delivery reliability for confident sourcing.MORE+
 Maillard Reaction Savory FlavorsHow Ethyl Maltol Purity Testing Supports Flavor Safety ComplianceEthyl Maltol purity testing strengthens flavor safety compliance through identity checks, impurity profiling, supplier verification, and audit-ready documentation.MORE+
 Microencapsulated FragrancesEssential Oil Extracts Compared for Fragrance and Wellness UsesEssential Oil Extracts compared for fragrance and wellness: explore scent profiles, extraction methods, stability, safety, and sourcing insights for smarter formulation choices.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat Drives Zero Calorie Sweeteners Bulk Price in 2026Zero calorie sweeteners bulk price in 2026: compare specifications, dosage, quality, freight, and supply risk to make smarter sourcing decisions.MORE+
 EPA FIFRA & FDA GRAS RegsSynthetic Food Preservatives Rules That Support Safer FormulasSynthetic Food Preservatives: learn the rules for safer formulas, compliant use levels, validated shelf life, labeling, and reliable microbial control.MORE+
 Micelle Fluidics & ChelationHow Anionic Industrial Dispersants Improve Coating StabilityAnionic industrial dispersants improve coating stability, pigment wetting, viscosity control, gloss, and storage performance. Learn how to select and test the right solution.MORE+
 Supercritical CO2 Essential OilsHow to Choose Eucalyptus Oil Grades for Clean, Consistent ProductsChoose the right Eucalyptus Oil grade with confidence. Compare cineole content, purity, origin, processing, documentation, and application fit for consistent products.MORE+
 Micelle Fluidics & ChelationWhat Are Cationic Surfactants and Where Are They Commonly Used?Cationic Surfactants deliver powerful surface affinity for disinfection, fabric softening, hair conditioning, antistatic control, and industrial treatments. Explore key uses and selection factors.MORE+