How to Verify Residue Control in Semiconductor Process Cleaners
Residue Control Is a Process Qualification Issue, Not a Cleaner Claim
In semiconductor manufacturing, a process cleaner may remove visible soil and still create an unacceptable contamination risk. A wafer can look clean while carrying trace ionic species, organic films, particles, metals, or poorly rinsed surfactant components that later interfere with deposition, lithography, etching, bonding, or electrical reliability testing.
That is why verifying residue control in Semiconductor Process Cleaners cannot stop at reviewing a product data sheet or comparing nominal purity. Quality teams need evidence that the cleaner, its dilution water, its delivery system, and its rinse sequence work together under actual operating conditions. Safety teams also need to confirm that the control strategy remains stable when a chemical is transferred, diluted, stored, or replaced.
The practical question is not simply, “Does this chemical clean?” It is: “After cleaning and rinsing, what remains on the process surface, how confidently can we measure it, and is the result acceptable for this process step?” The acceptable answer will differ between a less sensitive equipment-maintenance application and a wafer-facing wet process. There is no universal residue threshold that can be borrowed without considering the device architecture, process window, substrate material, and downstream exposure.
Define What “Residue” Means for the Actual Process
A common sourcing mistake is to treat residue as one category. In practice, it has several forms, and each points to a different verification method. A cleaner formulated with surfactants, solvents, chelants, corrosion inhibitors, pH adjusters, or stabilizers may leave very different signatures depending on concentration, bath age, temperature, dwell time, and rinse quality.
This distinction matters because a low total organic carbon result does not prove low metal contamination, and a clean ion chromatography profile does not rule out a persistent organic boundary layer. A meaningful verification plan starts by ranking likely contaminants from the cleaner formulation and the soil being removed. It should then connect those contaminants to the failure modes relevant to the process.
For example, a cleaner selected for removing machining oils from non-wafer process hardware may require strong evidence of rinseability and material compatibility. A chemistry introduced to a wafer-adjacent clean step demands a narrower contamination review, including raw-material controls, packaging cleanliness, filtration strategy, and batch-to-batch impurity consistency.
Start with a Risk-Based Incoming Qualification Package
Before running a large-scale trial, quality personnel should request a documentation package that answers practical questions rather than merely confirming that a product exists. The certificate of analysis is important, but it is only one layer. It normally reflects the supplier’s release testing for a particular batch; it may not capture every impurity or residue risk relevant to a specific fab process.
A stronger review includes the current safety data sheet, technical data sheet, certificate of analysis, lot traceability approach, storage conditions, shelf-life basis, packaging specification, and change-notification process. Where process sensitivity warrants it, the team should ask what contaminants are controlled in raw materials, whether final filtration is used, how containers are cleaned or qualified, and whether the supplier can provide method information for key purity claims.
The wording of claims deserves attention. “High purity,” “electronic grade,” or “low residue” can be commercially useful descriptions, but they are not substitutes for a mutually understood specification. The buyer should define which parameters need limits, which are monitored for information only, what analytical method is used, and how changes will be communicated. This is especially important when a cleaning formulation contains proprietary components. Confidentiality may limit disclosure, but it should not prevent an adequate risk assessment.
FCAS follows this broader approach across high-purity industrial cleaning materials and specialty surfactants: a chemical’s application performance has to be assessed alongside impurity control, formulation stability, packaging integrity, safety documentation, transport conditions, and supplier consistency. For semiconductor-related cleaning, those issues are tightly connected rather than separate procurement checkboxes.
Verify the Full Cleaning and Rinsing Sequence
A laboratory evaluation of undiluted cleaner provides useful information, but it does not represent the process. Residue is often created by the interaction between the cleaner, the soil load, the bath, the substrate, the rinse water, and the drying method. A product that rinses well from one material may behave differently on oxidized silicon, metal films, quartz, ceramics, fluoropolymers, or engineered plastics.
The verification run should reproduce the intended use as closely as practical: concentration, exposure time, temperature, agitation, replenishment conditions, rinse stages, rinse-water quality, drying conditions, and expected holding time before the next process. It is also useful to test both a fresh bath and a realistically aged bath. Fresh chemistry can look excellent while accumulated soil, dissolved metals, degraded organics, or depleted active components make the rinse step less forgiving later in production.
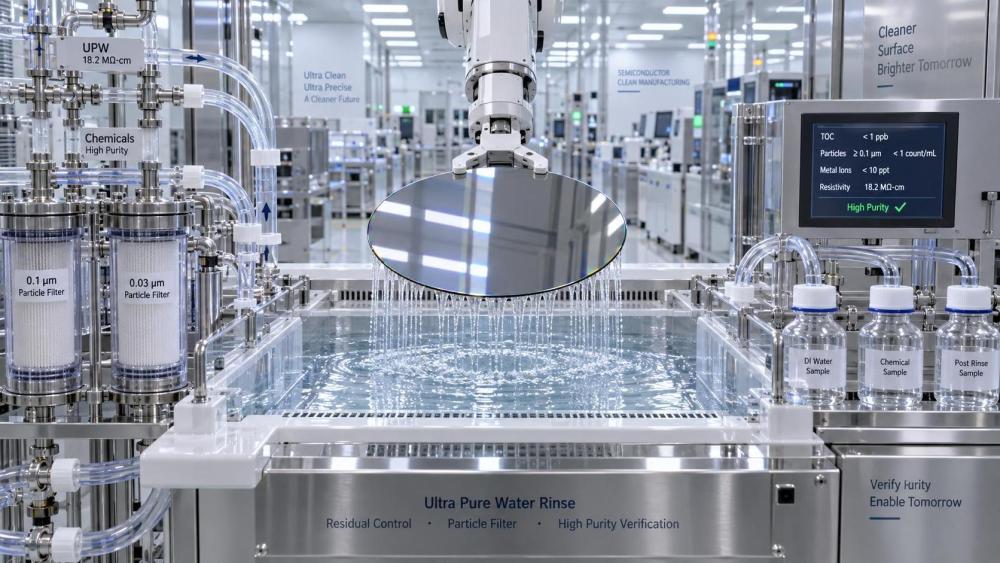
A practical test design should include controls. At minimum, compare an untreated reference, a process baseline if one exists, and the proposed cleaning sequence. Rinse blanks are equally important. If the blank already contains target ions, organics, or particles, the team cannot confidently assign a later result to the cleaner. In contamination work, poor blank control can invalidate a technically sophisticated analysis.
Sampling should reflect where residue is most likely to hide. Flat, open surfaces are rarely the only concern. Fixtures, threaded areas, narrow gaps, carrier interfaces, low-flow zones, and component backsides often retain chemistry longer. When a field complaint appears only after a production change, these overlooked geometries are usually worth checking before assuming the cleaner itself is defective.
Choose Analytical Methods That Answer a Specific Question
There is no single “residue test” for Semiconductor Process Cleaners. The method must be selected for the suspected contamination type and the decision being made. A fast screening method can be valuable for routine process control, while a more selective surface analysis may be needed during qualification or failure investigation.
Conductivity can provide a useful indication of ionic rinse progress, but it is not a complete cleanliness measurement. It may miss nonionic surfactants and many neutral organic residues. Likewise, TOC can help reveal organic carryover in rinse streams, yet it does not identify which organic is present or whether it forms a performance-relevant film. When the risk concerns a specific additive, decomposition product, or process contaminant, a targeted method is usually more defensible than relying only on a global screening result.
For surface-level questions, the recovery method matters as much as the instrument. Swabbing, solvent extraction, wafer extraction, and direct surface analysis can produce different answers because they collect different fractions of contamination. The procedure should specify the surface area, extraction solvent, contact time, sample container, handling controls, and reporting basis. Without that discipline, trend data become difficult to compare from lot to lot or site to site.
Quality teams should also confirm the method’s practical capability: detection limit, quantitation limit, known interferences, calibration approach, recovery performance, and uncertainty where relevant. A reported “non-detect” is meaningful only if the method can detect contamination at a level that matters to the process.
Do Not Separate Residue Control from Material Compatibility
Residue verification can be misleading if material compatibility is ignored. A cleaner may leave little measurable residue yet attack a seal, coating, polymer, adhesive, metal surface, or filter medium. The resulting extractables, flakes, corrosion products, or particles may appear later and be wrongly attributed to a rinse failure.
Compatibility testing should consider both immediate and delayed effects. Visual inspection alone is not enough for critical wetted components. Depending on the application, teams may need to observe discoloration, swelling, embrittlement, weight change, surface roughness, corrosion evidence, particle shedding, or changes in component function after chemical exposure and rinse cycles. Compatibility should be checked at the highest intended temperature and concentration, not only under convenient laboratory conditions.
This point is particularly relevant when changing suppliers. Even apparently similar cleaners can differ in trace stabilizers, solvent balance, surfactant package, pH reserve, or impurity profile. A substitution based only on concentration or a broad chemical family name is risky in a high-purity environment.
Build Ongoing Control Around Change, Not Just Release Testing
Once a cleaner has passed qualification, routine control should focus on the variables most likely to drift. These may include incoming lot identity, packaging condition, expiration status, dilution accuracy, bath concentration, bath age, particle control, rinse-water condition, filter replacement, and cleaning tool maintenance. The right frequency depends on process criticality and historical stability; it should not be copied blindly from another site.
A workable change-control agreement is often more valuable than an overly broad specification. Suppliers should be expected to notify customers of changes that could affect residue behavior: raw-material source changes, formulation adjustments, manufacturing-site transfers, revised filtration, altered packaging, modified test methods, or changes in storage and transport conditions. Internally, changes to rinse time, water source, drying temperature, recirculation, or bath life should trigger a proportionate review as well.
Safety management belongs in this system. Incorrect decanting, incompatible transfer equipment, mislabeled secondary containers, or inadequate ventilation can create both personnel hazards and contamination events. A chemical that is clean at the supplier’s fill line can acquire particles or extractables through poor handling after delivery. Traceability should therefore extend beyond the container lot to the point of use, dilution record, equipment used, and operator-controlled steps where feasible.
When Results Drift, Investigate the Sequence Before Blaming the Product
If residue results rise unexpectedly, start with the simplest traceable questions: Was the correct lot used? Was it within storage conditions? Did dilution, temperature, or rinse duration change? Were filters, rinse lines, carriers, or fixtures serviced? Did the analytical blank change? Has the incoming soil load shifted?
The cleaner may be the cause, but it is not always the first cause. In many real investigations, the issue lies in rinse-water quality, bath exhaustion, stagnant flow zones, contaminated transfer hardware, or an analytical sampling problem. Preserving retain samples, maintaining lot records, and documenting the process state at the time of sampling make that distinction far easier to resolve.
A credible residue-control program does not promise that every cleaner is universally suitable. It establishes a repeatable way to prove fitness for a defined process, detect meaningful change, and respond before a small contamination signal becomes a yield or reliability problem. For high-purity cleaning decisions, that is the standard worth building around.
Related News
 Antioxidants & Natural PreservativesWhat Quality Checks Matter When Sourcing Butylparaben for Personal CareButylparaben for personal care sourcing guide: compare assay, impurities, physical performance, documentation, traceability, and supplier quality to reduce formulation risk.MORE+
 Nano-microcapsule FormulationsHow Encapsulated Flavors Protect Taste During Processing and StorageEncapsulated Flavors protect taste from heat, oxygen, moisture, and storage loss. Explore smarter release, carrier selection, and processing strategies.MORE+
 Chelated Trace Element FertilizersHow Greenhouse Fertigation Systems Reduce Water and Fertilizer WasteGreenhouse fertigation systems reduce water and fertilizer waste with precise dosing, uniform irrigation, drainage monitoring, and smarter crop-zone control. Learn practical strategies.MORE+
 Supercritical CO2 Essential OilsHow Natural Essential Oil Blends Improve Consistent Product FragranceNatural essential oil blends help brands achieve consistent, appealing fragrance across batches. Explore smart blend design, stability testing, and product compatibility strategies.MORE+
 Non-ionic Surfactants & DefoamersHow to Choose Non Ionic Low Foaming Surfactants for CIP CleaningNon ionic low foaming surfactants for CIP cleaning: learn how to balance wetting, foam control, compatibility, and rinseability for reliable cleaning performance.MORE+
 Nano-microcapsule FormulationsHow Food Grade Cyclodextrin Complexes Protect Sensitive FlavorsFood grade cyclodextrin inclusion complexes help protect sensitive flavors from oxidation, evaporation, and processing loss while supporting controlled release and consistent sensory quality.MORE+
 Polymer-Coated Water Soluble NPKHow Fertilizer Coating Polymers Improve NPK Granule ReleaseFertilizer coating polymers for NPK granules improve controlled nutrient release, reduce loss risks, and enhance product consistency. Discover key selection and process insights.MORE+
 Chelated Trace Element FertilizersWhat Diammonium Phosphate Means for Crop Nutrition PlanningDiammonium Phosphate: learn how DAP supports early phosphorus access, nitrogen budgeting, smart placement, and balanced crop nutrition planning.MORE+
 Maillard Reaction Savory FlavorsHow to Assess a Flavor Bases Supplier List for Reliable SourcingGlobal Fine Chemicals & Agrochemical Intelligence Network flavor bases supplier list: assess specs, samples, supply risk, and true cost to source with confidence.MORE+
 Hydrocolloids & EmulsifiersHow Konjac Gum Powder Improves Texture in Low-Calorie FoodsKonjac gum powder improves body, stability, and mouthfeel in low-calorie foods. Discover practical tips for smoother sauces, beverages, and reduced-fat formulations.MORE+
 Supercritical CO2 Essential OilsWhat to Check Before Choosing a Botanical Essential Oils ManufacturerChoose a botanical essential oils manufacturer with confidence. Explore key checks for purity, traceability, compliance, batch consistency, and reliable supply.MORE+
 Microencapsulated FragrancesHow Fragrance Carriers for Detergents Improve Scent PerformanceFragrance carriers for detergents improve stability, fabric deposition, and long-lasting scent. Explore practical solutions for better wash-to-wear fragrance performance.MORE+
 Antioxidants & Natural PreservativesWhen Propyl Gallate Antioxidant Is the Right Choice for Oil StabilityPropyl gallate antioxidant: learn when it is the right choice for oil stability, shelf-life protection, processing compatibility, and smarter formulation decisions.MORE+
 Antioxidants & Natural PreservativesHow Potassium Sorbate Extends Shelf Life in Food and Beverage ProductsPotassium Sorbate helps food and beverage brands control yeast and mold spoilage. Explore pH, dosage, processing, and packaging strategies for reliable shelf life.MORE+
 Antioxidants & Natural PreservativesHow to Source Bulk Herbal Extracts With Reliable Quality ControlBulk herbal extracts sourcing guide: compare suppliers, verify traceability, review CoAs, and build reliable quality controls for safer, consistent purchasing.MORE+
 Antioxidants & Natural PreservativesWhat to Check Before Sourcing Butylparaben for Personal Care FormulasButylparaben for personal care sourcing guide: check market eligibility, purity, supplier controls, formula compatibility, packaging, and total risk before buying.MORE+
 Targeted Bio-pesticides & APIsChoosing Microbial Fungicides for Foliar Diseases in Integrated Crop ProgramsMicrobial fungicides for foliar diseases: learn how to match biology, formulation, tank compatibility, and timing for stronger integrated crop protection.MORE+
 Targeted Bio-pesticides & APIsHow Microbial Insecticides Control Caterpillars With Lower Crop Residue RiskMicrobial insecticides for caterpillars help protect crops with targeted early-larval control and lower residue-management pressure. Learn timing, coverage, compliance, and scouting essentials.MORE+
 Microencapsulated FragrancesHow to Add Encapsulated Laundry Fragrances Without Weakening Wash ResultsEncapsulated laundry fragrances: learn how to boost long-lasting scent while protecting cleaning power, stability, foam control, and fabric care.MORE+
 Supercritical CO2 Essential OilsHow Aroma Ingredients Shape Lasting and Skin-Safe Personal Care ProductsAroma ingredients for personal care: discover how to achieve lasting scent, formulation stability, skin safety, and confident product performance.MORE+
 Targeted Bio-pesticides & APIsInsecticides Explained Through Labels, Active Ingredients, and SafetyInsecticides explained through labels, active ingredients, formulations, and safety. Learn how to compare products, manage risk, and make informed crop protection decisions.MORE+
 Heavy-duty Industrial DegreasersHow to Select Parts Wash Cleaners for Automotive ComponentsParts wash cleaners for automotive components: learn how to match chemistry, materials, rinsing, safety, and waste controls for reliable cleaning results.MORE+
 Chelated Trace Element FertilizersHow Precision Fertigation Systems Improve Water and Nutrient ControlPrecision fertigation systems improve water and nutrient control with accurate dosing, uniform irrigation, smart monitoring, and reduced waste. Discover how to optimize crop performance.MORE+
 Hydrocolloids & EmulsifiersHow Bulk Price Factors Affect Hydrocolloid Stabilizer Blend SourcingHydrocolloid stabilizer blends bulk price: compare dosage efficiency, quality consistency, logistics, and documentation to reduce total sourcing costs.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow to Choose a Natural Sweeteners Supplier for Clean-Label ProductsNatural sweeteners supplier selection guide for clean-label products: compare formulation fit, traceability, documentation, and supply reliability.MORE+
 Non-ionic Surfactants & DefoamersWhat Cationic Surfactants Do and Where They Are UsedCationic Surfactants deliver antimicrobial action, conditioning, antistatic control, and surface treatment benefits. Explore key uses, compatibility, and safe selection tips.MORE+
 Targeted Bio-pesticides & APIsHow to Evaluate Pesticide Suspension Concentrates for Field StabilityPesticide Suspension Concentrates: learn how to evaluate field stability, redispersibility, dilution, tank-mix compatibility, and spray safety for reliable performance.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Systems for Meat Products Improve Texture and YieldHydrocolloid systems for meat products improve yield, texture, water retention, and slicing quality. Explore practical formulation strategies for stable, high-performing meat products.MORE+
 Microencapsulated FragrancesHow Laundry Fragrances for Liquid Detergents Improve Scent LongevityLaundry fragrances for liquid detergents: discover how fragrance design, deposition, and encapsulation create lasting fabric freshness and stronger product appeal.MORE+
 Nano-microcapsule FormulationsChoosing Fragrance Preparations That Perform Well in Personal WashFragrance preparations for personal wash: learn how to select options that protect clarity, stability, foam, scent performance, and packaging compatibility.MORE+
 Controlled-Release ThermodynamicsModified Cyclodextrins Explained for Controlled Fragrance ReleaseModified cyclodextrins enable controlled fragrance release, odor control, and volatile-note protection. Explore how they optimize performance in detergents, fabric care, and more.MORE+
 Microencapsulated FragrancesHow Fragrance Delivery Systems Improve Fabric Softener LongevityFragrance delivery systems for fabric softeners improve scent longevity through smart protection, reliable deposition, and controlled release for lasting freshness.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Cardamom Oil Supplier for Reliable SupplyNatural cardamom oil supplier evaluation guide: verify botanical origin, purity, batch consistency, documentation, packaging, and delivery reliability for confident sourcing.MORE+
 Maillard Reaction Savory FlavorsHow Ethyl Maltol Purity Testing Supports Flavor Safety ComplianceEthyl Maltol purity testing strengthens flavor safety compliance through identity checks, impurity profiling, supplier verification, and audit-ready documentation.MORE+
 Microencapsulated FragrancesEssential Oil Extracts Compared for Fragrance and Wellness UsesEssential Oil Extracts compared for fragrance and wellness: explore scent profiles, extraction methods, stability, safety, and sourcing insights for smarter formulation choices.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat Drives Zero Calorie Sweeteners Bulk Price in 2026Zero calorie sweeteners bulk price in 2026: compare specifications, dosage, quality, freight, and supply risk to make smarter sourcing decisions.MORE+
 EPA FIFRA & FDA GRAS RegsSynthetic Food Preservatives Rules That Support Safer FormulasSynthetic Food Preservatives: learn the rules for safer formulas, compliant use levels, validated shelf life, labeling, and reliable microbial control.MORE+
 Micelle Fluidics & ChelationHow Anionic Industrial Dispersants Improve Coating StabilityAnionic industrial dispersants improve coating stability, pigment wetting, viscosity control, gloss, and storage performance. Learn how to select and test the right solution.MORE+
 Supercritical CO2 Essential OilsHow to Choose Eucalyptus Oil Grades for Clean, Consistent ProductsChoose the right Eucalyptus Oil grade with confidence. Compare cineole content, purity, origin, processing, documentation, and application fit for consistent products.MORE+
 Micelle Fluidics & ChelationWhat Are Cationic Surfactants and Where Are They Commonly Used?Cationic Surfactants deliver powerful surface affinity for disinfection, fabric softening, hair conditioning, antistatic control, and industrial treatments. Explore key uses and selection factors.MORE+