How to Evaluate an Electronic Grade Cleaners Supplier
Choosing an electronic grade cleaners supplier requires more than comparing price and purity claims. Business evaluators must assess contamination control, material compatibility, batch consistency, technical documentation, regulatory readiness, packaging integrity, and supply reliability. This guide outlines the key criteria for identifying suppliers that can support demanding electronics, semiconductor-related, and high-purity industrial cleaning applications with dependable product performance.
The commercial difficulty is that “electronic grade” is not a universally identical product category. Its meaning changes with the cleaning step, the component being processed, the acceptable residue level, the materials in contact, and the customer’s own quality system. A cleaner used for removing machining oils from electronic housings has a very different risk profile from a chemistry used in precision assembly, display manufacturing, printed circuit board processing, or semiconductor-adjacent operations.
For that reason, supplier evaluation should begin with the process requirement rather than the supplier’s catalogue language. The objective is not merely to find a high-purity cleaner at an acceptable unit price. It is to identify a source capable of delivering repeatable cleaning outcomes without introducing particles, ionic contamination, organic residues, corrosion, material damage, or avoidable supply disruption.
Define the cleaning risk before comparing suppliers
A purchase specification that only states “electronic grade cleaner” leaves too much room for interpretation. Before approaching suppliers, the buyer should define what failure the cleaning process must prevent.
Important questions include:
- What contamination must be removed: oils, flux residues, fingerprints, particles, metal fines, silicone residues, polishing compounds, or adhesive residues?
- What materials will contact the cleaner: copper, aluminium, stainless steel, nickel, tin, solder mask, glass, ceramics, engineering plastics, elastomers, coatings, or sensitive assemblies?
- Is the process aqueous, semi-aqueous, solvent-based, vapour-based, ultrasonic, spray, immersion, manual wipe, or a combination?
- What is the downstream sensitivity? Will the cleaned part be coated, bonded, plated, encapsulated, soldered, optically inspected, electrically tested, or placed into a high-purity environment?
- Which residues are critical: non-volatile residue, chloride, fluoride, sulphate, sodium, potassium, particulate matter, surfactant film, or moisture?
- What rinse-water quality, drying method, filtration arrangement, and bath-control practices exist on site?
This work often reveals that the cleaner is only one element in a contamination-control system. A product can perform well in a supplier demonstration but fail in production if the process uses poor-quality rinse water, an overloaded bath, unsuitable filters, contaminated drying air, or incompatible equipment seals. Suppliers should be evaluated partly on whether they understand these operational interactions, rather than simply promising that their chemistry is “safe for electronics.”
Purity claims need to be converted into measurable release criteria
Purity is relevant, but it is not enough. A cleaner may have a high stated assay while still being unsuitable for a sensitive process because trace ions, particles, stabilizers, additives, or drying residues are not adequately controlled. The key issue is whether the supplier can define, measure, and consistently meet the contaminants that matter to the application.
For aqueous cleaners, relevant parameters may include conductivity, total organic carbon where appropriate, ionic contamination, metal content, chloride and sulphate limits, insoluble matter, pH, density, and non-volatile residue. For solvent systems, buyers may need to examine water content, acidity, evaporation residue, particulate contamination, stabilizer content, and suitability for the intended drying and ventilation conditions.
There is no single specification that fits every application. Requiring unnecessarily extreme limits can raise cost without improving real production performance. Conversely, accepting broad generic specifications can create a hidden risk when the cleaner is used before coating, fine-pitch assembly, bonding, high-voltage insulation, or precision inspection.
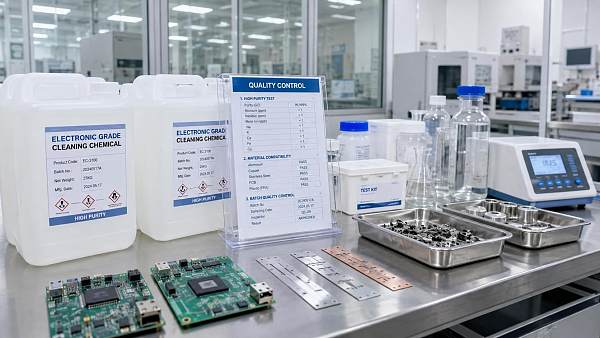
A credible electronic grade cleaners supplier should be able to explain the test methods behind its claims. A certificate of analysis is useful only if it identifies relevant parameters, specification ranges, results for the actual batch, test methods or controlled internal procedures, batch number, manufacturing date, and release status. A one-line certificate stating “pass” or “high purity” provides little protection in a quality investigation.
Batch consistency matters more than an impressive qualification sample
Many sourcing failures begin with a successful sample trial. The qualification batch may be freshly produced, carefully packed, and supported by intensive technical attention. Commercial supply can later show variation in cleaning strength, foam behaviour, residue profile, colour, odour, pH, or particle level. These changes may be small in a general industrial application but significant in precision electronics manufacturing.
Supplier assessment should therefore examine how consistency is maintained after sample approval. Useful questions include:
- Are key raw materials qualified from more than one source, and how are changes controlled?
- Does the supplier use dedicated or appropriately cleaned production equipment for high-purity grades?
- What controls prevent cross-contamination from pigments, metalworking fluids, surfactants, or other chemical lines?
- How are blending, filtration, filling, and transfer lines managed?
- What is the lot size, and how much variation can occur between manufacturing campaigns?
- Is retain-sample storage available for complaint investigation?
- Will the buyer receive advance notice of changes to formulation, raw-material source, manufacturing site, packaging, or test method?
Formal change notification is particularly important. A supplier may regard replacement of a solvent grade, surfactant source, corrosion inhibitor, or packaging liner as a routine internal adjustment. For the buyer, the same change can affect wetting, rinsability, residue formation, seal compatibility, or analytical test results. The commercial agreement should specify which changes require prior notification and, where necessary, requalification.
Assess cleaning performance together with material compatibility
A more aggressive cleaner is not automatically the better cleaner. Strong alkalinity, high solvent power, or elevated operating temperature can improve soil removal while increasing the risk of metal staining, attack on aluminium alloys, stress cracking in plastics, swelling of seals, loss of marking ink, solder-mask effects, or damage to adhesives and coatings.
Evaluation should include representative substrates and realistic process conditions. A bench test on a clean metal coupon is rarely enough. The trial should reflect actual soil load, concentration, temperature, contact time, mechanical action, rinse sequence, drying method, and expected bath age. When possible, parts should then be assessed not only for visual cleanliness but also for downstream performance: adhesion, coating uniformity, solderability, electrical reliability, corrosion resistance, optical quality, or bonding strength.
Suppliers should be asked for compatibility guidance, but generic compatibility charts should not replace application trials. The same polymer can react differently depending on stress, exposure time, temperature, grade, moulding additives, and residual contaminants. A supplier that acknowledges these limits and supports a structured trial usually represents less risk than one offering blanket assurances.
Look beyond the cleaner: packaging is part of contamination control
High-purity chemistry can lose its value during filling, storage, or transport. Packaging should be reviewed as carefully as the liquid specification, especially where the product is used in low-residue or controlled production environments.
The review should cover container material, cap and seal design, liner compatibility, tamper evidence, cleanliness of filling operations, filling environment, and protection against moisture uptake or solvent loss. For products sensitive to light, oxidation, or water absorption, the supplier should define storage conditions and realistic shelf life based on the actual package format.
Bulk supply creates additional questions. Intermediate bulk containers, drums, and tank deliveries can reduce handling cost but may increase contamination and traceability risks if containers are reused without appropriate control. Buyers should establish whether bulk containers are dedicated, reconditioned, or shared across chemical families; how previous contents are controlled; whether cleaning validation exists; and what documentation accompanies each delivery.
Packaging choices also affect total procurement cost. Small packs may offer better traceability and lower exposure after opening but generate more handling and waste. Bulk formats can lower price per litre, yet require appropriate storage, dispensing equipment, spill management, and inventory discipline. The lowest packaging cost is not necessarily the lowest cost of use.
Calculate total process cost, not just purchase price
Electronic cleaning chemistry is often treated as a consumable line item, but its real economic effect extends across yield, labour, water consumption, energy, waste treatment, maintenance, and failure risk. A lower-priced product can become costly if it requires higher concentration, produces persistent foam, shortens bath life, increases rinse-water demand, causes corrosion, or creates more difficult wastewater treatment.
A practical cost comparison should include the following:
- Delivered price, including hazardous-goods surcharges, packaging, freight, import costs, and local storage requirements;
- Recommended operating concentration and actual chemical consumption per production unit;
- Bath life under normal soil loading and the cost of replenishment or replacement;
- Water, energy, filtration, drying, and wastewater treatment requirements;
- Labour required for make-up, monitoring, cleaning, and corrective action;
- Scrap, rework, line stoppage, or customer-return risk associated with cleaning variation;
- Capital changes needed for pumps, seals, ventilation, filtration, or dosing equipment.
Cost-per-cleaned-part is generally more informative than price-per-kilogram. Where reliable production data is unavailable, suppliers should support a controlled pilot using agreed measurement points. It is reasonable to ask for a method to monitor concentration and bath condition, whether through titration, conductivity, refractive index, analytical testing, or another validated site-specific approach. Without process control, even a technically suitable cleaner can generate inconsistent results and disputed consumption figures.
Documentation and regulatory readiness reduce cross-border risk
In international procurement, incomplete documentation can delay customs clearance, create safety issues, or interrupt customer audits. The required document package depends on the destination market and use case, but buyers commonly need a current safety data sheet in the appropriate language and regulatory format, technical data sheet, certificate of analysis, transport classification, country-of-origin information, and clear product identification.
Where applicable, regulatory compliance may involve chemical inventory status, registration obligations, classification and labelling requirements, and restrictions on specific substances. Suppliers should not be selected solely because they state that a product is “compliant.” The buyer needs to determine which market requirements apply to its own import, use, distribution, and customer supply chain.
This is especially relevant for solvent-containing cleaners. Regulatory pressure relating to worker exposure, emissions, waste handling, and restricted substances can alter the practical cost and long-term availability of a chemistry. A replacement product may appear attractive because it is marketed as lower impact, but it still requires validation for cleaning effectiveness, material compatibility, drying behaviour, and any new safety controls.
Strong suppliers can provide documentation promptly, maintain revision control, and explain the limits of their compliance statements. They also have a clear process for handling inquiries about composition, transport, emergency response, and restricted-substance declarations without disclosing confidential formulation details unnecessarily.
Test supply resilience before awarding a long-term contract
Electronics supply chains are sensitive to interruption. A cleaning material may be a minor spend category but can stop a production line when it is unavailable or cannot be substituted quickly. Supply resilience should therefore carry more weight than its annual purchase value might suggest.
Evaluate manufacturing location, inventory position, raw-material dependence, export capability, lead time, minimum order quantity, warehouse strategy, and alternative logistics routes. A distributor can offer valuable local stock and rapid support, but the buyer should understand whether the distributor has direct technical authority, reliable access to batch documentation, and visibility into upstream supply conditions.
For critical materials, it is sensible to distinguish between a qualified primary source and an unqualified emergency option. Dual sourcing is useful only if both products have been properly tested in the relevant process. Maintaining a second supplier on paper, without completed validation and documented change control, may provide little protection during a disruption.
Use supplier audits and trials to separate capability from presentation
A supplier audit does not always require a large on-site programme. For lower-risk applications, a structured remote assessment supported by quality documents, manufacturing information, sample history, and a commercial review may be sufficient. For high-sensitivity processes, an on-site audit or detailed third-party assessment can be justified.
The most informative audit areas are often practical: segregation of high-purity lines, cleaning of transfer equipment, incoming raw-material controls, filtration practice, calibration of test equipment, nonconformance handling, complaint investigation, retained samples, and traceability from finished batch to key inputs. These subjects reveal more than broad statements about quality commitment.
Trials should be documented with agreed acceptance criteria before testing begins. This avoids the common situation in which the supplier focuses on visible soil removal while the user later identifies a residue, foam, corrosion, or downstream adhesion problem. A well-designed trial defines the part type, contamination type, operating window, analytical checks, performance thresholds, and decision process for scale-up.
What a defensible supplier decision looks like
The best electronic grade cleaners supplier is not necessarily the company with the lowest quote, the largest product range, or the most ambitious purity claim. It is the supplier whose product specification, process controls, packaging system, technical support, documentation, and delivery model match the actual risk of the cleaning application.
A defensible purchasing decision links commercial terms to technical evidence. It shows why the selected chemistry is appropriate for the soil and substrate, how batch quality will be verified, what changes require notification, how the material will be monitored in use, and what contingency exists if supply is interrupted. This approach may require more work before approval, but it reduces the far greater cost of production instability, quality escapes, and repeated requalification later.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+