How to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure Supply
The lowest quotation for ultra-pure cleaning chemistry can become the highest-cost option when a trace contaminant, unstable formulation, or damaged container interrupts wafer processing. A semiconductor cleaners factory should therefore be evaluated as a controlled supply system: raw-material selection, purification, blending, packaging, analytical release, change control, and delivery conditions all affect the chemical that reaches the point of use.
Start with the intended cleaning step rather than a generic purity grade. A chemical used for particle removal, organic residue removal, metallic contamination control, post-etch cleaning, or equipment maintenance faces different performance limits. Concentration, bath temperature, dilution water quality, contact time, substrate type, and downstream rinse sequence determine which contaminants matter most. A specification that is suitable for a less sensitive wet process may be unsuitable where low metallic residue, low particle count, or stable etch behavior is required.
Translate the Process Need into a Releasable Specification
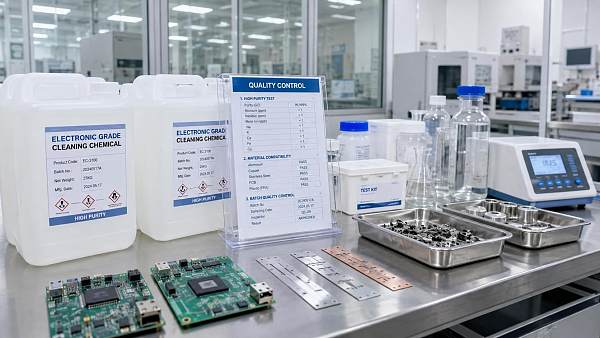
“High purity” is not a complete purchasing specification. It should be converted into properties that the factory can measure on every relevant batch and report in a consistent format. The required parameter set differs by chemistry, but often includes assay, water content, residue after evaporation, trace metals, anionic and cationic contaminants, particles, color, density, and acidity or alkalinity. For formulated cleaners, the composition range, surfactant residue, foaming behavior, rinseability, and compatibility with filters or delivery hardware may also need control.
Trace-metal limits need particular care. A total-metals figure can conceal an unacceptable contribution from a specific element. The relevant concern is often the element profile, the analytical detection capability, and the sampling method, not merely a statement that metals are “low.” Request the list of reported elements, the unit basis, the method used, method detection limits, and the treatment of results below detection. A result reported as non-detect has little value if the detection limit sits above the process threshold.
Particle specifications are frequently misunderstood in the same way. A single particle-count value is meaningful only with its size threshold, test method, sample handling method, and container condition. A factory can produce a clean bulk liquid that gains particles from a transfer hose, cap liner, filter housing, or packaging operation. Ask whether the release sample is drawn before or after final filtration and whether the test sample represents the finished, sealed package.
Look Past the Certificate of Analysis
A certificate of analysis is a batch-release record, not a complete demonstration of manufacturing control. Review several certificates from separate production dates, ideally spanning normal manufacturing conditions rather than consecutive fills from one campaign. The objective is to see whether reporting fields, units, analytical limits, product naming, and batch-to-batch results remain coherent. Repeated values exactly at a reporting threshold deserve clarification, especially where the test method has limited resolution.
Ask how specifications are established and what happens when an internal result approaches a limit. A reliable response describes hold procedures, investigation routes, retesting rules, disposition authority, and documentation. A weak response relies on broad assurances that every lot passes. The distinction matters because ultra-pure supply depends on preventing borderline material from being released through sampling variation or an informal retest.
Analytical capability should match the material risk. Inductively coupled plasma methods may be appropriate for elemental screening, while ionic contaminants, organic residues, and particles require different techniques. The exact instrument name is less useful than evidence that the method has suitable sensitivity, calibration discipline, contamination controls, and defined sample preparation. Acid digestion, dilution media, digestion vessels, and laboratory water quality can change a trace result. A factory should be able to explain how blank control and laboratory contamination are managed.
Retained samples are another practical indicator. Confirm how long finished-product samples are held, whether retain containers are representative of shipped packaging, and how a disputed batch would be investigated. When a deviation appears after delivery, the ability to compare the supplied container, factory retain, raw-material records, and filling record is far more useful than a generic statement of conformance.
Inspect the Contamination Pathway Through Production
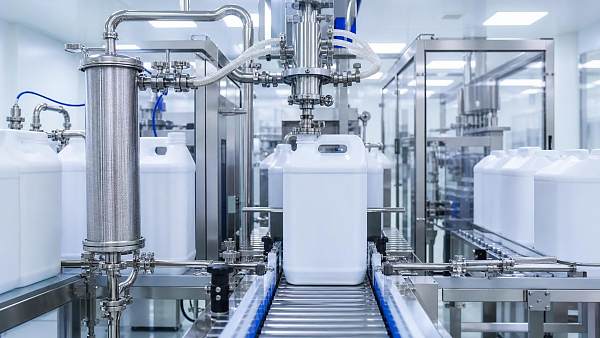
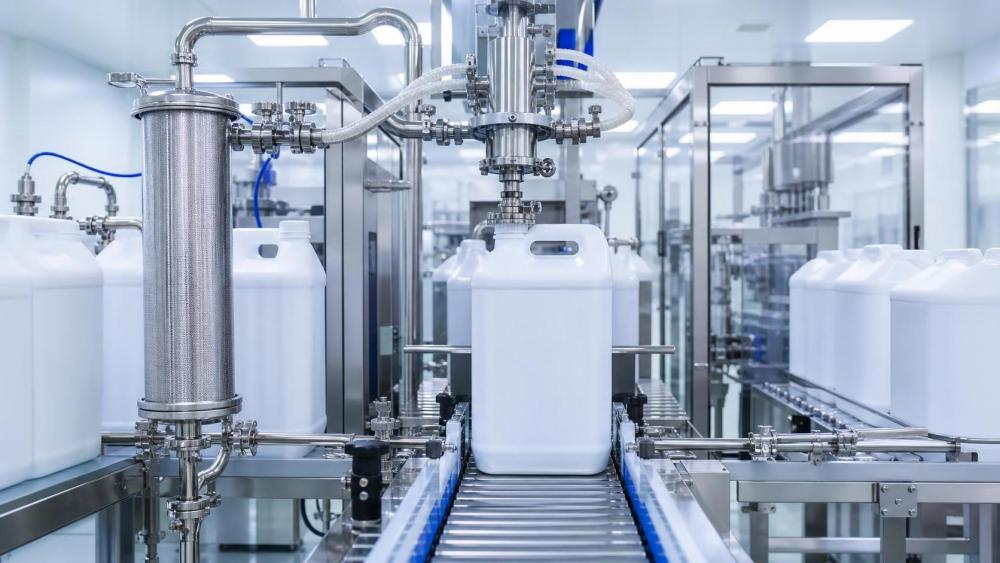
The important question during a factory assessment is not whether the facility looks orderly. It is whether the production route prevents contamination from entering, persisting, or cross-contacting the chemistry. Map the route from incoming material through storage, transfer, purification or blending, final filtration, filling, and finished-goods staging. Each connection point can add risk.
Dedicated equipment is preferable where chemical families or purity grades have incompatible contamination profiles. If vessels, lines, pumps, or filters are shared, examine the validated cleaning sequence, flush medium, recovery or disposal handling, and evidence used to confirm readiness for the next product. A line can be visually clean while still releasing residues that matter at semiconductor process levels. The concern is heightened when prior products contain metal-bearing additives, surfactants, stabilizers, pigments, corrosion inhibitors, or higher-residue solvents.
Water is often the hidden variable. Where water is used for dilution, washing, rinsing, or equipment cleaning, obtain a description of the water source, polishing steps, storage loop, monitoring points, and response to an out-of-limit result. Water quality should be considered alongside the cleaner itself. A high-grade concentrate diluted with poorly controlled water does not retain the expected impurity profile.
Final filtration needs a specific discussion. Filter material compatibility, pore rating, integrity verification, change frequency, installation controls, and differential-pressure management all influence product cleanliness. Finer filtration is not automatically better: an unsuitable membrane can shed extractables, alter a formulated cleaner, or create excessive hold-up and inconsistent first-fill material. The factory should demonstrate that the filtration choice suits the chemical and that filter replacement does not introduce a new contamination pathway.
Raw Materials and Change Control
Ultra-pure output cannot be separated from incoming-material discipline. Review whether each critical raw material has an approved source, incoming identity confirmation, relevant impurity controls, and segregation from general chemical inventory. A supplier may use nominally identical starting materials from multiple sources; their impurity patterns, packaging cleanliness, or stabilizer content may differ enough to alter finished product behavior.
Change notification deserves contractual attention. Changes in raw-material source, purification media, production site, vessel lining, filter type, packaging resin, cleaning agent, analytical method, or manufacturing route should be assessed before implementation when they could affect the delivered chemistry. An agreement should define what constitutes a reportable change, the notification period, supporting data expectations, and the disposition of inventory produced before and after the change. Without this discipline, a product name and nominal specification can remain unchanged while the practical contamination risk shifts.
Packaging Is Part of the Chemical Specification
Container choice affects cleanliness, safety, handling cost, and shelf-life confidence. The appropriate package depends on chemical compatibility, filling environment, shipment duration, dispensing arrangement, and the need to prevent air ingress or external contamination. Examine the container resin or metal grade, liner, cap, gasket, venting design, cleanliness procedure, and tamper-evident features. For reusable containers, investigate the return, inspection, cleaning, drying, and release process rather than assuming reuse is inherently unsuitable or acceptable.
Packaging failures are not limited to leaks. Extractables from closures, particles from cap threads, contamination from poorly controlled container storage, and mislabeled drums can all cause material rejection or a difficult investigation. Lot traceability should connect the finished chemical batch to the package lot, filling line, fill date, and closure components. That link is particularly important when only part of a shipment is affected.
Storage and transport requirements must be operationally realistic. A temperature-sensitive cleaner, a material vulnerable to moisture pickup, or a solution prone to crystallization needs stated transport controls that can actually be maintained across the route. Ask where the material is staged before dispatch, how trailers or freight containers are evaluated, how temperature excursions are recorded when required, and what happens when a seal is compromised. A factory that controls the filling room but cannot describe the handoff to logistics has an incomplete quality system.
Compare Landed Cost Against Failure Exposure
Unit price is only one part of the cost model. Meaningful comparison includes qualification samples, analytical verification, container format, minimum order quantity, usable shelf life on arrival, freight restrictions, cleaning or purge losses during changeover, inventory carrying requirements, and the likely cost of an urgent replacement shipment. A lower-priced material can lose its advantage when it requires extra incoming testing, has short remaining shelf life, or arrives in a format incompatible with existing chemical distribution hardware.
Qualification samples should be representative of normal production and normal packaging. Small laboratory bottles filled outside the standard production route are useful for initial compatibility work, but they do not prove commercial supply control. Before final approval, connect the sample to a documented batch, confirm its filling route, and establish whether the same release tests apply to routine deliveries.
Supply resilience should be judged with the same precision as purity. Clarify production lead time, batch size flexibility, raw-material dependency, qualified alternate equipment, reserved capacity arrangements where relevant, and the communication path for delay or deviation. Dual sourcing may reduce interruption exposure, but only when both materials are independently qualified and their impurity profiles, concentration ranges, packaging interfaces, and process outcomes are understood. Two sources carrying the same label are not automatically interchangeable.
Use a Focused Factory Assessment
A useful assessment follows the product through the site and tests the connection between documents and physical controls. Observe how a batch record identifies raw materials, equipment status, filtration, fill count, and release decision. Compare the stated cleaning procedure with equipment labels and maintenance records. Trace a recent finished lot backwards from the certificate to retained sample, packaging components, and incoming materials.
- Ask for an explanation of a recent deviation that did not result in product release. The value lies in the investigation logic, containment action, and record trail.
- Review a batch produced after equipment maintenance or a filter change, since these events often reveal whether restart controls are practical.
- Examine how unopened containers are protected before filling and how filled packages are segregated from non-released material.
- Confirm that technical, quality, logistics, and commercial contacts share the same product code, specification revision, and change-notification process.
The strongest semiconductor cleaners factory is not identified by a polished purity claim alone. It is identified by a traceable link between process requirements, analytical evidence, contamination controls, finished-package integrity, and disciplined handling of changes. That evidence creates a sound basis for comparing offers whose quoted specifications may initially appear identical.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+