How to Compare Semiconductor Process Cleaners from Different Suppliers
How to compare semiconductor process cleaners from different suppliers? For technical evaluation teams, the answer starts with process fit, contamination risk, material compatibility, and supplier control capability rather than price alone.
In semiconductor environments, a cleaner that looks acceptable on a general specification sheet may still create residue, surface damage, bath instability, or qualification delays in production.
This article explains how technical teams can compare semiconductor process cleaners in a practical way, using criteria that support sourcing decisions, validation planning, and long-term process reliability.
Start with the real search question: which cleaner is safer to qualify and more stable to use?
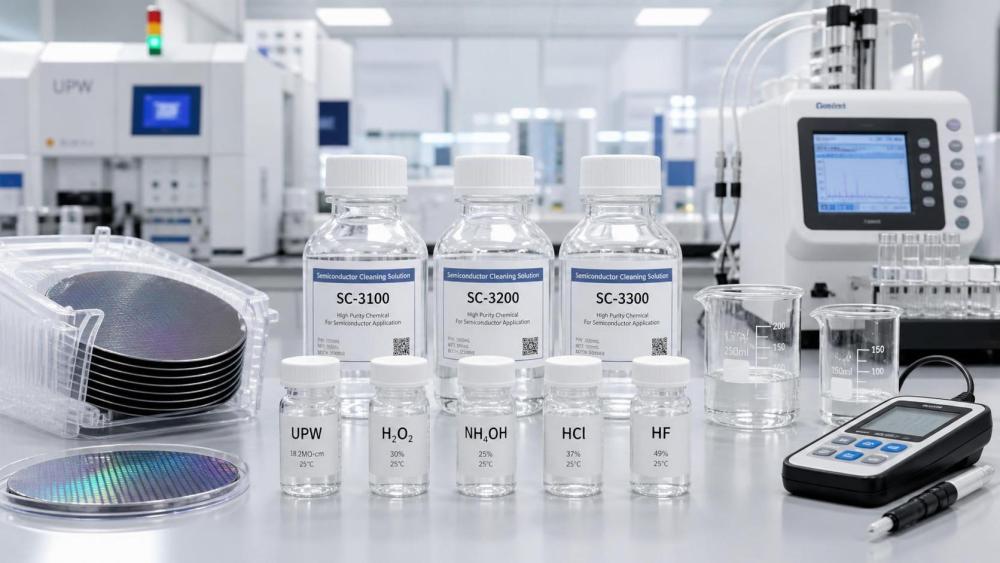
The core search intent behind “How to compare semiconductor process cleaners from different suppliers” is not academic. Buyers want a reliable comparison method for actual selection decisions.
Technical evaluation teams usually need to decide whether two products are truly equivalent, whether a lower-cost option brings hidden process risk, and whether a supplier can support stable production.
That means the comparison should focus on the full use case: cleaning target, substrate sensitivity, residue tolerance, rinse behavior, analytical control, packaging cleanliness, and documentation quality.
In practice, the best supplier is rarely the one with the shortest datasheet. It is the one whose cleaner performs consistently within your process window and can be supported over time.
Define the exact cleaning application before comparing any supplier claims
Many comparison exercises fail early because teams compare products by generic category names such as solvent cleaner, alkaline cleaner, surfactant cleaner, or high-purity cleaning agent.
Those labels are too broad for semiconductor process evaluation. A cleaner for photoresist residue, post-etch contamination, particle removal, or metal surface conditioning may require very different chemistry.
Before reviewing supplier offers, define the intended application in technical terms. Identify the contamination type, process step, substrate material, temperature range, contact time, and rinse sequence.
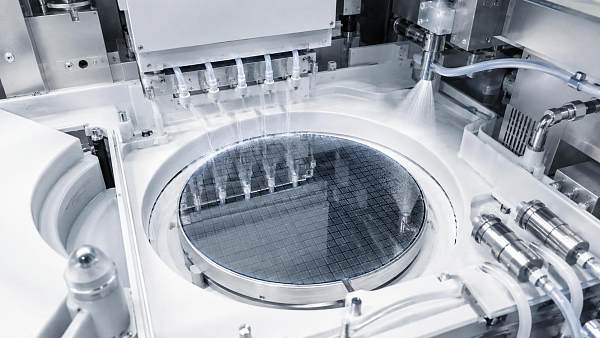
Also clarify whether the cleaner will be used in batch immersion, spray, megasonic, single-wafer, or manual maintenance cleaning. Method of use can change performance and compatibility significantly.
Once the application is defined clearly, the comparison becomes more meaningful. You are no longer comparing products in theory. You are comparing their ability to solve a specific process problem.
Compare contamination removal performance, not just product composition
The first technical question is simple: how effectively does each cleaner remove the target contamination under your actual operating conditions? Everything else comes after that baseline requirement.
Ask suppliers for performance data linked to relevant contamination classes, such as organic residues, particles, ionic contamination, metal traces, oxide-related films, or mixed process residues.
Be careful with performance claims generated under ideal laboratory conditions. A cleaner may perform well at high temperature or long dwell time but lose efficiency in your controlled production window.
Technical teams should compare removal efficiency across the same test design. Use aligned wafer types, contamination load, cleaning time, concentration, rinse conditions, and analytical measurement methods.
If possible, convert supplier comparison into a side-by-side validation matrix. This helps separate chemistry differences from test-condition differences and produces a defensible decision record.
Residue profile often matters more than aggressive cleaning strength
In semiconductor processing, strong cleaning performance is not enough if the product leaves surfactant film, organic residue, ionic traces, or decomposition byproducts on the surface.
A supplier may present a cleaner as highly efficient because it removes visible contamination quickly. But if post-clean residue remains, downstream yield loss may appear later in the process.
That is why residue control should be a major comparison category. Ask for data on total organic carbon contribution, ionic residue, non-volatile residue, metal content, and rinse-out behavior.
Technical teams should also examine whether the cleaner requires unusually intensive rinsing to achieve acceptable surface condition. Difficult rinse-out can increase water use, cycle time, and process variability.
When comparing suppliers, a slightly slower cleaner with cleaner rinse behavior may be a better process choice than a more aggressive chemistry with persistent trace residue.
Material compatibility is a critical filter, especially for advanced nodes and mixed materials
Semiconductor process cleaners contact sensitive materials, including silicon, silicon oxide, low-k materials, metals, photoresist systems, polymers, ceramics, seals, and equipment wetted parts.
Because of that, material compatibility is not a secondary issue. A cleaner that performs well on contamination removal can still create corrosion, swelling, surface roughening, delamination, or pattern damage.
Ask each supplier for compatibility data tied to the exact materials in your process and equipment. Generic statements such as “good compatibility with most substrates” are not enough.
Review pH range, solvent strength, oxidizing behavior, additive package, and known interactions with aluminum, copper, titanium, barrier layers, quartz, fluoropolymers, and elastomers if relevant.
If your process includes multiple materials in one cleaning sequence, the comparison becomes even stricter. The cleaner must work across the full stack without causing selective damage.
Purity grade and impurity control must be examined beyond headline specifications
For semiconductor-related cleaning materials, purity is not just a marketing term. It is a process control issue tied directly to contamination risk, consistency, and qualification confidence.
Do not stop at high-level purity claims. Ask for impurity profiles covering trace metals, chloride or sulfate levels, particles, water content, non-volatile matter, and lot-to-lot variation limits.
It is also useful to understand the supplier’s manufacturing and filtration controls. A product can meet one certificate of analysis while still showing inconsistent contamination behavior across batches.
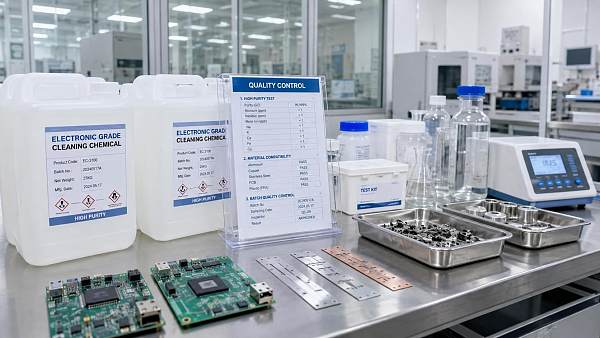
Technical evaluation teams should ask how specifications are monitored, which analytical instruments are used, and whether semiconductor-grade packaging and filling environments are controlled properly.
When two cleaners appear chemically similar, impurity management often becomes the real differentiator. This is especially true when processes have narrow tolerance for metallic or ionic contamination.
Evaluate bath stability, shelf life, and operating consistency under production conditions
A cleaner may pass a short trial but still cause trouble during routine use if it separates, degrades, absorbs moisture, changes pH, or loses activity during storage and operation.
That is why supplier comparison should include stability in both unopened packaging and in-use conditions. Shelf life on paper is useful, but operating stability matters more for manufacturing teams.
Ask whether the product is sensitive to temperature fluctuation, light exposure, metal ion introduction, or dilution water quality. These factors can affect concentration control and repeatability.
For recirculated or monitored cleaning systems, determine whether the chemistry remains stable over the expected bath life. Instability can increase maintenance frequency and reduce line efficiency.
A technically strong supplier should be able to explain failure modes clearly, not just provide a nominal shelf-life figure. That supports better process planning and change-control management.
Documentation quality reveals whether a supplier is ready for serious technical support
For technical evaluation personnel, documentation is part of product quality. Weak documentation usually signals weak process understanding, limited quality discipline, or insufficient customer support capability.
Review the completeness and clarity of the technical data sheet, safety data sheet, certificate of analysis, regulatory declarations, storage guidance, and packaging specifications.
Ask whether the supplier can provide lot traceability, change notification procedures, impurity trend data, recommended operating ranges, and troubleshooting guidance for qualification work.
If the product may be used across multiple global sites, also assess whether the supplier can support documentation consistency across regions and respond to customer audits when needed.
In many B2B chemical sectors, including high-purity industrial cleaning materials, documentation readiness helps procurement and engineering teams move faster with lower internal friction.
Do not separate supplier capability from product comparison
Semiconductor process cleaners should never be compared as chemistry alone. The supplier’s manufacturing discipline, quality systems, delivery reliability, and technical responsiveness are part of the product value.
Ask practical questions. Can the supplier maintain batch consistency at commercial scale? Are packaging materials appropriate for contamination-sensitive environments? What is the lead-time stability history?
Also assess whether the supplier has experience supporting qualification, process troubleshooting, and specification alignment with demanding industrial customers rather than only general cleaning markets.
Some suppliers can provide a promising sample but struggle with repeated large-scale delivery, documentation control, or post-sale technical support. That creates avoidable operational risk.
For technical evaluation teams, the best comparison model includes both product data and supplier capability scorecards. This gives a more accurate picture of total sourcing risk.
Use a weighted comparison matrix instead of informal product discussions
When multiple departments are involved, cleaner selection can become fragmented. Engineering emphasizes performance, procurement emphasizes cost, and quality teams emphasize documentation and traceability.
A weighted comparison matrix helps align these priorities. Typical categories include removal efficiency, residue level, compatibility, purity, batch consistency, stability, packaging, technical support, and commercial terms.
Not every category should carry equal weight. For semiconductor applications, contamination control, residue profile, and compatibility usually deserve more weight than headline unit price.
Include mandatory pass-fail criteria as well. For example, if a cleaner fails on a critical substrate compatibility test, it should not remain in consideration because of lower cost.
This structured method improves internal communication and makes final approval easier. It also creates a documented basis for future supplier reviews or requalification exercises.
Consider total cost of ownership, not only purchase price
Technical teams know that the cheapest cleaner is often not the lowest-cost solution. Semiconductor process economics depend on yield, cycle time, water use, waste treatment, maintenance, and failure risk.
Compare dosage, operating temperature, cleaning time, rinse demand, bath life, filtration requirement, packaging efficiency, and disposal implications across suppliers.
A cleaner with higher purchase cost may reduce defect risk, shorten rinse steps, improve bath stability, or extend equipment uptime. Those gains can outweigh the price difference quickly.
This is especially important for facilities working in high-purity processing environments where contamination incidents are expensive and root-cause analysis can consume substantial engineering resources.
For sourcing teams working with technical evaluators, total cost of ownership provides a more realistic framework than basic price-per-kilogram comparison.
What technical evaluators should ask suppliers before final selection
A strong supplier comparison process depends on asking the right questions early. Start with application-specific performance data and request the exact test conditions behind every claim.
Ask for impurity specifications by analyte category, not only summary purity. Request compatibility evidence for your substrates, equipment materials, seals, and operating temperatures.
Confirm lot-to-lot control limits, change notification policy, packaging cleanliness standards, storage conditions, and shelf-life validation basis. These details often expose hidden differences between suppliers.
It is also useful to ask how the supplier handles customer complaints, out-of-spec events, and technical troubleshooting during line qualification. Response discipline matters in real production.
Suppliers that answer these questions clearly and consistently are usually easier to qualify and more dependable in long-term supply relationships.
Conclusion: compare semiconductor process cleaners as process control tools, not commodity chemicals
When technical teams ask how to compare semiconductor process cleaners from different suppliers, the most practical answer is to evaluate process fit before commercial attractiveness.
The right cleaner should remove the target contamination, rinse cleanly, protect sensitive materials, maintain purity, remain stable in use, and come from a supplier with disciplined quality control.
That comparison requires structured testing, aligned data review, and supplier capability assessment. It cannot be reduced to broad product labels or simple price comparison.
For FCAS readers working in technical evaluation, procurement, formulation support, or industrial cleaning material sourcing, this approach creates better decisions with lower qualification risk.
In short, the best semiconductor process cleaner is the one that performs consistently inside your real process window and is backed by a supplier capable of supporting that performance every time.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+