How to Compare Metal Cleaning Chemicals Wholesale Offers
Wholesale sourcing of metal cleaning chemicals looks simple until a buyer tries to compare offers that appear similar on a quotation sheet. Two products may both be described as alkaline degreasers, low-foam metal cleaners, or multi-metal process cleaners, yet differ substantially in dilution rate, bath life, corrosion behavior, wastewater burden, documentation quality, and fit with the actual production line.
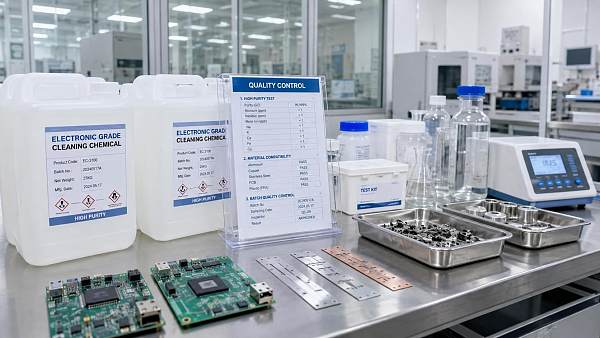
For business evaluators, the central question is not which supplier posts the lowest drum or tonne price. It is which offer produces the lowest reliable cost of cleaned parts at the required quality level, without creating avoidable disruption in machining, coating, assembly, maintenance, or compliance work. That distinction matters across metal fabrication, automotive components, general machinery, electronics-related operations, maintenance cleaning, and high-purity processing environments.
A sound comparison of metal cleaning chemicals wholesale offers begins with the operating problem. Procurement teams should define the soil, substrate, process stage, downstream requirement, and operating constraints before treating chemical quotations as directly comparable.
Start with the contamination and the downstream process
Metal cleaning is not one job. A lubricant-rich stamped steel component, a machined aluminum part carrying coolant residue, a stainless-steel vessel with heat-affected deposits, and a copper-based electronic component may all require different cleaning approaches. An offer that performs well on mineral oil may be weak against drawing compounds, polishing residues, carbonaceous soils, fingerprints, oxide films, or mixed contamination.
The next process step often determines what “clean enough” means. A part heading to powder coating or electroplating may need highly consistent wetting and minimal residual film. A component prepared for welding may need to avoid residues that affect joint quality. A maintenance application may tolerate some cosmetic variation but require fast oil removal and operator-friendly handling. In precision work, even trace residues, ionic contamination, or rinse-water carryover can be commercially significant.
Before comparing supplier proposals, evaluators should document the following:
- Metal substrates and alloys involved, including any mixed-metal assemblies.
- Primary soils, their loading level, and whether contamination changes by supplier, season, or production shift.
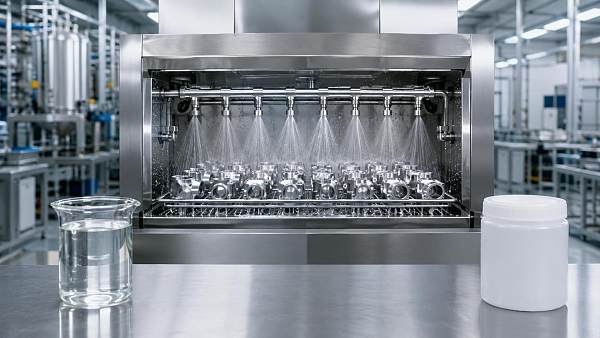
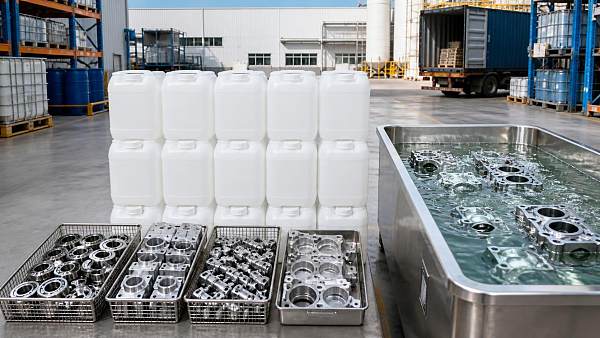
- Cleaning method: immersion, spray, ultrasonic, manual wipe, circulation, or a combined process.
- Operating temperature, contact time, agitation, water quality, and available rinse stages.
- Required surface condition before coating, assembly, inspection, storage, or shipment.
- Constraints involving foam, odor, worker exposure, wastewater treatment, equipment materials, and local compliance obligations.
This preparation prevents a common sourcing error: comparing a general-purpose cleaner with a formulation designed for a narrower, more demanding process and concluding that the latter is overpriced. The products may serve different risk profiles even when their headline descriptions are close.
Convert the quote into an in-use cost
Quoted price is a necessary starting point, but it is a poor final decision metric. A concentrated cleaner sold at a higher per-kilogram price can cost less in operation if it is used at a lower dilution, maintains performance longer, reduces reject rates, or limits rework. Conversely, a low-priced product may require frequent replenishment, aggressive operating conditions, more rinsing, or additional corrosion protection.
Procurement should ask every bidder to state the recommended operating concentration and conditions for the specified soil and substrate. If a supplier gives only a broad range, the evaluation team should request a test-based recommendation or treat the quote as preliminary.
Where production data exist, the most useful comparison is usually cost per accepted cleaned part, not cost per litre delivered. In lower-volume maintenance operations, cost per completed cleaning job may be more practical. The calculation does not need false precision; its purpose is to expose assumptions that a unit-price comparison hides.
Buyers should also separate one-time trial costs from recurring operating costs. A supplier may need to support bath conversion, line cleaning, operator training, or parameter adjustment. These costs can be justified where a new chemistry lowers continuing risk, but they should be visible in the business case.
Assess substrate compatibility before accepting broad claims
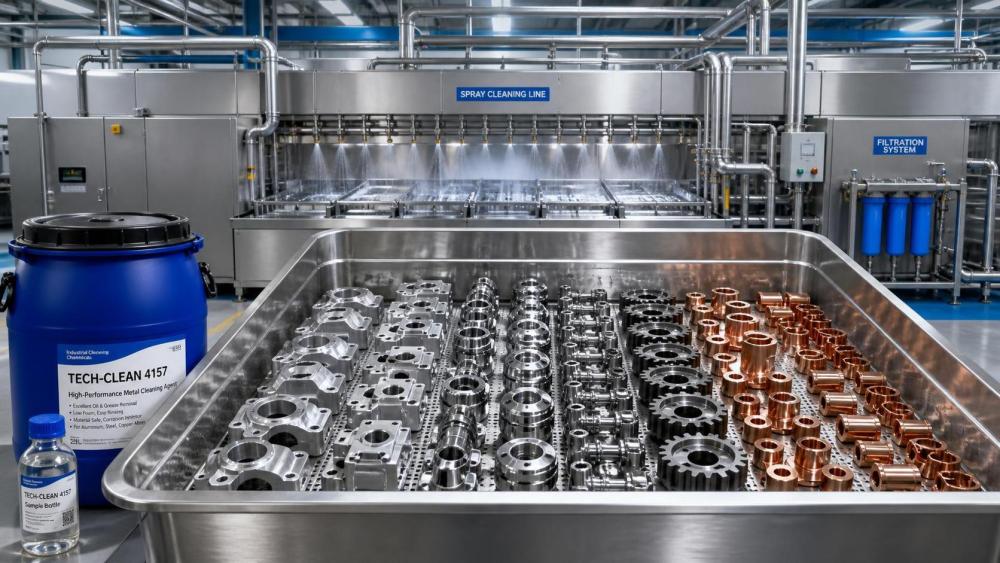
“Suitable for multiple metals” is useful marketing language but not a sufficient technical conclusion. Alkalinity, chelating agents, solvents, surfactant systems, inhibitors, and operating temperature can affect aluminum, zinc, galvanized steel, brass, copper, magnesium-containing alloys, and coated surfaces differently. A cleaner that removes oil effectively may etch a sensitive alloy, darken a surface, affect dimensional tolerances, or make later finishing less consistent.
For mixed-material parts, compatibility needs to be tested against the complete assembly rather than against isolated coupons only. Elastomers, seals, adhesives, plastics, painted elements, and marking inks can be exposed during cleaning. Equipment compatibility matters as well: pumps, spray nozzles, filtration systems, tanks, and seals may have limits under strong alkaline, acidic, solvent-containing, or high-temperature conditions.
Corrosion protection deserves separate attention. Some aqueous cleaners include temporary corrosion inhibitors, but the protection period depends on humidity, rinse quality, drying speed, packaging, handling, and storage conditions. A supplier statement that parts are “rust protected” should be translated into a defined expectation: for which metal, for how long, under what storage conditions, and after which cleaning parameters? Where surface appearance or interim storage matters, shop-floor validation is more reliable than a generic product claim.
Performance should be demonstrated under realistic line conditions
Laboratory beaker tests and supplier demonstrations are useful screens, not final proof. They may use fresh solutions, controlled soils, optimized temperature, and ideal contact time. Actual production lines introduce oil loading, metal fines, water hardness, variable dwell time, contamination carryover, inconsistent part orientation, and operator practices.
A practical trial should define a pass/fail standard in advance. Depending on the process, that may include visual cleanliness, water-break behavior, gravimetric residue, contact angle, coating adhesion, salt-spray performance, weld quality, particle counts, or a customer-specific inspection requirement. The selected measure should reflect the downstream risk rather than merely the easiest test to perform.
It is also important to observe how performance changes as the bath ages. A chemical can show excellent initial cleaning but lose control as oil accumulates or as the active components are depleted. Ask suppliers how they recommend monitoring bath condition: titration, conductivity, pH, refractometer readings, split tests, oil-load measurements, or laboratory analysis. The answer should be understandable to the operations team and workable at the site.
Questions that reveal a more complete offer
- What operating range is recommended for our soil and alloy combination?
- Which bath-control method will indicate when replenishment or change-out is needed?
- How does the formulation behave under high oil loading and metal-fine contamination?
- What defoaming strategy is required in spray or high-agitation systems?
- Can the product tolerate local water hardness, or is softened or deionized water needed?
- What evidence supports compatibility with our downstream coating, welding, bonding, or inspection step?
- What technical support is available during trial, conversion, and production troubleshooting?
These questions distinguish a chemical offer from a usable process proposal. They also give commercial teams a defensible basis for evaluating technical support rather than treating it as an informal promise.
Documentation is part of the supply, not an administrative extra
For wholesale chemical purchasing, incomplete documentation can turn a technically acceptable product into an operational liability. Safety data sheets, technical data sheets, certificates of analysis where relevant, transport classification, composition disclosures appropriate to the buyer’s requirements, and regulatory status information should be reviewed early.
Requirements vary by location and application. Buyers should verify the current obligations applicable to their jurisdiction, customer sector, and transport route rather than assume that a document package prepared for one market is sufficient for another. Specific regulatory conclusions, registrations, restricted-substance status, and labeling requirements should be confirmed with the supplier and, where necessary, internal regulatory specialists.
Documentation quality can also signal supplier discipline. Consistent revision control, clear product identifiers, realistic storage conditions, batch traceability, and unambiguous emergency information make it easier to manage an incident, customer audit, or cross-border shipment. A quote that omits these details may still be viable, but the missing information should be resolved before a long-term award.
Compare packaging, logistics, and inventory risk
Wholesale economics can deteriorate through logistics rather than chemistry. Drums, intermediate bulk containers, bulk tank deliveries, and smaller packs each change handling cost, inventory exposure, and contamination risk. The lowest freight cost per kilogram may come with inventory levels that exceed shelf-life comfort, storage capacity, or cash-flow limits.
Packaging must suit the product and site conditions. Strong cleaners, oxidizing materials, solvent-containing blends, and products sensitive to freezing or high heat may need specific storage controls. Confirm the net quantity, packaging material, seal arrangement, palletization, labeling, returnable-container terms where applicable, and damage claim process. For imported materials, clarify responsibility for customs documentation, dangerous-goods requirements, delivery terms, and delays at port or border.
Supply continuity is particularly important when cleaning chemistry is qualified with a downstream coating or customer approval process. A sudden formula change, batch inconsistency, or delivery interruption can create a production issue that cannot be solved by purchasing a nominally equivalent product from another source overnight. Evaluators should ask about manufacturing location, lead times, minimum order quantities, second-source arrangements, raw-material exposure, change-notification procedures, and retention samples.
There is a tradeoff here. Dual sourcing may reduce interruption risk, but qualification and inventory complexity rise when two formulations behave differently. In some operations, a primary supplier with a prequalified contingency product is more manageable than two interchangeable-looking offers with no controlled conversion plan.
Watch for claims that are directionally true but commercially incomplete
Several common statements deserve closer examination. “Concentrated” does not automatically mean lower cost; the required dilution and replenishment pattern matter. “Low foam” may be meaningful in a specific spray pressure and temperature range but not under all operating conditions. “Environmentally friendly” is too broad to guide procurement without information on ingredients, wastewater behavior, transport classification, worker handling, and local disposal rules.
Likewise, “non-corrosive” may refer to the supplied concentrate, a recommended working solution, one substrate, or a limited contact time. “No residue” depends on rinsing quality and drying. “Universal cleaner” may be valuable for maintenance simplification but may not meet the surface-control needs of precision coating or electronics-related work.
The commercial response is not to reject these claims. It is to turn each into a testable condition. What exactly is being claimed, at what concentration, on which material, and against which acceptance criterion? Suppliers able to answer that clearly are easier to manage over the life of the contract.
A structured award decision reduces avoidable rework
For a meaningful metal cleaning chemicals wholesale decision, business evaluators should score offers across more than price. A weighted model can include in-use cost, cleaning performance, substrate and downstream compatibility, bath manageability, safety and regulatory documentation, packaging and delivery reliability, technical support, and supplier-change controls. The weighting should reflect the cost of failure in the specific operation.
In a general maintenance environment, availability, ease of use, and total cleaning cost may dominate. In a coating line, rinseability and adhesion risk can outweigh a modest price difference. In a high-purity or electronics-related application, documentation, contamination control, and consistency may be decisive even when the initial chemical cost is higher.
The strongest purchasing decision is therefore usually made after a limited but disciplined production trial, supported by a clear total-cost model and an agreed supply specification. It gives procurement a commercial basis for negotiation while preserving the technical conditions that keep the cleaning process stable. That is where a wholesale offer becomes a dependable operating choice rather than simply the cheapest item on a price list.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+