How to Choose Electronic Cleaning Chemicals for Sensitive PCB and Semiconductor Lines
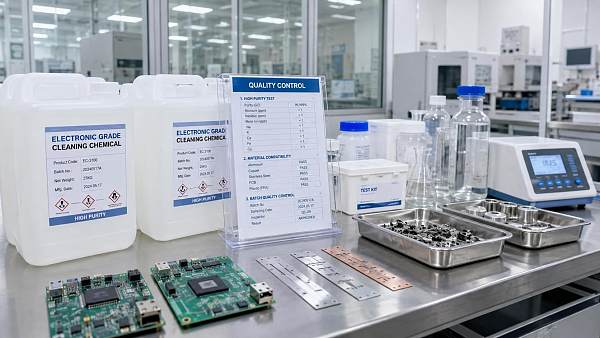
Choosing the right Electronic Cleaning Chemicals for sensitive PCB and semiconductor lines is less about finding the strongest cleaner and more about controlling what the cleaner leaves behind. In these environments, a chemistry can remove flux, oils, and particles perfectly on paper and still fail in production because it introduces ionic residue, attacks metals, swells polymers, or leaves process variability too wide for stable yield.
That is why technical evaluators usually need a decision framework, not a product list. The real question is whether a cleaning chemistry fits the board design, the contamination profile, the line architecture, the drying window, and the compliance constraints that surround modern electronics manufacturing.
What the cleaning step is really trying to protect
On PCB lines, cleaning is often tied to soldering residues, handling soils, and process chemicals. On semiconductor-related lines, the tolerance is much tighter: even trace contamination can affect adhesion, dielectric behavior, corrosion risk, or long-term reliability. In both cases, the purpose is not cosmetic cleanliness. It is process stability.
That changes how chemical selection should be judged. A formulation that strips residues quickly may still be a poor fit if it creates hidden risks later in assembly, encapsulation, testing, or field use. For sensitive lines, the important metric is not only removal efficiency but residual behavior after rinsing, evaporation, and drying.
Start with the contamination profile, not the chemistry family
The same Electronic Cleaning Chemicals do not perform equally across all soils. Evaluators should first identify what actually needs to be removed:
- Rosin and no-clean flux residues
- Fingerprints, skin oils, and assembly lubricants
- Particulates and dust
- Oxidized or baked-on organic films
- Metal-containing residues from soldering or machining
That matters because a cleaner optimized for one residue class may underperform on another, or require process conditions that are too harsh for fragile assemblies. For example, a solvent system that handles light organic soils well may not have enough wetting or solvency for aged flux. An aqueous cleaner may be excellent on particulate removal but create drying and compatibility issues on tight-pitch assemblies or moisture-sensitive packages.
The practical rule is simple: define the dominant contaminant first, then check whether the chemistry is actually matched to that soil under your temperature, time, and agitation limits.
Compatibility usually decides the outcome
Compatibility is where many cleaning programs fail quietly. A chemistry can pass a bench test and still create damage across a real line because the production environment contains mixed materials and mixed tolerances.
For PCB and semiconductor applications, look closely at:
- Metals: copper, aluminum, silver, gold, solder alloys, nickel finishes
- Polymers: solder masks, conformal coatings, adhesives, encapsulants, label materials
- Device structures: fine-pitch features, wire bonds, sensors, MEMS-related surfaces, high-density interconnects
- Downstream process steps: coating, bonding, potting, inspection, packaging
Residual chemistry can matter as much as direct attack. Some cleaners do not visibly damage a surface but still leave behind ions or surfactants that interfere with adhesion or accelerate corrosion under humidity. Others are safe on the substrate but too aggressive for printed legends, coatings, or elastomeric parts used elsewhere in the same line.
For sensitive lines, compatibility testing should include not only immediate appearance but also post-clean aging, humidity exposure, and any later thermal or mechanical stress the assembly will see.
Purity and residue control are not marketing terms
Technical evaluators should treat purity as a specification to interrogate, not a label to trust. In electronic cleaning, low residue is not just about how much material is left after drying. It is also about what kind of residue remains and whether it is mobile under field conditions.
Useful questions include:
- What is the ionic contamination profile after cleaning and drying?
- Are nonvolatile residues measured under conditions close to the actual process?
- Does the chemistry require a rinse, and if so, what water quality is assumed?
- How sensitive is performance to bath loading or contamination buildup?
In semiconductor-adjacent work, the margin is especially narrow. A chemistry that performs acceptably in a lower-risk electronics line may not be acceptable where ultra-low ionic residues, particle control, and repeatability are essential. If the supplier cannot explain residue behavior in a way that matches your process, the product is not yet qualified for your application.
Drying and rinse behavior often make or break the line
Cleaning does not end when the contaminant is detached. The material must also leave the surface in a controlled way. That means the evaluator needs to understand evaporation rate, rinse compatibility, foam tendency, water miscibility, and drying load.
Some common failure modes are predictable:
- Fast evaporation that leaves redeposited residue at edges and under components
- Slow drying that traps moisture in tight geometries
- Excess foaming that disrupts spray or ultrasonic action
- Poor rinsability that leaves surfactant films behind
If a line uses fine pitch assemblies, blind vias, under-component spaces, or tight packaging geometries, drying behavior becomes a process variable, not a housekeeping detail. The best chemistry on paper can still be operationally weak if the drying window is too long or too sensitive to ambient change.
Process method matters as much as formulation
The right cleaner in the wrong process is still the wrong answer. Ultrasonic, spray, immersion, wipe, vapor, and batch systems all stress the chemistry differently. A formulation that works well in immersion may behave differently in spray equipment because of wetting, aerosol formation, or foaming. Likewise, a chemistry intended for bench cleaning may not be robust enough for high-throughput automated lines.
Evaluators should verify:
- Operating temperature range
- Exposure time sensitivity
- Agitation or ultrasonic compatibility
- Filterability and bath life
- Compatibility with inline monitoring or replenishment routines
For semiconductor-sensitive environments, consistency over time matters more than peak performance in a fresh bath. A cleaner that degrades slowly in use, absorbs contaminants predictably, and can be controlled tightly is usually more valuable than one that looks aggressive in the first hour and unstable afterward.
Compliance is now part of the technical spec
For industrial buyers, compliance is no longer separate from performance. Environmental rules, worker exposure limits, waste handling requirements, and restricted substances lists all affect what can be deployed and sustained in production.
That is especially true where global sourcing, export programs, or multinational manufacturing sites are involved. A chemistry may work technically but still create headaches if it is difficult to approve under internal EHS rules or if its ingredient profile complicates documentation, transport, or disposal. For some operations, solvent choice also affects insurance, ventilation design, and storage cost.
Do not assume a cleaner that is “electronics safe” is automatically suitable for your facility. Ask for the full picture: hazard classification, SDS consistency, residue data, process compatibility, and any known restrictions under current environmental or customer-specific requirements. Where claims are unclear, treat them as provisional until verified.
What to compare in supplier claims
Supplier datasheets are useful, but they are not enough. In sensitive applications, evaluators should compare claims against test conditions, not headlines.
The strongest short list usually contains cleaners that are not just effective, but testable, monitorable, and easy to keep within spec across shifts and sites.
How to run a practical selection process
A disciplined selection process usually works better than broad vendor comparison. For most technical teams, the sequence should look like this:
- Define the contamination class and the failure mode you are trying to prevent
- List all exposed materials and downstream process steps
- Set residue, drying, and compatibility thresholds before testing
- Run side-by-side trials under production-like conditions
- Inspect not only immediate cleanliness but also aging, adhesion, and corrosion outcomes
- Check whether bath maintenance and supply chain control are realistic at scale
This approach reduces the common mistake of choosing a chemistry that looks strong in lab cleaning tests but becomes fragile in real operations. In electronics manufacturing, process fit often matters more than maximum cleaning power.
The hidden tradeoff is usually between aggressiveness and control
For sensitive PCB and semiconductor lines, every cleaning choice sits on a tradeoff curve. Stronger chemistry can shorten cycle time and loosen mechanical cleaning demands, but it may also increase compatibility risk, drying burden, or compliance friction. Milder chemistry can be easier to approve and safer on materials, but only if the process has enough time, temperature, and mechanical support to achieve the needed cleanliness.
The best choice is rarely the most aggressive product in the catalog. It is the one that holds performance within a narrow band, across the real mix of soils, materials, and process windows your line actually runs.
That is the standard technical evaluators should use. If a candidate cleaner cannot demonstrate repeatable residue control, material compatibility, and operational consistency under your conditions, it is not ready for sensitive electronics work, no matter how clean the brochure sounds.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+