How Semiconductor Cleaners for Post CMP Cleaning Prevent Defects
Why Post-CMP Cleaning Is a Yield-Control Issue, Not a Final Rinse
Chemical mechanical planarization is essential to creating the flat surfaces required for advanced semiconductor structures, but it also leaves behind a difficult mixture of abrasive particles, slurry components, oxidizers, corrosion inhibitors, dissolved metals, and organic residues. These materials may be present at very low levels, yet low-level contamination can still translate into particle defects, electrical leakage, corrosion, poor film adhesion, or downstream lithography failures.
For quality control and safety professionals, the key question is not simply whether a wafer appears clean after polishing. The practical question is whether the post-CMP cleaning step consistently removes process residues without changing the surface chemistry, attacking exposed films, creating new contaminants, or increasing environmental and operator-handling risk.
Semiconductor cleaners for post CMP cleaning are therefore part of the process-control system. Their role is to separate unwanted residues from increasingly sensitive wafer surfaces while maintaining compatibility with the films, device geometry, water-quality system, equipment materials, and waste-treatment infrastructure already in place. A cleaner that performs well in a laboratory particle-count test may still be unsuitable in production if it causes metal corrosion, foam-related tool instability, filter loading, cross-contamination, or inconsistent results across batches.
The industry often describes post-CMP cleaning as a residue-removal problem. In practice, it is a defect-prevention, materials-compatibility, and process-safety problem at the same time.
What Actually Remains on the Wafer After CMP?
The residue profile depends on the polishing application. Oxide, tungsten, copper, barrier-layer, and dielectric CMP processes use different slurry systems and present different cleaning challenges. A post-CMP cleaning formulation must be evaluated against the actual residue rather than against a generic definition of “slurry removal.”
Typical contaminants can include colloidal silica, alumina, ceria, or other abrasive particles; metal ions from the film or polishing environment; oxidizer residues; complexing agents; surfactants; polymeric dispersants; pad debris; and fragments released from filters, piping, brushes, or tool components. Some residues are physically attached to the surface. Others are chemically adsorbed, trapped in recessed features, or redeposited during rinsing and drying.
As feature sizes decrease and material stacks become more complex, the location of contamination matters as much as the total quantity. A particle in an open field may be detected and removed without affecting function. A smaller particle or metallic residue at a line edge, via, trench, or high-aspect-ratio feature can become a yield-limiting defect. This is why visual inspection alone is insufficient as an acceptance criterion.
Quality teams should also avoid treating all particles as equivalent. A cleaner may remove bulk abrasive particles effectively but leave trace metals, organic films, or chemically modified residues behind. Conversely, a highly aggressive chemistry may lower particle counts while introducing corrosion pits or changes in surface roughness. The best result is not the strongest cleaning action. It is controlled removal with no unacceptable surface damage.
How Cleaning Chemistry Prevents Defects
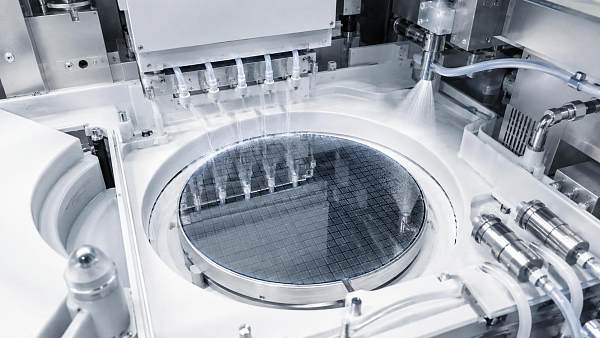
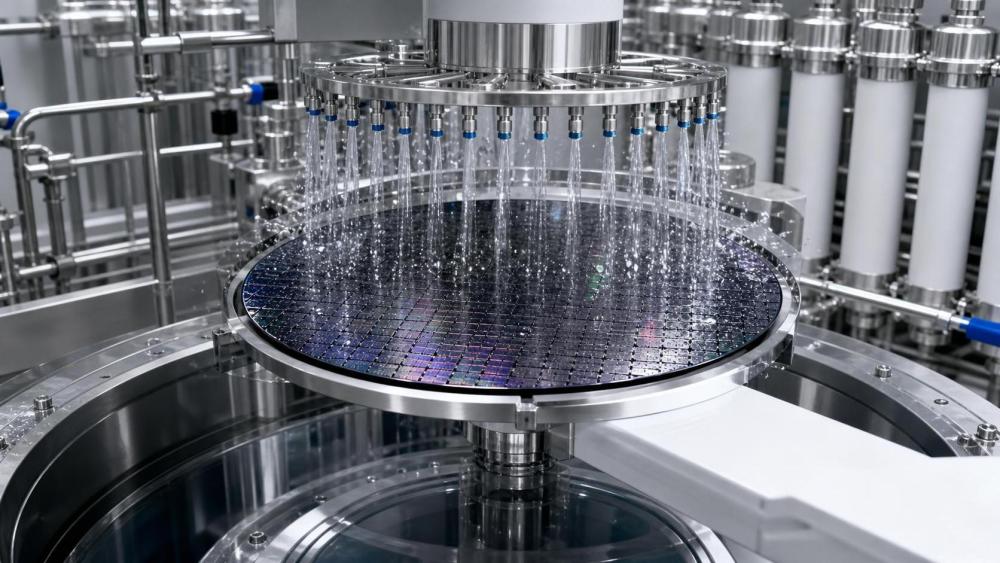
Post-CMP cleaners typically rely on a balance of several functions: wetting the wafer surface, loosening adhered particles, complexing or solubilizing metallic residues, dispersing removed materials so they do not redeposit, controlling electrostatic interactions, and supporting efficient rinsing. Depending on the process, formulations may use acids, bases, chelating agents, oxidizing or reducing components, corrosion inhibitors, surfactants, and high-purity water-compatible additives.
That balance is important because the cleaner interacts with both the contaminant and the exposed device surface. For example, a chemistry designed to lift metal-containing residue may need strong complexation, but the same chemical environment could alter copper, cobalt, tungsten, ruthenium, barrier layers, or dielectric films if concentration, temperature, or contact time moves outside the qualified window.
Particle removal is often influenced by surface charge and wetting behavior. Abrasive particles can adhere through electrostatic attraction, mechanical trapping, or interactions with adsorbed organic material. A well-designed cleaner can modify these interactions and keep the released particles dispersed in the liquid phase until they are removed through rinsing. Poor dispersion control creates a familiar production problem: residues are detached in one area and redeposited elsewhere on the wafer or inside the cleaning tool.
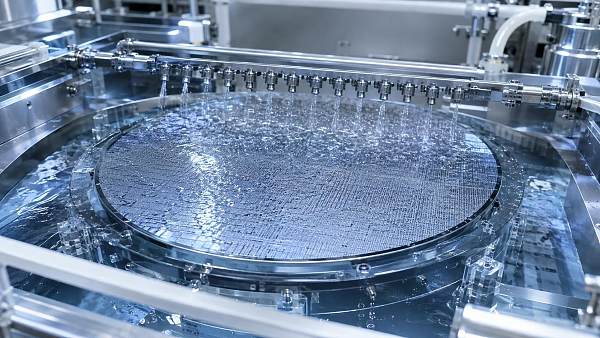
Rinse performance is equally important. Some formulations remove contaminants effectively but require extensive rinsing to prevent cleaner residues from remaining on the surface. If rinse capacity, water quality, nozzle coverage, flow distribution, or drying conditions are inadequate, the apparent cleaning benefit can be lost. The final wafer condition reflects the entire sequence, not the chemical step in isolation.
The Main Failure Modes to Investigate
When post-CMP defects rise, changing the cleaner concentration is an understandable first reaction, but it is often too narrow. A defect signature may originate from slurry drift, brush wear, water contamination, filter breakthrough, equipment dead zones, chemical aging, or a mismatch between the cleaning formulation and a changed upstream material stack.
The following failure modes deserve structured investigation:
- Particle persistence: abrasive residues remain attached because the chemistry does not adequately wet, disperse, or detach them under actual tool conditions.
- Particle redeposition: removed contaminants are not kept suspended or are carried back onto the wafer during recirculation, inadequate rinse flow, or drying.
- Metal contamination: dissolved or particulate metals remain after CMP, migrate through the cleaning sequence, or are introduced through chemical, water, hardware, or handling sources.
- Galvanic or chemical corrosion: a cleaner interacts with exposed conductive materials and causes recess, pitting, discoloration, electrical variation, or barrier damage.
- Organic residue carryover: surfactants, polymers, pad fragments, and slurry additives are incompletely removed and interfere with later deposition, lithography, or bonding steps.
- Process-window drift: nominally qualified chemistry produces different results because dilution accuracy, bath age, temperature, filtration, flow rate, or wafer loading has changed.
- Cross-contamination: residues from one CMP module, product family, or material stack affect another process route through shared tools, carriers, chemicals, or rinse systems.
A useful investigation begins with the defect mechanism, not with the cleaner supplier or a single process variable. QC teams should compare defect maps, particle size distribution, elemental analysis where available, film-loss data, electrical test results, cleaner lot records, slurry lots, tool maintenance history, and water-system status. The objective is to distinguish correlation from cause.
Selection Criteria That Matter in Production
Procurement decisions often begin with purity specifications and price, but post-CMP applications need a broader qualification framework. High purity is necessary, yet it does not prove that the formulation is compatible with a specific wafer stack or cleaning tool. Likewise, a product that has been successful in one fab environment may not transfer directly to another because slurry chemistry, device architecture, equipment design, and rinse configuration differ.
For high-purity chemical applications, a certificate of analysis should be treated as one input rather than the entire qualification package. Teams should define which impurities are relevant to their device and process flow, how the supplier controls them, what analytical methods are used, and whether the reporting limits are meaningful for the fab’s contamination budget. A reported “below detection limit” result is only useful when the detection limit itself is appropriate.
Common Assumptions That Can Create Risk
One common assumption is that a more aggressive cleaner will always provide lower defectivity. This is not reliable. Stronger acidity, alkalinity, oxidizing power, or chelation may improve removal of one residue class while increasing attack on sensitive materials. In advanced structures, a modest increase in film loss or localized corrosion can be more damaging than a visible particle count.
Another assumption is that cleaner performance can be validated with blanket wafers alone. Blanket-wafer studies are valuable for understanding film compatibility and gross contamination behavior, but patterned wafers reveal different risks. Pattern density, feature geometry, exposed interfaces, capillary effects, and local galvanic conditions can change how residues are retained and how the chemistry behaves.
It is also risky to assume that changing a chemical supplier is only a purchasing decision. Even where nominal composition and basic specifications appear similar, trace impurities, stabilizer systems, packaging materials, filtration practices, and manufacturing controls can affect results. Supplier changes should follow a documented change-control process with fit-for-purpose testing, not only paperwork comparison.
Finally, teams should not assume that post-CMP cleaning can compensate indefinitely for an unstable CMP step. Cleaning chemistry has limits. If slurry particle size has shifted, pad conditioning has deteriorated, downforce is inconsistent, or endpoint control is unstable, downstream cleaning may reduce symptoms without resolving the source of variation.
Building a Practical Qualification and Control Plan
A robust approach starts by defining the defect and contamination risks associated with each CMP-clean sequence. This should include the material stack, slurry type, expected residue classes, sensitive downstream operations, and acceptable limits for particle counts, metallic contamination, film loss, and electrical impact. Limits should reflect device risk, not simply historical averages.
During cleaner qualification, it is useful to evaluate normal operating conditions as well as credible excursions. Testing can include lower and higher concentration boundaries, temperature variation, extended contact time, aged chemistry, maximum wafer loading, delayed rinse conditions, and representative tool idle periods. These studies identify whether a formulation has a forgiving process window or only performs under tightly controlled laboratory conditions.
For ongoing control, quality teams should connect chemical management with tool and metrology data. Relevant controls may include incoming chemical verification, lot traceability, dilution records, bath-life limits, point-of-use filtration monitoring, water-quality checks, process temperature, nozzle or brush maintenance, defect inspection trends, and periodic surface analysis. The right control frequency depends on process criticality and historical stability; it should be justified by risk rather than applied uniformly across every cleaning step.
Documentation matters particularly when a site manages multiple fabs, outsourced operations, or a changing supplier base. A clear record of formulation identity, material safety information, approved packaging, storage limits, change notification requirements, sampling methods, and escalation criteria reduces the chance that a supply-chain change becomes an unexplained yield event months later.
Safety and Environmental Controls Are Part of Process Quality
Post-CMP chemistries may involve corrosive, reactive, toxic, or metal-binding components. Even when a product is designed for lower hazard or improved environmental handling, site-specific risk assessment remains necessary. Concentrated chemical delivery, manual connection points, drum or tote handling, leaks, incompatible cleaning agents, and wastewater interactions deserve attention alongside wafer performance.
Safety managers should review the full use cycle: receiving, storage, transfer, dilution, point-of-use delivery, maintenance, spill response, waste segregation, and disposal. The relevant safety data sheet provides a starting point, but it cannot replace evaluation of local equipment materials, ventilation, secondary containment, emergency equipment, and operator exposure routes.
Waste streams can be especially complex because they may contain abrasive particles, dissolved metals, oxidizers, chelating agents, and residual surfactants. A cleaner that improves wafer cleaning may alter metal precipitation behavior or interfere with existing treatment chemistry. Any change in cleaning formulation, concentration, or consumption rate should therefore be reviewed with environmental health and wastewater teams before full deployment. Local discharge requirements and reporting obligations should be verified for the specific site.
What to Watch as Semiconductor Cleaning Requirements Evolve
The direction of travel is clear even though each device generation has its own process details: semiconductor cleaning is becoming more selective, more tightly monitored, and more closely linked to upstream and downstream process integration. New materials, advanced packaging, heterogeneous integration, and increasingly complex interconnect structures place more pressure on post-CMP cleaning to remove residues without damaging interfaces that may be chemically or mechanically fragile.
This will increase demand for cleaner chemistries with lower metal backgrounds, more predictable rinse behavior, stronger material selectivity, and better compatibility with automated chemical-delivery systems. It will also make supplier documentation and change control more important. A formulation cannot be judged solely by a specification sheet; its value lies in how consistently it supports the qualified process over time.
For QC and safety leaders, the most productive next step is usually to map the current post-CMP sequence against actual defect modes, material vulnerabilities, chemical controls, and waste-handling constraints. That exercise often reveals whether the priority is a new semiconductor cleaner, tighter concentration control, improved rinsing, better contamination monitoring, or correction of an upstream CMP instability. The cleaner is important, but defect prevention depends on managing the complete system around it.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+