How Precision Cleaning Agents Protect Semiconductor Yield and Reliability
A wafer clean can appear successful while still creating the conditions for yield loss later in the line. A surface may look visually clear, yet retain trace metals, organic film, particles lodged in high-aspect-ratio features, or residues from the cleaner itself. These contaminants can interfere with deposition, lithography, etch uniformity, bonding, electrical testing, and long-term device behavior.
The practical answer is not simply to select the highest-purity chemistry available. Precision cleaning agents for semiconductors protect yield and reliability when their removal mechanism, impurity profile, material compatibility, and rinse behavior match the contamination and process stage. Technical evaluation should therefore focus on what remains after cleaning, what the chemistry may attack or alter, and how consistently the process performs across normal production variation.
Why a “clean-looking” wafer may still be at risk
Semiconductor surfaces are sensitive to contamination at levels that ordinary industrial cleaning logic does not address. The concern is not limited to visible particles. A cleaning sequence can leave ionic residues, organic traces, metallic contaminants, dissolved material that redeposits during drying, or surface changes that become apparent only after a downstream process.
For example, an organic residue may reduce photoresist adhesion or contribute to pattern defects. Metal ions can affect electrical properties, create leakage pathways, or become embedded during thermal processing. Particle contamination can cause local pattern failure, while inadequate rinsing may leave a residue that changes surface energy and disrupts later coating or bonding steps.
These risks become harder to manage when device geometries shrink, films become thinner, and structures become more complex. A formulation that performs adequately on an open, robust surface may not remove contaminants effectively from trenches, vias, or patterned areas. It may also be unsuitable for delicate metal stacks, dielectric layers, barrier films, or mixed-material assemblies.
Start with the contamination event, not the cleaner category
When evaluating a cleaning agent, the first question should be: what must be removed, from which surface, and before which downstream operation? A product selected only because it is described as a solvent, surfactant, degreaser, acidic cleaner, or alkaline cleaner may be poorly matched to the actual defect mechanism.
A useful investigation separates contaminants into functional groups:
- Particles: abrasive debris, polishing residues, airborne particles, filter shedding, handling contamination, or process by-products.
- Organic residues: photoresist remnants, polymerized etch residues, oils, fingerprints, adhesive traces, lubricants, and solvent-borne films.
- Inorganic and metallic contamination: metal ions, oxides, salts, slurry components, corrosion products, and residues from previous wet processes.
- Process chemical carryover: residues from developers, etchants, strippers, plating chemistries, CMP slurries, or rinse stages.
- Water-related contamination: minerals, dissolved gases, ionic species, microbial by-products in poorly controlled systems, or particles introduced through distribution equipment.
The same surface can carry more than one type. A polymer film may trap particles, while metallic residues may be associated with a reaction layer beneath the film. In such cases, a single cleaning chemistry may not be enough. The order of removal matters because an aggressive first step can harden residue, redeposit loosened material, or expose a sensitive layer before the surface is ready.
Match the cleaning mechanism to the process limitation
Precision cleaning is often discussed as a chemical selection exercise, but the cleaning mechanism includes chemistry, wetting, contact time, temperature, agitation, rinsing, and drying. A chemistry that dissolves a residue in a laboratory beaker may still underperform on a patterned wafer if it cannot wet narrow features, displace trapped air, or carry dissolved contaminants away from the surface.
Removing organic films without creating a new residue problem
Organic residues vary widely. Some dissolve readily in compatible solvents; others are cross-linked, thermally altered, plasma-modified, or mixed with inorganic by-products. The relevant questions are whether the cleaning agent can penetrate the residue, break its attachment to the surface, and keep the removed material dispersed until it is rinsed away.
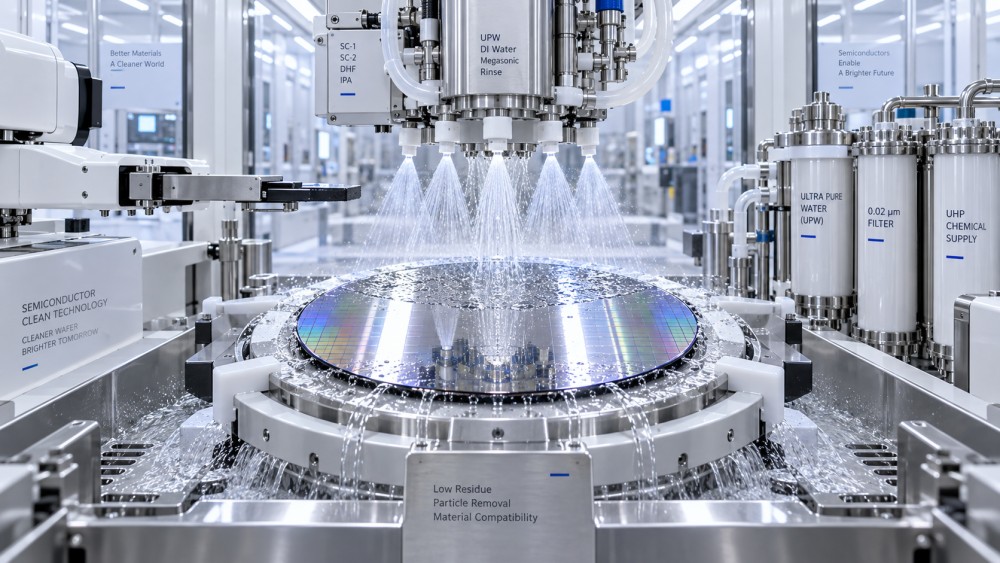
Surfactant-containing systems can improve wetting and soil lift, especially where residues are uneven or strongly adhered. However, their use requires careful rinse evaluation. A surfactant that helps detach contamination but leaves adsorbed material on a hydrophilic surface can create downstream variability. Low-residue behavior is therefore not a marketing phrase; it must be considered as part of the complete wash-rinse-dry sequence.
Controlling particles is different from dissolving contamination
Particles generally need to be detached, suspended, and removed before they settle again. Surface tension, flow pattern, mechanical energy, filtration, bath turnover, and particle loading all influence success. A cleaner may be chemically appropriate but unable to remove particles effectively if the process has poor circulation or insufficient control of bath contamination.
Particle redeposition is a frequent blind spot. Once particles are released, they must remain dispersed long enough to be flushed from the system. This is why fluid management, rinse quality, and filtration cannot be assessed separately from the cleaning chemistry. A low particle count at chemical make-up does not guarantee low particle exposure after the bath has been in use.
Metal removal requires selectivity
Removing metallic contamination often depends on complexation, oxidation state control, pH, and the condition of the substrate. The challenge is to remove unwanted metals without etching, staining, corroding, or roughening the functional layer. This becomes especially important where copper, aluminum, nickel, cobalt, tungsten, or other process-sensitive materials may be present.
A chemistry that removes metal ions efficiently from one surface can damage another material in the same assembly. Evaluation should therefore include exposed films, interfaces, and edge regions rather than testing only an ideal blanket coupon. Mixed surfaces can behave differently because galvanic effects, trapped chemistry, and local differences in surface energy alter the response.
Material compatibility is a yield-control requirement
Cleaning agents are expected to remove unwanted material while preserving the intended surface. That expectation sounds simple, but compatibility must be evaluated beyond obvious etching or visible discoloration. Subtle changes in roughness, oxide condition, contact angle, film thickness, adhesion, or electrical behavior may create defects only after later processing.
Technical teams should identify the materials that can be exposed during the cleaning window, including base substrates, deposited films, barrier layers, passivation materials, photoresist remnants, sealants, adhesives, and packaging-related materials where applicable. The exposure conditions also matter. A short immersion at ambient temperature may be acceptable, while extended recirculation, elevated temperature, ultrasonic energy, or repeated cycles may not be.
Compatibility testing should reflect the real process sequence whenever possible. Testing a chemistry only before a critical film is deposited does not answer whether it is safe after etch, CMP, metallization, or patterning. The cleaning step has to be judged in its actual location in the flow.
Purity specifications matter, but they do not tell the whole story
High purity is essential for semiconductor-related applications, yet a purity statement alone cannot establish process suitability. Technical evaluators need to understand which impurities are controlled, how consistently they are controlled between batches, and whether the analytical approach is relevant to the defect risk.
Trace metals, anions, nonvolatile residues, particles, moisture, and organic extractables may each matter differently depending on the application. A solvent used before a sensitive deposition step may require attention to nonvolatile residue and water content. A water-based cleaning formulation may require strict control of ionic contamination and particle generation. Materials used in recirculated systems should also be assessed for changes during use, not only at initial delivery.
Documentation should support a meaningful review of incoming quality and process risk. Batch-level consistency, storage guidance, packaging compatibility, filtration practices, and handling requirements can be as important as the nominal chemical specification. Packaging that introduces extractables, a transfer system with unsuitable seals, or an uncontrolled point-of-use filter can undermine the benefit of a well-selected cleaning agent.
The rinse step determines whether cleaning is complete
A cleaning agent is not fully effective until it and the removed contaminants are cleared from the surface. This is particularly important with formulations designed to wet effectively, emulsify oils, complex metals, or disperse particles. Their functional components must not remain in patterns, recesses, or drying marks.
Rinse performance depends on water quality, flow direction, exchange rate, temperature, feature geometry, and the tendency of the chemistry to cling to the surface. A weak rinse can convert a removal problem into a carryover problem. In practical troubleshooting, defects that appear after a cleaning change may be caused by insufficient rinsing rather than inadequate cleaning power.
Drying should be evaluated as part of the same system. Water marks, residue rings, and localized deposits can arise when dissolved materials concentrate during evaporation. Surface condition, drying method, and drain behavior may affect whether the final wafer is truly residue-free. A process that produces acceptable results at low loading can behave differently when throughput, bath age, or carryover increases.
A practical path for screening candidate chemistries
Early-stage screening is more useful when it is designed around a known failure mode rather than a broad comparison of product descriptions. Define the surface, contaminant, process equipment, and downstream sensitivity before choosing test conditions. The goal is to identify acceptable operating windows and eliminate options that create obvious compatibility or rinse risks.
- Define the starting condition. Record the suspected residue, surface materials, prior process exposure, and where defects are observed. Separate confirmed facts from assumptions.
- Set the non-negotiable limits. These may include prohibited materials, maximum exposure temperature, time limits, restrictions on metal attack, or required rinse conditions.
- Compare cleaning mechanisms. Determine whether dissolution, emulsification, particle dispersion, oxidation, complexation, or a staged sequence is needed.
- Test the complete sequence. Include wash, agitation or flow conditions, rinsing, and drying. Do not judge a cleaner solely from its performance before rinse.
- Inspect both removal and preservation. Check for remaining contaminants as well as surface change, corrosion signs, deposits, altered wetting, or downstream process effects.
- Challenge the operating window. Review reasonable variation in concentration, temperature, contact time, loading, and bath age to identify sensitivity before transfer to routine use.
A candidate should not be considered robust simply because it works under one narrow condition. Semiconductor yield protection depends on repeatability. A chemistry that requires unusually tight timing, perfect rinsing, or constant manual adjustment may introduce more process risk than a slightly less aggressive option with a wider stable operating window.
When defects persist after a cleaning change
When contamination-related defects remain after introducing a new chemistry, it is tempting to increase concentration or extend contact time. That may help in some cases, but it can also increase attack on sensitive films, raise carryover, or make removal of the cleaner itself more difficult. The better response is to determine whether the failure is due to insufficient chemistry, poor access, redeposition, contaminated equipment, inadequate rinse, or a defect source upstream of the cleaning step.
Inspect the full fluid path: chemical storage, transfer lines, pumps, valves, filters, tanks, nozzles, and rinse delivery. A compatible cleaning agent cannot compensate for particles shed by degraded components, contamination accumulated in dead legs, or incompatible wetted materials. Likewise, an apparent cleaning defect may originate from upstream residue that has been altered by heat or plasma exposure and is no longer removable by the original method.
For sensitive device structures or processes with mixed exposed materials, changes should be confirmed through controlled engineering evaluation before broader implementation. The relevant decision is not whether the agent cleans aggressively; it is whether it removes the targeted contamination reliably while leaving the wafer in the required condition for the next critical operation.
Related News
 Antioxidants & Natural PreservativesWhat Quality Checks Matter When Sourcing Butylparaben for Personal CareButylparaben for personal care sourcing guide: compare assay, impurities, physical performance, documentation, traceability, and supplier quality to reduce formulation risk.MORE+
 Nano-microcapsule FormulationsHow Encapsulated Flavors Protect Taste During Processing and StorageEncapsulated Flavors protect taste from heat, oxygen, moisture, and storage loss. Explore smarter release, carrier selection, and processing strategies.MORE+
 Chelated Trace Element FertilizersHow Greenhouse Fertigation Systems Reduce Water and Fertilizer WasteGreenhouse fertigation systems reduce water and fertilizer waste with precise dosing, uniform irrigation, drainage monitoring, and smarter crop-zone control. Learn practical strategies.MORE+
 Supercritical CO2 Essential OilsHow Natural Essential Oil Blends Improve Consistent Product FragranceNatural essential oil blends help brands achieve consistent, appealing fragrance across batches. Explore smart blend design, stability testing, and product compatibility strategies.MORE+
 Non-ionic Surfactants & DefoamersHow to Choose Non Ionic Low Foaming Surfactants for CIP CleaningNon ionic low foaming surfactants for CIP cleaning: learn how to balance wetting, foam control, compatibility, and rinseability for reliable cleaning performance.MORE+
 Nano-microcapsule FormulationsHow Food Grade Cyclodextrin Complexes Protect Sensitive FlavorsFood grade cyclodextrin inclusion complexes help protect sensitive flavors from oxidation, evaporation, and processing loss while supporting controlled release and consistent sensory quality.MORE+
 Polymer-Coated Water Soluble NPKHow Fertilizer Coating Polymers Improve NPK Granule ReleaseFertilizer coating polymers for NPK granules improve controlled nutrient release, reduce loss risks, and enhance product consistency. Discover key selection and process insights.MORE+
 Chelated Trace Element FertilizersWhat Diammonium Phosphate Means for Crop Nutrition PlanningDiammonium Phosphate: learn how DAP supports early phosphorus access, nitrogen budgeting, smart placement, and balanced crop nutrition planning.MORE+
 Maillard Reaction Savory FlavorsHow to Assess a Flavor Bases Supplier List for Reliable SourcingGlobal Fine Chemicals & Agrochemical Intelligence Network flavor bases supplier list: assess specs, samples, supply risk, and true cost to source with confidence.MORE+
 Hydrocolloids & EmulsifiersHow Konjac Gum Powder Improves Texture in Low-Calorie FoodsKonjac gum powder improves body, stability, and mouthfeel in low-calorie foods. Discover practical tips for smoother sauces, beverages, and reduced-fat formulations.MORE+
 Supercritical CO2 Essential OilsWhat to Check Before Choosing a Botanical Essential Oils ManufacturerChoose a botanical essential oils manufacturer with confidence. Explore key checks for purity, traceability, compliance, batch consistency, and reliable supply.MORE+
 Microencapsulated FragrancesHow Fragrance Carriers for Detergents Improve Scent PerformanceFragrance carriers for detergents improve stability, fabric deposition, and long-lasting scent. Explore practical solutions for better wash-to-wear fragrance performance.MORE+
 Antioxidants & Natural PreservativesWhen Propyl Gallate Antioxidant Is the Right Choice for Oil StabilityPropyl gallate antioxidant: learn when it is the right choice for oil stability, shelf-life protection, processing compatibility, and smarter formulation decisions.MORE+
 Antioxidants & Natural PreservativesHow Potassium Sorbate Extends Shelf Life in Food and Beverage ProductsPotassium Sorbate helps food and beverage brands control yeast and mold spoilage. Explore pH, dosage, processing, and packaging strategies for reliable shelf life.MORE+
 Antioxidants & Natural PreservativesHow to Source Bulk Herbal Extracts With Reliable Quality ControlBulk herbal extracts sourcing guide: compare suppliers, verify traceability, review CoAs, and build reliable quality controls for safer, consistent purchasing.MORE+
 Antioxidants & Natural PreservativesWhat to Check Before Sourcing Butylparaben for Personal Care FormulasButylparaben for personal care sourcing guide: check market eligibility, purity, supplier controls, formula compatibility, packaging, and total risk before buying.MORE+
 Targeted Bio-pesticides & APIsChoosing Microbial Fungicides for Foliar Diseases in Integrated Crop ProgramsMicrobial fungicides for foliar diseases: learn how to match biology, formulation, tank compatibility, and timing for stronger integrated crop protection.MORE+
 Targeted Bio-pesticides & APIsHow Microbial Insecticides Control Caterpillars With Lower Crop Residue RiskMicrobial insecticides for caterpillars help protect crops with targeted early-larval control and lower residue-management pressure. Learn timing, coverage, compliance, and scouting essentials.MORE+
 Microencapsulated FragrancesHow to Add Encapsulated Laundry Fragrances Without Weakening Wash ResultsEncapsulated laundry fragrances: learn how to boost long-lasting scent while protecting cleaning power, stability, foam control, and fabric care.MORE+
 Supercritical CO2 Essential OilsHow Aroma Ingredients Shape Lasting and Skin-Safe Personal Care ProductsAroma ingredients for personal care: discover how to achieve lasting scent, formulation stability, skin safety, and confident product performance.MORE+
 Targeted Bio-pesticides & APIsInsecticides Explained Through Labels, Active Ingredients, and SafetyInsecticides explained through labels, active ingredients, formulations, and safety. Learn how to compare products, manage risk, and make informed crop protection decisions.MORE+
 Heavy-duty Industrial DegreasersHow to Select Parts Wash Cleaners for Automotive ComponentsParts wash cleaners for automotive components: learn how to match chemistry, materials, rinsing, safety, and waste controls for reliable cleaning results.MORE+
 Chelated Trace Element FertilizersHow Precision Fertigation Systems Improve Water and Nutrient ControlPrecision fertigation systems improve water and nutrient control with accurate dosing, uniform irrigation, smart monitoring, and reduced waste. Discover how to optimize crop performance.MORE+
 Hydrocolloids & EmulsifiersHow Bulk Price Factors Affect Hydrocolloid Stabilizer Blend SourcingHydrocolloid stabilizer blends bulk price: compare dosage efficiency, quality consistency, logistics, and documentation to reduce total sourcing costs.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow to Choose a Natural Sweeteners Supplier for Clean-Label ProductsNatural sweeteners supplier selection guide for clean-label products: compare formulation fit, traceability, documentation, and supply reliability.MORE+
 Non-ionic Surfactants & DefoamersWhat Cationic Surfactants Do and Where They Are UsedCationic Surfactants deliver antimicrobial action, conditioning, antistatic control, and surface treatment benefits. Explore key uses, compatibility, and safe selection tips.MORE+
 Targeted Bio-pesticides & APIsHow to Evaluate Pesticide Suspension Concentrates for Field StabilityPesticide Suspension Concentrates: learn how to evaluate field stability, redispersibility, dilution, tank-mix compatibility, and spray safety for reliable performance.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Systems for Meat Products Improve Texture and YieldHydrocolloid systems for meat products improve yield, texture, water retention, and slicing quality. Explore practical formulation strategies for stable, high-performing meat products.MORE+
 Microencapsulated FragrancesHow Laundry Fragrances for Liquid Detergents Improve Scent LongevityLaundry fragrances for liquid detergents: discover how fragrance design, deposition, and encapsulation create lasting fabric freshness and stronger product appeal.MORE+
 Nano-microcapsule FormulationsChoosing Fragrance Preparations That Perform Well in Personal WashFragrance preparations for personal wash: learn how to select options that protect clarity, stability, foam, scent performance, and packaging compatibility.MORE+
 Controlled-Release ThermodynamicsModified Cyclodextrins Explained for Controlled Fragrance ReleaseModified cyclodextrins enable controlled fragrance release, odor control, and volatile-note protection. Explore how they optimize performance in detergents, fabric care, and more.MORE+
 Microencapsulated FragrancesHow Fragrance Delivery Systems Improve Fabric Softener LongevityFragrance delivery systems for fabric softeners improve scent longevity through smart protection, reliable deposition, and controlled release for lasting freshness.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Cardamom Oil Supplier for Reliable SupplyNatural cardamom oil supplier evaluation guide: verify botanical origin, purity, batch consistency, documentation, packaging, and delivery reliability for confident sourcing.MORE+
 Maillard Reaction Savory FlavorsHow Ethyl Maltol Purity Testing Supports Flavor Safety ComplianceEthyl Maltol purity testing strengthens flavor safety compliance through identity checks, impurity profiling, supplier verification, and audit-ready documentation.MORE+
 Microencapsulated FragrancesEssential Oil Extracts Compared for Fragrance and Wellness UsesEssential Oil Extracts compared for fragrance and wellness: explore scent profiles, extraction methods, stability, safety, and sourcing insights for smarter formulation choices.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat Drives Zero Calorie Sweeteners Bulk Price in 2026Zero calorie sweeteners bulk price in 2026: compare specifications, dosage, quality, freight, and supply risk to make smarter sourcing decisions.MORE+
 EPA FIFRA & FDA GRAS RegsSynthetic Food Preservatives Rules That Support Safer FormulasSynthetic Food Preservatives: learn the rules for safer formulas, compliant use levels, validated shelf life, labeling, and reliable microbial control.MORE+
 Micelle Fluidics & ChelationHow Anionic Industrial Dispersants Improve Coating StabilityAnionic industrial dispersants improve coating stability, pigment wetting, viscosity control, gloss, and storage performance. Learn how to select and test the right solution.MORE+
 Supercritical CO2 Essential OilsHow to Choose Eucalyptus Oil Grades for Clean, Consistent ProductsChoose the right Eucalyptus Oil grade with confidence. Compare cineole content, purity, origin, processing, documentation, and application fit for consistent products.MORE+
 Micelle Fluidics & ChelationWhat Are Cationic Surfactants and Where Are They Commonly Used?Cationic Surfactants deliver powerful surface affinity for disinfection, fabric softening, hair conditioning, antistatic control, and industrial treatments. Explore key uses and selection factors.MORE+