Choosing Degreasing Solvents for Electronic Components Without Residue
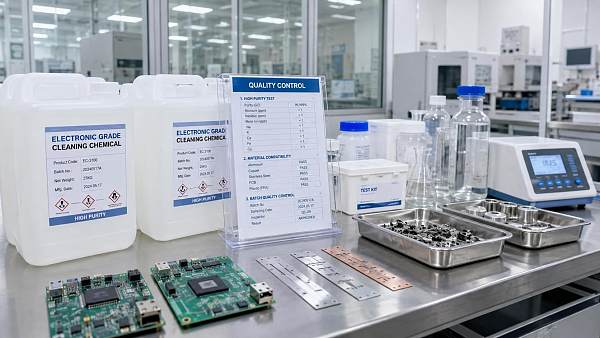
Selecting degreasing solvents for electronic components is no longer just about removing oils and flux residues. For quality control and safety management teams, the right choice has to hold several conditions together at once: cleaning efficiency, material compatibility, low toxicity, regulatory fit, and genuinely low-residue performance. In electronics, a solvent that “cleans well” in a simple bench test can still create later failures through ionic contamination, stress cracking, trapped moisture, or worker exposure issues. That is why the real decision is not which solvent is strongest, but which solvent remains reliable across the full process window.
People searching for guidance on degreasing solvents for electronic components are usually dealing with a practical tension. They may have visible contamination, soldering residues, machining oils, fingerprints, adhesive traces, or particulate carryover. At the same time, they are under pressure to protect assemblies, meet cleanliness targets, avoid rework, and stay within internal EHS rules or customer requirements. In that environment, solvent selection becomes a process control issue, not a simple purchasing item.
Why residue matters more than many teams first assume
In electronic assemblies, residue is rarely just a cosmetic defect. A thin remaining film can interfere with coating adhesion, connector performance, contact resistance, wire bonding, optical clarity, thermal transfer, or long-term insulation reliability. The risk becomes more serious when the contamination is not visually obvious. Some residues are transparent, low-mass, and easy to miss, yet still create leakage current, corrosion potential, or outgassing problems in sealed or high-reliability devices.
This is where a common misunderstanding appears: a fast-evaporating solvent is often assumed to be a no-residue solvent. That is not automatically true. Evaporation rate alone does not determine cleanliness. Residue can come from the contaminant being redeposited, from stabilizers or additives in the solvent system, from incomplete rinsing, from poor bath maintenance, or from interaction between the solvent and the substrate. In other words, “dries quickly” and “leaves nothing behind” are related, but they are not the same judgment.
For quality teams, the working question is narrower and more useful: after cleaning and drying under actual line conditions, does the component meet the required surface cleanliness and reliability criteria? For safety managers, an equally important question sits beside it: can that result be achieved consistently without introducing unacceptable inhalation, flammability, waste, or operator handling risk?
Start with the contamination, not the solvent brochure
Many poor solvent decisions begin with supplier-first thinking. In practice, the evaluation should begin with the soil load and the component structure. “Electronic components” covers a wide range of cleaning challenges, and those challenges do not respond equally to the same chemistry.
- Flux residues may be rosin-based, no-clean, water-soluble, or modified by reflow profile.
- Oils can be light machining lubricants, stamping oils, drawing compounds, greases, or silicone-containing materials.
- Adhesive residues may soften, smear, swell, or cross-link under heat.
- Particles may need displacement and rinse behavior more than chemical solvency alone.
A solvent that performs well on hydrocarbon oils may struggle with polar residues. A product that dissolves flux efficiently may be too aggressive for certain plastics, labels, cable jackets, conformal coatings, potting interfaces, or elastomer seals. This is why broad claims such as “universal electronics cleaner” should be treated cautiously in procurement discussions.
Before narrowing candidates, teams usually need a basic contamination map: what is on the surface, how much is present, where it accumulates, and what failure mode it creates if left behind. Without that step, cleaning trials often become misleading because the solvent is being judged against an undefined target.
The decision criteria that matter in real production
When companies compare degreasing solvents for electronic components, the discussion often starts with solvency strength and unit price. Those are relevant, but they are not enough. In production settings, the better decision usually comes from looking at six factors together.
1. Cleaning performance under actual process conditions
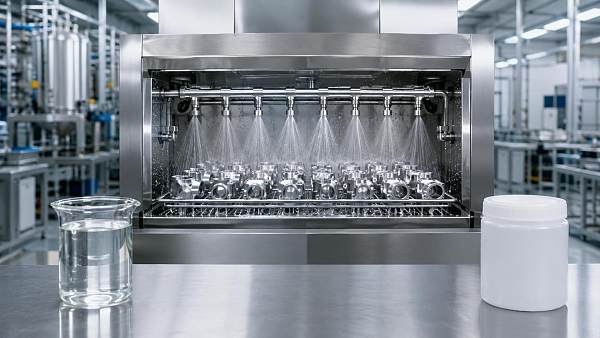
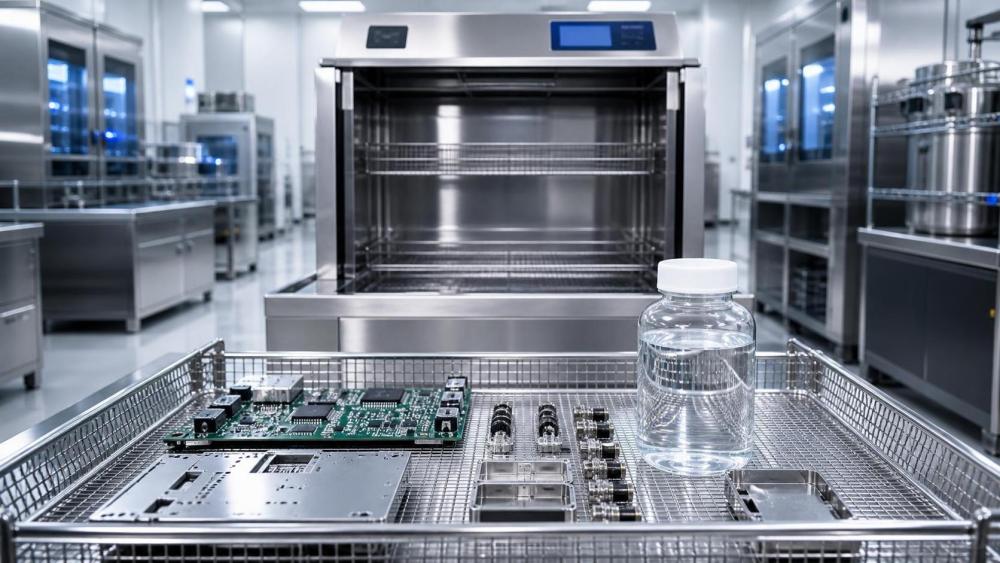
Lab wipe tests can overstate performance. Production reality includes dwell time limits, bath loading, agitation method, spray pressure, temperature control, drying conditions, and component geometry. Tight gaps, under-component spaces, blind holes, and mixed-material assemblies can change the result significantly. A solvent should be tested in the same cleaning method that will be used on the line: vapor degreasing, immersion, spray-in-air, ultrasonic, manual wipe, or hybrid process.
2. Material compatibility
Compatibility is one of the most underestimated failure points. Metals, solder joints, ceramics, engineering plastics, acrylic windows, polycarbonate housings, epoxies, labels, inks, and elastomers do not respond the same way to solvent exposure. The problem is not always immediate attack. Some materials pass a short exposure test but fail later through swelling, embrittlement, haze, crazing, seal degradation, or adhesion loss. For safety and QC teams, compatibility testing should include both immediate appearance and delayed performance checks.
3. Residue and rinse behavior
The solvent should remove contamination without spreading it or leaving a film. In some systems, rinse stages, filtration, distillation, or bath refresh intervals matter as much as the solvent itself. If the process depends on “self-drying” behavior, teams should verify whether dissolved soils remain suspended cleanly or reattach during evaporation. Low non-volatile residue is important, but so is low carryover from the process setup.
4. Worker safety and plant controls
Some effective solvents create operational burdens that cannot be ignored. Flash point, vapor pressure, ventilation demand, skin contact risk, exposure limits, and closed-equipment requirements may affect whether a solvent is practical at all. A safety manager will usually look beyond the SDS headline and ask harder questions: what controls are required at the workstation, what happens during maintenance, how stable is the solvent under repeated use, and how is contaminated waste managed?
5. Regulatory and customer compliance
This area varies by region, export destination, and end-use sector. Restrictions may involve volatile organic compounds, hazardous air pollutants, worker exposure thresholds, transport classification, fluorinated chemistries, or customer-specific substance controls. In electronics supply chains, compliance pressure often arrives through customer questionnaires before it arrives through law. That makes documentation quality almost as important as the chemistry itself.
6. Supply reliability and change control
Even a technically suitable solvent becomes a risk if availability is unstable, formulation changes are poorly communicated, or regional sourcing is uncertain. For high-purity cleaning applications, batch consistency matters. A procurement decision should therefore include supplier quality systems, impurity control, packaging integrity, lead time stability, and notice procedures for formulation or manufacturing-site changes.
Which solvent families are typically considered
There is no single best chemistry for every electronics cleaning task, but most evaluations fall into a few broad categories. These categories should be treated as starting points rather than fixed recommendations, since exact formulations differ widely.
In recent years, many teams have had to revisit older assumptions about precision cleaning chemistries. Solvents once treated as standard options may now face tighter review due to environmental policy, worker safety expectations, or customer sustainability programs. That does not mean they are unusable; it means the justification burden is higher, and substitution planning is more common.
How QC and EHS priorities should meet in the same validation plan
In many factories, quality control tests and safety reviews happen on separate tracks. That is inefficient and can produce late-stage conflicts. A solvent may pass cleaning trials and then fail on ventilation cost, waste profile, operator exposure, or storage restrictions. Or the reverse happens: a solvent looks attractive from an EHS standpoint but cannot reliably meet cleanliness thresholds in dense assemblies.
A better approach is a joint validation plan with shared acceptance criteria. That plan usually includes:
- Defined contamination types and representative test coupons or real components
- Cleaning method, temperature, dwell time, agitation, and drying conditions
- Visual cleanliness plus functional or analytical verification where needed
- Material compatibility screening, including plastics and markings
- Operator handling review and required engineering controls
- Waste, storage, transport, and emergency response considerations
For higher-risk applications, teams may also review ionic contamination, insulation resistance, contact reliability, outgassing behavior, or coating adhesion after cleaning. The exact test package depends on the product class. A consumer appliance board and a high-reliability industrial control module do not carry the same consequence of failure.
What often goes wrong during selection
One recurring problem is choosing a solvent based on removal power alone. Strong solvency can hide downstream costs: higher reject rates from plastic damage, increased fire control requirements, longer drying, stronger odor complaints, or more difficult waste classification. Another issue is evaluating a solvent using fresh chemistry in a clean lab setup, then assuming the same result will hold in a loaded production bath near end-of-life.
Teams also underestimate the importance of process contamination returning from outside the solvent itself. Dirty baskets, poor rinse discipline, evaporated bath concentration shift, operator wiping materials, compressed air quality, and packaging contact after cleaning can all compromise a “no-residue” claim. When failures appear, the solvent gets blamed first even though the process may be the true cause.
There is also a documentation problem in the market. Some product descriptions use broad phrases such as “electronics-safe,” “precision-grade,” or “residue-free” without giving enough information on test conditions. Buyers should press for specifics: residue data, compatibility notes, typical use limits, impurity profile where relevant, and any application constraints. If those details are vague, the risk is being pushed downstream to the user.
What to ask suppliers before moving to plant trials
Procurement and technical teams can save time by asking more disciplined questions early. Useful supplier discussions usually include:
- What contaminant classes has the solvent been validated against?
- What substrate compatibility data are available, and under what exposure conditions?
- Does the formulation contain stabilizers or additives that may affect residue behavior?
- What is the recommended cleaning method and operating window?
- How should bath life be monitored and maintained?
- What are the packaging options for high-purity or sensitive use?
- Are there any known regulatory or transport concerns in target markets?
- How is formulation change communicated to customers?
For a B2B platform audience, this is where supplier evaluation becomes more than a technical conversation. The solvent itself matters, but so do batch consistency, technical service responsiveness, certificate quality, and the supplier’s ability to support revalidation if regulations shift.
The market direction is toward narrower tolerances and fewer assumptions
The broader specialty chemical market is moving toward more application-specific decisions, and electronics cleaning follows that pattern. Buyers are less willing to accept generic solvent claims. They want clearer evidence on residue control, safer handling, and stable documentation. At the same time, environmental expectations are rising, and some solvent classes may face tighter commercial scrutiny even before formal restrictions become universal.
For safety managers, that means substitution pressure will likely continue. For quality teams, it means cleaning validation may need to become more rigorous, especially where assemblies are becoming denser, more mixed in material composition, or more sensitive to low-level contamination. The trend is not simply toward “greener” solvents or “stronger” solvents. It is toward solvents and cleaning systems that are easier to defend technically, operationally, and commercially.
That is usually the right way to frame the decision. The best degreasing solvent for electronic components is the one that meets cleanliness targets without creating a second problem in materials, people, compliance, or supply continuity. Once that standard is applied consistently, the shortlist tends to become much clearer.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+