Why Non Ionic Semiconductor Surfactants Help Control Particle Defects
Particle defects in semiconductor cleaning are rarely controlled by one variable alone. A particle may originate from the wafer, process chamber, slurry residue, photoresist fragments, packaging, water system, filter shedding, or the cleaning formulation itself. The cleaning chemistry must therefore do more than dissolve a visible soil: it must wet complex surfaces, detach fine residues, keep them from redepositing, and rinse away without leaving an ionic or organic film behind.
Non-ionic semiconductor surfactants can support that balance because they reduce interfacial tension without intentionally adding charged species to the process bath. Their value is not simply that they are “mild” or “low foam.” In high-purity cleaning, a suitable non-ionic surfactant can improve liquid access to hydrophobic contamination, promote particle lift-off, stabilize detached residues long enough for removal, and improve rinse uniformity. Yet the same surfactant can become a defect source if its purity, concentration, temperature behavior, or removal profile is not tightly controlled.
Why particle removal depends on wetting before it depends on chemistry
Many semiconductor surfaces are chemically heterogeneous. A wafer may carry native oxide, exposed silicon, dielectric films, metal features, photoresist residue, organic films, polishing residues, or patterned topography. Water-based cleaning solutions do not always spread uniformly across these surfaces, particularly where hydrophobic organic materials or low-energy residues are present. Poor wetting creates local regions where the cleaning liquid cannot efficiently reach the contaminant-substrate interface.
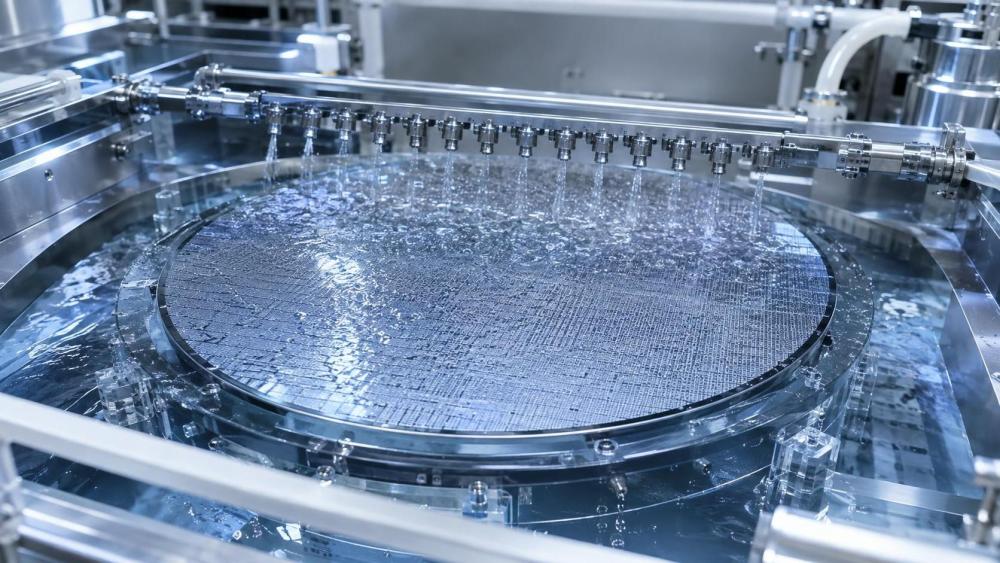
A non-ionic surfactant contains a hydrophobic segment that associates with oils, polymers, and other low-polarity soils, together with a hydrophilic segment that remains compatible with the aqueous phase. At a sufficiently effective concentration, the surfactant lowers surface and interfacial tension. This can reduce the contact angle of the cleaning solution, helping the liquid penetrate narrow structures and spread across surfaces that would otherwise resist aqueous wetting.
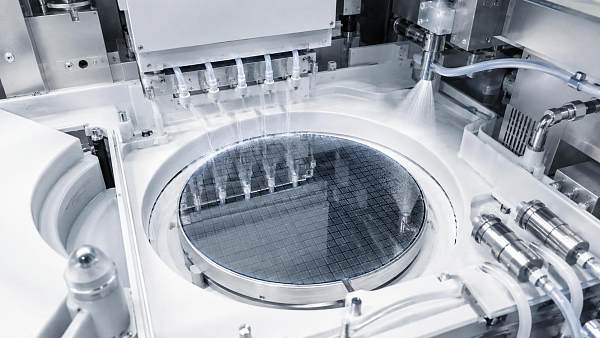
That effect matters for particles because a particle is often held in place by more than simple gravity. Adhesion may involve van der Waals forces, electrostatic interactions, capillary forces, dried chemical residues, polymeric binders, or a thin organic film acting as an adhesive layer. Better wetting allows the solution to enter the particle-substrate interface. Once the underlying film is softened, displaced, emulsified, or dissolved by the full cleaning system, the particle is more likely to be released by fluid shear, spray impact, megasonic energy, brush action, or other mechanical components of the process.
The surfactant is therefore not a substitute for the primary cleaning chemistry. It is an interfacial control component. A formulation that attacks the contaminant chemically but wets poorly may leave localized particle populations. Conversely, a surfactant-rich formulation with weak soil-removal chemistry may disperse material without fully removing the source of adhesion.
How non-ionic chemistry can reduce ionic contamination risk
The distinction between non-ionic and ionic surfactants is especially important in semiconductor-related applications. Anionic and cationic surfactants dissociate in water and introduce charged groups and counterions. Those ions can complicate residue control, alter surface charge, interact with process chemistries, or create concerns where mobile ionic contaminants are tightly restricted.
Non-ionic surfactants do not dissociate in the same way in aqueous solution. Their hydrophilicity is commonly derived from uncharged polar groups, such as polyether, sugar-derived, or other neutral structures. This does not mean that every non-ionic surfactant is automatically appropriate for high-purity use. “Non-ionic” describes the surfactant’s functional behavior, not its total contamination profile.
A product can be non-ionic while still containing trace metals, residual catalysts, salts from processing, low-molecular-weight by-products, unreacted feedstocks, degradation products, packaging-derived extractables, or insoluble particles. For defect-sensitive cleaning, the meaningful question is not whether the surfactant class is non-ionic in principle. It is whether the delivered material, at the intended dilution and under actual process conditions, meets the contamination-control requirements of the cleaning operation.
This distinction prevents a common qualification error: accepting a material based on a generic surfactant description or a standard industrial specification. Commodity-grade non-ionic surfactants may perform well in metal cleaning, hard-surface detergents, or general electronics cleaning while being unsuitable for environments where trace residue, metal content, particle background, and lot consistency are controlled much more tightly.
Particle lift is only useful if redeposition is prevented
Detaching a particle from the wafer is not the same as removing it from the process. Once released, particles can collide with another surface, become trapped in patterned features, deposit during drainage, or remain in stagnant regions of the tool. The cleaning bath must keep the detached material mobile until it is carried away and removed by filtration, overflow, replacement, or rinse.
Non-ionic surfactants can assist through micellar solubilization and dispersion. Above the concentration at which surfactant aggregates form, hydrophobic fragments and some organic residues can be incorporated into micellar structures or associated with surfactant-rich domains. This reduces the tendency of oily or polymeric contaminants to agglomerate and reattach. For particles associated with organic films, that can be particularly useful: the surfactant does not merely move the particle but can help disrupt the adhesive phase that supports redeposition.
However, dispersing particles is not universally beneficial. If the formulation stabilizes particles too effectively but the tool’s filtration, bath turnover, or rinse sequence cannot remove them, the system may retain a circulating particle load. The quality concern then shifts from initial cleaning efficiency to bath cleanliness and carryover. Particle-control performance must be evaluated as a complete sequence: contaminant release, transport, capture or purge, rinsing, drying, and final surface inspection.
The rinse step is where a useful surfactant can become a residue problem
Non-ionic surfactants are often selected because they can improve wetting and reduce water-break behavior during cleaning. But their relatively low volatility and surface activity also create a basic challenge: they are designed to adsorb at interfaces. If the rinse is inadequate, residual surfactant can remain on the wafer, in high-aspect-ratio features, on tool surfaces, or at liquid-air boundaries.
Residual organic film can interfere with later process steps even when no obvious particle is visible. It may affect surface energy, coating uniformity, adhesion, etch behavior, oxidation behavior, or analytical measurements. In some cases, an incompletely rinsed surfactant layer can attract later contamination or alter the way a surface dries, indirectly contributing to watermark and particle-related defects.
Rinse compatibility must therefore be evaluated together with cleaning performance. Important considerations include the surfactant’s water solubility, molecular weight distribution, adsorption tendency, cloud point behavior, concentration, temperature, rinse-water quality, flow pattern, and rinse duration. A formulation that works at bench scale can behave differently in a recirculating tool or a spray process where dead legs, low-flow zones, and component surfaces retain chemistry.
Low concentration is not automatically safer. Below the level needed for reliable wetting, performance can become uneven across the wafer or from lot to lot. Above the level that the rinse can clear efficiently, residual film and foaming risk increase. The practical operating window is determined by process validation, not by a generic dosage range published for unrelated industrial cleaning uses.
Temperature and cloud point deserve explicit control
Many polyether-based non-ionic surfactants show temperature-dependent solubility in water. At elevated temperatures, some systems approach a cloud point at which the solution becomes less uniform and surfactant-rich phases can begin to form. Even before visible clouding, changes in micelle structure, wetting behavior, foam response, and adsorption can influence particle-removal consistency.
For quality control, this means the acceptable temperature range should not be defined only by the cleaning tool’s heater setting. It should account for local thermal variation, heat-up time, chemical replenishment temperature, recirculation conditions, and storage history. A surfactant that remains clear in a laboratory beaker may behave differently when mixed with alkaline components, solvents, oxidizers, dissolved organics, or high-purity water at operating temperature.
Compatibility testing should also consider the complete formulation. Electrolytes, pH modifiers, solvents, oxidizing agents, and dissolved contaminants can shift surfactant behavior. A non-ionic surfactant may be chemically uncharged but still be sensitive to formulation conditions that alter phase stability or cause haze, precipitation, or particle formation. Any visible turbidity in a high-purity cleaning solution is a process signal requiring investigation rather than an acceptable cosmetic variation.
Purity control is broader than an assay value
Assay or active-content data alone do not establish suitability for semiconductor cleaning. A high assay confirms the approximate amount of the intended surfactant, but it does not describe the contaminants most relevant to defect control. Incoming-material control should be built around the actual risk profile of the process.
Typical areas requiring review include:
- particle count and filtration condition of the supplied material;
- trace metals and other inorganic contaminants relevant to the process sensitivity;
- ionic residue, conductivity, and extractable inorganic content where applicable;
- nonvolatile residue after evaporation or controlled thermal treatment;
- water content, color, haze, and evidence of phase separation;
- organic impurity profile, especially low-molecular-weight residues and unreacted feedstocks;
- lot-to-lot consistency in surface tension, cloud point, and cleaning-process performance;
- container cleanliness, closure integrity, and potential extractables from packaging materials.
The relevant acceptance limits are process-specific. A limit suitable for one cleaning stage may be inadequate for another, depending on device architecture, material stack, downstream sensitivity, and defect budget. It is more defensible to link raw-material specifications to an established process risk assessment than to rely on broad statements such as “electronic grade” without defining the associated analytical controls.
Filtration protects the process, but it does not correct an unsuitable chemistry
Point-of-use filtration is a critical barrier against particles introduced during storage, transfer, blending, or recirculation. It can remove insoluble contaminants and gel-like material above the filter’s effective retention range. It cannot remove dissolved ionic contaminants, most molecular organic residues, or a surfactant film that remains adsorbed on a wafer after rinsing.
Filter compatibility is also part of qualification. Surfactants and co-solvents can extract materials from filter media, change wetting behavior during start-up, or contribute to pressure-rise behavior when interacting with contamination in the bath. A filter that is appropriate for ultra-pure water is not automatically suitable for a surfactant-containing formulation. Pre-flush requirements, hold-up volume, chemical exposure time, and potential extractables should be assessed under representative conditions.
From a defect-investigation perspective, an increase in wafer particle counts should not automatically be attributed to the surfactant itself. Useful differentiation includes comparing unused filtered chemistry, recirculated bath samples, post-filter samples, rinse-water samples, and tool blank runs. This helps separate raw-material contamination from particle generation in the tool, contamination released from process hardware, inadequate bath maintenance, or ineffective rinsing.
Safety controls should follow the formulation, not the word “non-ionic”
Non-ionic surfactants are sometimes treated as inherently low-risk because they are uncharged and often used at low concentration. That is not an adequate safety conclusion. Hazard characteristics depend on the individual chemical structure, concentration, co-formulants, and operating conditions. Some materials can irritate skin or eyes, generate aerosols during spraying, become slippery when spilled, or present hazards when heated or mixed with incompatible chemicals.
Safety review should use the supplier’s current safety data sheet and the actual process design. The assessment should cover chemical transfer, drum or tote handling, dilution sequence, ventilation, splash and aerosol exposure, spill containment, compatibility with oxidizers or strong acids and bases, waste treatment, and emergency decontamination. Where the surfactant is blended into a proprietary cleaner, the hazards of the complete mixture govern handling controls.
It is also important to distinguish worker safety from wafer safety. A chemistry may be manageable with appropriate personal protective equipment and engineering controls while still being unacceptable for a critical clean because of trace contamination or rinse residue. These are separate approval decisions and should not be collapsed into a single “safe to use” judgment.
What a defensible qualification decision looks like
Non ionic semiconductor surfactants help control particle defects when their interfacial benefits are matched to a validated removal and rinse process. The strongest qualification logic does not begin with a supplier claim about low foam, high purity, or non-ionic character. It begins with the defect mechanism that must be controlled: poor wetting, organic-bound particles, redeposition, bath particle loading, residue after rinse, or process variability caused by temperature and concentration.
A suitable evaluation connects material data to wafer-level outcomes. It verifies that the surfactant improves coverage and particle removal under representative chemistry, temperature, agitation, and dwell conditions; that it does not create unacceptable residue or foam; that its impurity profile remains within process limits; and that filtration, rinsing, storage, and transfer controls preserve that performance over the intended operating life.
The central point is straightforward: non-ionic chemistry can reduce one important source of process risk—intentional ionic surfactant contribution—while improving wetting and soil transport. It does not eliminate contamination risk. In semiconductor cleaning, defect control depends on treating the surfactant as a tightly specified process material whose purity, stability, compatibility, and removability must be demonstrated as carefully as its cleaning action.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+