When Silicone Free Industrial Defoaming Agents Solve Process Foam
When Silicone Free Industrial Defoaming Agents Solve Process Foam
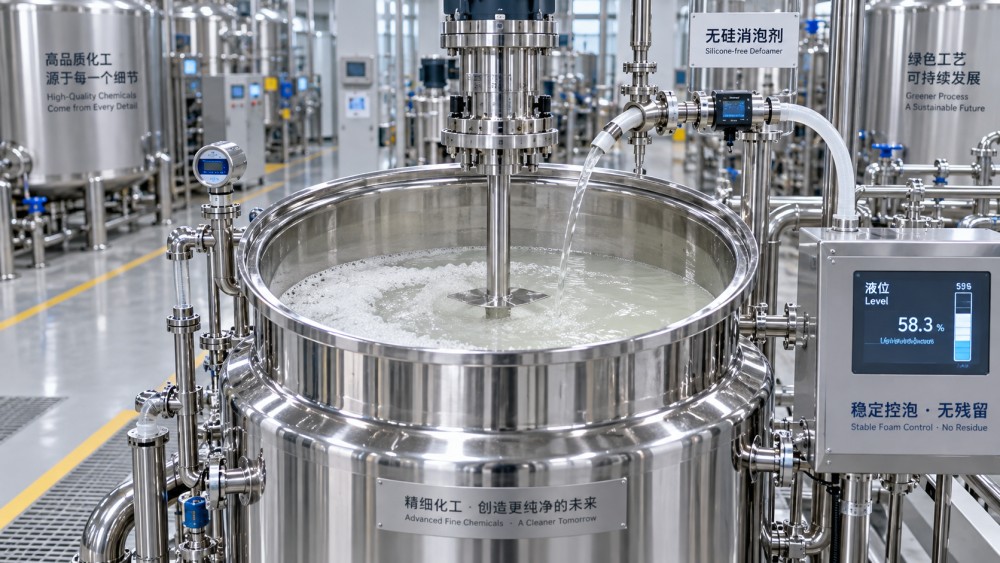
Persistent foam is rarely just a visual nuisance. In an industrial cleaning tank, mixing vessel, coating line, wastewater unit, or formulated chemical batch, foam can conceal liquid level, trigger pump cavitation, reduce usable vessel capacity, slow filtration, interfere with sensors, and create inconsistent operating conditions from one shift to the next. The obvious response is to add a stronger defoamer. Yet that is not always the right response, especially when silicone residue can create problems later in the process.
Silicone free industrial defoaming agents are used when foam control is necessary but silicone-based chemistry presents a compatibility, cleanliness, surface-quality, or downstream processing concern. They are not automatically superior to silicone defoamers; silicone products can be highly efficient in many systems. The question is whether the process can tolerate what remains after the foam has collapsed. Where even trace silicone contamination may affect coating adhesion, painting, printing, bonding, electronic cleaning, or high-purity rinsing, a silicone-free approach is often worth evaluating early rather than treating as a last-minute correction.
For operators, the practical objective is not simply “no foam.” It is stable foam control at the lowest workable addition level, without creating separation, residue, fish-eyes, loss of cleaning performance, altered viscosity, or complications in the next production stage.
Why some process foam becomes difficult to control
Foam forms when air is dispersed into a liquid and stabilized by surface-active materials. In real plants, those materials may be intentional ingredients such as surfactants, emulsifiers, dispersants, wetting agents, proteins, polymers, or detergents. They may also arrive indirectly through soils, oils, formulation carryover, recirculated water, or changes in raw-material quality. Agitation, pumping, spraying, pressure release, high-speed filling, filtration, and air entrainment all supply the mechanical energy needed to keep the foam alive.
This is why a defoamer that performs well in a simple beaker test may fail in a production loop. A laboratory sample may not reproduce shear, temperature swings, continuous air introduction, soil loading, dwell time, or the order in which ingredients are added. Foam behavior can also shift during a batch: an early-stage problem may be caused by surfactant wetting, while late-stage foam may be reinforced by viscosity increase, particulate loading, or polymer development.
Before selecting an antifoam, operators should separate two related but different tasks. Defoaming means knocking down foam that already exists. Foam prevention means limiting new foam formation during mixing, transfer, circulation, or use. A product can be fast at collapsing surface foam but weak against repeated aeration. Another may act more slowly but keep a recirculation system stable over time. The process requirement decides which performance matters more.
When silicone-free chemistry is the sensible choice
Silicone-free defoamers are commonly considered in systems where downstream surface quality is critical. In coatings, inks, paints, adhesives, and surface-treatment operations, silicone migration can sometimes contribute to coating defects or make later finishing less predictable. The exact risk depends on the materials, application method, cleaning sequence, and surface specification, but the concern is familiar enough that many facilities prefer to avoid silicone where compatibility is uncertain.
Industrial cleaning is another important setting. A low-foam cleaner must still wet a contaminated surface, lift soil, disperse oil, and rinse acceptably. When parts are later painted, plated, bonded, printed, or used in sensitive assemblies, the cleaner and its foam-control additives should be assessed as part of the whole process rather than as isolated ingredients. The relevant question is not merely whether the bath looks calm; it is whether the cleaned part remains suitable for its next operation.
High-purity and electronics-related cleaning environments may impose even tighter internal requirements. Here, a silicone-free label alone does not prove suitability. Operators may need to consider residue profile, rinseability, ionic contamination concerns, packaging cleanliness, and the chemistry of every component introduced into the system. A supplier’s technical data and the facility’s own qualification procedure both matter.
The same reasoning appears in chemical formulation. Crop-protection suspensions, liquid fertilizers, food-processing auxiliaries, fermentation-related systems, water-based industrial products, and specialty surfactant blends can all foam during manufacture or filling. If the end formulation must retain a particular appearance, dispersion stability, wetting behavior, or application profile, the defoamer must be tested for side effects rather than selected only by its initial knockdown speed.
What silicone-free defoamers are made to do
Silicone-free antifoam systems can be based on mineral oils, vegetable-derived oils, hydrophobic particles, fatty alcohols, esters, polyethers, or other tailored organic carriers. Their behavior depends on how effectively the defoamer enters the foam film, destabilizes it, and spreads at the air-liquid interface. The formulation must be sufficiently incompatible with the foaming medium to disrupt foam, but not so incompatible that it separates, creates visible defects, or becomes impossible to distribute evenly.
That balance explains why the phrase “silicone free” is only a starting point. Two silicone-free products can behave very differently in the same bath. One may disperse rapidly in alkaline aqueous cleaner but lose effectiveness in a hot recirculating system. Another may remain active under shear but leave an oily film that is unacceptable before coating. In a water-based formulation, a defoamer designed for processing may not be appropriate for the finished product, where long-term storage stability and end-use appearance are more important.
A good selection process therefore considers the full liquid environment: pH, temperature, hardness of process water, surfactant package, solvent content, solids loading, salt level, viscosity, mixing intensity, and expected residence time. Changes that appear small on paper can alter foam stability dramatically. A plant switching to a new non-ionic surfactant, changing water source, or increasing pump speed may find that a previously reliable antifoam no longer behaves the same way.
A practical way to investigate a foam problem
When foam becomes disruptive, adding more defoamer is often the fastest action—and sometimes the least informative one. Excess dosing can mask the real cause while creating new compatibility issues. A better investigation starts with the operating moment at which foam changes: during raw-material charging, high-shear dispersion, tank circulation, spray application, heating, filtration, or final filling. This observation narrows the likely mechanism.
- Record whether foam is transient, persistent, or continuously regenerated by pumping or air ingress.
- Note the batch temperature, pH, water quality, agitation speed, transfer rate, and additions made shortly before foam appeared.
- Check whether the issue follows a specific raw-material lot, cleaning cycle, operator practice, or equipment condition.
- Define the downstream restriction clearly: silicone avoidance, coating quality, rinse cleanliness, food-contact review, storage stability, or another project-specific requirement.
- Test the defoamer in the actual formulation or bath under representative shear and temperature, not only in deionized water.
For a batch process, it can be useful to compare addition points. A small pre-addition before high-shear mixing may prevent a foam surge, whereas a later top-dose may only collapse foam temporarily. In continuous systems, metering location matters just as much. A defoamer introduced where turbulence disperses it thoroughly may perform differently from the same product injected into a quiet tank zone. Poor dosing equipment, blocked lines, or inconsistent feed rates can easily be mistaken for a chemistry failure.
Do not trade foam for another defect
The most common selection mistake is focusing on immediate foam collapse while overlooking the finished system. In coatings and inks, examine gloss, leveling, crater formation, adhesion, and appearance after drying. In industrial cleaners, examine soil removal, rinse behavior, residue, corrosion protection, and compatibility with treated substrates. In agricultural or specialty chemical formulations, review physical stability, redispersibility, spray behavior, and any effect on the active ingredient or carrier system. Food-related applications require their own assessment of formulation suitability and applicable regulatory requirements; an industrial-grade defoamer should never be assumed suitable simply because it is silicone-free.
There is also a difference between a processing aid and an in-can additive. A defoamer used during manufacture may be removed, diluted, or rendered irrelevant in later stages. A defoamer retained in the final product remains part of the formulation and must be compatible throughout storage and use. Operators should communicate this distinction when requesting samples or technical support. It affects product choice, test design, dosage expectations, and documentation needs.
Storage and handling deserve attention as well. Some defoamer dispersions can settle or separate over time, particularly after exposure to unsuitable temperatures. If a product requires mixing before use, that instruction should be incorporated into normal operating practice rather than treated as an optional note. A properly selected defoamer can still appear ineffective if only the carrier phase is drawn from a partially separated drum.
How to compare options without relying on broad claims
A useful comparison does not ask which defoamer is “best.” It asks which candidate controls the relevant foam under actual process conditions while preserving every property that matters after the foam is gone. A simple internal trial plan can compare initial knockdown, resistance to repeated aeration, dose-response behavior, persistence after heating or shear, and visible or functional side effects. The same evaluation should include a blank sample and, where appropriate, the current in-use defoamer as a reference.
Documentation should match the application. Depending on the project, teams may need a technical data sheet, safety documentation, composition information appropriate to the supplier relationship, allergen or food-contact statements where relevant, regulatory status for the intended market, and confirmation of silicone-free status. These documents should be reviewed against the specific application, not filed as generic proof of fitness. Requirements may differ by region, end use, and customer specification.
This broader view is central to the work covered by the Global Fine Chemicals & Agrochemical Intelligence Network (FCAS). Across specialty surfactants, industrial cleaners, defoamers, agrochemical formulations, food ingredients, and high-purity processing materials, product evaluation is increasingly tied to application fit, batch consistency, safety documentation, packaging, transport, and downstream compatibility. The useful commercial question is no longer just “What is the active chemistry?” but “What happens when this chemistry enters our actual process?”
The decision point is usually downstream
Silicone free industrial defoaming agents solve process foam most effectively when silicone avoidance is connected to a real operational need: protecting a finish, maintaining cleaning quality, preventing problematic residues, supporting a sensitive formulation, or meeting a defined internal specification. They are less useful when chosen only because “silicone-free” sounds safer, without confirming whether the alternative chemistry is compatible with the system.
For the operator facing foam on the line, the next step is practical: identify where the air enters, define whether prevention or knockdown is needed, test candidates at realistic conditions, and inspect the result after the process—not only during it. That approach turns defoamer selection from a reactive dosing exercise into a controlled process decision.
Related News
 Antioxidants & Natural PreservativesWhat Quality Checks Matter When Sourcing Butylparaben for Personal CareButylparaben for personal care sourcing guide: compare assay, impurities, physical performance, documentation, traceability, and supplier quality to reduce formulation risk.MORE+
 Nano-microcapsule FormulationsHow Encapsulated Flavors Protect Taste During Processing and StorageEncapsulated Flavors protect taste from heat, oxygen, moisture, and storage loss. Explore smarter release, carrier selection, and processing strategies.MORE+
 Chelated Trace Element FertilizersHow Greenhouse Fertigation Systems Reduce Water and Fertilizer WasteGreenhouse fertigation systems reduce water and fertilizer waste with precise dosing, uniform irrigation, drainage monitoring, and smarter crop-zone control. Learn practical strategies.MORE+
 Supercritical CO2 Essential OilsHow Natural Essential Oil Blends Improve Consistent Product FragranceNatural essential oil blends help brands achieve consistent, appealing fragrance across batches. Explore smart blend design, stability testing, and product compatibility strategies.MORE+
 Non-ionic Surfactants & DefoamersHow to Choose Non Ionic Low Foaming Surfactants for CIP CleaningNon ionic low foaming surfactants for CIP cleaning: learn how to balance wetting, foam control, compatibility, and rinseability for reliable cleaning performance.MORE+
 Nano-microcapsule FormulationsHow Food Grade Cyclodextrin Complexes Protect Sensitive FlavorsFood grade cyclodextrin inclusion complexes help protect sensitive flavors from oxidation, evaporation, and processing loss while supporting controlled release and consistent sensory quality.MORE+
 Polymer-Coated Water Soluble NPKHow Fertilizer Coating Polymers Improve NPK Granule ReleaseFertilizer coating polymers for NPK granules improve controlled nutrient release, reduce loss risks, and enhance product consistency. Discover key selection and process insights.MORE+
 Chelated Trace Element FertilizersWhat Diammonium Phosphate Means for Crop Nutrition PlanningDiammonium Phosphate: learn how DAP supports early phosphorus access, nitrogen budgeting, smart placement, and balanced crop nutrition planning.MORE+
 Maillard Reaction Savory FlavorsHow to Assess a Flavor Bases Supplier List for Reliable SourcingGlobal Fine Chemicals & Agrochemical Intelligence Network flavor bases supplier list: assess specs, samples, supply risk, and true cost to source with confidence.MORE+
 Hydrocolloids & EmulsifiersHow Konjac Gum Powder Improves Texture in Low-Calorie FoodsKonjac gum powder improves body, stability, and mouthfeel in low-calorie foods. Discover practical tips for smoother sauces, beverages, and reduced-fat formulations.MORE+
 Supercritical CO2 Essential OilsWhat to Check Before Choosing a Botanical Essential Oils ManufacturerChoose a botanical essential oils manufacturer with confidence. Explore key checks for purity, traceability, compliance, batch consistency, and reliable supply.MORE+
 Microencapsulated FragrancesHow Fragrance Carriers for Detergents Improve Scent PerformanceFragrance carriers for detergents improve stability, fabric deposition, and long-lasting scent. Explore practical solutions for better wash-to-wear fragrance performance.MORE+
 Antioxidants & Natural PreservativesWhen Propyl Gallate Antioxidant Is the Right Choice for Oil StabilityPropyl gallate antioxidant: learn when it is the right choice for oil stability, shelf-life protection, processing compatibility, and smarter formulation decisions.MORE+
 Antioxidants & Natural PreservativesHow Potassium Sorbate Extends Shelf Life in Food and Beverage ProductsPotassium Sorbate helps food and beverage brands control yeast and mold spoilage. Explore pH, dosage, processing, and packaging strategies for reliable shelf life.MORE+
 Antioxidants & Natural PreservativesHow to Source Bulk Herbal Extracts With Reliable Quality ControlBulk herbal extracts sourcing guide: compare suppliers, verify traceability, review CoAs, and build reliable quality controls for safer, consistent purchasing.MORE+
 Antioxidants & Natural PreservativesWhat to Check Before Sourcing Butylparaben for Personal Care FormulasButylparaben for personal care sourcing guide: check market eligibility, purity, supplier controls, formula compatibility, packaging, and total risk before buying.MORE+
 Targeted Bio-pesticides & APIsChoosing Microbial Fungicides for Foliar Diseases in Integrated Crop ProgramsMicrobial fungicides for foliar diseases: learn how to match biology, formulation, tank compatibility, and timing for stronger integrated crop protection.MORE+
 Targeted Bio-pesticides & APIsHow Microbial Insecticides Control Caterpillars With Lower Crop Residue RiskMicrobial insecticides for caterpillars help protect crops with targeted early-larval control and lower residue-management pressure. Learn timing, coverage, compliance, and scouting essentials.MORE+
 Microencapsulated FragrancesHow to Add Encapsulated Laundry Fragrances Without Weakening Wash ResultsEncapsulated laundry fragrances: learn how to boost long-lasting scent while protecting cleaning power, stability, foam control, and fabric care.MORE+
 Supercritical CO2 Essential OilsHow Aroma Ingredients Shape Lasting and Skin-Safe Personal Care ProductsAroma ingredients for personal care: discover how to achieve lasting scent, formulation stability, skin safety, and confident product performance.MORE+
 Targeted Bio-pesticides & APIsInsecticides Explained Through Labels, Active Ingredients, and SafetyInsecticides explained through labels, active ingredients, formulations, and safety. Learn how to compare products, manage risk, and make informed crop protection decisions.MORE+
 Heavy-duty Industrial DegreasersHow to Select Parts Wash Cleaners for Automotive ComponentsParts wash cleaners for automotive components: learn how to match chemistry, materials, rinsing, safety, and waste controls for reliable cleaning results.MORE+
 Chelated Trace Element FertilizersHow Precision Fertigation Systems Improve Water and Nutrient ControlPrecision fertigation systems improve water and nutrient control with accurate dosing, uniform irrigation, smart monitoring, and reduced waste. Discover how to optimize crop performance.MORE+
 Hydrocolloids & EmulsifiersHow Bulk Price Factors Affect Hydrocolloid Stabilizer Blend SourcingHydrocolloid stabilizer blends bulk price: compare dosage efficiency, quality consistency, logistics, and documentation to reduce total sourcing costs.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow to Choose a Natural Sweeteners Supplier for Clean-Label ProductsNatural sweeteners supplier selection guide for clean-label products: compare formulation fit, traceability, documentation, and supply reliability.MORE+
 Non-ionic Surfactants & DefoamersWhat Cationic Surfactants Do and Where They Are UsedCationic Surfactants deliver antimicrobial action, conditioning, antistatic control, and surface treatment benefits. Explore key uses, compatibility, and safe selection tips.MORE+
 Targeted Bio-pesticides & APIsHow to Evaluate Pesticide Suspension Concentrates for Field StabilityPesticide Suspension Concentrates: learn how to evaluate field stability, redispersibility, dilution, tank-mix compatibility, and spray safety for reliable performance.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Systems for Meat Products Improve Texture and YieldHydrocolloid systems for meat products improve yield, texture, water retention, and slicing quality. Explore practical formulation strategies for stable, high-performing meat products.MORE+
 Microencapsulated FragrancesHow Laundry Fragrances for Liquid Detergents Improve Scent LongevityLaundry fragrances for liquid detergents: discover how fragrance design, deposition, and encapsulation create lasting fabric freshness and stronger product appeal.MORE+
 Nano-microcapsule FormulationsChoosing Fragrance Preparations That Perform Well in Personal WashFragrance preparations for personal wash: learn how to select options that protect clarity, stability, foam, scent performance, and packaging compatibility.MORE+
 Controlled-Release ThermodynamicsModified Cyclodextrins Explained for Controlled Fragrance ReleaseModified cyclodextrins enable controlled fragrance release, odor control, and volatile-note protection. Explore how they optimize performance in detergents, fabric care, and more.MORE+
 Microencapsulated FragrancesHow Fragrance Delivery Systems Improve Fabric Softener LongevityFragrance delivery systems for fabric softeners improve scent longevity through smart protection, reliable deposition, and controlled release for lasting freshness.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Cardamom Oil Supplier for Reliable SupplyNatural cardamom oil supplier evaluation guide: verify botanical origin, purity, batch consistency, documentation, packaging, and delivery reliability for confident sourcing.MORE+
 Maillard Reaction Savory FlavorsHow Ethyl Maltol Purity Testing Supports Flavor Safety ComplianceEthyl Maltol purity testing strengthens flavor safety compliance through identity checks, impurity profiling, supplier verification, and audit-ready documentation.MORE+
 Microencapsulated FragrancesEssential Oil Extracts Compared for Fragrance and Wellness UsesEssential Oil Extracts compared for fragrance and wellness: explore scent profiles, extraction methods, stability, safety, and sourcing insights for smarter formulation choices.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat Drives Zero Calorie Sweeteners Bulk Price in 2026Zero calorie sweeteners bulk price in 2026: compare specifications, dosage, quality, freight, and supply risk to make smarter sourcing decisions.MORE+
 EPA FIFRA & FDA GRAS RegsSynthetic Food Preservatives Rules That Support Safer FormulasSynthetic Food Preservatives: learn the rules for safer formulas, compliant use levels, validated shelf life, labeling, and reliable microbial control.MORE+
 Micelle Fluidics & ChelationHow Anionic Industrial Dispersants Improve Coating StabilityAnionic industrial dispersants improve coating stability, pigment wetting, viscosity control, gloss, and storage performance. Learn how to select and test the right solution.MORE+
 Supercritical CO2 Essential OilsHow to Choose Eucalyptus Oil Grades for Clean, Consistent ProductsChoose the right Eucalyptus Oil grade with confidence. Compare cineole content, purity, origin, processing, documentation, and application fit for consistent products.MORE+
 Micelle Fluidics & ChelationWhat Are Cationic Surfactants and Where Are They Commonly Used?Cationic Surfactants deliver powerful surface affinity for disinfection, fabric softening, hair conditioning, antistatic control, and industrial treatments. Explore key uses and selection factors.MORE+