How to Select Defoamers for Fermentation Without Reducing Yield
Selecting defoamers for fermentation is not a matter of finding the fastest foam knockdown. A product can make the vessel look calm while quietly reducing oxygen transfer, affecting cell growth, complicating filtration, or lowering recovery downstream. The practical target is controlled foam at the lowest effective addition rate, with no meaningful penalty to process performance or final yield.
That distinction matters because fermentation foam is not always a sign of poor operation. Proteins, peptides, carbohydrates, cells, media components, aeration rate, agitation, and metabolic changes can all contribute. The wrong response is to treat every foam event with a large manual dose of antifoam. The better response is to identify when foam occurs, what is driving it, and which defoamer chemistry fits the organism, medium, process stage, and product-recovery route.
In short: choose a defoamer that is effective under your real fermentation conditions, then prove that its minimum working dose does not harm oxygen transfer, microbial performance, or downstream separation.
Why Defoamers Can Reduce Fermentation Yield
Foam control and yield are connected through more than one mechanism. In aerobic fermentation, the first concern is often oxygen transfer. Many defoamers reduce surface tension and alter gas-liquid behavior. That is how they collapse foam, but excessive or poorly matched antifoam can also reduce the volumetric oxygen-transfer capacity of the broth. When oxygen demand is already close to the equipment limit, even a modest reduction can push the culture into oxygen limitation.
The result is not always immediate. Operators may first see a change in dissolved oxygen control, increased agitation demand, higher air or oxygen enrichment requirements, a shift in feed behavior, or a longer batch time. In sensitive processes, the culture may change its metabolic pathway before anyone identifies the antifoam dose as a contributing factor.
Downstream effects can be just as expensive. Hydrophobic defoamers may interfere with membrane filtration, adsorption, extraction, chromatography, centrifugation, or product crystallization. Some can persist in the broth and accumulate in solid fractions. A defoamer that performs well in a seed fermenter may therefore be unsuitable for a process where the final product must meet tight purity, residue, sensory, or regulatory expectations.
This does not mean antifoams should be avoided. It means they should be treated as process aids with a defined performance window, not as emergency additives used without a control strategy.
Start With the Fermentation, Not the Defoamer Catalog
A supplier may offer silicone, polyether, mineral-oil-based, ester-based, vegetable-oil-based, or emulsion antifoams. Those categories are useful starting points, but they are not a selection decision by themselves. The same chemistry can behave very differently depending on formulation, active content, emulsifier package, broth composition, sterilization method, and feed profile.
Before requesting samples, build a short process description. It should answer a few operational questions:
- What organism is being cultivated: bacteria, yeast, filamentous fungi, mammalian cells, or another culture?
- Is the process aerobic, oxygen-enriched, anaerobic, or intermittently aerated?
- When does foaming begin: after inoculation, during feeding, near peak biomass, or during harvest?
- What are the maximum agitation speed, gas flow, vessel fill volume, pressure, and operating temperature?
- Will the broth go through filtration, centrifugation, membrane concentration, extraction, or chromatography?
- Does the application require food-grade, pharmacopeial, low-residue, allergen, halal, kosher, or other specific documentation?
These answers usually eliminate unsuitable options quickly. For example, a robust industrial enzyme fermentation may tolerate a broader range of antifoam chemistries than a food fermentation with sensitive flavor requirements. A process using microfiltration deserves early compatibility work, because a defoamer that controls foam well can still cause flux decline or difficult cleaning later.
Foam timing is especially informative. Foam that appears only after a nutrient feed may point to the feed composition, feed rate, or localized mixing issue rather than a general antifoam deficiency. Foam that rises sharply as biomass increases may be a genuine capacity issue, but it can also indicate inadequate headspace, excessive aeration, or poor gas dispersion. Changing the defoamer alone may hide the root cause without improving batch consistency.
Evaluate Defoamers for Fermentation on Three Process Risks
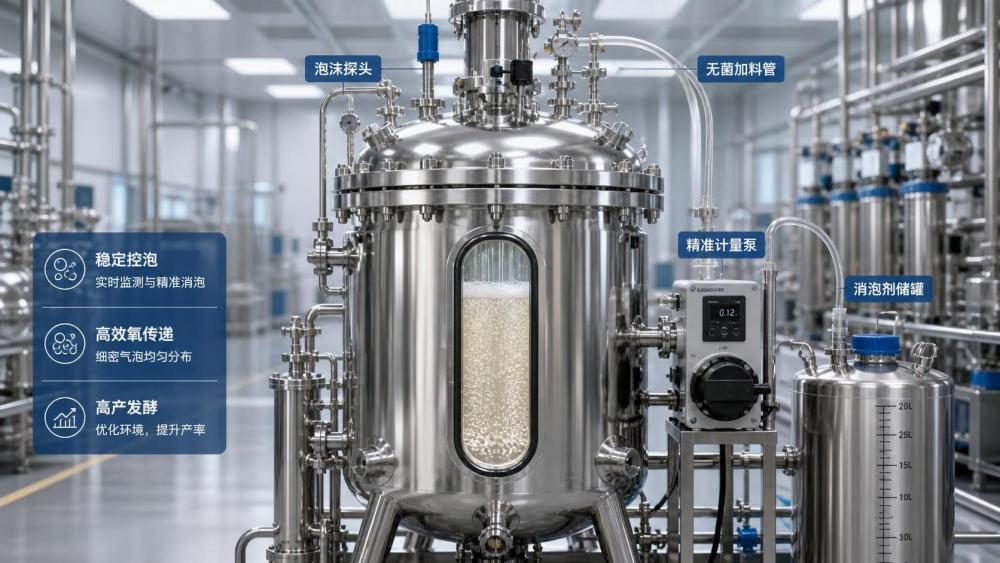
A useful evaluation separates foam performance from biological and downstream risk. A sample should pass all three tests. Fast collapse in a beaker is not enough.
1. Foam-control performance at the lowest practical dose
Look beyond “foam disappears.” Record the dose required to prevent overflow or probe fouling under representative aeration and agitation. Also observe whether the product gives immediate knockdown but poor persistence, or whether it controls foam steadily with small additions. A defoamer that needs frequent large shots may create more process variability than one that works at a slightly higher initial dose but remains effective through the growth phase.
For automated systems, check how the material behaves in the dosing line. Some emulsions separate during storage, settle, thicken at low temperature, or lose performance after repeated pumping. If a product requires continuous agitation in its day tank, that should become part of the operating procedure rather than an assumption left to the shift team.
2. Culture compatibility and oxygen-transfer impact
Run side-by-side fermentation trials using a no-antifoam control where safely possible, the current product, and the candidate product. Compare not just final titer but the batch profile: dissolved oxygen trend, agitation cascade, gas demand, pH control, feed rate, biomass, substrate consumption, product formation, and batch duration.
The candidate does not have to produce a better yield to be acceptable. It must show that foam control can be achieved without a meaningful adverse shift in the critical process indicators. Define “meaningful” before testing, based on your validated process limits and production economics. Do not rely on a single batch; biological systems have normal variation, and one apparent improvement may have nothing to do with the antifoam.
A common mistake is testing antifoam only in a lab flask. Shake-flask screening can identify obvious toxicity or gross incompatibility, but it cannot reliably reproduce sparger behavior, power input, hydrostatic pressure, gas holdup, or oxygen-transfer limits in a production vessel. Bench or pilot bioreactor trials are far more relevant when yield risk is significant.
3. Downstream compatibility
Take candidate-treated broth into the first meaningful downstream step. For a filtered product, measure filtration behavior and inspect whether the filter becomes unusually hydrophobic or difficult to rinse. For centrifuged material, check clarification and solids handling. For purified products, examine whether the defoamer creates visible phase problems, unusual fouling, or changes in recovery.
This is where low-dose silicone products can be attractive in some applications: they may provide strong foam suppression at small additions. But “silicone” is not automatically the correct answer. Depending on the purification train, residual silicone can be difficult to manage. Likewise, oil-based or natural-oil formulations may be preferred in selected food or biological processes, yet they can change downstream loading or contribute to analytical interference. Compatibility must be demonstrated on the actual route.
Match the Chemistry to the Process Window
Silicone-based defoamers are commonly chosen when strong, rapid foam control is needed at low dosage. They can be effective in demanding aerated systems, but require careful assessment where membrane performance, surface-sensitive downstream operations, or residue control are critical.
Polyether-based products can offer useful compatibility in certain fermentation systems and are often considered where dispersion and controlled addition matter. Their behavior varies substantially with molecular structure and formulation, so broad claims are not reliable. Test the exact commercial grade, not just a generic chemistry label.
Vegetable-oil, ester, and other non-silicone defoamers may be appropriate where a particular regulatory profile, food-contact position, or downstream preference makes them attractive. They can also be less desirable where oxidation, emulsion stability, or higher dose demand becomes a concern. The right choice depends on the whole process, not on whether the label sounds more natural or more technical.
Water-based emulsions are convenient for dosing and may disperse well in aqueous media. Their weakness is physical stability: poor storage, freeze-thaw exposure, or insufficient mixing can separate the emulsion and cause inconsistent dosing. Concentrates may reduce transport volume, but their dilution and handling need more control. Confirm the supplier's storage conditions, recommended mixing practice, shelf life, and sterilization guidance.
Do Not Ignore Sterilization and Addition Method
Many selection failures happen after a good trial because the production handling method is different. Ask whether the antifoam will be added before sterilization, sterilized separately, introduced through a sterile port, or dosed during the run. Heat can alter some emulsions and affect their performance. Sterile filtration may also be impractical for certain products or may retain part of the active material. Supplier documentation should address the intended method, but site-specific confirmation is still needed.
Pre-charge addition is simple and can prevent foam at startup, but it creates continuous exposure of the culture and may reduce oxygen transfer throughout the batch. On-demand dosing limits total usage and is often better for yield protection, provided the foam sensor, pump response, and control logic are reliable. A hybrid approach is common: a small validated pre-charge followed by controlled additions only when the foam signal requires it.
Positioning matters. Adding defoamer too close to a sensor can give a false impression of success while foam remains active elsewhere. Adding it where mixing is poor can create local concentration spikes. In a well-designed system, the dosing point promotes rapid distribution without interfering with sterile boundaries or sampling practices.
A Practical Trial Plan Before You Change Suppliers
When evaluating a replacement, avoid changing chemistry, dosage strategy, and operating conditions all at once. That makes the result difficult to interpret. Start with the current antifoam as the reference. Then test one candidate at a conservative initial dose, using the same foam-control logic and comparable process conditions.
For each run, capture antifoam consumption, number of additions, foam events, dissolved oxygen behavior, gas and agitation demand, feed interruptions, final yield, and the performance of the first downstream unit operation. Review deviations with the production team, not only with purchasing. Operators often notice early warning signs such as a sticky probe, unstable foam sensor, line blockage, or unusual vessel wall deposits before those issues appear in a final report.
Only after a candidate performs consistently should you optimize dosage. Reducing the dose step by step is usually safer than beginning with an aggressive amount and trying to work backward. The lowest effective dose is not merely a cost target. It reduces the chance of oxygen-transfer loss, downstream contamination, and batch-to-batch variation.
Questions to Ask a Defoamer Supplier
Request a technical data sheet and safety documentation, but go further. Ask for the chemistry class, active content, carrier system, density, viscosity range, storage limits, recommended dilution, sterilization compatibility, and lot-to-lot quality controls. For regulated production, verify the documentation relevant to your market and end use rather than accepting a general statement of suitability.
It is also reasonable to ask whether the supplier has application experience in similar organisms and downstream processes. That information should guide trial design, not replace it. A supplier cannot know the behavior of your medium, equipment geometry, feed strategy, or impurity profile without process-specific work.
FCAS, a B2B knowledge platform covering specialty chemicals and industrial surfactant applications, can help procurement and technical teams structure this comparison around formulation stability, documentation readiness, packaging, storage, and application fit. The final approval, however, should remain tied to evidence from your own fermentation and downstream conditions.
FAQ
Can adding more antifoam lower yield?
Yes. Excessive dosing can reduce oxygen transfer, affect cell behavior, or create downstream losses. More antifoam is justified only when the process data show that foam control still requires it.
Is silicone antifoam always the most effective option?
It is often highly effective at low dosage, but effectiveness alone is not enough. Evaluate downstream compatibility, residue expectations, and membrane or purification performance before selecting it.
Should antifoam be added before fermentation starts?
A small pre-charge can be useful when early foam is predictable. For many processes, on-demand dosing better limits total antifoam exposure. The choice should follow foam timing and validated process behavior.
What is the first sign that a defoamer is hurting the process?
Watch for a change in dissolved oxygen control, increased agitation or gas demand, altered feeding behavior, or unexpected downstream fouling. Final yield is a late indicator, not the only one to monitor.
The best defoamers for fermentation are rarely selected by chemistry name or purchase price alone. Choose the product that controls foam consistently at the minimum validated dose, remains stable in your handling system, protects culture performance, and does not create a problem for the next operation. That is the standard that protects yield in real production, not just in a foam test.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+