How Ethoxylated Surfactants Improve Wetting and Cleaning in Textile Processing
How Ethoxylated Surfactants Improve Wetting and Cleaning in Textile Processing
In textile processing, poor wetting is rarely an isolated problem. It often shows up later as uneven scouring, patchy bleaching, inconsistent dye uptake, residual spinning oil, or finishing defects that are difficult to trace back to the preparation stage. A fabric may look acceptable after one operation and still create trouble in the next bath. That is why ethoxylated surfactants for textile processing are usually evaluated not simply as “wetting agents,” but as part of a wider system involving water quality, fiber type, contaminants, temperature, liquor circulation, alkali level, and rinsing capacity.
Ethoxylated surfactants are non-ionic materials produced by adding ethylene oxide units to a hydrophobic starting material, often an alcohol, fatty acid, fatty amine, or alkylphenol derivative. Their practical value comes from the balance between the water-attracting ethoxy chain and the oil-attracting hydrophobic group. This balance allows the surfactant to reduce surface tension, help water enter compact textile structures, emulsify oils, suspend detached soils, and support their removal during washing and rinsing.
The chemistry sounds straightforward. Selection is not. A surfactant that wets greige cotton quickly in a laboratory beaker may foam excessively in a jet machine, lose performance in a high-electrolyte bath, destabilize a peroxide system, or leave a residue that affects later dyeing. Technical evaluation needs to focus on process behavior rather than a single headline property.
Why Textile Wetting Requires More Than Low Surface Tension
Textile substrates resist water for different reasons. Cotton and viscose can contain natural waxes, pectins, processing oils, and dirt. Polyester, nylon, and acrylic fibers are inherently more hydrophobic and may carry spin finishes, lubricants, oligomeric residues, or soil picked up during storage and handling. Blended fabrics make the picture less tidy: the preparation chemistry must reach both hydrophilic and hydrophobic components without creating redeposition or dyeing complications.
Static surface-tension reduction is useful, but it does not fully predict real wetting. In continuous pretreatment, pad application, spraying, or rapid immersion, dynamic wetting matters. The surfactant must migrate to newly created liquid–air and liquid–fiber interfaces quickly enough to allow the bath to spread and penetrate. Dense woven constructions, yarn packages, towels, and knitted fabrics can all expose weaknesses that a simple surface-tension value fails to reveal.
Capillary penetration also depends on the fabric’s construction and trapped air. In practice, a low-foam penetrant can be more valuable than an aggressively foaming detergent, particularly where equipment relies on rapid circulation through packages or fabric ropes. Excess foam can interfere with pump performance, level control, and liquor exchange. It may also create a false impression of cleaning strength while making the process less controllable.
The Cleaning Mechanism: Wetting, Emulsification, Dispersion, and Rinsing
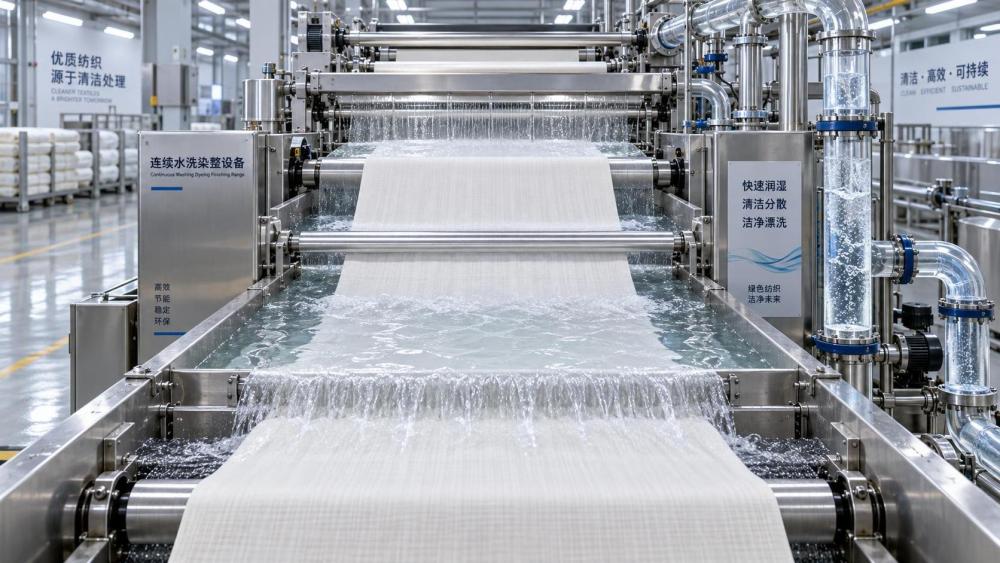
Ethoxylated non-ionic surfactants do not “dissolve” every contaminant in the same way. Their cleaning contribution usually involves several linked actions. They first improve contact between the aqueous bath and the contaminated surface. Once water reaches the fiber, the hydrophobic portion of the surfactant can associate with oils and waxes, while the ethoxylate chain keeps the resulting droplets or particles dispersed in water. Micelles may form above a concentration characteristic of the specific surfactant system, helping solubilize some hydrophobic materials.
For scouring, the critical point is not just detachment. The removed soil must remain dispersed long enough to leave with the liquor. If an emulsified oil destabilizes during cooling, dilution, or rinsing, it can redeposit on the fabric. This is one reason formulators often combine an ethoxylated wetting agent with a dispersant, sequestrant, alkali source, anti-redeposition component, or solvent-like co-surfactant. The optimal package depends on the soil load and the machinery, not on the surfactant family alone.
Rinse behavior deserves similar attention. Some high-performing detergents can be difficult to rinse from dense fabrics or absorbent substrates. Residual surfactant may alter absorbency, create uneven dye affinity, contribute to foam in downstream baths, or affect the hand of a finished textile. A technical evaluator should therefore assess cleaning and rinsing as one sequence. Strong removal in the first bath is not enough if the system leaves behind process-sensitive residues.
How Ethoxylation Level Changes Performance
The number and distribution of ethylene oxide units influence water solubility, hydrophilic-lipophilic balance, cloud point, detergency, and foam profile. Broadly speaking, lower-EO alcohol ethoxylates tend to have a more lipophilic character and can be effective in emulsifying oily contaminants or serving as co-surfactants. Higher-EO grades generally show greater water affinity and can offer stronger solubilizing or wetting behavior in aqueous systems. But these are directional tendencies, not a substitute for testing.
Cloud point is especially relevant in hot textile processes. Some non-ionic ethoxylates become less soluble above a characteristic temperature, particularly in the presence of salts or alkali. This can be useful in certain cleaning mechanisms, but it can also lead to bath haze, separation, spot risk, or reduced consistency if the formulation is not designed for the operating window. The relevant question is not whether a surfactant has a cloud point; it is whether its behavior remains acceptable at the actual bath temperature, concentration, electrolyte level, and water hardness.
Different Textile Stages Put Different Demands on the Surfactant System
In desizing and scouring, ethoxylated surfactants are commonly expected to assist with rapid wetting and the removal of waxes, oils, size residues, and particulate contamination. Their compatibility with enzymes, alkali, chelating agents, and peroxide stabilizer systems needs to be checked. An apparently minor incompatibility can reduce enzyme activity, create bath instability, or make peroxide control harder to interpret.
Bleaching introduces another layer of caution. Surfactants must not be assumed to be inert simply because they are non-ionic. A candidate should be screened within the intended bleaching formulation and temperature profile. The aim is to confirm that wetting improves without unacceptable foam, decomposition concerns, loss of whiteness consistency, or difficult wash-off. There is no useful shortcut here: fabric, water quality, and chemical package all influence the outcome.
For polyester preparation and alkaline weight-reduction environments, resistance to temperature and alkalinity becomes more demanding. Oily spin finishes can be chemically diverse, so a surfactant package that works on one supplier’s finish may not be equally effective on another. When the processing site changes fiber source or spinning oil, it is sensible to revisit the cleaning test rather than assume that the existing recipe remains robust.
In dyeing, ethoxylated surfactants may be used for wetting, leveling support, washing-off, or dispersion assistance, depending on the dye class and substrate. Yet stronger detergent action is not automatically better. With disperse dyes, for example, uncontrolled interactions with dispersants and dye particles can affect bath behavior. With reactive dyeing, salt and alkali additions can change solubility and foam. The surfactant must be assessed as part of the full recipe, including dye auxiliaries and the dyehouse’s operating sequence.
Foam Control Is a Process Requirement, Not a Cosmetic Preference
Textile teams sometimes compensate for inadequate wetting by increasing surfactant dosage. That approach can work in a small trial and fail at scale. More surfactant can mean more foam, more rinsing demand, and a higher chance of residue. In high-turbulence equipment, the useful dosage range may be narrower than expected. A low-foam alcohol ethoxylate, or a formulated blend with a suitable defoaming component, is often easier to run than a high-foaming product with impressive laboratory detergency.
It is also worth separating persistent foam from transient foam. Some systems foam during charging but collapse rapidly under processing conditions; others appear manageable at first and build foam as soils and chemical additives accumulate. A representative evaluation should include the actual water source, expected soil load where possible, operating temperature, circulation intensity, and holding time. A cylinder shake test alone can be a useful screening tool, but it is not a machine simulation.
Regulatory and Supply-Chain Questions That Should Be Asked Early
Not all ethoxylated surfactants have the same environmental or market acceptance profile. Alkylphenol ethoxylates, particularly nonylphenol ethoxylates, have faced restrictions or customer-driven phase-outs in many textile supply chains because of their degradation profile and associated environmental concerns. Whether a material is acceptable depends on its identity, intended market, customer requirements, and applicable chemical controls. It should be verified against current destination-market obligations and brand or buyer restricted-substance requirements rather than inferred from the generic term “non-ionic surfactant.”
For procurement and technical approval, the specification package should go beyond active content. Useful documents typically include a current safety data sheet, technical data sheet, composition or regulatory declaration where appropriate, batch-consistency information, storage guidance, and confirmation of relevant restricted-substance expectations. Trace contaminants, residual ethylene oxide-related concerns, odor, color, and packaging compatibility may matter in sensitive applications even when they are not the primary performance criteria.
This is where structured chemical intelligence has practical value. Platforms such as FCAS help technical and procurement teams compare specialty surfactant categories in the context of formulation stability, handling, documentation, application fit, and supply reliability. The productive conversation is not “which product is cheapest?” but “which material can be consistently qualified for this fabric, this machine, this customer specification, and this operating window?”
A More Reliable Qualification Approach
A sensible qualification program begins with a defined failure mode. Is the issue slow wetting, residual oil, poor absorbency, uneven bleaching, redeposition, foam, or post-dyeing wash-off? These problems may overlap, but they do not always require the same surfactant architecture. Testing without a clear failure definition often produces a long list of “acceptable” products and no defensible selection.
Start with laboratory screening on representative fabric and water. Then move to a pilot or production-scale trial that reflects actual liquor ratio, temperature ramp, mechanical action, bath additions, and rinse sequence. Evaluate the treated textile, not only the bath: absorbency, appearance, shade uniformity, hand, odor, residual contamination, and downstream compatibility all matter. Where recognized test methods such as absorbency or water-repellency assessments are used, the method and acceptance criteria should be agreed in advance because the relevant test depends on the fabric and intended end use.
The best ethoxylated surfactant for textile processing is rarely the product with the lowest surface tension or the strongest foam. It is the one that delivers repeatable penetration and soil removal within the real constraints of the process, then rinses cleanly enough to protect the next operation. That is a narrower and more useful definition of performance—and the one technical evaluators should insist on before approving a surfactant system.
Related News
 Antioxidants & Natural PreservativesWhat Quality Checks Matter When Sourcing Butylparaben for Personal CareButylparaben for personal care sourcing guide: compare assay, impurities, physical performance, documentation, traceability, and supplier quality to reduce formulation risk.MORE+
 Nano-microcapsule FormulationsHow Encapsulated Flavors Protect Taste During Processing and StorageEncapsulated Flavors protect taste from heat, oxygen, moisture, and storage loss. Explore smarter release, carrier selection, and processing strategies.MORE+
 Chelated Trace Element FertilizersHow Greenhouse Fertigation Systems Reduce Water and Fertilizer WasteGreenhouse fertigation systems reduce water and fertilizer waste with precise dosing, uniform irrigation, drainage monitoring, and smarter crop-zone control. Learn practical strategies.MORE+
 Supercritical CO2 Essential OilsHow Natural Essential Oil Blends Improve Consistent Product FragranceNatural essential oil blends help brands achieve consistent, appealing fragrance across batches. Explore smart blend design, stability testing, and product compatibility strategies.MORE+
 Non-ionic Surfactants & DefoamersHow to Choose Non Ionic Low Foaming Surfactants for CIP CleaningNon ionic low foaming surfactants for CIP cleaning: learn how to balance wetting, foam control, compatibility, and rinseability for reliable cleaning performance.MORE+
 Nano-microcapsule FormulationsHow Food Grade Cyclodextrin Complexes Protect Sensitive FlavorsFood grade cyclodextrin inclusion complexes help protect sensitive flavors from oxidation, evaporation, and processing loss while supporting controlled release and consistent sensory quality.MORE+
 Polymer-Coated Water Soluble NPKHow Fertilizer Coating Polymers Improve NPK Granule ReleaseFertilizer coating polymers for NPK granules improve controlled nutrient release, reduce loss risks, and enhance product consistency. Discover key selection and process insights.MORE+
 Chelated Trace Element FertilizersWhat Diammonium Phosphate Means for Crop Nutrition PlanningDiammonium Phosphate: learn how DAP supports early phosphorus access, nitrogen budgeting, smart placement, and balanced crop nutrition planning.MORE+
 Maillard Reaction Savory FlavorsHow to Assess a Flavor Bases Supplier List for Reliable SourcingGlobal Fine Chemicals & Agrochemical Intelligence Network flavor bases supplier list: assess specs, samples, supply risk, and true cost to source with confidence.MORE+
 Hydrocolloids & EmulsifiersHow Konjac Gum Powder Improves Texture in Low-Calorie FoodsKonjac gum powder improves body, stability, and mouthfeel in low-calorie foods. Discover practical tips for smoother sauces, beverages, and reduced-fat formulations.MORE+
 Supercritical CO2 Essential OilsWhat to Check Before Choosing a Botanical Essential Oils ManufacturerChoose a botanical essential oils manufacturer with confidence. Explore key checks for purity, traceability, compliance, batch consistency, and reliable supply.MORE+
 Microencapsulated FragrancesHow Fragrance Carriers for Detergents Improve Scent PerformanceFragrance carriers for detergents improve stability, fabric deposition, and long-lasting scent. Explore practical solutions for better wash-to-wear fragrance performance.MORE+
 Antioxidants & Natural PreservativesWhen Propyl Gallate Antioxidant Is the Right Choice for Oil StabilityPropyl gallate antioxidant: learn when it is the right choice for oil stability, shelf-life protection, processing compatibility, and smarter formulation decisions.MORE+
 Antioxidants & Natural PreservativesHow Potassium Sorbate Extends Shelf Life in Food and Beverage ProductsPotassium Sorbate helps food and beverage brands control yeast and mold spoilage. Explore pH, dosage, processing, and packaging strategies for reliable shelf life.MORE+
 Antioxidants & Natural PreservativesHow to Source Bulk Herbal Extracts With Reliable Quality ControlBulk herbal extracts sourcing guide: compare suppliers, verify traceability, review CoAs, and build reliable quality controls for safer, consistent purchasing.MORE+
 Antioxidants & Natural PreservativesWhat to Check Before Sourcing Butylparaben for Personal Care FormulasButylparaben for personal care sourcing guide: check market eligibility, purity, supplier controls, formula compatibility, packaging, and total risk before buying.MORE+
 Targeted Bio-pesticides & APIsChoosing Microbial Fungicides for Foliar Diseases in Integrated Crop ProgramsMicrobial fungicides for foliar diseases: learn how to match biology, formulation, tank compatibility, and timing for stronger integrated crop protection.MORE+
 Targeted Bio-pesticides & APIsHow Microbial Insecticides Control Caterpillars With Lower Crop Residue RiskMicrobial insecticides for caterpillars help protect crops with targeted early-larval control and lower residue-management pressure. Learn timing, coverage, compliance, and scouting essentials.MORE+
 Microencapsulated FragrancesHow to Add Encapsulated Laundry Fragrances Without Weakening Wash ResultsEncapsulated laundry fragrances: learn how to boost long-lasting scent while protecting cleaning power, stability, foam control, and fabric care.MORE+
 Supercritical CO2 Essential OilsHow Aroma Ingredients Shape Lasting and Skin-Safe Personal Care ProductsAroma ingredients for personal care: discover how to achieve lasting scent, formulation stability, skin safety, and confident product performance.MORE+
 Targeted Bio-pesticides & APIsInsecticides Explained Through Labels, Active Ingredients, and SafetyInsecticides explained through labels, active ingredients, formulations, and safety. Learn how to compare products, manage risk, and make informed crop protection decisions.MORE+
 Heavy-duty Industrial DegreasersHow to Select Parts Wash Cleaners for Automotive ComponentsParts wash cleaners for automotive components: learn how to match chemistry, materials, rinsing, safety, and waste controls for reliable cleaning results.MORE+
 Chelated Trace Element FertilizersHow Precision Fertigation Systems Improve Water and Nutrient ControlPrecision fertigation systems improve water and nutrient control with accurate dosing, uniform irrigation, smart monitoring, and reduced waste. Discover how to optimize crop performance.MORE+
 Hydrocolloids & EmulsifiersHow Bulk Price Factors Affect Hydrocolloid Stabilizer Blend SourcingHydrocolloid stabilizer blends bulk price: compare dosage efficiency, quality consistency, logistics, and documentation to reduce total sourcing costs.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow to Choose a Natural Sweeteners Supplier for Clean-Label ProductsNatural sweeteners supplier selection guide for clean-label products: compare formulation fit, traceability, documentation, and supply reliability.MORE+
 Non-ionic Surfactants & DefoamersWhat Cationic Surfactants Do and Where They Are UsedCationic Surfactants deliver antimicrobial action, conditioning, antistatic control, and surface treatment benefits. Explore key uses, compatibility, and safe selection tips.MORE+
 Targeted Bio-pesticides & APIsHow to Evaluate Pesticide Suspension Concentrates for Field StabilityPesticide Suspension Concentrates: learn how to evaluate field stability, redispersibility, dilution, tank-mix compatibility, and spray safety for reliable performance.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Systems for Meat Products Improve Texture and YieldHydrocolloid systems for meat products improve yield, texture, water retention, and slicing quality. Explore practical formulation strategies for stable, high-performing meat products.MORE+
 Microencapsulated FragrancesHow Laundry Fragrances for Liquid Detergents Improve Scent LongevityLaundry fragrances for liquid detergents: discover how fragrance design, deposition, and encapsulation create lasting fabric freshness and stronger product appeal.MORE+
 Nano-microcapsule FormulationsChoosing Fragrance Preparations That Perform Well in Personal WashFragrance preparations for personal wash: learn how to select options that protect clarity, stability, foam, scent performance, and packaging compatibility.MORE+
 Controlled-Release ThermodynamicsModified Cyclodextrins Explained for Controlled Fragrance ReleaseModified cyclodextrins enable controlled fragrance release, odor control, and volatile-note protection. Explore how they optimize performance in detergents, fabric care, and more.MORE+
 Microencapsulated FragrancesHow Fragrance Delivery Systems Improve Fabric Softener LongevityFragrance delivery systems for fabric softeners improve scent longevity through smart protection, reliable deposition, and controlled release for lasting freshness.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Cardamom Oil Supplier for Reliable SupplyNatural cardamom oil supplier evaluation guide: verify botanical origin, purity, batch consistency, documentation, packaging, and delivery reliability for confident sourcing.MORE+
 Maillard Reaction Savory FlavorsHow Ethyl Maltol Purity Testing Supports Flavor Safety ComplianceEthyl Maltol purity testing strengthens flavor safety compliance through identity checks, impurity profiling, supplier verification, and audit-ready documentation.MORE+
 Microencapsulated FragrancesEssential Oil Extracts Compared for Fragrance and Wellness UsesEssential Oil Extracts compared for fragrance and wellness: explore scent profiles, extraction methods, stability, safety, and sourcing insights for smarter formulation choices.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat Drives Zero Calorie Sweeteners Bulk Price in 2026Zero calorie sweeteners bulk price in 2026: compare specifications, dosage, quality, freight, and supply risk to make smarter sourcing decisions.MORE+
 EPA FIFRA & FDA GRAS RegsSynthetic Food Preservatives Rules That Support Safer FormulasSynthetic Food Preservatives: learn the rules for safer formulas, compliant use levels, validated shelf life, labeling, and reliable microbial control.MORE+
 Micelle Fluidics & ChelationHow Anionic Industrial Dispersants Improve Coating StabilityAnionic industrial dispersants improve coating stability, pigment wetting, viscosity control, gloss, and storage performance. Learn how to select and test the right solution.MORE+
 Supercritical CO2 Essential OilsHow to Choose Eucalyptus Oil Grades for Clean, Consistent ProductsChoose the right Eucalyptus Oil grade with confidence. Compare cineole content, purity, origin, processing, documentation, and application fit for consistent products.MORE+
 Micelle Fluidics & ChelationWhat Are Cationic Surfactants and Where Are They Commonly Used?Cationic Surfactants deliver powerful surface affinity for disinfection, fabric softening, hair conditioning, antistatic control, and industrial treatments. Explore key uses and selection factors.MORE+