How Can an Alkaline Degreasers Exporter Support Global Cleaning Supply
Global cleaning supply is moving toward application-specific alkaline degreasing rather than a single high-caustic product sold into every market. The shift is visible in the questions surrounding each shipment: Will the concentrate remain stable after a long transit? Can it remove drawing oil without staining aluminum? Does it rinse cleanly before coating or assembly? Are labels, safety documents, and pack sizes aligned with the destination? An alkaline degreasers exporter supports supply continuity when those questions are addressed as part of the product offer, not after a container has already left port.
Alkaline cleaners work by loosening, emulsifying, dispersing, or saponifying oily soils. Their apparent simplicity can hide important differences. A light maintenance film on painted machinery, a burnt lubricant on steel parts, a machining fluid residue, and a greasy kitchen surface do not respond to the same balance of alkalinity, surfactant package, chelation, solvent content, temperature, and contact time. Supply channels become more dependable when product ranges are organized around these differences.
Demand Is Shifting from Generic Strength to Controlled Cleaning Performance
High pH is often treated as a shortcut for cleaning power. It is only one part of the result. A strongly alkaline formula may cut heavy grease quickly on carbon steel, yet leave an unsuitable surface on aluminum, zinc, galvanized steel, painted panels, some plastics, or sensitive electronic assemblies. Conversely, a moderately alkaline formula with effective wetting and emulsification may outperform a harsher concentrate on light oils, especially where cold cleaning, low foam, or fast rinsing is required.
This distinction matters across international supply because end uses vary widely. Parts washers, spray systems, immersion tanks, manual maintenance cleaning, vehicle workshops, food-area exterior cleaning, and institutional facilities have different operating conditions. Water hardness, local wash-water temperature, equipment design, wastewater handling, and available rinse capacity also change the real performance of a degreaser.
An exporter with a technically coherent range can separate these uses instead of presenting every grade as a general-purpose product. Heavy-duty caustic degreasers, aluminum-compatible cleaners, low-foam spray-wash formulas, solvent-boosted maintenance products, and non-silicated alternatives serve different cleaning windows. Clear positioning reduces the common problem of a product appearing ineffective simply because it was applied outside the conditions for which it was formulated.
Formulation Consistency Protects the Channel After Arrival
Industrial cleaning products are often diluted before use. That makes batch consistency especially important: a small change in active alkalinity, surfactant balance, viscosity, density, or defoamer performance can become noticeable after dilution. A concentrate that looks similar in the drum may produce excessive foam in a recirculating washer, split in hard water, leave an oily film during rinsing, or require an unexpected dose adjustment.
Useful technical documentation should therefore describe more than a broad product name. It should identify the intended cleaning method, recommended dilution range, operating temperature where relevant, expected foam behavior, compatible substrates, rinse guidance, storage conditions, and basic physical characteristics used for incoming inspection. Material safety information and transport classification must match the actual shipped formulation and destination requirements.
Alkalinity should also be described with care. A pH value from a diluted sample does not automatically show how much usable alkaline reserve remains when acidic contamination enters a wash bath. Free alkalinity, total alkalinity, and titration procedures may be more meaningful for some industrial processes, but their interpretation depends on the product design and test method. Comparing values taken from unrelated test methods is a frequent source of false equivalence between concentrates.
Material Compatibility Cannot Be Reduced to a Single Label
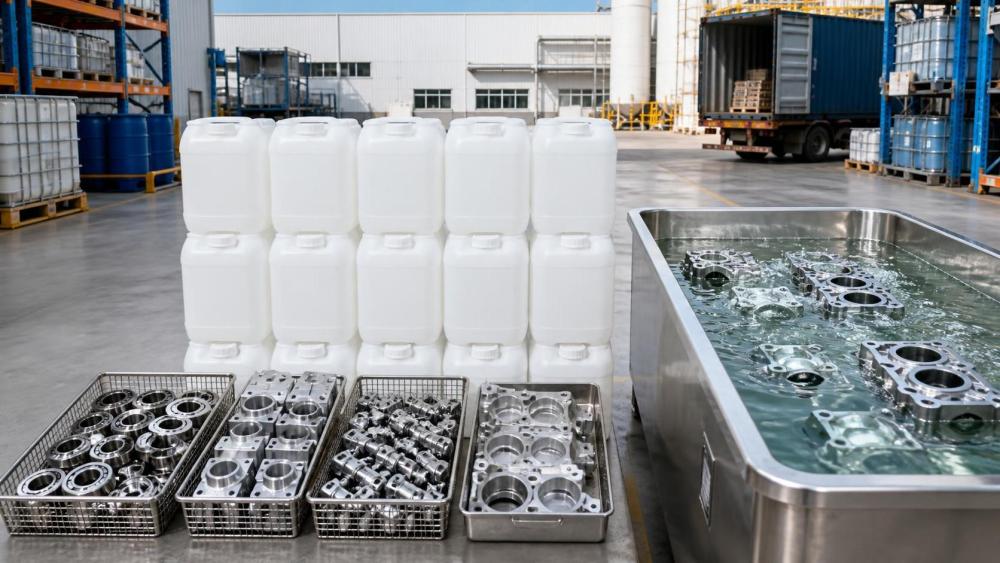
“Safe for metal” is too broad to guide a cleaning program. Carbon steel, stainless steel, aluminum alloys, copper-containing alloys, zinc-coated components, magnesium, and mixed-metal assemblies behave differently in alkaline solutions. Time, temperature, concentration, agitation, and post-cleaning rinsing all affect the outcome. A formula suitable for brief contact in a spray washer can still discolor or etch a softer metal during prolonged immersion.
Silicates, inhibitors, chelating agents, and buffering components may improve protection in some systems, but they can introduce other considerations. Silicate residues can interfere with subsequent coating or precision cleaning where residue limits are tight. Strong chelation may assist cleaning in hard water, while also changing the behavior of metal ions carried into a working bath. A corrosion inhibitor has value only within its tested dilution and operating range; it should not be interpreted as blanket protection against misuse.
Plastics and elastomers need the same attention. Polypropylene and high-density polyethylene may tolerate many alkaline concentrates well, whereas acrylics, polycarbonate, certain coatings, adhesive bonds, and soft rubber components can be more sensitive. Container selection, dispensing fittings, pump seals, trigger sprayers, and labels are part of compatibility planning. A liquid that is stable in a compatible drum can become a leakage or stress-cracking issue when transferred into an unsuitable smaller package.
The Soil Must Be Identified Before the Product Is Chosen
“Oil” is not a single soil category. Mineral cutting oils, water-miscible coolant residues, grease thickened with soap, carbonized lubricants, polishing compounds, waxes, fingerprint soils, and animal or vegetable fats respond through different mechanisms. Alkalinity is particularly useful when fatty soils can be saponified, but it may have limited effect on polymerized deposits or heavily baked contamination without heat, mechanical force, or a complementary solvent system.
A recurring field error is to judge a degreaser from the first visual change. A surface can look clean while retaining a thin hydrophobic residue that later causes poor paint adhesion, plating defects, or erratic bonding. The reverse can also occur: a darkened surface may result from chemical attack or oxidation rather than remaining soil. Water-break behavior, wipe tests, process-specific adhesion checks, and controlled comparisons on representative parts give a more useful indication than appearance alone.
- Machining and metal fabrication: Removal must be evaluated alongside flash-rust control, low foam in spray equipment, and compatibility with the next operation, such as welding, phosphating, coating, or assembly.
- Automotive maintenance: Grease removal from engines, chassis parts, and workshop tools often requires strong wetting on cold, uneven surfaces. Overspray risk matters where painted plastics, aluminum components, or electrical connectors are nearby.
- Institutional and facility cleaning: The working concern is often manageable dilution, soil suspension, rinseability, and safe use on frequently touched surfaces rather than maximum caustic strength.
- Precision and electronic cleaning: Ionic residue, water quality, drying marks, and component compatibility can outweigh raw degreasing speed. A general industrial alkaline cleaner is not automatically appropriate for these applications.
Packaging and Transport Are Part of Product Performance
Export support is tested when the product moves through temperature changes, extended storage, port handling, and local repacking. A formula should be assessed for phase stability, sediment formation, viscosity shift, container deformation, cap integrity, and label adhesion under realistic distribution conditions. Freezing and repeated heat exposure can destabilize some surfactant systems, while excessive headspace or incompatible closures can contribute to leakage in alkaline liquids.
Packaging choice should reflect the route to use. Bulk containers can simplify high-volume supply but require compatible pumps, transfer procedures, secondary containment, and reliable labeling through multiple handling stages. Smaller drums or jerrycans can make local storage and controlled issue easier, yet increase the number of closures and handling events. A concentrated product reduces freight weight per unit of working solution, but only when the local dilution process is controlled. Poorly marked dosing instructions or an unsuitable dispensing method can erase that freight advantage through overuse, inconsistent cleaning, and avoidable complaints.
Labels should remain legible after abrasion, moisture, and chemical contact. Product identifiers, dilution directions, hazard communication, storage cautions, and batch traceability need to stay connected to the physical pack. Repacking without a controlled transfer of these details creates confusion between similar grades, particularly where low-foam and high-foam products are both stocked for different equipment.
Documentation Needs to Support a Real Operating Conversation
Documentation is often treated as an administrative requirement, but it also determines how accurately a cleaning chemical is used. A technical data sheet that only lists appearance and pH leaves major operational questions unanswered. Useful documents explain the target soils, substrates excluded or requiring prior testing, dilution basis, temperature window, foam profile, contact-time limits, rinsing need, and storage range. Safety documentation should be current, consistent with labels, and available in forms suitable for the markets served.
Changes must be managed carefully. A replacement surfactant, revised preservative, altered solvent level, or new packaging source can affect foam, odor, clarity, cleaning speed, freeze-thaw behavior, or material compatibility even where the headline description is unchanged. Revision control, retained batch samples, and a clear notice process allow stock already in the channel to be distinguished from later production. That discipline is especially valuable when a cleaner is used before a sensitive downstream process.
Reliable Supply Depends on Technical Alignment Before Repeat Orders
The first shipment should establish more than a commercial specification. It should establish a shared basis for use: the soil being removed, the part material, application method, water quality, dilution equipment, target cleanliness, rinse sequence, and likely storage environment. This narrows the gap between laboratory cleaning demonstrations and routine field results.
When performance changes, the investigation should begin with the working bath rather than immediately assuming a product defect. Concentration can drift as water evaporates or as operators top up inconsistently. Oils accumulate and consume cleaning capacity. Hardness salts can reduce surfactant efficiency or deposit on surfaces. Spray pressure, nozzle condition, bath temperature, and rinse quality can all alter results. A retained concentrate sample, batch record, and basic bath-control method make it possible to distinguish formulation variation from process drift.
Global cleaning supply becomes more resilient when alkaline degreasing is treated as a controlled application system. The exporter’s contribution lies in maintaining reproducible chemistry, presenting limits plainly, protecting the product through packaging and transport, and keeping technical records aligned with the grade that reaches the cleaning operation.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+