Fatty Alcohol Ethoxylates Explained for Reliable Industrial Formulations
Fatty Alcohol Ethoxylates are among the most widely used non-ionic surfactants in industrial chemistry because they can deliver several functions at once: wetting solid surfaces, lifting oily soil, stabilizing emulsions, dispersing particles, and helping poorly soluble materials enter water-based systems. They appear in household and institutional cleaning products, textile auxiliaries, agrochemical adjuvants, coatings, metalworking fluids, pulp and paper chemicals, and specialty formulations.
Yet the name covers a broad family rather than one standard material. A C12-C14 alcohol ethoxylate with three moles of ethylene oxide behaves very differently from a C12-C14 grade with seven or nine moles, even when both are described as “fatty alcohol ethoxylates.” For formulation teams, distributors, and market researchers, the important question is therefore not whether a formulation uses an alcohol ethoxylate, but which hydrophobe, ethoxylation range, physical form, impurity profile, and performance balance it requires.
A surfactant family defined by two linked variables
Fatty alcohol ethoxylates are produced by reacting a fatty alcohol with ethylene oxide. Their general structure is an alcohol-derived hydrophobic chain linked to a hydrophilic chain of ethoxy units. The alcohol portion may be based on natural oleochemical feedstocks, such as palm kernel oil, coconut oil, tallow, or other fatty sources, or on synthetic linear alcohols derived from petrochemical routes.
The carbon-chain distribution matters. Shorter-chain materials, often in the C9-C11 or C10-C13 range, may provide strong wetting and detergency but can have different odor, solvency, foam, and environmental characteristics from longer C12-C15 or C16-C18 grades. Linear alcohol structures are generally preferred where biodegradability and predictable surfactant behavior are important. Branched alcohol ethoxylates may offer useful low-temperature handling, solubility, or wetting properties, but should not be assumed to perform identically to linear alternatives.
The second defining variable is the average ethylene oxide, commonly written as EO number or molar ethoxylation level. This indicates the average number of ethoxy units added to the alcohol. It is an average because commercial products contain a distribution of molecules rather than one single, uniform species.
Lower-EO alcohol ethoxylates tend to be more oil-soluble and are often useful for water-in-oil emulsification, oily soil removal, and certain low-water or solvent-containing systems. Mid-range grades often provide a practical balance of detergency, wetting, and emulsification. Higher-EO grades are more water-soluble and can be better suited to oil-in-water emulsions, solubilization, hard-surface cleaning, and aqueous concentrates. This is a useful starting rule, but it is not a substitute for testing: performance also depends on chain length, branching, temperature, electrolytes, other surfactants, solvents, and the soil or active ingredient being managed.
Why HLB is useful, but insufficient on its own
Hydrophilic-lipophilic balance, or HLB, is frequently used to screen non-ionic surfactants. As ethoxylation increases, HLB generally rises, indicating a stronger affinity for water. For a formulator selecting an emulsifier, HLB can help narrow the field quickly.
However, relying on HLB alone is a common source of unsuccessful scale-up. Two products with comparable HLB values can show substantially different cloud points, foam patterns, viscosity effects, electrolyte tolerance, interfacial film strength, and compatibility with actives. A pesticide emulsifiable concentrate, for example, may require an emulsifier blend that remains stable after dilution in hard water and across variable field temperatures. A single alcohol ethoxylate selected only by HLB may not provide that stability.
The same limitation applies in detergent development. A grade that removes mineral oil effectively in a laboratory test may lose efficiency when mixed with alkaline builders, hydrotropes, polymers, corrosion inhibitors, or high levels of salts. In practice, formulators use HLB as a directional tool and then evaluate actual formulation behavior: phase stability, cleaning response, dilution stability, foam, rinse quality, and storage performance.
Performance in real industrial systems
In cleaning formulations, fatty alcohol ethoxylates are valued because they lower surface tension and help water spread across contaminated surfaces. Their micelles can surround oily soil and assist its removal or suspension. They are widely used in degreasers, laundry detergents, dishwashing systems, vehicle cleaners, institutional cleaning products, and industrial maintenance fluids.
The practical performance target changes by application. For a low-foam automatic cleaning system, rapid wetting may be required without persistent foam. For manual washing or some textile processes, a more visible and stable foam profile may be acceptable or even desirable. Alcohol ethoxylates are often called “low-foam non-ionics,” but this description is too broad. Foam is affected by EO level, carbon-chain profile, concentration, temperature, spray action, water hardness, and co-surfactants. A supplier’s foam test method should therefore be reviewed before comparing grades.
In agrochemical formulations, these surfactants may serve as wetting agents, emulsifiers, dispersants, or adjuvant components. They can help hydrophobic active ingredients disperse after dilution, improve leaf-surface coverage, or support emulsion formation in liquid products. Their role should be assessed in relation to the active ingredient, solvent package, crop-use conditions, water quality, and target regulatory profile. Good performance in an emulsifiable concentrate does not automatically mean that the same grade is suitable for suspension concentrates, soluble liquids, or biological formulations.
Textile processing uses alcohol ethoxylates for scouring, wetting, washing, and dyeing-related operations. Here, low-temperature activity, resistance to process water conditions, low residue, and interaction with dyes or finishing agents can be more important than simple detergency. In coatings, pigments, inks, and polymer emulsions, the relevant questions are often whether the surfactant supports wetting and dispersion without causing excess foam, water sensitivity, film defects, or incompatibility with the binder system.
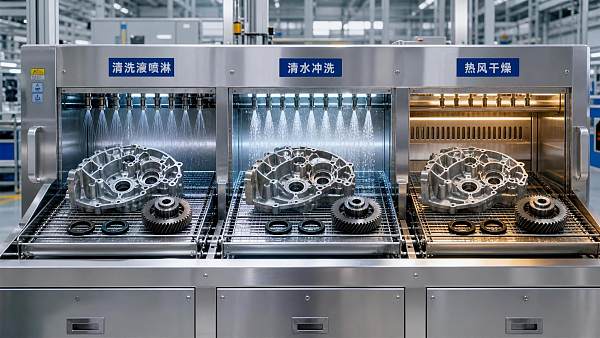
For metal cleaning and industrial degreasing, alcohol ethoxylates are commonly combined with alkalinity sources, solvents, chelating agents, hydrotropes, and corrosion-control additives. The balance between soil removal and rinse behavior is critical. A material that cleans strongly but leaves a difficult-to-rinse residue may be unsuitable for precision parts, coating preparation, or downstream processing.
Cloud point is an operational property, not merely a data-sheet number
Many fatty alcohol ethoxylates exhibit a cloud point in water: at a certain temperature, the surfactant solution becomes cloudy as solubility changes. This behavior is characteristic of many non-ionic ethoxylated surfactants and can be highly relevant in processing.
A cloud point near the expected operating temperature can change detergency, foam, emulsion stability, and appearance. In some cleaning applications, operating close to this transition can support oily soil removal. In other systems, clouding may signal a risk of instability, separation, reduced clarity, or inconsistent dilution performance. The reported cloud point also depends on concentration and test medium. A value measured in deionized water should not be treated as a direct prediction of performance in a salt-containing detergent, agrochemical tank mix, or solvent-rich concentrate.
This is one reason product comparisons should include more than a single specification sheet. Researchers should ask how a property was measured, what medium was used, and whether the supplier can provide performance data relevant to the intended formulation environment.
Compatibility: strong versatility, but no universal fit
As non-ionic surfactants, fatty alcohol ethoxylates are often compatible with anionic, amphoteric, and many cationic ingredients. This makes them useful blending partners. They can improve wetting in anionic detergent systems, adjust foam in amphoteric blends, and help solubilize fragrance oils or hydrophobic additives in some aqueous products.
Still, “non-ionic” should not be interpreted as universally compatible. High electrolyte levels can alter solubility and phase behavior. Some polymers, resins, preservatives, biocides, dyes, and active ingredients can create haze, viscosity shifts, precipitation, or separation. Strongly acidic or strongly alkaline environments, especially at elevated temperatures and long holding times, also require application-specific stability checks.
Compatibility with packaging deserves attention as well. Surfactant concentrates may affect labels, seals, liners, or certain plastics, particularly where solvents are present. Cold storage can create crystallization, increased viscosity, or phase changes in some grades. These are not necessarily product defects; they may be manageable through appropriate storage limits, warming procedures, or grade selection. They do, however, affect logistics planning and customer handling instructions.
Environmental and regulatory questions require product-specific answers
Fatty alcohol ethoxylates are often considered a more acceptable alternative to alkylphenol ethoxylates in applications where the latter face significant environmental and regulatory scrutiny. However, the two categories should not be treated as interchangeable from a compliance perspective. A formulation described as “APEO-free” should be supported by clear raw-material control, appropriate declarations, and, where needed, analytical verification.
Biodegradability is another area where broad claims can mislead. Many linear fatty alcohol ethoxylates have favorable biodegradation characteristics, but actual environmental classification and acceptance depend on the specific material, test data, regional requirements, concentration, and downstream formulation. Carbon-chain composition, branching, ethoxylation distribution, and impurities can all affect the profile. Procurement documents should request the relevant safety data sheet, regulatory status information, and biodegradability evidence where environmental claims are commercially important.
Ethoxylated materials also require attention to residual ethylene oxide and 1,4-dioxane management. These substances may arise from the manufacturing process and are relevant to occupational safety, product stewardship, and customer specifications. Acceptable limits differ by application and jurisdiction. A grade suitable for an industrial cleaner may not meet expectations for a sensitive consumer, food-contact-adjacent, or high-purity application. The correct approach is to define the required specification before sourcing rather than assuming that all alcohol ethoxylates have the same impurity controls.
How to compare supplier offerings without comparing names alone
Commercial labels such as “C12-14 7EO” are useful shorthand, but they do not guarantee equivalent formulation results between suppliers. Differences may exist in alcohol feedstock composition, average EO level, EO distribution, color, odor, water content, free alcohol content, residual catalyst-related materials, cloud point, pour point, and trace impurities. Even modest variation can matter in sensitive emulsions or low-odor finished products.
A practical comparison begins with the intended function. Is the surfactant expected to wet a hydrophobic powder, emulsify a solvent phase, remove oil, control foam, improve spreading, or stabilize a concentrate after dilution? Once the core role is defined, the buyer or technical evaluator can compare the properties that actually govern performance.
- Hydrophobe composition: carbon-chain range, linearity, source, and batch consistency.
- Ethoxylation level: average EO number and, when critical, information on distribution.
- Physical behavior: appearance, active content, water content, viscosity, pour point, and cloud point under relevant conditions.
- Application response: wetting time, detergency, emulsion stability, foam, rinse behavior, and dilution stability.
- Quality and stewardship: safety documentation, impurity specifications, regulatory declarations, traceability, and change-control practices.
- Supply practicality: packaging format, temperature-controlled logistics where necessary, lead time, storage guidance, and technical support for trials.
For multi-region supply chains, documentation consistency can be as important as chemistry. Distributors and importers may need to confirm transport classification, local inventory status, labeling requirements, and whether a supplier can maintain consistent specifications across manufacturing sites. A low purchase price can be offset quickly by reformulation work, rejected batches, unstable storage, or incomplete compliance documentation.
The most common selection mistake: treating a surfactant as a commodity
Fatty Alcohol Ethoxylates are mature, widely available materials, which can make them appear interchangeable. In straightforward applications, substitution may indeed be simple. In demanding formulations, it is not. The surfactant sits at the interface between oil, water, solids, air, and process conditions; small structural differences can therefore produce disproportionate changes in final product behavior.
The most reliable selection path is to connect the chemistry to the operational problem. Identify the phase system, temperature range, water quality, active ingredients, required foam profile, regulatory constraints, and storage conditions. Screen a short list of grades, then test the finished formulation rather than the surfactant in isolation. This approach provides a more realistic basis for product development, supplier qualification, and market assessment than choosing solely by EO number or price per kilogram.
As industrial formulations move toward lower environmental impact, more demanding performance targets, and tighter documentation expectations, alcohol ethoxylates will remain important building blocks. Their value lies not in being universal surfactants, but in offering a tunable platform. Understanding that tunability is what allows formulators and sourcing teams to use them reliably.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+