How to Choose Parts Wash Cleaners for Automotive Components Without Damage
How to Choose Parts Wash Cleaners for Automotive Components Without Damage
Introduction: Selecting parts wash cleaners for automotive components requires more than strong degreasing power. Technical evaluators must balance cleaning performance, material protection, safety, and process control.
The correct cleaner removes oils, carbon, machining fluids, polishing compounds, and particulate contamination without changing dimensions, finishes, sealing performance, or downstream assembly reliability.
A sound evaluation starts with the component and its contaminants, then compares chemistry, temperature, concentration, mechanical action, rinse quality, corrosion protection, and validation evidence.
Start With the Part, Not the Cleaner Claim
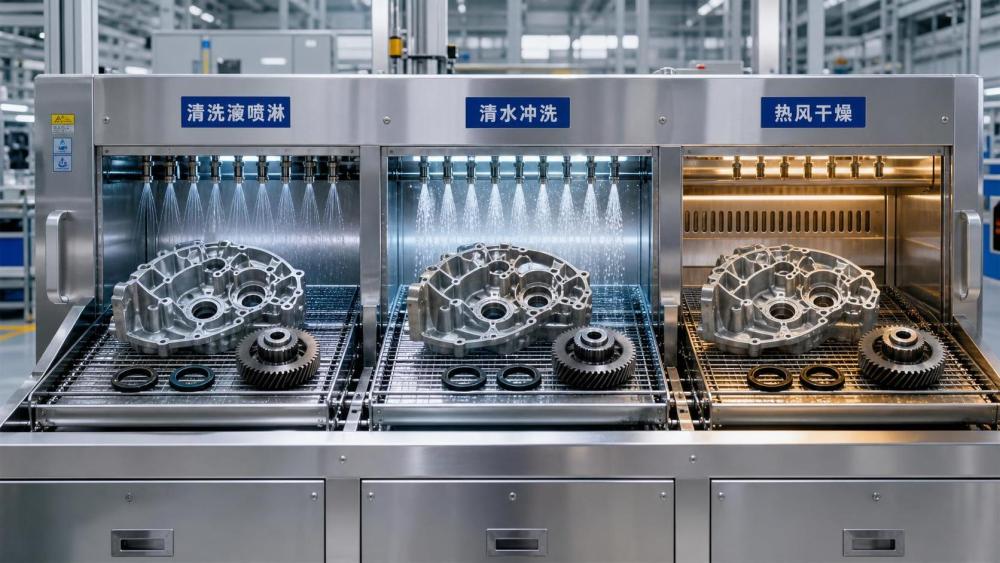
Technical teams should first identify every material exposed during washing, including base metals, coatings, elastomers, plastics, adhesives, plated surfaces, sensors, and electronic interfaces.
Automotive assemblies increasingly combine aluminum, magnesium, steel, copper, zinc alloys, engineered polymers, and rubber seals. A cleaner safe for one material may damage another.
For example, high-alkaline products may clean aluminum efficiently but can etch sensitive alloys, dull polished surfaces, discolor anodized layers, or weaken certain adhesive bonds.
Similarly, aggressive solvents may rapidly dissolve grease but can cause stress cracking in polycarbonate, swelling in elastomer seals, haze on transparent plastics, or coating softening.
Create a component-material map before requesting samples. Include material grades, surface treatments, roughness requirements, critical tolerances, and all temporary protective films or assembly lubricants.
This map prevents a common purchasing mistake: approving parts wash cleaners for automotive components based only on visible cleanliness after a short laboratory demonstration.
Visible cleanliness is not enough when cleaned parts must be painted, bonded, welded, assembled with seals, exposed to heat, or used near electrical connections.
Define the Soil Removal Requirement Precisely
Cleaner selection becomes more reliable when the soil is described by chemical type, thickness, age, cure state, location, and expected removal standard.
Common automotive soils include mineral oils, synthetic lubricants, stamping oils, drawing compounds, waxes, carbon deposits, metal fines, coolants, corrosion inhibitors, and fingerprints.
Aqueous alkaline cleaners generally perform well on saponifiable oils, particulate soils, and many machining residues when paired with sufficient temperature and mechanical energy.
Neutral or mildly alkaline systems may be preferable for mixed-material parts, sensitive aluminum components, electronic housings, decorative surfaces, and assemblies containing elastomeric seals.
Solvent-based cleaners can be effective for heavy oils, waxes, adhesives, and low-water-tolerance applications, but require stricter compatibility, ventilation, exposure, and fire-risk assessment.
Do not assume that a cleaner removing fresh oil will also remove aged, oxidized, heat-cured, or polymerized deposits from engine, transmission, or braking components.
Ask suppliers to identify the primary removal mechanism, such as emulsification, solvency, saponification, dispersion, wetting, chelation, or mechanical lift-off through spray action.
Compare Cleaner Chemistry Against Material Compatibility
Material compatibility is the central risk-control issue when selecting parts wash cleaners for automotive components. Compatibility should be demonstrated under actual operating conditions, not assumed.
Aluminum alloys deserve particular attention because high pH, elevated temperature, prolonged immersion, and inadequate inhibitor packages can cause darkening, etching, or corrosion.
Magnesium and zinc-containing parts are even more sensitive. Their evaluation should include visual inspection, mass change, corrosion evidence, dimensional checks, and coating adhesion testing.
Ferrous components require adequate flash-rust protection after washing. The cleaner, rinse stage, drying method, handling time, and plant humidity all influence corrosion outcomes.
Copper, brass, and electrical contact materials may tarnish when exposed to unsuitable alkalinity, oxidizing ingredients, sulfur-containing contaminants, or poorly controlled rinse water.
For plastics and elastomers, review supplier compatibility data for the specific polymer grade. General statements such as “plastic-safe” provide insufficient technical assurance.
Useful compatibility tests include immersion exposure, cyclic washing, elevated-temperature exposure, tensile testing for seals, gloss checks, hardness measurement, and microscopic surface examination.
Where a part contains bonded seals or overmolded elements, test the assembled configuration. Isolated coupon testing can miss capillary retention, adhesive attack, or trapped-residue problems.
Assess Operating Conditions as Part of the Formula
A cleaner is not evaluated independently from its operating window. Temperature, concentration, dwell time, spray pressure, agitation, and bath contamination determine practical performance.
Higher temperature often improves oil removal and reduces viscosity, but it can accelerate chemical attack, increase evaporation, destabilize emulsions, and raise energy consumption.
Increasing concentration may improve cleaning margins, yet it can increase residue formation, foam, wastewater load, and risk to aluminum, coatings, and sensitive polymers.
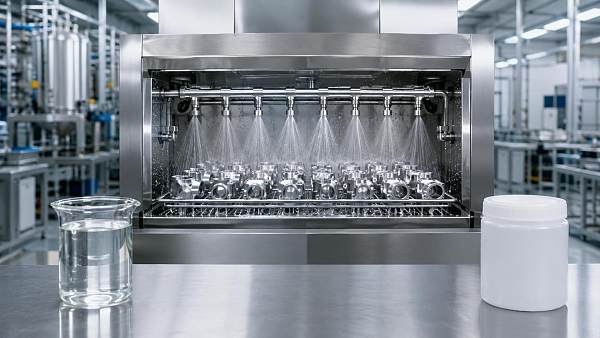
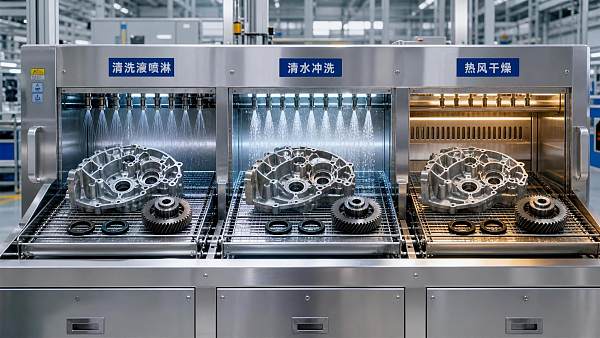
Spray washing provides strong mechanical action and is suitable for complex geometries, but excessive pressure can drive fluid into connectors, bearings, cavities, and sealed interfaces.
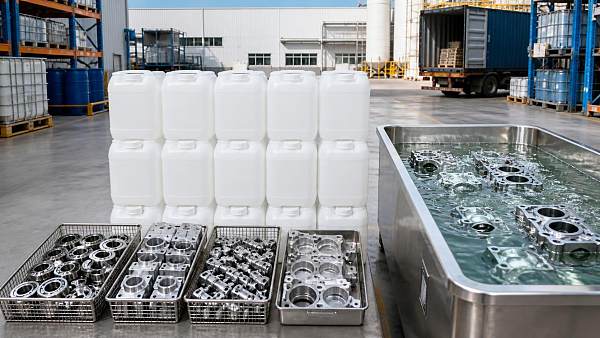
Immersion systems improve access to internal channels and recessed surfaces. However, longer contact times require closer control of material attack and carryover between stages.
Ultrasonic cleaning can release fine particles from difficult geometries, but cavitation may harm fragile assemblies, thin coatings, bonded structures, or components with entrapped air.
During trials, document the entire process recipe rather than only the product name. A repeatable specification needs concentration limits, temperature range, cycle time, and maintenance rules.
Make Rinsing and Drying Part of the Validation Plan
Many cleaning failures occur after the main wash stage. Residual surfactants, salts, dissolved soils, and poor-quality water can compromise otherwise successful cleaning results.
Rinse quality matters especially before painting, adhesive bonding, precision assembly, leak testing, electrical inspection, and coating operations where minor residues affect performance.
Specify rinse-water quality according to downstream sensitivity. Hard water may leave mineral deposits, while excessive conductivity can indicate ionic residue risks on critical parts.
Counterflow rinsing can reduce water use and cleaner carryover. Multiple rinses may be justified where components have complex passages or high cleanliness specifications.
Drying must remove retained water without overheating sensitive materials. Air knives, heated air, vacuum drying, and centrifugal methods should match component geometry and production volume.
Inspect hidden areas after drying, including blind holes, threads, channels, connector cavities, and gasket grooves. These areas can retain both soils and cleaning chemistry.
For corrosion-sensitive steel parts, define the maximum allowable time between washing, drying, packaging, and assembly. Temporary protection may be necessary in humid facilities.
Use Measurable Acceptance Criteria Instead of Visual Inspection Alone
Visual appearance remains useful, but it should not be the sole acceptance criterion. Many performance-critical contaminants are invisible after washing and drying.
Choose testing methods based on the downstream process. Water-break testing can indicate surface wetting, while gravimetric analysis measures residual nonvolatile contamination more directly.
Particle counting is important for hydraulic, fuel-system, transmission, and precision-machined components. Define particle size ranges, extraction methods, and acceptable contamination limits.
Contact-angle measurement can support coating and bonding evaluations, although results require controlled handling and should be interpreted alongside practical adhesion or coating tests.
For electronic or electrically sensitive components, ionic contamination testing and insulation-resistance checks may be more relevant than conventional degreasing assessments.
Where parts will be bonded, painted, or sealed, run downstream validation. Confirm coating adhesion, adhesive cure, gasket performance, and leak-test results after representative cleaning cycles.
Include both immediate and aged samples. Some compatibility failures, such as flash corrosion, stress cracking, or adhesion loss, become visible only after storage or thermal exposure.
Evaluate Bath Life, Contamination Control, and Process Stability
A laboratory-clean result does not prove production suitability. Technical evaluators should assess how the cleaner performs as oils, particles, salts, and process contaminants accumulate.
Bath loading changes cleaner concentration, pH, foam behavior, oil separation, corrosion protection, and rinse carryover. These shifts can create inconsistent results between production batches.
Ask whether the formulation supports skimming, coalescence, filtration, ultrafiltration, or oil-splitting behavior. The preferred approach depends on soil type and wash-system design.
Filtration protects critical components from redeposition of metal fines and abrasive particles. It is particularly important for precision parts with narrow channels or sealing surfaces.
Monitor practical control parameters, including concentration, alkalinity, conductivity, pH, temperature, oil loading, foam level, and corrosion-inhibitor performance where applicable.
A supplier should provide a clear bath-maintenance method, test frequency, replenishment approach, discard criteria, and guidance for managing abnormal contamination events.
Stable process control lowers the likelihood of intermittent cleaning defects, unplanned downtime, rejected assemblies, corrosion complaints, and costly investigations after shipment.
Include Safety, Regulatory, and Wastewater Factors Early
Cleaner selection affects more than technical performance. It also changes worker exposure, ventilation requirements, fire controls, wastewater treatment, transportation obligations, and documentation workload.
Review the safety data sheet for corrosivity, volatility, flammability, inhalation hazards, sensitization concerns, and recommended personal protective equipment under actual use conditions.
Low-odor or water-based does not automatically mean low risk. High alkalinity, aerosolized spray mist, and elevated operating temperatures can still create meaningful exposure concerns.
Confirm whether the formulation contains regulated substances, restricted solvents, persistent fluorinated materials, heavy metals, or ingredients that complicate customer compliance requirements.
Wastewater planning should consider oil emulsification, chemical oxygen demand, metal contamination, treatment compatibility, sludge generation, discharge limits, and disposal cost.
For global automotive supply chains, request current technical data, safety documentation, regulatory declarations, and consistent batch-identification practices from the cleaner supplier.
FCAS recommends treating documentation quality as a supplier-evaluation factor because incomplete chemical information increases qualification delays and creates avoidable compliance uncertainty.
Build a Practical Qualification Matrix for Supplier Comparison
A structured comparison matrix helps technical teams move beyond subjective sample feedback. Score each candidate cleaner against defined criteria and assign evidence-based weighting.
Core categories should include soil removal, material compatibility, corrosion control, rinse performance, drying behavior, bath life, operating cost, safety, wastewater impact, and supplier support.
Weighting should reflect component risk. A cleaner for a steel bracket may prioritize throughput, while a cleaner for electronic fuel-system parts requires stricter residue control.
Request trials using production-representative soils, parts, equipment, water quality, loading rates, and cycle times. Simplified tests can be useful, but they should not replace validation.
Document failure thresholds before testing begins. This prevents teams from adjusting standards after reviewing results and makes cross-functional approval more defensible.
Include procurement, quality, production, environmental health and safety, and downstream-process representatives in the final decision when the cleaner affects multiple departments.
The lowest purchase price rarely represents the lowest total cost. Consider energy use, bath replacement, rejects, maintenance, water consumption, labor, downtime, and compliance burden.
Conclusion: Choose the Lowest-Risk Cleaning System
The best parts wash cleaners for automotive components are not necessarily the strongest products. They are the systems that consistently remove required soils without harming materials or processes.
Technical evaluators should begin with component materials and contaminants, then validate chemistry, operating conditions, rinsing, corrosion control, measurable cleanliness, and long-term process stability.
When supplier claims are supported by representative trials, compatibility data, bath-management guidance, and complete documentation, cleaner selection becomes a controlled engineering decision rather than a purchasing gamble.
A disciplined qualification process protects component quality, reduces downstream failures, supports regulatory readiness, and helps automotive manufacturers maintain reliable cleaning performance as materials and assembly designs evolve.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+