How Acidic Metal Cleaning Chemicals Reduce Rework and Maintenance Costs
Rework in metal processing often starts with a surface that looked acceptable at first inspection but still carried oxide film, heat tint, light rust, embedded scale, alkaline residue, or hard water salts. When that surface moves into coating, welding, plating, assembly, or storage, the remaining contamination can cause adhesion failure, uneven appearance, flash corrosion, staining, poor conductivity, or fit problems. Acidic metal cleaning chemicals are usually selected when neutral or alkaline systems cannot reliably dissolve mineral-based deposits. The cost value comes from removing the layer that keeps forcing the same part back into cleaning, polishing, or repair.
A cheaper cleaner can become expensive if it requires longer immersion time, repeated brushing, extra rinsing, or unplanned line stops. In contrast, a well-matched acidic cleaner may shorten the cleaning window because it attacks oxides and inorganic soils directly. That can reduce labor tied to manual touch-up, lower the amount of rejected work-in-progress, and stabilize downstream steps that depend on a uniform metal surface. The saving does not come from the drum price alone. It usually appears in fewer repeat cycles, less tool contamination, and fewer maintenance calls caused by residue left inside tanks, spray lines, fixtures, and transfer racks.
Why rework often begins in the cleaning stage
Many cleaning problems are created by a mismatch between soil type and chemical action. Oil, drawing lubricants, and waxes usually need surfactants or alkaline chemistry first. Oxides, rust films, weld discoloration, and inorganic scale often respond better to acids. If an acidic product is used as a universal cleaner without understanding the incoming contamination, the line may remove one problem while leaving another behind. A part can leave the bath brighter but still carry carbonized oil, polishing compound, or smut. Rework follows because the surface condition was visually improved without being chemically clean enough for the next process.
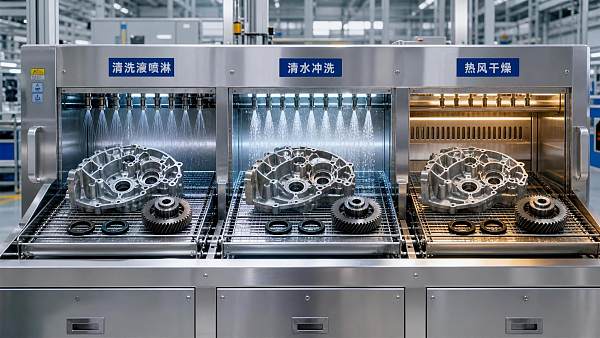
The reverse mismatch is just as common. Facilities sometimes keep extending the life of alkaline cleaners against a surface that now carries heavier oxide loading, water scale, or post-heat-treatment discoloration. Operators may compensate with hotter baths, longer dwell time, or repeated passes. Those adjustments consume time, add energy cost, and still may not restore consistency. When acidic metal cleaning chemicals are introduced at the correct point in the sequence, the process often becomes simpler: remove oil first if needed, dissolve oxide and mineral residue in a controlled acid stage, then rinse thoroughly before passivation, coating, or assembly.
Where acidic chemistry cuts maintenance cost
Maintenance expense is not limited to the cleaning bath itself. Residual oxides and mineral salts can build up on spray nozzles, pumps, heat exchangers, conveyors, and holding fixtures. In recirculating systems, that buildup may restrict flow, distort spray pattern, and create uneven cleaning across the load. A system then appears to have a chemistry problem when the real issue is hardware fouling. Proper acidic cleaning can reduce this accumulation because it keeps both the part and parts of the cleaning line closer to their intended operating condition.
There is also a less obvious maintenance effect at the interface between cleaned metal and storage. If a surface leaves the line with acid drag-out, chloride residue, or incomplete rinse water removal, corrosion may appear during staging or shipment. That creates repeat handling, repackaging, and equipment cleanup around storage areas. A suitable formulation paired with a realistic rinse design lowers that risk. The maintenance benefit comes from cleaner tanks and racks, but also from avoiding corrosion-related cleanup outside the cleaning area.
Material compatibility decides whether savings are real
Acid strength alone says very little about operating cost. Carbon steel, stainless steel, copper alloys, aluminum, galvanized surfaces, and mixed-metal assemblies do not respond the same way. A formulation that removes scale quickly from steel may etch aluminum, darken brass, or attack zinc layers. If the cleaner strips too aggressively, surface roughness can rise, dimensional tolerance may shift, and decorative finish quality can drop. That turns the cleaning stage into the cause of rework rather than the cure.
Compatibility should be reviewed with the actual substrate, not the generic metal family listed in a catalog. The same stainless grade may behave differently after welding, laser cutting, stamping, or heat treatment. Aluminum castings with trapped soils can react differently from rolled sheet. Fasteners assembled with dissimilar metals may hold acidic solution in crevices, where corrosion continues after the visible surface appears clean. A technically acceptable product on coupons can still fail on production geometry.
That is why a purchasing comparison should look beyond active acid type and concentration range. Inhibitors, wetting behavior, foam profile, residue level after rinse, and sensitivity to dissolved metal loading all affect the total cost of use. An inhibited acidic cleaner with stable performance across changing bath conditions may prevent more scrap than a more aggressive alternative that loses control as iron, copper, or calcium accumulates.
Bath control matters more than nominal concentration
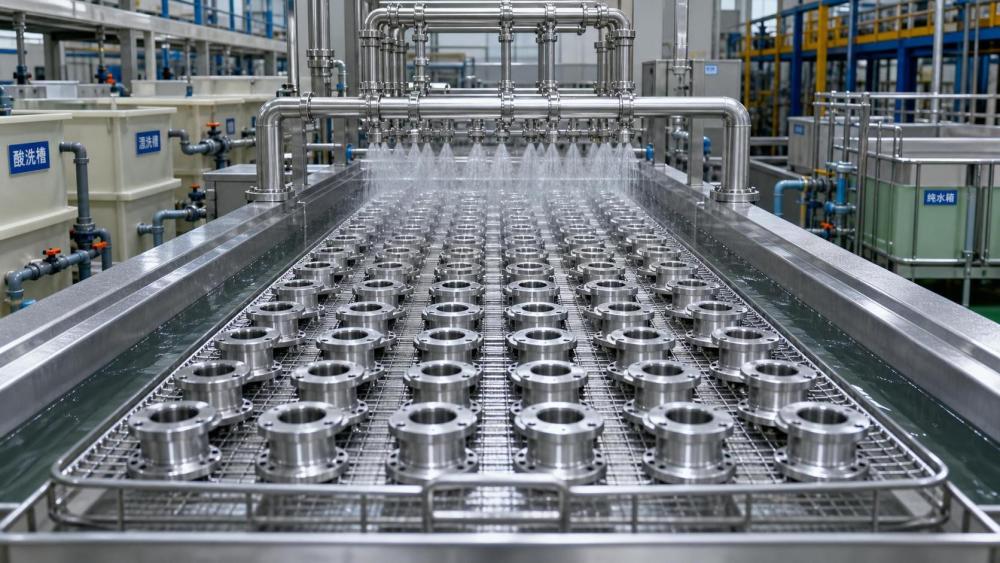
Some of the worst rework patterns come from assuming that a fresh-bath concentration defines the whole process. In actual production, acidic metal cleaning chemicals change as they dissolve scale, pick up metal ions, mix with dragged-in oils, and lose activity through carryout. A bath that still tests within the original concentration window may already be giving poor wetting or uneven attack because contamination has shifted the chemistry. If only concentration is monitored, the line can continue producing borderline surfaces until failure becomes visible downstream.
Useful control points often include free acid, total acid, dissolved metal loading, sludge formation, bath temperature, contact time, and rinse conductivity. The right mix depends on whether the system is immersion, spray, ultrasonic, wipe-on, or circulation cleaning for closed equipment. These details influence replacement frequency and maintenance intervals. A product that appears economical per shipment may need more frequent dumping if it is intolerant of metal pickup or hard-water conditions.
Water quality deserves more attention than it usually gets. Hardness minerals can react with some formulations, reduce effective cleaning, and leave deposits that look like incomplete rinsing. In surface-sensitive applications, poor rinse water can recreate the same spotting problem the acid stage was supposed to remove. That means the cleaning chemical gets blamed for a utility issue, and more material is purchased without solving the defect. Evaluating the full cleaning circuit often prevents this kind of false economy.
Common specification gaps that lead to hidden cost
Many chemical quotations are compared on packaging size, delivery lead time, and stated application range, but cost exposure often sits in the omissions. If the technical sheet does not clearly state the metals suitable for contact, the temperature window, recommended construction materials for tanks and pumps, sludge behavior, ventilation considerations, and rinse requirements, extra work shifts to the plant after purchase. The line then spends time discovering whether the cleaner attacks seals, clouds sight glasses, or requires a different dosing routine than the previous product.
Transport and storage also influence cost. Some acidic materials may require tighter segregation from alkalis, oxidizers, or reactive metals during warehousing. Others can crystallize or separate if exposed to low temperature, which creates dosing inconsistency after delivery. If these conditions are not aligned with site practice, the issue shows up as waste, handling delay, or quality drift rather than as a straightforward supply problem.
Another gap appears when the chemical is evaluated only in the cleaning tank and not against the full production sequence. Metal cleaned for powder coating, electroplating, adhesive bonding, precision assembly, or food-contact equipment maintenance does not have the same tolerance for residue. A cleaner that is acceptable before rough fabrication may be unsuitable before a sensitive finishing step. Rework can then appear far away from the cleaning line, making root cause harder to identify.
Operational signals that an acidic cleaner is reducing total cost
The strongest sign is usually process stability rather than a dramatic visual change. Parts exit the cleaning stage with more consistent wetting, fewer water breaks, and less variation between rack positions or batch centers. Downstream coating or finishing becomes less erratic. Manual intervention drops because fewer pieces need spot treatment with abrasive pads, hand acids, or repeat immersion. Equipment around the line stays cleaner for longer periods, especially nozzles, transfer hooks, and rinse sections.
Waste handling can also become more predictable. Some formulations generate heavy sludge quickly as they dissolve scale and metal fines, while others keep byproducts suspended until filtration or bath replacement. Neither approach is automatically better; the practical issue is whether the behavior fits the site's maintenance rhythm. If solids load overwhelms filtration or makes tank cleanout frequent and messy, a lower unit price may still create higher operating cost.
Comparing acidic cleaners without oversimplifying the decision
Acid type matters, but so does formulation design. Organic acids may be selected where gentler treatment or lower odor is preferred, though cleaning speed and residue behavior should still be tested under realistic conditions. Mineral acid-based products can be effective on stubborn oxide and scale, but inhibitor quality, equipment compatibility, and rinse demand become more important. Blended systems that include surfactants, dispersants, or corrosion inhibitors may perform better on mixed soils than a simple acid concentrate.
In practical sourcing terms, comparison should include:
- How the cleaner behaves on the actual contamination mix rather than on clean metal coupons.
- Whether it maintains performance as dissolved metal rises during normal production.
- The construction materials required for tanks, pumps, seals, and transfer piping.
- How easily it rinses, especially before coating, plating, adhesive application, or high-purity handling.
- What kind of residue, odor, or visible staining may remain if rinse quality fluctuates.
- How much operator intervention is needed when bath activity starts to drift.
These points are more useful than a simple strong-versus-mild comparison because rework usually comes from instability, not from insufficient label claims.
Where process coordination affects chemical cost
Cleaning chemistry is often purchased by one function and lived with by several others. The line that receives incoming metal, the team running pretreatment, maintenance staff responsible for pumps and tanks, and the group handling finishing defects may all see different parts of the same problem. If those observations are not connected, an acidic cleaner can be replaced repeatedly without resolving the true cause of rework. One site may focus on rust removal speed while another cares more about rinse burden, bath life, or compatibility with wastewater neutralization. The lower total cost usually appears when those conditions are discussed before the product is locked in.
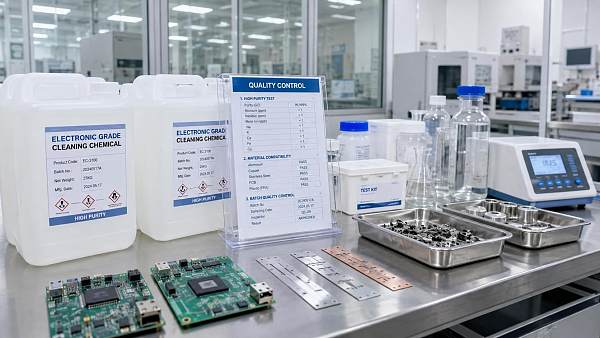
In sectors dealing with industrial surfactants, specialty solvents, or high-purity cleaning materials, this coordination becomes even more important because small residue differences may affect later process reliability. A metal cleaner that performs well in general fabrication may still be unsuitable where surface films interfere with conductivity, seal integrity, or contamination control.
Acidic metal cleaning chemicals reduce rework and maintenance costs when they are matched to the metal, the soil, the equipment, and the next step after cleaning. The wrong product can still make the surface look clean. The right one leaves fewer surprises in finishing, fewer deposits in the system, and fewer maintenance tasks created by the cleaning stage itself.
Related News
 Antioxidants & Natural PreservativesHow Propionates Extend Shelf Life While Meeting Food Safety RequirementsPropionates extend shelf life by controlling mold in bakery and moisture-sensitive foods. Explore smart dosage, compliance, supplier quality, and safer distribution strategies.MORE+
 Maillard Reaction Savory FlavorsHow Concentrated Flavor Pastes Solve Batch-to-Batch Flavor VariationConcentrated flavor pastes help manufacturers reduce batch-to-batch variation with precise dosing, reliable dispersion, and stronger sensory consistency.MORE+
 Nano-microcapsule FormulationsWhat to Verify When Choosing a Cyclodextrin Inclusion Complexes ManufacturerChoose a cyclodextrin inclusion complexes manufacturer with confidence: verify complexation evidence, loading, stability, process control, and batch consistency.MORE+
 Zero-Calorie Sweeteners & AcidulantsHow Liquid Flavors for Soft Drinks Improve Taste Consistency at ScaleLiquid flavors for soft drinks help manufacturers achieve reliable taste consistency at scale through accurate dosing, controlled mixing, stability management, and sensory quality control.MORE+
 Heavy-duty Industrial DegreasersHow to Evaluate a Degreasing Surfactants Factory for Industrial CleaningDegreasing surfactants factory evaluation guide: compare cleaning performance, foam control, quality consistency, documentation, compatibility, and supply reliability.MORE+
 Zero-Calorie Sweeteners & AcidulantsWhat to Check When Choosing a Saccharin Sodium Supplier for Global OrdersChoose a reliable saccharin sodium supplier for global orders. Learn how to assess quality, documentation, packaging, export readiness, and total landed reliability.MORE+
 Non-ionic Surfactants & DefoamersHow Non Ionic Industrial Dispersants Prevent Sedimentation in Water Based FormulasNon ionic industrial dispersants help prevent sedimentation in water-based formulas. Discover practical controls for stable, redispersible industrial suspensions.MORE+
 Antioxidants & Natural PreservativesHow Oxidation Resistant Flavor Encapsulates Protect Taste During ProcessingOxidation resistant flavor encapsulates help protect delicate taste through heat, oxygen, and storage. Discover how to improve flavor retention, release, and processing consistency.MORE+
 Polymer-Coated Water Soluble NPKHow to Choose Resin Coated NPK Fertilizers for Efficient Nutrient ReleaseResin Coated NPK Fertilizers: learn how to match release duration, nutrient profiles, granule quality, and supplier reliability to your crop programme for better efficiency and lower costs.MORE+
 Microencapsulated FragrancesHow Cyclodextrin Inclusion Complexes for Fragrances Improve Scent LongevityCyclodextrin inclusion complexes for fragrances enhance scent longevity through controlled release, improved stability, and application-specific performance. Discover how to optimize lasting aroma.MORE+
 Hydrocolloids & EmulsifiersHow Sodium Alginate for Textile Printing Improves Paste ControlSodium alginate for textile printing improves paste control, sharpens print definition, and supports reliable reactive dye production. Explore key formulation insights.MORE+
 Antioxidants & Natural PreservativesHow to Choose Green Tea Extract for Stable, Consistent FormulationsGreen Tea Extract selection guide for stable, consistent formulations—compare standardization, solubility, carriers, stability, and batch quality with confidence.MORE+
 Maillard Reaction Savory FlavorsHow Reaction Flavors Create Richer Taste in Baked and Savory FoodsReaction Flavors bring roasted, toasted, and savory depth to bakery, snacks, sauces, and plant-based foods. Learn how to select profiles that perform after processing.MORE+
 Maillard Reaction Savory FlavorsCan Flavor Bases Withstand High-Temperature Baking Without Losing Flavor?Can flavor bases withstand high temperature baking? Discover how heat, moisture, encapsulation, and formula design affect flavor retention in baked goods.MORE+
 EPA FIFRA & FDA GRAS RegsHow High Intensity Sweeteners for Tabletop Use Meet Labeling StandardsHigh intensity sweeteners for tabletop use: discover how accurate labeling, serving claims, ingredient lists, nutrition data, and regional rules support compliant market entry.MORE+
 Antioxidants & Natural PreservativesIs TBHQ for Shortening Safe and Effective for Longer Shelf Life?TBHQ for shortening: discover how safe, compliant antioxidant use can reduce rancidity, protect quality, and support longer shelf life through validated controls.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Choosing an Electronic Cleaning Chemicals FactoryElectronic cleaning chemicals factory selection guide: evaluate purity, compatibility, residue control, quality consistency, documentation, and total process cost.MORE+
 Hydrocolloids & EmulsifiersHow Thickening Agents Improve Texture and Stability in Food FormulasThickening Agents improve food texture, stability, suspension, and mouthfeel. Discover how to select the right solution for sauces, beverages, desserts, and more.MORE+
 Ultra-pure Semiconductor CleanersSelecting Low Residue Semiconductor Wafer Cleaners for Critical ProcessesLow residue semiconductor wafer cleaners: learn how to select compatible, rinse-ready solutions that protect critical processes, reduce contamination risk, and support reliable yield.MORE+
 Synthesis CAPEX & Yield ROIHow to Evaluate a Semiconductor Process Cleaners Manufacturer for YieldSemiconductor process cleaners manufacturer evaluation guide: assess purity, lot consistency, rinse behavior, compatibility, and change control to protect wafer yield.MORE+
 EPA FIFRA & FDA GRAS RegsWhat to Check Before Choosing a Sucralose Supplier for Food ProductionChoose a reliable sucralose supplier with confidence. Explore essential checks for quality, compliance, batch consistency, traceability, packaging, and supply reliability.MORE+
 Polymer-Coated Water Soluble NPKWhich Specialty Fertilizers Best Support High-Value Crop Production?Specialty Fertilizers for high-value crops: compare controlled-release, water-soluble, micronutrient, and biostimulant options for precision, quality, and reliable results.MORE+
 Supercritical CO2 Essential OilsHow to Evaluate a Natural Aroma Chemicals Manufacturer for Reliable SupplyNatural aroma chemicals manufacturer evaluation guide: verify traceability, batch consistency, compliance, application support, capacity, and total cost to secure reliable supply.MORE+
 Chelated Trace Element FertilizersChoosing Chelated Magnesium Fertilizers for More Efficient Crop NutritionChelated Magnesium Fertilizers: learn how to match product stability, water quality, and application methods for efficient crop nutrition and stronger results.MORE+
 Targeted Bio-pesticides & APIsHow Organic Botanical Insecticides Can Improve Integrated Pest ManagementOrganic botanical insecticides can strengthen IPM through targeted pest control, smarter monitoring, safer application, and better protection of crops and beneficial insects.MORE+
 Hydrocolloids & EmulsifiersHow Hydrocolloid Stabilizer Blends Keep Sauces Smooth and StableHydrocolloid stabilizer blends for sauces help prevent separation, improve texture, and deliver smooth, reliable performance from production to shelf.MORE+
 Non-ionic Surfactants & DefoamersWhat to Check Before Buying Low Residue Surfactants WholesaleLow residue surfactants wholesale: learn what to check for composition, rinse performance, batch consistency, and supplier reliability before placing bulk orders.MORE+
 Non-ionic Surfactants & DefoamersWhy Non Ionic Semiconductor Surfactants Help Control Particle DefectsNon ionic semiconductor surfactants help reduce particle defects through better wetting, dispersion, rinse control, and high-purity process qualification.MORE+
 Ultra-pure Semiconductor CleanersHow to Evaluate a Semiconductor Cleaners Factory for Ultra-Pure SupplySemiconductor cleaners factory evaluation guide: verify ultra-pure specifications, contamination controls, packaging integrity, and supply resilience before qualification.MORE+
 Hydrocolloids & EmulsifiersHow Cold Soluble Hydrocolloid Systems Improve Instant Sauce TextureCold soluble hydrocolloid systems help instant sauces achieve smooth, stable texture, controlled viscosity, and better suspension—learn how to optimize hydration and mouthfeel.MORE+
 Non-ionic Surfactants & DefoamersHow Can an Alkaline Degreasers Exporter Support Global Cleaning SupplyAn alkaline degreasers exporter supports global cleaning supply with stable formulations, tailored performance, compliant packaging, and reliable technical guidance.MORE+
 Supercritical CO2 Essential OilsWhat Should You Know About Natural Aroma Chemicals and Their UsesNatural Aroma Chemicals: explore how to select, test, and formulate natural aroma ingredients for fragrances, food, personal care, and home care products.MORE+
 Zero-Calorie Sweeteners & AcidulantsAre High Intensity Sweeteners for Tabletop Use Right for Your ProductExplore high intensity sweeteners for tabletop use: compare taste, carriers, serving cost, stability, packaging, and compliance to build a successful product.MORE+
 Heavy-duty Industrial DegreasersHow to Choose Parts Wash Cleaners for Automotive Components Without DamageParts wash cleaners for automotive components: learn how to remove oils and residues while protecting metals, plastics, seals, coatings, and downstream assembly performance.MORE+
 Hydrocolloids & EmulsifiersHow Does Locust Bean Gum Powder Improve Texture in Clean-Label FoodsLocust bean gum powder improves clean-label food texture with smoother body, better water control, and reliable stability across dairy alternatives, sauces, bakery, and frozen desserts.MORE+
 Antioxidants & Natural PreservativesWhy Ferulic Acid Matters in Modern Antioxidant FormulationsFerulic Acid helps modern formulations enhance oxidative stability, protect sensitive ingredients, and support differentiated product performance across key applications.MORE+
 Chelated Trace Element FertilizersHow to Use Triple Superphosphate for Phosphorus Deficient SoilTriple superphosphate for phosphorus deficient soil: learn soil testing, precise rates, smart placement, and pH management to improve crop phosphorus uptake.MORE+
 Hydrocolloids & EmulsifiersWhat Determines Konjac Gum Bulk Price for Reliable Cost PlanningKonjac gum bulk price depends on grade, glucomannan content, logistics, and functional performance. Learn how to compare quotes and plan reliable landed costs.MORE+
 Hydrocolloids & EmulsifiersHow to Choose Food Stabilizers for Dairy Drinks Without Texture IssuesFood stabilizers for dairy drinks: learn how to prevent separation, sediment, and gummy texture with the right protein-compatible system and process controls.MORE+
 Microencapsulated FragrancesHow Microencapsulated Fragrance Systems Improve Long-Lasting ScentMicroencapsulated fragrance systems protect scent, control release triggers, and deliver longer-lasting fragrance across laundry, personal care, and cleaning products.MORE+